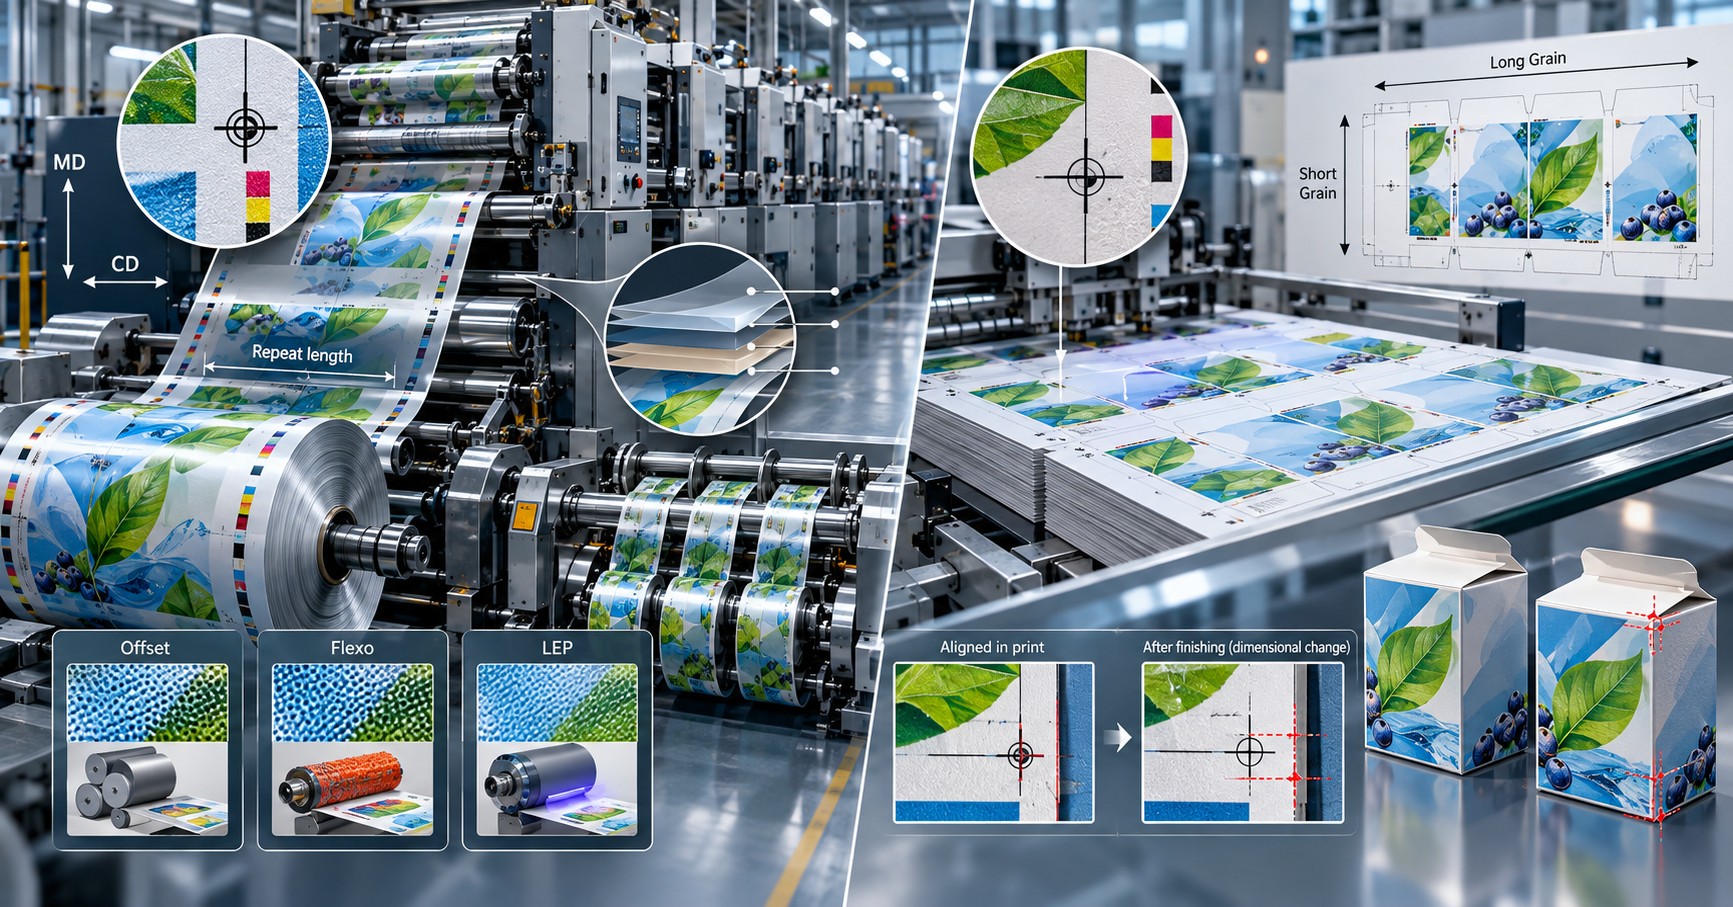
The Hidden Geometry of Printing
Why a perfectly registered print can become the wrong package
By Ronen Dolev
A press can be operating correctly, all color separations can be in excellent register, and the approved artwork can look exactly as intended. Yet at the die-cutter, laminator, slitter, or form-fill-seal machine, the job may no longer fit. A fold lands inside a graphic element; an eye mark is detected, but the cut falls in the wrong place; a pouch image becomes too short for the sealing window.
The instinctive response is often to correct registration at the press. But color registration may still be perfect. What has changed is the geometry of the printed image, the substrate, or their position relative to the converting tool. The critical question is therefore not simply, "Is the print registered?" but which process stage changed the dimensions, under what measurement conditions, and whether that change can be controlled.
This article follows dimensional accuracy from prepress through offset, flexography, and liquid electrophotography (LEP), then through lamination, slitting, die-cutting, and package forming. It distinguishes press corrections from finishing corrections, and explains when predictive image compensation is justified—and when it merely conceals an unstable process.
1. Registration is not dimensional accuracy
Color-to-color registration measures relative alignment between separations. It does not, by itself, establish that the complete image has the correct length, width, angle, or position against a cutter or seal. If all color separations are carried by the same shrinking web, they may remain mutually registered while the package repeat becomes too short. Similarly, a perfectly printed folding-carton sheet can expand before die-cutting, shifting image-to-crease alignment without disrupting color-to-color registration.
The useful distinctions are: color-to-color registration (alignment among separations); repeat length (distance between equivalent marks in consecutive web repeats); print-to-cut, print-to-crease, and print-to-seal registration (position relative to functional converting features); and dimensional stability (how a substrate retains dimensions under specified conditions). These characteristics must be recorded independently.
2. Directional terminology: roll-fed and sheet-fed are not the same
For a continuous roll-fed web, machine direction (MD) is the material-production direction along the web, and cross direction (CD) is perpendicular to it. Transverse direction (TD) is also commonly used for polymer films. Record the actual web orientation through printing and converting: rotating or reorienting an item on a web can change which artwork dimension coincides with MD.
For sheet-fed Paper and board, the production-relevant grain designation is long grain (LG) or short grain (SG). Long grain means that the predominant fiber direction is parallel to the sheet's longer side. Short grain means the predominant fiber direction is parallel to the sheet's shorter side. Thus, a 700 × 500 mm sheet can be LG if the grain runs along the 700 mm dimension, or SG if it runs along the 500 mm dimension.
These are related descriptions, not interchangeable coordinate systems. MD/CD remain useful in paper science as directions in the original web; LG/SG identify fiber orientation relative to the cut sheet. A sheet's print-feed direction is another question entirely. Always specify an explicit grain arrow on the job ticket or production drawing rather than inferring grain from dimension order.
3. Five mechanisms that change printed geometry
Elastic extension occurs while the web is under tension and may largely recover after tension is removed. Permanent deformation or creep can remain after unloading, especially when stress, time, and temperature interact. Thermal dimensional change can occur when oriented films release residual stress on heating. Hygroexpansion occurs when paper and board gain or lose moisture. Nonuniform deformation includes skew, curl, width profile change, and different local strain across the sheet or web.
Do not label every negative dimensional change "shrinkage." A mark-to-mark distance measured on a tensioned web and the same distance measured on a relaxed sample describe different mechanical states. Also distinguish a true size change from pure translation: moving an image relative to the web edge is not the same as changing its width.
4. Sheet-fed offset: moisture, grain, and fan-out
Paper and paperboard are hygroscopic. As moisture content changes, fiber swelling produces dimensional change, usually greater across the fiber direction than along it. For an LG 700 × 500 mm sheet, a larger humidity-driven response may appear in the 500 mm dimension; for an SG sheet of the same size, it may appear in the 700 mm dimension. The actual result depends on the paper furnish, coating, manufacturing history, environmental conditions, and conditioning time.
In conventional dampened offset, interaction with fountain solution can contribute to expansion or differential fan-out across a sheet. It is not the only possible cause: sheet handling, gripper control, packing, cylinder settings, and mechanical registration must also be examined. Dry offset, UV-curing workflows, and other offset variants cannot be assigned identical moisture or thermal mechanisms.
A carton may leave the offset press in acceptable register, then move out of alignment with its die after different storage conditions. Before changing the plate artwork, compare controlled sheet dimensions at press exit and at die-cutting; confirm LG/SG, moisture conditioning, and crease-line orientation against the grain.
5. Roll-fed offset: add MD tension and drying effects
In web offset, the substrate is guided continuously under tension. The Paper's moisture response remains relevant, while MD extension, CD width change, web tracking, dryer exposure, and subsequent cooling may create additional variation. A correction suitable for a sheet-fed press should not automatically be copied to a web press. Record substrate dimensions under a defined tension state, not merely at the in-line inspection station.
6. Flexography: plate geometry and substrate strain are separate
A flat photopolymer plate is wrapped around a cylinder or sleeve. Its printing surface lies at a larger radius than the mounting surface, changing the circumferential geometry. Prepress therefore commonly applies plate-distortion compensation to shorten the flat imaged artwork in the printing direction before mounting. The required factor depends on plate construction, thickness, mounting system, and the mechanical repeat. Use a verified plate supplier or prepress calculation rather than an assumed universal percentage.
Standard plate compensation is distinct from additional, product-specific distortion applied to counter known downstream changes. It is also distinct from MD extension of the substrate under web tension. When repeat length is wrong, determine whether the error was present in the first printed sample, occurred when the web was released, or developed only during converting.
Mechanical limit: in a conventional cylinder-driven flexographic configuration, the physical pitch of consecutive repeats is constrained by the effective printing circumference and press mechanics. Distorting artwork within one repeat cannot automatically change the physical interval between one revolution's register mark and the next. Changing that repeat may require a different cylinder or sleeve, a compatible variable-repeat arrangement, or another verified mechanical/process solution.
7. LEP: digital geometry without a flexographic plate
In liquid electrophotography (LEP), the image is written digitally, developed, and transferred through an intermediate blanket. Supported platforms may provide image-scaling and geometric correction controls through the writing/imaging system. These adjustments can change printed image dimensions without manufacturing new offset or flexographic plates. Available correction axes, increment size, acceptable limits, and interaction with machine calibration depend on the platform and must be checked for the specific press.
The absence of a flexographic plate does not make the substrate dimensionally invariant. In sheet-fed LEP, paperboard moisture and LG/SG remain relevant. In roll-fed LEP, web tension and MD/CD material properties remain relevant. Although a heated blanket participates in LEP ink-film formation, the blanket temperature is not necessarily the temperature the substrate experiences; actual thermal exposure depends on the press configuration and transfer conditions.
LEP scaling modifies the image written on the substrate. It cannot independently reverse permanent distortion that arises later in a laminator, slitter, or pouch machine. That later distortion must first be located, characterized, and stabilized.
8. Comparison of printing technologies
Engineering question | Offset | Flexography | LEP |
|---|---|---|---|
Main image-forming mechanism | Plate to blanket to substrate | Flexible plate to substrate | Digital image and intermediate transfer |
Routine curved flexo plate correction | Not applicable | Often required | Not applicable |
Artwork-size correction | Prepress / plate imaging; supported press adjustments | Prepress/new plate or image carrier; supported press controls | Supported digital image scaling |
Roll-fed MD/CD effects | If web-fed | If web-fed | If web-fed |
Sheet-fed grain-related effects | LG / SG for Paper or board | LG / SG if sheet-fed paper/board | LG / SG for Paper or board |
Can a stable finishing offset be precompensated? | Yes, within tooling and print constraints | Yes, within tooling and repeat constraints | Yes, within imaging and process limits |
Can precompensation repair unstable finishing? | No | No | No |
9. Paper and board versus polymer films
Paper and folding board: moisture uptake and loss, fiber orientation, multilayer construction, and conditioning can cause sheet size changes and increase curl and crease sensitivity. Specify LG/SG for the cut sheet, and verify the grain arrow relative to critical folds.
BOPET / PET: many heat-stabilized grades offer useful stiffness and dimensional stability, but oriented polyester films can still exhibit tension response and heat-induced shrinkage depending on grade and exposure.
BOPP: biaxial orientation influences tensile and thermal response in MD and CD. Do not assume identical behavior in the two directions or across film suppliers.
PE: many polyethylene films are relatively compliant and may show greater tension-driven extension or creep than stiffer comparable film structures. Properties depend strongly on resin family, film thickness, orientation, and multilayer design.
MDO-PE: machine-direction orientation can increase MD stiffness; residual thermal response depends on the specific stabilization process. The name alone does not establish a shrinkage allowance.
Laminated structures: PET/adhesive/PE, BOPP/adhesive/PE, and other constructions can develop internal stress when layers enter lamination at different strain states or respond differently to heat. Compare the finished construction, not only the data sheets of individual films.
10. Web tension: force is not the same as strain
For a simplified uniform uniaxial case, longitudinal engineering stress can be estimated as sigma = F / (w × t), where F is the web tension force, w is the web width, and t is the thickness. If an elastic linear approximation is appropriate, strain is epsilon = sigma / E, where E is the directional tensile modulus. Many films are viscoelastic: time, temperature, rate, and prior strain can alter this relationship.
Consequently, equal tension forces on PET and PE webs do not imply equal strain. Nor should laminator A and laminator B necessarily use identical numerical tension settings: effective tension depends on width, thickness, span, winding diameter, equipment geometry, and the film's behavior. Use validated operating windows, not universal set points.
11. Thermal change must be tested in both directions
Oriented films may change length and width when heated. Some grades are stabilized for specific thermal windows, while others retain appreciable shrinkage potential. A film can show one change in MD and a different change in CD. The relevant variables are actual film temperature, exposure time, restraint, and subsequent relaxation—not just a heater controller reading.
For root-cause work, measure MD and CD change under a defined test method and compare with actual production exposure. ISO 11501 and ASTM D1204 cover related thermal dimensional-change testing but use differing technical methods; results must not be treated as directly interchangeable.
12. Why finishing creates a new geometry
Printing and finishing are mechanically different processes. A job can satisfy all agreed press-exit measurements yet become incorrect because a following operation changes its dimensions or its position relative to the package features. The main finishing mechanisms include differential web strain in lamination, thermal relaxation during coating or drying, time-dependent changes under laminate conditions, variable winding stress, skew or lateral shifts during slitting, and cutter/servo registration errors during package forming.
The first rule is to separate physical image distortion from positioning error. A servo-controlled cutter can correct timing or mark-to-cut offset within its usable range. It cannot necessarily restore the physical size of an image whose printed substrate has permanently contracted.
13. Lamination: first control the two webs, not the artwork
Consider reverse-printed PET laminated to PE. The two materials differ in stiffness, extension behavior, thickness, and possibly thermal response. If they are bonded under different elastic strains, the final structure may carry residual stress. After unloading or subsequent conditioning, one layer may try to recover more than the other; adhesion constrains independent recovery, and the laminate can change length, curl, or both.
A disciplined check records the tension of each incoming web, width and thickness, unwind braking and draw settings, nip loading, thermal conditions, alignment, and measured repeat length before and after lamination under comparable conditions. The correct goal is not simply equal force readings. It is a validated strain/tension balance that preserves laminate bond quality and downstream dimensional stability.
Adhesive cure may change mechanical properties over time, but cure does not automatically mean the laminate will shrink. Verify whether the measured size continues to change after the approved conditioning period; do not attribute a dimensional change to adhesive chemistry without evidence. After adjustments, confirm adhesion, bond integrity, appearance, food-contact or other functional requirements as applicable.
14. Slitting and rewinding: length, edge position, and winding stress
Slitting does not inherently change the printed length. However, web transport through the slitter, rewind tension, tapered tension controls, roll hardness, edge guiding, and winding history can expose or create strain-related variation. A lateral cut-position error can move an image closer to the roll edge while leaving its physical width unchanged. This is print-to-edge, not necessarily CD shrinkage.
Measure repeat length separately from print-to-edge and web width. When troubleshooting, check the actual tension at the sample point and inspect whether changes correlate with roll diameter, lane position, or time on the machine.
15. Die-cutting and folding: separate sheet size from tool position
A sheet-fed folding-carton job may arrive at the die-cutter with altered dimensions after storage. First verify sheet condition, LG/SG, conditioning history, and image-to-sheet-edge distances. Then verify gripper or feed alignment, die positioning, crease tooling, and converter repeatability. A die-cut offset with unchanged sheet dimensions is not the same defect as sheet expansion.
Grain orientation also affects folding response and the risk of cracking along critical creases. LG/SG must therefore be defined against the actual carton layout and fold lines, not treated as a generic preference divorced from the finished package.
16. Form-fill-seal: registration controls cannot cure every deformation
At the package-forming machine, mark sensors and servo controls synchronize web feed, sealing, and cut timing. If the repeat remains constant but a cut occurs too early, a sensor position, mark design, tool timing, or software reference error may be the cause. If the physical repeat changes along the roll, the converter may run out of correction range even while it correctly reads every eye mark.
Record measured repeat, mark-to-seal distance, mark-to-cut distance, film tension, and actual production speed. Check whether the defect follows the web material, repeats once per printed cycle, changes during acceleration, or appears only at a particular roll radius. Use print-to-cut and print-to-seal tolerances that reflect functional package requirements, not color registration alone.
17. What can be corrected on the press—before finishing?
Offset, sheet-fed: correct actual feed and registration errors first; control moisture conditioning, gripper and sheet handling, packing, and relevant press mechanical conditions. If a reproducible image-size mismatch remains, adjust artwork geometry in prepress and output a corrected offset plate using the controlled CTP workflow. In some press configurations, supported registration and image-position controls provide additional adjustment. Re-imaging changes the image on the plate; it is not the same as physically stretching an installed metal plate.
Offset, roll-fed: stabilize web tension, drying and cooling conditions, web path, and registration systems. For repeat or circumferential constraints, assess the cylinder/press configuration. Plate-image distortion can alter artwork dimensions within allowed bounds but does not guarantee a new physical repeat pitch on a mechanically fixed system.
Flexography: verify cylinder or sleeve repeat, plate thickness, mounting, the ordinary plate-distortion factor, and MD tension. Correct plate artwork distortion in prepress, produce an appropriately revised plate, and confirm register across all separations. Where supported, use register and servo controls for position—not as a substitute for physical dimensional stability. Distinguish image scale within the repeat from the repeat pitch determined by tooling.
LEP, sheet-fed or roll-fed: first verify imaging calibration and substrate handling. Where the platform supports it, adjust imaging-system scaling in the necessary direction, then verify position, color registration, and final output at the specified measurement state. Do not assume every LEP product supports every axis or arbitrary scale magnitude, and do not override the press's calibration or substrate operating limits.
All technologies: a correction that aligns the printed image at press exit is successful only if that is the approved acceptance state. If the customer requires final finished dimensions, press-exit geometry may deliberately differ from the finished target only after documented, controlled, predictive compensation has been approved.
18. What must be corrected in finishing—after printing?
When press-exit dimensions are correct, and distortion first appears downstream, the converter owns the first technical investigation. In lamination, correct validated web-draw balance, web-temperature exposure, nip conditions, alignment, and material selection. In coating/drying, evaluate actual substrate temperature and residence time. In conditioning, define the time and ambient conditions before measurement. In slitting/rewinding, correct web tension profiles, alignment, guiding, and winding stress. In sheet-fed die-cutting, correct tool location, feed registration, and environmental conditioning. In form-fill-seal, correct sensor reading, servo timing, feed tension, and the allowable registration control window.
Do not reduce thermal exposure or nip pressure indiscriminately: these changes can impair drying, bond strength, seal integrity, coating performance, or product compliance. Every finishing correction must preserve all functional quality criteria.
19. A decision rule: process correction or print precompensation?
Case A: downstream error varies by roll, lane, time, temperature, or machine speed. This is an unstable process. Correct its cause, verify repeatability, and avoid a fixed prepress scale factor.
Case B: the web or sheet is dimensionally correct, but cutter position is wrong. Correct the converting registration system; image scaling is usually the wrong lever.
Case C: a downstream dimensional change is stable, necessary for the validated process, and repeatable. Consider approved geometric precompensation. Confirm that the press and tooling can actually produce the required image geometry and repeat spacing. Test the complete finished product rather than judging the adjusted print at press exit alone.
Case D: distortion varies across the image or between MD and CD. A single uniform scale factor may be inadequate. Diagnose skew, local strain, asymmetric heat, material thickness profile, or web-tracking differences before adopting any multidimensional correction map.
20. How predictive precompensation is calculated
Suppose the required finished repeat is 400.0 mm, while a validated downstream process consistently reduces the length by 0.30%, measured under comparable conditions. Assuming a uniform multiplicative shrinkage factor, the target dimension before that process would be:
L_before = L_finished / (1 − 0.003) = 400 / 0.997 = 401.204 mm.
This value is an illustrative mathematical result, not a recommended press setting. It is valid only if the 0.30% change is repeatable, the measurement states are comparable, and the process can physically deliver the proposed pre-finishing geometry. In LEP, the image-writing scaling range may constrain the available adjustment. In conventional flexo or offset, the cylinder repeat pitch or other press geometry may prevent the desired 401.204 mm physical repeat even if an artwork image can be distorted inside the original mechanical repeat. Tooling or process redesign may be necessary.
If MD and CD changes differ, calculate and validate each axis separately. For nonuniform distortion, an overall percentage is insufficient. Record measured averages, spread, lot variability, minimum and maximum, and capability against the finished-product tolerance; do not choose compensation from a single sample.
21. Worked diagnosis: a 400 mm PET/PE packaging repeat
Assume a reverse-printed PET web is approved at 400.0 mm repeat at press exit under a defined unloaded measurement condition. PET is laminated to PE. After lamination and the specified conditioning period, repeated samples measure 398.8 mm at the same defined condition. This hypothetical case shows where to look, not a claimed historical production failure.
First, confirm that both measurement systems are calibrated and use the same mark reference and environmental conditions. Then measure an identified print repeat immediately before the laminator, after laminator exit, after conditioning, after slitting, and at package forming. Record both incoming-web tension settings and material lots. If the change appears during lamination, examine draw/tension matching, nip, and temperature. If the first change occurs only during winding or conditioning, focus there. If the repeat remains 400.0 mm but the cut shifts, investigate cutter registration rather than shrinkage.
Do not change the LEP image scaling, flexo plates, or offset plates until this stage-specific evidence is clear. If the finishing process is corrected and the finished repeat returns to target, no print precompensation is needed. If a stable unavoidable residual remains, validate compensation against real finished packages and preserve the previous settings as a rollback baseline.
22. Diagnostic map: identify what actually changed
Observed defect | First measurement | Likely investigation | Preferred initial action |
|---|---|---|---|
All colors register, repeat too short. | Repeat under defined tension. | Web strain, thermal change, plate/image geometry | Locate first stage of change. |
Repeat correct, cut misplaced. | Print-to-cut / sensor timing | Die or FFS control | Correct converter registration |
Sheet image fits press proof, misses die | Conditioned sheet size, LG/SG | Humidity, feed, die position | Stabilize sheet / verify tooling |
Flexo repeat wrong from first print. | Plate factor, cylinder repeat | Plate distortion or mechanical pitch | Correct plate/prepress or tooling |
LEP image size wrong at press exit | Imaging dimension and calibration | Digital scale/substrate handling | Apply verified press-side scaling |
Repeat changes after lamination. | Before/after repeat, both web tensions | Differential strain, temperature | Stabilize lamination |
Repeat varies with rewind diameter. | Repeat vs. diameter/tension. | Winding tension and web recovery | Stabilize rewinding |
Image drifts toward web edge. | Print-to-edge, web path | Guiding/slitting position | Correct lateral alignment |
One web edge changes more than the other | Cross-web dimensional map | Skew, thickness, temperature profile | Correct asymmetry at source |
23. Seven-point production measurement protocol
- 1. Define the finished-package datum: printed fiducial, cut line, fold, or seal reference—not only the color bars.
- 2. Specify material orientation: MD/CD for roll-fed webs; LG/SG and a grain arrow for sheet-fed paper/board.
- 3. Define measurement state: temperature, humidity, web tension or unloaded conditioning time, and whether the sample is before or after lamination cure.
- 4. Measure press exit: repeat, width, diagonals/skew where relevant, and print-to-edge or image-to-sheet-edge offsets.
- 5. Sample the same stages: press exit, lamination exit, conditioning, slitting, and final package; use traceable samples and suitable calibrated devices.
- 6. Test repeatability: collect different positions across the web, multiple repeats, and independent rolls or production runs when appropriate.
- 7. Approve the corrective action against the final product: document process settings, residual error, quality side effects, and rollback criteria.
24. Case studies by printing process
Sheet-fed offset—carton shifts at die-cutting: the print is mutually registered but finished carton creases are out of position. Check LG/SG against the imposed layout, conditioned sheet dimensions, storage humidity, and die feed before modifying CtP image scale. If a stable paper-size response persists in a controlled supply chain, a verified artwork compensation may be appropriate—but the packaging tool and grain orientation still define final acceptance.
Web flexography—repeat length has two possible causes: if the discrepancy is visible in the first printed sample, investigate plate-distortion calculation, mounting, cylinder pitch, and in-process web tension. If it appears only after the web relaxes, investigate material strain. Avoid mixing normal plate-curvature compensation with finishing precompensation in a single undocumented factor.
Roll-fed LEP—print passes, laminate fails: LEP can scale its written image on supported platforms, but doing so before stabilizing the laminator can conceal variable web draw. First measure the laminate's before/after change, correct the laminator, and validate final package function. If residual change is stable and unavoidable, establish a documented press-scaling test using the approved finished-repeat target.
Sheet-fed LEP—cut sheet changes during storage: digital imaging does not prevent moisture-driven paperboard movement. Check LG/SG and controlled storage between printing and die-cutting. Do not blame the image-writing system when the sheet physically changes after press exit.
25. Acceptance criteria and change control
A robust specification states both where and under which conditions dimensions must conform: at press exit, in a relaxed web, after adhesive conditioning, or on the finished package. It defines relevant MD/CD or image dimensions, functional print-to-cut and print-to-seal tolerances, measurement methods, and acceptable variation. A color-registration tolerance cannot replace the dimensional specification of a finished package.
Version-control any approved predictive correction. Store the measured downstream shrink/expansion factor, source material lot, press imaging or plate compensation version, converter settings, trial samples, quality sign-off, and reasons for any later reset. If the film grade, lamination structure, process temperature, die, or packaging machine changes, revalidate the compensation rather than silently carrying it over.
26. Technical standards and what they do—and do not—prove
ISO 187:2022 defines conditioning/test atmospheres for Paper, board, and pulp. It supports comparable sheet measurements but does not itself prescribe a print compensation factor.
ASTM D882-26 defines tensile testing for thin plastic sheet and film. Tensile modulus and extension data help characterize strain susceptibility, but test rates and geometry differ from high-speed web transport.
ISO 11501:1995, confirmed current in 2025, addresses longitudinal and transverse dimensional change of film and sheeting on heating. ASTM D1204-25 addresses linear dimensional change of nonrigid thermoplastic film at specified elevated temperature and time. These methods are not technically identical, and their test results are not directly interchangeable.
For flexographic plate distortion, published engineering studies and prepress references document the relationship between mounted-plate geometry and the required image correction. Equipment-specific values still require verification against the actual plate and mounting workflow.
27. Glossary of essential terms
Term | Meaning |
|---|---|
Registration | Relative position of printed elements or a production reference |
Color-to-color registration | Alignment between printed color separations |
Repeat length | Distance between equivalent points on consecutive printed repeats |
Print-to-cut / print-to-crease / print-to-seal | Printed image alignment to a functional converting feature |
MD / CD | Machine/cross directions of a continuous roll-fed web |
LG / SG | Long/short grain; fiber direction relative to the longer / shorter side of a cut sheet |
Plate-distortion compensation | Conventional flexographic prepress correction for mounting a flat plate around a cylinder |
Digital image scaling | Change of written image geometry on supported digital imaging systems |
Predictive precompensation | Deliberate, verified print-side correction for a stable downstream dimensional change |
Web tension | Force applied to a moving web. |
Hygroexpansion | Dimensional response to changes in moisture content |
Thermal shrinkage | Dimensional reduction associated with heat exposure in susceptible films |
Creep/recovery | Time-dependent deformation / partial return after unloading |
Translation/scaling/skew | Pure position change/size change / angular distortion |
Nonuniform distortion | Spatially varying deformation that cannot be described by one scale factor |
FFS | Form-fill-seal packaging process |
Conclusion — correct the stage that causes the error
In industrial printing, a perfect color-to-color register is only one dimension of quality. Paper and board change with moisture and grain orientation; polymer webs respond to MD tension and thermal history; laminated structures can carry residual strain. Offset, flexography, and LEP also differ in how image geometry can be changed on press or in prepress.
The decisive engineering distinction is where the distortion first appears. If it is present at press exit, correct the appropriate press, plate, imaging, or substrate-handling parameter. If printing is dimensionally correct and distortion develops in finishing, stabilize the laminator, slitter, die-cutter, or FFS process first. Only when a residual dimensional change is stable, unavoidable, measurable, and compatible with tooling should it be countered by a deliberate press-side precompensation.
Registration tells us whether the colors fit each other. Dimensional control tells us whether the printed image still fits the package after every production step.
Professional references
- ISO 187:2022, Paper, board and pulps — Standard atmosphere for conditioning and testing and procedure for monitoring the atmosphere and conditioning of samples.
- ASTM D882-26, Standard Test Method for Tensile Properties of Thin Plastic Sheeting.
- ISO 11501:1995, Plastics — Film and sheeting — Determination of dimensional change on heating.
- ASTM D1204-25, Standard Test Method for Linear Dimensional Changes of Nonrigid Thermoplastic Sheeting or Film at Elevated Temperature.
- Valdec, D., Tomerlin, R., Hajdek, K., & Miljkovic, P. (2022). Influence of the Polymer Plate Thickness on the Plate Distortion Factor in Flexography. Tehnicki glasnik, 16(1), 47–52.
- Professional Prepress, Printing, & Publishing, sample chapter, sections on flexographic plate distortion and paper grain direction.
- PrintWiki, Long-Grain, grain orientation relative to the longer dimension of a sheet.
Editorial note: The 400.0/398.8 mm example is a hypothetical calculation, not evidence from a specific manufacturing failure. This article contains no universal tension, scaling, heating, or cure values. Confirm platform capabilities and validate all changes against the actual material, equipment, and final product requirements.