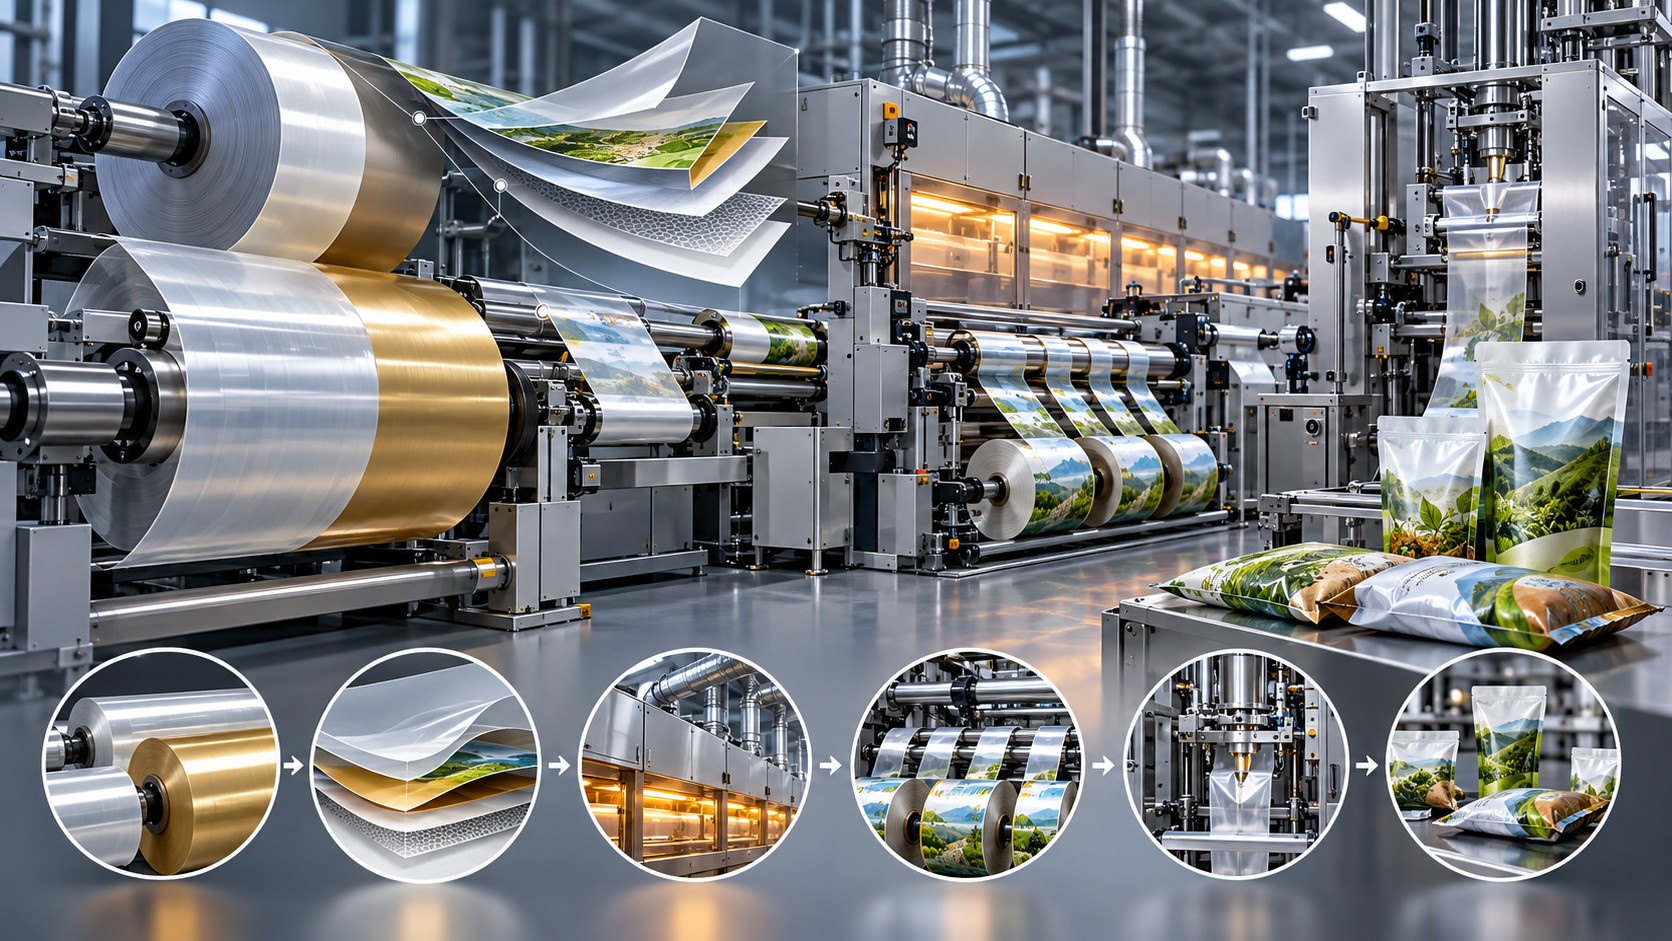
Cutting Is More Than Separation: When Converting Determines Flexible Packaging Performance
Slitting, Rewinding, Punching, Laser Scoring, Perforation, and Pouch Converting—How knife choice, web tension, roll quality, and cutting engineering determine whether printed film becomes a reliable package
By Ronen Dolev
When the Roll Looks Perfect, but the Packaging Machine Cannot Run It
A printed, laminated roll enters the converting department. Its PET/INK/ADH/PE construction is intended for food packages on a horizontal form-fill-seal (HFFS) machine. Color meets specification, print registration is accurate, and the laminate has passed the required readiness checks before converting. The roll is mounted on the slitter-rewinder, where the operator positions the knives, enters the required widths, and stabilizes the tension-control system.
The parent web travels through a sequence of rollers, passes the cutting station, and separates into narrower lanes. The individual lanes are rewound onto new cores. At first inspection, everything looks excellent: roll widths fall within tolerance, edges appear clean, print sits correctly relative to the edges, and the rolls look even. The shipment is approved.
At the customer's HFFS machine, however, small variations develop between the printed graphics and the cross-cutting unit. Wrinkles begin to form as the web passes over the forming shoulder, and package geometry becomes inconsistent. The operator checks the web guide, changes tension, and reduces speed. Some symptoms improve, but instability returns. Replacing the problem roll with another from the same print job restores normal operation.
The investigation turns to converting. Although the rolls were produced on the same machine, their winding conditions were not identical. Under magnification, the suspect roll also reveals small edge defects that were invisible during the initial visual inspection. Two independent factors may now be contributing to downstream trouble: a damaged edge that can initiate a tear, and a winding profile that prevents stable unwinding across the full diameter.
Slitting is not merely dividing a wide roll into narrow ones. It is a continuous cutting operation on a multilayer structure moving under tension. Rewinding is not merely collecting the material. It creates an internal distribution of forces that affects the roll's behavior in the next machine. Punching, perforation, and laser scoring similarly change structural integrity and tear performance. Converting quality is proven not at the slitter exit, but in the package made from the roll.
Understand the Construction Before Choosing a Knife
Flexible packages use PET, BOPP, PE, CPP, OPA, aluminum foil, metalized films, and constructions containing barrier layers such as EVOH, SiOx, or AlOx. Some are monoweb structures; others contain two or more films joined through lamination or produced by coextrusion. Each ply serves different mechanical and functional purposes.
For example, in PET/INK/ADH/PE, PET commonly provides the outer printed web while PE functions as the inner sealant. PET/AL/PE incorporates aluminum foil as a barrier component. Two laminates of similar total thickness may respond very differently to the same knife. PET can offer comparatively high stiffness and dimensional stability; PE can be more extensible; thin foil can be vulnerable to local cracks and pinholes. Oriented films such as BOPP or MDO-PE may have strongly directional behavior.
The choice of cutting method must therefore consider the whole construction: stiffness, extensibility, ply combination, thickness distribution, barrier sensitivity, anticipated mechanical loads, and the quality required at the freshly cut edge. The laminate should have passed its process-specific readiness checks before qualification trials; the chemistry and curing of laminating adhesives are addressed in a separate article.
Machine Direction and Transverse Direction
Roll-fed flexible materials are commonly described by machine direction (MD), parallel to the web travel, and transverse direction (TD) or cross direction (CD), across the width. In oriented films, tensile properties, elongation, shrinkage, and tearing behavior can differ by direction.
Slitting normally makes longitudinal cuts parallel to MD. Punching, tear notches, transverse cross-cutting, and laser scoring may intentionally create tear paths with different relationships to film orientation. A polymer film that tears easily in one direction does not necessarily behave the same way when the tear is initiated in the perpendicular direction. This difference matters most in easy-open packs and recyclable mono-material structures with orientation-dependent properties.
The Slitting Process: From Parent Roll to Daughter Rolls
A slitter-rewinder typically includes an unwind station, web-transport rollers, tension-control and guiding devices, the cutting station, edge-trim removal, and one or more winding stations. The parent roll is unwound, the web is stabilized and presented to the knives, and each cut lane follows a defined route to its rewind core.
Output requirements are simultaneous rather than sequential: correct lane width, clean edges, stable tracking, controlled particles, appropriate winding structure, and suitable presentation for the next machine. Poor web control can degrade cut quality; a clean cut does not guarantee acceptable rewinding; a roll that looks good at rest may unwind badly on a high-speed packing line.
Three Cutting Methods, Three Different Mechanisms
Three primary categories dominate industrial film slitting: razor slitting, shear slitting, and score/crush slitting. They are not interchangeable simply because they produce a similar visible cut.
Razor Slitting: Direct Separation With a Sharp Blade
Razor slitting places a sharp blade against a moving web. Some systems support the film over a suitably grooved roller; others cut through a controlled free span. Blade-edge geometry, sharpness, mounting angle, local web support, knife-holder stability, and film tension all affect the result.
When the knife is properly selected for a compatible film, razor cutting can be efficient and produce a good edge. As wear develops, the blade may stretch or drag the polymer before it separates. This can create roughness, minute cracks, particles, and local tear initiators. In multilayer laminates, the plies may not respond identically to the local load. Tool-change criteria should therefore reflect edge quality and process history, not just the point at which the blade stops cutting.
Shear Slitting: Controlled Scissor-Like Cutting
In shear slitting, upper and lower knives act like scissors. The interaction between their edges shears the web locally. With appropriate tools and settings, the method can deliver high-quality edges across a wide range of films, laminates, and foils.
The key variables are overlap, shear angle, and side load. Overlap is the geometrical engagement of the two knife edges. Too little can cause incomplete or unstable cutting; too much can increase contact, friction, wear, and possible web damage. Side load maintains the necessary lateral knife engagement. Too much accelerates wear, while too little can lose effective contact. The relative shear or cant angle controls how the edges meet and develop the cut.
These settings interact. Increasing all of them does not make cutting more robust. The best setup uses the intended knife-holder geometry and the minimum effective load for stable separation, confirmed with the production material.
Score / Crush Slitting: Concentrated Pressure Against an Anvil
Crush slitting presses a circular knife against a hard anvil surface, separating the web through concentrated mechanical loading. Edge profile, edge radius, applied force, anvil condition, and film properties determine the cut. Excessive load may compact the edge, cause local distortion, or generate debris. Insufficient load may produce incomplete separation.
This method can be appropriate for selected materials and equipment, but sensitive barrier laminates require careful evaluation. Even where the edge looks clean to the eye, localized compression may affect layer integrity. Approval should be based on microscopic edge inspection and downstream package behavior as appropriate.
Comparing Slitting Methods
Method | Cutting mechanism | Critical settings | Potential defects |
|---|---|---|---|
Razor | Direct sharp-blade cutting | Sharpness, angle, support, tension | Film dragging, rough edges, tears |
Shear | Scissor-like action between two knives | Overlap, shear angle, side load | Friction, dust, unstable edge quality |
Crush / Score | Compression against an anvil | Edge radius, force, anvil surface | Edge compaction, particles, ply damage |
The preferred method should be qualified with the actual laminate, not selected from nominal polymer identity or web thickness alone.
Choosing the Knife: Sharpness Is Only One Variable
Knife material, hardness, surface condition, bevel geometry, edge finish, wear resistance, and intended production life all contribute to performance. A very fine edge can reduce penetration force but may be more vulnerable to wear or local damage in certain materials. A more robust edge can last longer but impose a different force profile on the film. Film extensibility and orientation are as relevant as nominal thickness.
A suitable knife for a single PET film is not automatically suitable for PET/PE, and it should not automatically be approved for a laminate containing thin aluminum foil. Qualification should consider edge cleanliness under magnification, particle formation, ply integrity, and the web's response under downstream tensile load.
Overlap, Shear Angle, and Side Load: What the Operator Is Actually Setting
Shear angle. The angle of knife engagement affects the contact zone and separation stability. In certain knife-holder designs, angles around 0.25°, 0.5°, and 0.75° are offered, but these are equipment-specific geometries—not universal film recipes. DIENES describes common applications that use one angle and others that require different settings.
Overlap. Geometrical overlap needs to be adequate to establish the shear point, but excessive overlap can increase the path along which the film contacts the knife. This can promote rubbing, particles, and edge degradation. Too little overlap can produce incomplete cuts.
Side load. Lateral force maintains the intended edge engagement. Excessive side load shortens knife life; insufficient side load impairs cut quality. The right combination is derived from equipment specifications and trials with the intended web.
Never attempt to correct a bad shear cut by indiscriminately increasing overlap, side load, and speed. First, check the reference geometry, knife condition, holder condition, and actual edge failure.
Why There Is No Universal Slitting-Knife Height or Penetration Formula
Some folding-carton creasing systems use fixed rule-height references and starting formulas for crease channels. Flexible-film slitting uses very different physical mechanisms. Razor cutting depends on blade location relative to the web and support; shear cutting depends on the engagement of two knives; crush cutting depends on the edge profile and contact pressure against an anvil.
The question is therefore not simply "How deep should the knife enter a 70-micron film?" Two films of the same nominal gauge can require different knife settings due to stiffness, orientation, coating, and layer structure. Knife setup must follow the correct machine and tool documentation, and its acceptance must be demonstrated on a representative sample.
The Knife Holder Is Part of the Cutting System
Even a new, sharp blade can produce a defective edge in a poorly maintained holder. Bearing play, vibration, insufficient rigidity, incorrect clamping, or movement of the mounting position can change how the blade engages the material. This may cause repeating or speed-dependent edge defects.
Inspection should include the knife, holder, bearings, adjustment mechanism, and repeatability after a blade change. Where a machine can switch between razor, shear, and crush heads, each complete configuration should have its own approved operating window. Rapid tool change is convenient but does not remove the need for material-specific validation.
Why the Quality of the Cut Edge Matters
The edge is mechanically vulnerable. Under the microscope, an apparently straight edge may show roughness, tiny tears, a stretched layer, or the beginning of interply separation. When the film passes through form-fill-seal equipment, longitudinal tension can grow these initial defects into a full web break.
Where a structure contains thin foil or high-barrier coatings, localized damage can also impair functionality. Abrasion and cutting friction may produce particles that accumulate near the cutting station or enter wound rolls. Edge inspection therefore must go beyond width checks; in high-value or safety-sensitive uses, cleanliness, cut morphology, and barrier integrity may be decisive acceptance criteria.
Slitting Layout: Engineering the Widths
Suppose a parent roll measures 1,250 mm and is intended to supply four 300 mm daughter rolls. The combined product width is 1,200 mm, leaving 50 mm for trim and other allowances. If the layout is symmetrical, 25 mm on each side is a possible starting allocation.
This is a geometrical illustration, not a production setting. Actual layout must account for graphic placement, seal zones, print registration marks, lane tolerances, web-guide travel, and whether the quoted parent width includes unusable material. Cross-web thickness variations can affect how rolls from different lanes wind, even when nominal widths match.
Edge Trim Is a Production Variable
Trim removal helps eliminate nonproduct material, but it also creates a running waste web. Trim strips that are too narrow may break during extraction; excessive trim wastes expensive laminate. Poor waste management can reintroduce debris into the web path. Specify both the edge-trim allocation and the waste-removal system for the film thickness, line speed, and slit layout.
Web Tension: Enough Control Without Unnecessary Stretch
Web tension holds the material on a stable path and presents it correctly to the knives. Insufficient tension can cause tracking instability, flutter, or wrinkles. Excessive tension can stretch the film, alter dimensions, worsen edge defects, or increase load on laminate interfaces.
Tensile behavior depends on elastic modulus, film thickness, web width, orientation, and structure. A total force of 100 N on a one-meter-wide web is not the same force per unit width as 100 N on a 0.5-meter web. For comparisons, tension may be expressed in N/m, provided the reference units are clear. But force per width alone is not enough to predict strain without thickness and modulus.
Separate Tension Zones
A slitter-rewinder commonly has an unwind tension zone, a transport and slitting zone, and a rewind tension zone. Each has a different purpose. Unwind control permits stable release of the parent roll; slitting-zone control stabilizes position at the knives; rewind control governs the forming roll. A single indicated tension reading may not describe the conditions at all stations. Sensor calibration and control response therefore matter as much as the displayed setpoint.
Rewinding: Building a Roll With Predictable Internal Stress
After cutting, each lane is wound onto a core. Roll diameter rises continuously, so the relationship between torque and web tension changes with radius. Real machines also include friction losses and mechanical effects; the winding controller must account for the increasing diameter rather than applying an arbitrary fixed drive command.
A useful winding framework is TNT: Tension, Nip, and Torque. Tension is the force of the incoming web; nip is contact load at a lay-on or contact roller where present; torque drives the roll. Together they influence how tightly the layers pack, the pressure within the roll, and subsequent unwinding behavior.
An over-tight roll can develop excessive interlayer pressure and local defects. A loose roll may allow layer movement or telescoping. The visual smoothness of a roll is not sufficient evidence of its functional winding quality.
Taper Tension: Why a Growing Roll Often Needs a Changing Profile
Many winding systems use taper tension, reducing or otherwise adjusting the target tension as diameter grows to manage the stress distribution through the roll. The appropriate taper depends on material stiffness, film thickness, friction, roll width, final diameter, and the intended handling conditions. A PET web, a highly flexible PE structure, and an aluminum-containing laminate may not require the same profile.
Qualification must consider roll-start stability and performance through to the final diameter. In addition to the immediate roll inspection, test unwinding after representative storage, transport, and diameter reduction on the downstream machine where possible.
Differential Winding: Why Lanes From One Parent Roll Can Behave Differently
A wide film may have small differences in thickness across its width. Once divided into narrow lanes, those differences can cause daughter rolls to grow at different rates as layers accumulate. A rigid common drive that does not accommodate these differences may apply unequal effective tension to the individual rolls.
A differential-winding system can allow individual rolls to accommodate differences through controlled torque transmission, depending on the particular shaft and design. This can improve the uniformity of rewound rolls, but it does not repair a severely defective thickness profile, wrinkles, or poor upstream web guidance. Diagnose the actual source of tension or diameter variation.
Telescoping, Starring, Wrinkles, and Blocking
Telescoping
Successive layers move sideways in the axial direction, forming a stepped roll. Possible causes include inadequate winding tension, poor torque distribution, interlayer friction, alignment issues, and handling or storage conditions. Determine whether the displacement exists immediately after winding or grows during storage.
Starring
Radial wrinkles or distortions create a star-like pattern in portions of the roll. These can indicate an inappropriate internal stress distribution, depending on the material and winding method. Examine the winding profile rather than automatically blaming the knife.
Wrinkles
Web wrinkles can arise from uneven tension, misaligned rollers, thickness-profile variation, poor web path, or instability as layers enter the roll. Locate where the wrinkle first forms—at the unwind, transport section, cutting station, or rewind.
Blocking
Blocking is unintended adhesion of adjacent wound surfaces. Temperature, winding pressure, surface chemistry, ink, or varnish can contribute. It should not automatically be interpreted as failure of laminating-adhesive curing; the stuck surfaces and the mechanism must be established first.
Punching: Functional Openings in Flexible Films
Mechanical punching can form hang holes, windows, openings for special components, and other functional features. Tool geometry and local film support are critical because thin flexible films may stretch before separating. In a laminate, different plies respond differently to the punch. An improperly formed opening may initiate a tear or concentrate stress near a seal or an attachment point.
Where a structure contains a barrier, evaluate whether the punch is intended to cut through it. An opening required for a component is fundamentally different from an unintended hole in a barrier package. Hole dimensions, edge morphology, position, waste removal, and downstream performance need separate acceptance criteria.
Perforation: Designing a Controlled Tear
Perforation produces a series of cut and uncut segments. The remaining connections, or ties, provide the strength necessary to resist accidental opening while permitting a user to tear at the intended point. If the ties are too weak, the package may open prematurely; if too strong, the tear can become difficult or stray from the desired line.
The ratio of cuts to ties is only one variable. Polymer type, thickness, orientation, laminate bonding, and the location of nearby seals also influence opening behavior. Evaluate both tear initiation and tear propagation on the finished package, not simply the flat film.
Laser Scoring: Creating Easy-Open Behavior Without Destroying the Structure
Laser scoring selectively weakens material along a designed path. In certain PET/PE constructions, it may be possible to weaken outer PET while preserving continuity of the inner PE. That outcome must be demonstrated: wavelength, optical absorption, film chemistry, layer thickness, power, speed, beam positioning, and laminate construction all influence the result.
Excessive scoring can damage sealant or barrier layers and create unexpected leakage or premature tearing. Insufficient scoring can leave consumers unable to open the package as intended. A path that ignores film orientation may tear inconsistently even if its geometric position is accurate.
Why Some PE Easy-Open Structures Are Challenging
Highly extensible PE structures, including selected recyclable mono-material designs, can stretch before tearing. A scored line may therefore initiate a tear but fail to guide it through the intended path. In suitable applications, an adapted laser process or a revised opening geometry may improve behavior, but these changes must be validated on the actual converted construction. Test tear initiation, propagation, retention of sealant continuity, and barrier performance.
Micro-Perforation: Gas Exchange Is Not the Same as Easy Opening
Laser micro-perforation can be used to establish controlled gas transfer in selected packages, such as fresh produce where package atmosphere management is part of the design. In oxygen-sensitive, high-barrier packaging, the same microholes could be a major defect. Design starts with the product's shelf-life and atmosphere requirements, not simply the number or diameter of perforations.
Do not confuse a micro-perforation used to permit respiration with a selective laser score used to open the package. Both may use a laser, but their functional goals and validation tests are different.
Comparing Functional Cutting Operations
Process | Purpose | Principal risk | Qualification test |
|---|---|---|---|
Slitting | Divide a parent roll into lanes | Edge damage, winding defects | Width, edge quality, unwinding stability |
Mechanical punching | Create a local opening | Tears, delamination, misplaced hole | Geometry, edges, opening function |
Perforation | Enable controlled tearing | Premature or difficult opening | Opening force and tear path |
Laser scoring | Selectively weaken a region | Damage to preserved layers | Tear behavior, continuity, barrier |
Micro-perforation | Enable controlled gas exchange | Inappropriate oxygen/moisture transfer | Gas transmission and product shelf-life |
The correct test follows the function. Tear force alone is not enough when perforations exist to manage the package's internal atmosphere; a clean slit edge does not prove the roll will unwind stably on the filling line.
Cross-Cutting: Transverse Separation on the Packaging Machine
Slitting generally cuts lengthwise along MD. On form-fill-seal equipment, a separate cross-cutting operation cuts across the web to divide packages at their intended pitch. Synchronization among web movement, printed registration marks, sensors, sealing jaws, and the cross-cutting unit determines the print-to-cut position.
If the web stretches inconsistently or the wound roll unwinds with unstable tension, printed graphics may drift relative to the transverse cut. A cut-to-print error is therefore not always a failed eye-mark sensor. Investigate roll stability, web tension, print repeat, synchronization, and the point where deviation begins.
Folding and Pouch-Making: The Cut Web Becomes a Package
Flexible webs generally form their three-dimensional shape without the board-creasing rules used in folding cartons. HFFS and VFFS equipment uses forming shoulders, collars, and other geometries to redirect the web under tension. Separate pouch-making machines can produce empty pouches through folding and sealing before a later filling stage. Those are distinct process routes.
A sound winding profile helps the web run over the forming equipment without wrinkles. A clean edge reduces unintended tear initiation. A weakness at a laminate interface may become visible only as bending and heat are applied. A slitter roll is therefore qualified for the machine and package geometry that will use it, not just for its dimensions on a winding shaft.
Gussets, Zippers, and Spouts: Localized Demands on Converting Accuracy
Gusset regions can involve multiple folds and several film plies meeting in a small area. Zippers require correct alignment and a compatible attachment or sealing process. Spouts typically create a specialized region where hole placement, component geometry, and sealing parameters interact. An inaccurate punch or slit width can produce a functional failure much later during spout installation or sealing.
Such features must be considered when setting the slitting layout and tolerances. Finished-package dimensional checks should include the distance between openings, printed information, sealed edges, and attached components, not just the parent roll's trim width.
Heat Sealing: Cutting and Winding Can Affect the Seal Zone
Sealing depends on the selected sealant layer and its temperature, pressure, and dwell-time conditions. Converting also plays a role. Incorrect width can change the intended seal position. Unstable unwinding can create wrinkles through the seal zone. Particles, folds, or contamination can prevent uniform contact.
Distinguish an actual sealant-interface failure from a geometry, web-transport, or lamination-related defect. ASTM F88/F88M measures seal strength but does not, by itself, establish package tightness or integrity. When leak tightness is required, use suitable additional tests for the construction and intended end use.
Quality Control: Qualify Both the Roll and the Finished Package
Roll acceptance should cover width and dimensional tolerances, core size, final diameter, the position of graphics relative to slit edges, cut morphology, particles, and any signs of ply separation. Inspect winding condition: telescoping, radial distortion, wrinkles, pressure marks, and blocking. Where necessary, test unwinding across the roll diameter after representative storage.
If punching, perforation, or laser scoring is present, add functional checks for hole placement, opening force, tear path, retained-layer continuity, and gas/barrier behavior, as appropriate. Finally, run representative pouch-making or form-fill-seal trials. A flat film's barrier result does not automatically represent a sharply folded, punched, sealed finished package.
Relevant Testing Standards
Standard | Typical application |
|---|---|
ISO 4593 | Mechanical scanning measurement of plastic-film thickness |
ISO 8295 | Coefficient of friction of plastic film and sheeting |
ASTM F392/F392M | Flex durability conditioning for flexible barrier materials |
ASTM F88/F88M | Seal strength of flexible barrier materials |
ASTM F3039 | Dye-penetration leak detection for nonporous packaging |
These documents define test methods, not universal pass/fail values for every product. Acceptance limits must be tied to the package construction, packed product, filling process, and required shelf life.
Troubleshooting: Slitting and Knife Systems
Symptom | Potential causes | Diagnostic action |
|---|---|---|
Incomplete or unstable cut | Worn blade, unsuitable overlap, vibration | Check knife geometry and holder stability |
Rough or pulled edge | Edge wear, unsuitable knife profile | Inspect at magnification and compare with new blade |
Cutting dust or particles | Friction, side load, method mismatch | Review blade contact and debris collection |
Tear begins at film edge. | Local cut defect, excessive web tension | Inspect edge profile and web stresses. |
Incorrect daughter-roll width | Knife positions, guiding drift, layout error | Recheck setup geometry and web-guide control |
Repeating periodic defect | Bearings, vibration, holder play | Inspect mechanical drive and knife holder |
Edge delamination | Local cutting loads or weak interply interface | Map failure plane and compare knife methods |
Premature knife wear | Excessive force, rubbing, wrong geometry | Inspect side load, overlap, and edge materials |
Troubleshooting: Web Tension and Rewinding
Symptom | Potential causes | Diagnostic action |
|---|---|---|
Telescoping | Tension, friction, torque, alignment | Review winding profile and storage |
Starring | Excessive or uneven internal stresses | Examine roll-build conditions |
Wrinkles | Misalignment, tension, thickness profile | Locate first formation along web path |
Loose roll | Insufficient torque or winding tension | Check taper and rewind drive |
Over-tight roll | Excessive torque or nip load | Check internal stress and roll pressure |
Blocking | Pressure, heat, surface chemistry | Identify sticking surfaces and history |
Different behavior among lanes | Cross-web gauge variation, torque distribution | Evaluate differential winding |
Registration drift in FFS | Unstable unwind, stretch | Compare roll and packaging line response |
Troubleshooting: Punching, Laser Scoring, and Pouch-Making
Symptom | Potential causes | Diagnostic action |
|---|---|---|
Inaccurate punched opening | Tool registration, support, web movement | Check position and punching geometry |
Tears around opening | Stress concentration, poor cut edge | Inspect shape and localized damage |
Perforation tears too early | Ties too weak, unsuitable design | Test tear initiation and shipping resistance |
Package difficult to open. | Inadequate scoring, film orientation | Evaluate opening force and path. |
Barrier loss after laser scoring | Excessive score depth, damaged ply | Test continuity and barrier integrity |
Wrinkles at forming shoulder | Roll instability, tension, forming geometry | Locate first deformation |
Incorrect transverse cut | Registration, tension, synchronization | Check eye marks and cross-cut controls |
Local sealing defects | Web wrinkles, contamination, heat or pressure | Identify seal failure mechanism |
Case Study: PET/PE Roll That Wrinkles on an HFFS Machine
A reverse-printed PET/INK/ADH/PE laminate is slit to the required width for pillow packs. One daughter roll produces wrinkles around the forming shoulder; another from the same job runs successfully. Begin by determining whether wrinkles are already present in the roll or arise only while the web is being transported through the HFFS machine.
If the roll shows telescoping or interlayer movement, examine rewind tension and torque distribution. If the roll is stable at rest but the web wrinkles during transport, inspect web path, tension, roller alignment, and thickness profile. If deformation begins only at the forming shoulder, investigate shoulder geometry and film compatibility. Run a controlled comparison between the good and problem rolls at the same packaging settings. Locate the *first point* of instability rather than changing every machine setting at once.
Case Study: Edge-Initiated Tears in a PET/METPET/PE Structure
A PET/METPET/PE high-barrier laminate is slit with a razor system. The edges look acceptable at first, but web breaks begin on one side during packaging. Magnification reveals drag marks and tiny edge defects. Examine blade sharpness, holder angle, support, and tension at the cutting station. Compare with a fresh blade or, where the machine and structure permit, an appropriately set shear-slitting trial.
Do not accept the alternate method on appearance alone. Assess film handling, laminate integrity, particle level, and the function of the barrier construction. A cutting improvement is real only when the resulting roll survives downstream transport and converting without compromising its design requirements.
Case Study: An Easy-Open Pouch That Tears Off the Intended Path
A laser-scored food pouch opens easily at the tear start, but the tear sometimes deviates into the seal region. In some specimens, the film stretches before breaking; in others, the tear propagates off-center. Investigate film orientation, selective-score depth, laminate construction, and the geometrical relationship among score, notches, and seals.
Conduct controlled trials changing one parameter at a time. Measure initiation force and track propagation, then verify retained barrier and seal integrity after changes. The target is not merely the lowest opening force: the package must remain intact during filling, transport, and storage and open reliably only when intended.
Qualifying the Complete Slitting and Converting Process
Start from the finished package and work backward. Define package geometry, filling or pouch-making equipment, barrier and sealing requirements, and any easy-open or component-attachment features. Establish the actual film construction and confirm that upstream manufacturing has released it for converting.
Choose a candidate slitting method, knife type, edge geometry, lane layout, and cutting tolerances. Run a trial and examine edge quality, including magnification where necessary. Qualify web tension, rewinding, and storage response. If punching, perforation, or laser scoring is required, add separate functional trials. Finally, prove the result on representative pouch-making or form-fill-seal equipment.
The acceptance target is a repeatable operating window, not one good-looking roll or one successful machine run.
The Construction and Converting Card
A robust record should describe the film construction and individual plies, original parent-roll width, print orientation, next-machine requirements, slitting method, knives, holder specification, and cutting geometry. For shear cutting, document overlap, shear angle, and side load in the terms used by the equipment supplier. For razor cutting, note the blade and its mounting geometry; for crush, specify edge profile, anvil, and loading condition.
Record daughter-roll widths, edge trim, core diameter, final diameter, tension zones, winding taper, and nip settings where applicable. Add functional specifications for punches, perforations, laser scores, and print-to-feature registration. Include the findings of the representative packaging-machine trial and the conditions that trigger requalification. Changes in film grade, thickness, laminate structure, cutting method, or downstream machine can affect performance even if the package artwork is unchanged.
Cutting Is Not the End of the Process
The flexible-packaging industry puts great effort into printing, materials, primers, and lamination. But an accurately printed, properly prepared roll is not necessarily ready to become a package. Slitting changes the edges. Rewinding redistributes stresses. Punching creates openings and stress concentrations. Laser scoring and perforation change how the film tears. Pouch-making and form-fill-seal add bending, tension, pressure, and heat.
When a web breaks, I want to know the slitting method, the blade's condition, and what the edge looks like under magnification before changing packaging-line speed. When wrinkles appear, I want to understand how the roll was wound and whether thickness and tension vary across lanes. When easy-open performance is erratic, I want to understand film orientation, score depth, and how the different plies interact.
The right knife isn't just the one that cuts. A good roll is not merely straight and neat. A successful package continues to function predictably through every subsequent operation. The roll is an intermediate product. The finished package is where converting quality is ultimately measured.
Professional References and Further Reading
- 1.
- 2.
- 3.
- 4.
- 5.
- 6.
- 7.
- 8.
- 9.
- 10.
- 11.
- 12.
- 13.
TECHNICAL NOTE: Cutting method, knife angle, overlap, side load, web tension, rewind profile, and laser-scoring conditions must be established for the specific equipment, material construction, supplier recommendations, and qualification results. Numerical examples are not universal machine settings.