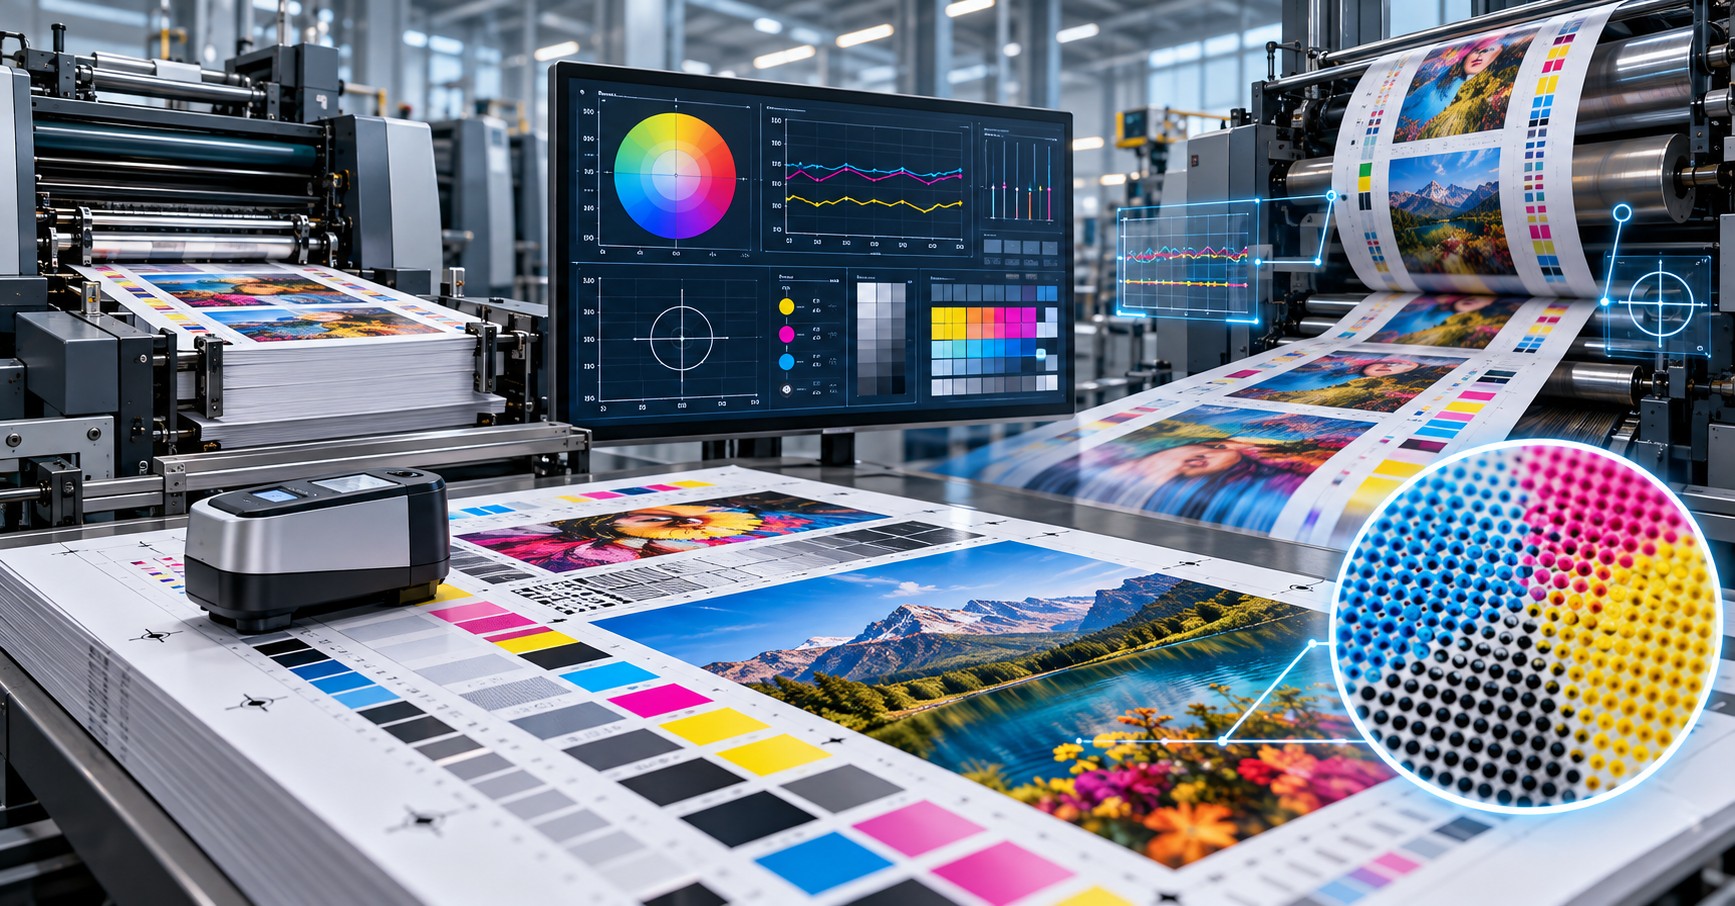
The Physics and Feedback Control of Color Consistency in Offset, Flexography, Gravure, and Liquid Electrophotography
Ronen Dolev | Industrial Color Engineering | October 2026
An approved first sheet is a starting condition, not a guarantee of stability.
The first printed sheet is approved. The solids meet the agreed density or colorimetric aims, the neutral balance looks right, and an important brand color falls within tolerance. The digital file has been released; the plate, where used, remains unchanged. Several hours later, a production sample shows a different hue or a lower optical density. Nothing obvious was changed in the artwork. Why did the printed color move?
Because a printing press does not reproduce color by executing a mathematical file alone. It reproduces color by repeatedly forming, delivering, transferring, and stabilizing physical ink layers on a changing substrate. The machinery, ink system, intermediate surfaces, environment, and measurement chain are dynamic. Drift is therefore possible even with unchanged image data. What matters is not the unrealistic promise of zero variation, but a qualified process that can detect meaningful change, distinguish its mechanism, and hold the printed result inside the required limits.
This article compares conventional offset, flexography, and gravure with sheet-fed and web-fed liquid electrophotography (LEP). It emphasizes the difference between open-loop adjustment and measurement-based feedback, explains why electrostatic fields and particle charge add a distinct layer of complexity in LEP, and sets out a practical, technology-neutral investigation method. [1–12]
1. The four questions that color control must answer
Accuracy describes how close a measured print is to a defined color aim under declared measurement conditions. Consistency describes how the result behaves along a production run and over time. Uniformity describes its variation between positions across a sheet or web. Repeatability describes how closely a qualified result can be reproduced in another run or defined condition.
These are different questions. A press may be extremely consistent but consistently wrong. Another press may print the correct central patch while its two edges disagree. A third may start on target but move steadily away as the run progresses. None of these conditions can be diagnosed from a single start-up sample or a mean Delta E value.
Likewise, optical density (OD), tone value increase (TVI), spectral reflectance, CIELAB and Delta E are complementary—not interchangeable. OD is useful for diagnosing ink-solid process behavior; TVI helps locate changes in tone reproduction; CIELAB components show the direction of a shift; and a color-difference metric such as CIEDE2000 summarizes the size of the difference relative to an agreed reference. A small Delta E does not prove unchanged ink transfer, and a stable solid OD does not prove unchanged neutral balance or overprint color. [9–12]
2. Why an unchanged file cannot hold a physical process constant
Color reproduction depends on the resulting ink layer and its optical interaction with the substrate. In conventional processes, the delivered ink volume, ink-film splitting, plate or engraved cell, impression, rheology, and drying state all affect the print. In LEP, electrostatic imaging, electrically driven liquid development, intermediate transfer, particle charge, and thermal-mechanical transfer help create the final image.
The process also moves toward or away from thermal and operational equilibrium. Ink temperature and rheology may change; solvents or water may evaporate; fountain-solution conditions may drift; surfaces can accumulate deposits; rolls, blankets or developers may wear; and another substrate batch may display different absorbency, gloss, roughness or coating chemistry. Some changes create gradual drift, some create steps after a reel or material change, and some produce positional nonuniformity rather than an average shift.
Not every change requires corrective action. A statistically stable, capable press can remain within product limits without frequent adjustment. The controller or operator should intervene when the evidence shows a meaningful departure, a loss of predictability, or a genuine risk of exceeding specification—not whenever the last reading differs slightly from the preceding one.
3. Open-loop settings versus closed-loop color control
An open-loop action sets an operating parameter and assumes the process will deliver the expected result: an ink-key position, a dilution setting, an imaging calibration state, or a defined pressure. Such a setting can be effective under qualified conditions, but it receives no direct confirmation from the output unless a person or sensor measures the print.
A closed-loop approach compares the printed result against a reference and uses the measured error to decide whether and how to act. Its simplified logic is:
Approved reference → Printing process → Measured print → Error assessment → Bounded correction → Verified print.
The underlying control problem is not simply to make the error vanish at the next measurement. A correction takes time to propagate; samples contain noise; and the action used to improve one channel may disturb another. Overcorrection can turn harmless random fluctuations into oscillating color. Closed-loop systems therefore need sensible sampling, appropriate filtering or decision rules, actuator limits, an understanding of process delay, and a clearly defined state to return to.
When automation makes color more consistent, it can conceal a changing physical process. Increasing correction magnitude may be an early sign that a consumable, temperature, ink state, or transfer condition is moving away from its established baseline. A healthy control strategy monitors both the final result and, when accessible, the growing correction effort. [7, 8]
4. Offset lithography: ink film, dampening, and response delay
In conventional wet offset, the output depends on a distributed ink train, the plate, blanket, substrate, and ink–water interaction. Ink-key settings influence ink supply, but the film delivered to the substrate is not simply proportional to one key movement. Ink splits repeatedly in roller nips. Temperature changes rheology and tack. Fountain solution interacts with the ink; the amount and character of emulsified water can alter transfer and print quality. The response also depends on the substrate and transfer surface.
Research on the emulsification of sheet-fed offset inks measured solid density and dot gain during runs and showed that changes in fountain-solution behavior can affect both ink–water balance and print variation. Separate research into fountain-solution chemistry found relationships among operating water properties, dot behavior, and printed quality. These studies support the conclusion that stable image input does not make ink transfer invariant. They do not establish a single universal optimum for all ink and dampening formulations. [1, 2]
Color correction may be carried out manually using measured solids and tone patches, or automatically by sensing the output and adjusting the ink supply. In either case, the inking train introduces a delay between action and final printed response. Successive key movements made before that response is known can lead to oscillation. The correct practice is to verify the measurement, determine whether the deviation is localized to a zone or present across the sheet, allow for the press's known response, and check the printed outcome before making another change.
A density shift with otherwise stable tone reproduction suggests a different investigation from a localized TVI shift or a neutral cast with acceptable solids. Some deviations require repairing the transfer or dampening condition—not adding ink.
5. Flexography: rheology, anilox transfer, and contact mechanics
Flexographic printing meters ink through an anilox and transfers it through a relief plate to the substrate. Engraved cell geometry matters, but nominal cell volume does not guarantee the same usable quantity of ink will leave the cells under every condition. Transfer also depends on blade condition, ink viscosity and rheology, temperature, plate surface, impression, speed, substrate, and drying behavior.
Water- and solvent-based systems may change as volatile components evaporate or as operators add replenishment fluid. Some water-based formulations are sensitive to pH; the relevance of pH depends on the resin system and must not be generalized to every flexographic ink. A loss of transfer can also arise from contamination or partial blockage of anilox cells, even when a viscosity record looks normal.
Controlled studies have shown that viscosity, ink chemistry, and substrate type affect density and tone reproduction, while separate flexographic experiments linked ink temperature and anilox specification to transfer behavior. The direction and magnitude of change depend on the system: higher viscosity does not universally mean higher or lower printed density. [3, 4]
A sound investigation compares solid patches and midtones, maps left-to-right uniformity, and records ink condition, temperature, press speed, anilox, and impression status. Manual or automated replenishment and viscosity control support consistency, but do not replace spectrophotometric confirmation of the printed result. An ink formulation change should not be the first response to a mechanical transfer problem.
6. Gravure: engraved volume does not eliminate variability
Gravure meters liquid ink from engraved cells and transfers it through a printing nip. Cell geometry provides a repeatable physical basis for deposition, but actual transfer depends on ink rheology, solvent balance, doctor-blade condition, contact pressure, substrate behavior, and drying conditions. A fixed engraved cylinder cannot make a changing liquid formulation or doctoring condition irrelevant.
During a long run, controlling the ink condition and verifying measured output are therefore still necessary. The same distinction applies: the system may exhibit stable average density while changing its across-web uniformity, or a change in the measured color may arise from the substrate rather than the engraved cylinder.
7. LEP adds a second physical system: electrostatic image formation
Liquid electrophotography (LEP) is digital in its image description but physical in image formation. A reusable photoconductive surface is charged, selectively exposed to create an electrostatic latent image, developed with charged pigment-and-resin particles dispersed in an insulating liquid, and transferred to an intermediate blanket. On the intermediate surface, the image consolidates before the final transfer to the print substrate.
Color consistency therefore depends on charging stability and optical exposure, liquid development, ink condition, first transfer, blanket behavior, thermal-mechanical transfer, and substrate optics. An unchanged raster file does not guarantee that the delivered colorant mass, tone reproduction, or transfer efficiency remains unchanged. Electrical process variables add mechanisms that conventional offset and flexographic presses do not share. [5, 6]
In this article, LEP refers to process principles, not the controls or specifications of a particular product. Sheet-fed and web-fed implementations can differ substantially in sensing, sampling, and feedback architecture.
8. Applied voltage, local electric field, and particle charge are different quantities
A developing ink layer in LEP is influenced by the electrostatic potential of the imaging surface, the applied potentials of neighboring components, the field in the development region, and the electrical properties and charge state of the particles. These are not synonyms.
Voltage (potential difference) is a difference in electrical potential. The electric field is the local field that acts on a charge. Particle charge describes the electrical charge carried by a dispersed ink particle. In basic electrostatics, the force on a charged particle is F = qE. A simple planar approximation sometimes expresses an average field as E ≈ ΔV/d; actual development zones are more complicated because geometry, deposited charges, and dielectric properties affect the local field.
Thus, maintaining one applied voltage does not necessarily maintain identical particle motion if ink charge distribution, conductivity, local geometry, or charge retention changes. The same recorded voltage can coexist with a different effective development or transfer condition. Conversely, a measured change in optical density is not evidence, by itself, of an electrical fault. Competing explanations include ink concentration, the transfer path, blanket condition, substrate optics, and measurement.
9. The growing ink layer can influence its own electrical environment
When charged particles are attracted to an imaging region, they form a developing colorant layer. Charge associated with that layer, together with its thickness and dielectric properties, can modify the local distribution of electric potential and field. The magnitude and direction depend on architecture and conditions; it would be inaccurate to claim that the potential always increases or always decreases during layer build-up.
A second time-dependent effect concerns charge retention. A published experimental study of liquid electrophotographic ink examined how charge behaves between electrically driven transfers and after mechanical transfer. It demonstrated that retention and decay occur over time scales relevant to printing. Another study examined the dielectric response of thin polymer coatings used in an intermediate LEP transfer surface under changes in temperature, pressure, voltage, and frequency. These studies establish credible physical mechanisms; they do not show that voltage drift is the dominant cause of every color-consistency problem on commercial presses. [5, 6]
The engineering implication is precise: stable color depends on repeatable effective development and transfer conditions, not merely on a nominal supply voltage or a fixed digital separation. A shift in particle charge or electric-field distribution can alter deposition behavior, which in turn can influence film coverage, optical density, tone response, or transfer uniformity. The actual causal chain in a particular production incident must be verified with available measurements and controlled comparisons.
10. Multi-separation image building and the meaning of a 'changing layer'
Several color separations may be developed sequentially and, in some LEP architectures, accumulated on a common intermediate surface before a single composite transfer to the substrate. In other architectures, the transfer sequence differs. The optical and physical state encountered by later separations can differ from that of the first; local charge, dielectric layering, film thickness, and transfer condition may all be relevant to engineering models of image formation.
It is essential, however, to distinguish within-image layer interaction from time-based color drift across thousands of impressions. The first concerns how multiple separations combine in one image. The second concerns whether the press reproduces that combination consistently as operating conditions evolve. A plausible electrostatic mechanism for one should not be presented as proof of the other without direct evidence.
11. Sheet-fed LEP: periodic verification with dedicated samples
In a class of sheet-fed LEP control architectures, dedicated measurement sheets are produced at selected intervals and read by a measurement path operating in parallel with production. This arrangement enables repeated color verification while the production stream continues. The sampled sheet provides evidence about the current printed state; a supported feedback mechanism can then apply bounded corrections.
Because these measurements are discrete, the sample interval and detection-to-correction delay matter. A short disturbance occurring between samples might not be observed; a persistent drift can be found and compensated when its signal is large enough, and the correction authority is appropriate. The press baseline, color reference, substrate definition and measurement method remain prerequisites.
This describes a general sheet-fed implementation principle, not a universal rule for every sheet-fed LEP press. No proprietary sample frequencies, menus, calibration forms, correction algorithms or product-specific values are reproduced.
12. Web-fed LEP: feedback from measured marks along the web
In web-fed LEP architectures with supported continuous color control, dedicated measuring strips or marks can be printed along the moving web. A spectrophotometric measuring system reads the output over successive sections and permits comparison with a reference acquired under defined conditions. Depending on implementation, monitoring and corrections may cover installed process inks and selected emulated spot colors.
A web-fed process provides time-ordered observations along the machine direction (MD). Across-web measurements, when available, describe the cross direction (CD); do not confuse one dimension with the other. Repeated MD measurements can reveal gradual drift, step changes at reel transitions, stop/restart effects, and control responses. A cross-web nonuniformity problem may remain even when the average longitudinal trend is stable.
Monitoring an emulated spot color is not necessarily equivalent to controlling its underlying process channels. A process-channel adjustment may influence many image colors; a color-specific recipe compensation may affect a more limited set of separations. In all cases, feedback maintains a defined printed state; it does not create a physically unattainable color or repair missing dots and poor transfer.
How the measurement architecture changes the feedback loop
Control aspect | Sheet-fed LEP | Web-fed LEP |
|---|---|---|
Observation | Dedicated measurement sheets or sampling path | Printed measuring marks along a moving web |
Sampling behavior | Discrete verification events separated in time | Successive longitudinal observations in MD |
Across-width behavior | Multiple positions across a sheet can be evaluated | CD uniformity needs relevant across-web sampling |
Feedback limitation | Correction follows sample production and reading | Correction follows strip detection and analysis |
Shared constraint | A qualified reference and physical press baseline are essential | A qualified reference and physical press baseline are essential |
This is a conceptual comparison of implementation classes; equipment capabilities and controller details vary.
13. Color consistency, continuous color calibration, and color tracking
Color consistency is a required output property. Continuous color calibration (CCC) is a family of feedback-based production functions that use repeated measurements to help preserve the output state. Color tracking is the reporting or supervisory function that displays measured deviations, trends, and warnings. Tracking alone is not correction, and correction alone is not full root-cause diagnosis.
An important distinction is that an in-run reference can be derived from an approved initial printing condition. Such a controller may maintain consistency relative to that starting state even if the initial state was not accurately matched to the customer's intended color. First establish and approve the color aim; then maintain it through the run. A controller may also need to establish a new reference following defined process changes. Rules vary by sensing architecture and must not be generalized across systems.
Product color requirements are established on the finished item, when finishing changes its optical appearance. A press-side measurement before varnish or lamination cannot by itself guarantee the final packaged result.
14. Why a color-tracking screen cannot tell you the root cause
A chart displaying an increasing Delta E can be highly informative without revealing the mechanism. Consider a spot color moving toward lower chroma. Possible causes include changes in one process ink, tone response, transfer efficiency, substrate optics, or measurement conditions. Delta E expresses the difference, not which process component produced it.
For diagnosis, examine signed changes in L*, a*, and b*; supporting spectral data when available; solid OD; tone response; neutral patches; overprints; and location across the sheet or web. A controller's adjustment history can add evidence about compensation burden, but growing correction demand is a warning to investigate, not proof of a failed component.
Never use spot-recipe modification to conceal an unqualified press condition. Confirm the baseline first. If it is stable yet an approved recipe cannot reach the target, controlled recipe refinement may be justified; if the baseline itself has moved, restore the physical process before changing the recipe. [7, 8]
15. Measurement discipline and statistical process control
A meaningful color trend requires a stable measurement method. Instrument calibration and agreement, measurement conditions (such as M0/M1/M2 where relevant), geometry, backing, sampling position, sample state, and the agreed formula for color difference all affect comparability. ISO 13655 describes spectral measurement and colorimetric computation in the graphic arts. ISO 20654 provides a metric for the tone value of spot colors. [9, 10]
A specification limit is not a statistical control limit. A job may meet a customer's Delta E tolerance while showing a persistent drift. Conversely, a statistically stable process can remain consistently off-target. Charts such as Shewhart, EWMA, or CUSUM may be useful when assumptions, sampling, and baseline selection are defensible. Short-interval samples may be autocorrelated, and a control chart copied from another process may be misleading.
The monitoring plan should identify critical colors, spatial positions, time intervals, stop/restart checks and escalation rules. Do not average before- and after-calibration measurements indiscriminately: they may represent different control states. A change in substrate, coating, or finishing condition should likewise be documented as a new relevant factor rather than silently pooled into one population.
16. A diagnostic matrix for production color drift
Observation | Plausible mechanisms | Best next discrimination |
|---|---|---|
Gradual solid-density change in one ink | Ink condition, metering, development or transfer | Compare ink/transfer records, solid OD, and tone patches by time |
Solids stable; gray balance moves | Differential tone behavior or process-channel relationship | Measure midtones, neutrals and signed Lab changes |
Step at substrate or reel change | Surface optics, coating, moisture, or preparation | Compare known reference vs new lot under same measurement condition |
Variation confined to a cross-web zone | Local ink delivery, impression, developer, or transfer nonuniformity | Map positions rather than relying on overall average |
Gradual change despite frequent corrections | Baseline movement; controller compensation burden | Inspect intervention history and independent physical checks |
Drift appears only after finishing. | Varnish, adhesive, film optics, or curing change | Compare press sheet and finished construction separately |
LEP deviation with suspected electrostatic contribution | Particle charge, development field, or dielectric/transfer behavior | Review qualified electrical/process indicators, isolate non-electrical causes |
Sudden offset response to key adjustments | Ink-train response delay and overcorrection | Wait for response, compare ink-key history and successive measurements |
This table presents investigative hypotheses, not automatic root-cause labels. A measured symptom must be connected to a verified mechanism before a permanent corrective action is declared.
17. A controlled method for maintaining color through a long run
Establish the printing condition. Confirm that the press, consumables, ink system, and defined substrate are qualified; identify the screening, calibration state, output characterization, and critical color aims. Resolve transfer or material defects before attempting to compensate for them numerically.
Approve the first measurable state. Retain a start-up reference under a declared measurement condition. Record its solids, midtones, neutrals, and critical brand colors. Where finishing materially alters appearance, retain or define a finished-product reference as well.
Sample in time and space. Define a risk-based schedule and positions appropriate to the job and technology. Capture the first acceptable impression, meaningful intermediate points, the end of the run, and samples after major stops, material changes, or relevant maintenance. Avoid invented universal sampling intervals.
Separate detection from response. Confirm that a trend is real before changing ink feed, viscosity, electrostatic, or digital calibration settings. Identify whether the problem affects one channel, many channels, a region of the sheet/web, or only the finished structure. Allow time for controller and press response.
Verify each correction. Record what was adjusted, why it was adjusted, the expected direction of change, and the measured result. Avoid several simultaneous changes unless a validated procedure explicitly requires them. Repeated adjustments without a stable diagnosis can produce apparent improvement while obscuring a developing fault.
Close the loop on the product, not only the screen. Confirm that the released sheets or reels satisfy the agreed requirements. Mark the portions printed before and after any significant calibration or intervention. Review the trend and accumulated correction effort for next-run learning.
18. Three illustrative investigations
Offset: the wandering blue. At start-up, a blue brand color passes. Density subsequently fluctuates while operators repeatedly adjust one ink zone. The correction record shows that changes were made before the previous movement had fully propagated through the inking system. An engineering investigation separates measured color noise from actual drift, assesses the ink–water state, and introduces a controlled decision interval. This is a hypothetical example, not a published trial.
Flexography: the solids pass, the tint fails. A midtone area grows heavier while a solid patch remains acceptable. A reflex correction to viscosity alone would be unjustified. The team checks the anilox, plate impression, tone-patch behavior, ink temperature, and substrate, and then tests one variable at a time. You can change TVI without changing the measured solid proportionally; the print data, not a single setting, decide the next step. This is a hypothetical example.
LEP: color remains stable, but corrections grow. The output Delta E remains inside limits through a long production session, yet increasingly large digital corrections are needed. That result can reflect successful feedback and also signal a need to check the process baseline. The team compares ink condition, transfer surfaces, calibration history, substrate, and qualified electrostatic/process indicators. No electrical cause is declared without evidence. This is a hypothetical example.
19. Engineering conclusion: controlled color is not a motionless process
A conventional or LEP press is capable of stable production, but the physical state that produces its color is never guaranteed by an unchanged file, plate, or nominal parameter alone. Offset must govern ink-film distribution and ink–water interaction; flexography must control rheology and metered transfer; gravure must maintain fluid and cell-transfer conditions; and LEP must additionally preserve repeatable electrically driven image formation and intermediate transfer.
In both sheet-fed and web-fed LEP, continuous color control may preserve the printed result through recurring measurement and correction. Their sampling paths differ, but neither bypasses the requirement for a qualified physical process. The electrical potentials, local electric fields, and particle charges that shape liquid development add important variables to stability—without implying that a color deviation proves a voltage fault.
The strongest press-control systems distinguish what the customer sees from what the machine is doing to produce it. They measure the outcome, understand process delay, diagnose the mechanism, correct only within known authority, and verify the finished product. The goal is not to eliminate every physical change. It is to keep the approved color reproducible throughout the entire run, and to know when the system is working harder to achieve it.
Research, standards, and evidence notes
[1] Chen, Q. (1986). Emulsification Rate of Sheet-Fed Offset Ink and Its Effect on Printed Quality. Rochester Institute of Technology thesis.
[2] Virtanen, J., Kataja, K., & Varjos, P. (2003). The Effect of Tap Water and Fountain Solution on Sheet-Fed Offset Print Quality. VTT research report.
[3] Gençoğlu, E. N. (2012). Influence of Ink Viscosity on Dot Gain and Print Density in Flexography. Asian Journal of Chemistry, 24, 1999–2002.
[4] Keawkul, P., Pachonklaew, P., & Waleetorncheepsawat, B. (2022). Optimization of Printing Conditions to Achieve Effective Ink Transfer in Flexographic Printing. Journal of Printing Science and Technology, 59, 298–302.
[5] Anthony, T. C., Chang, S., Lam, Q., & Gila, O. (2012). Experimental study of ink-particle charge retention in LEP; NIP28 proceedings, article art00059_2.
[6] Kahatabi, R., Salalha, W., Forgacs, P., Yacoub, N., & Avramov, D. (2012). Dielectric Properties Study of Thin Polymer Film Layers Used in LEP. NIP28 proceedings.
[7] Ink Flow Control by Multiple Models in an Offset Lithographic Printing Process (2008). Computers & Industrial Engineering.
[8] ISO 12647-2:2013. Graphic technology — Process control — Part 2: Offset lithographic processes.
[9] ISO 12647-6:2020. Graphic technology — Process control — Part 6: Flexographic printing.
[10] ISO 13655:2017. Graphic technology — Spectral measurement and colorimetric computation for graphic arts images.
[11] ISO 20654:2017. Graphic technology — Measurement and calculation of spot color tone value.
[12] Technical materials supplied for this article (2020–2023): process-color consistency, production tracking, and sheet-fed/web-fed LEP feedback architectures. Consulted for conceptual differentiation only; no operating recipes, proprietary tables, copyrighted diagrams, or brand-specific workflows are reproduced.
Evidence and intellectual-property note. The descriptions above are original synthesis from publicly described mechanisms, research, standards metadata, and supplied technical training materials. Control concepts should not be read as claims that all presses expose the same sensors, automation, or set points. The research describes mechanisms and experimental observations; hypothetical cases are explicitly identified. A technical reference is not certification of a specific press or its commercial performance. For publication, use the current locally applicable versions of all purchased standards and the validated procedures of the relevant equipment manufacturer.