Ronen Dolev
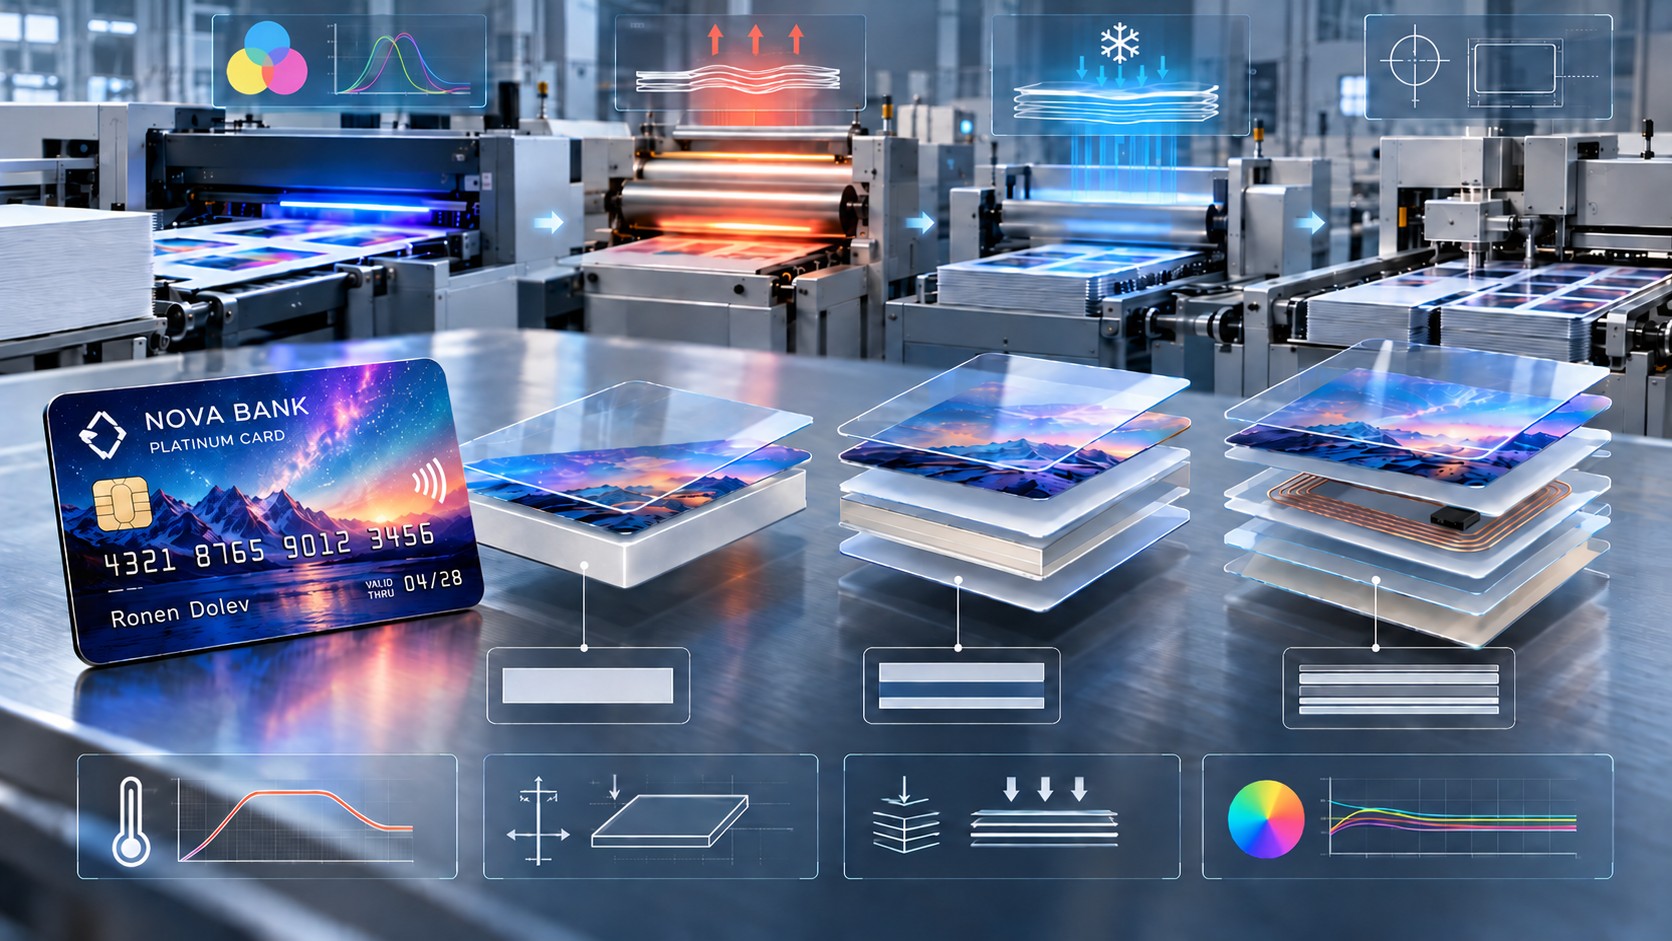
A plastic card is not simply a printed piece of PVC. It is a designed, multilayer product whose final quality depends on what happens before printing, during thermal consolidation, and after the sheet leaves the laminating machine. This article follows the application-development process from finished-card requirements and core architecture through material selection, surface preparation, LEP printing, hot- and cold-lamination cycles, punching, and qualification. A focused troubleshooting section appears at the end.
The application begins with the finished card
Plastic cards share a familiar shape, but their intended functions can differ greatly. A gift or membership card may primarily carry visual information. An access card may be handled frequently and must maintain its dimensions and surface integrity over time. An identification or financial card may need greater mechanical durability and compatibility with defined reader systems. A contactless card adds another requirement: an antenna-bearing inlay must survive manufacturing and perform reliably inside the finished card.
For an industrial development project, the first question is therefore not whether the digital printing press can print the selected PVC. It is what the finished card must do and which tests will prove it can. The answer governs the core construction, layer-thickness budget, protective overlays, thermal bonding method, positioning references, and acceptance criteria.
In the widely used ID-1 format, the nominal dimensions are 85.60 × 53.98 mm with a nominal thickness of 0.76 mm, as specified within the ISO/IEC 7810 physical-characteristics framework. The applicable edition, tolerances, mechanical performance requirements, and any additional scheme or customer requirements must be established for the actual card category. These measurements belong to the completed product—not merely to the printed sheet before lamination.
A card structure that looks attractive and prints cleanly can still be unfit for manufacturing if its layers move, soften, cloud, separate, or distort during later stages. This is why the application must be engineered as one production route rather than as separate, individually successful operations.
Choosing the architecture: solid, split, or multi-core
The technical distinctions include simple or solid-core cards protected by varnish, solid-core cards with external lamination, split-core constructions, and multi-core constructions. These are not simply marketing categories. They describe different interfaces, layer thicknesses, and bonding responsibilities.
Architecture | Typical construction | Practical application and development focus |
|---|---|---|
Simple/solid core with varnish | One plastic core with printed graphics and protective coating | Membership, business, promotional, and simple access cards; fewer interfaces and no overlay lamination |
Solid/mono core with lamination | One relatively thick printed core protected by outer overlays | Gift, membership, and identification cards; the thick core must be printable and dimensionally stable |
Split core with lamination | Two core sheets brought together, typically with transparent overlays outside | Applications needing front/back construction flexibility and controlled card-body geometry |
Multi-core with lamination | Multiple functional layers with an optional antenna-bearing inlay | Contactless access, identification, and other advanced cards; inlay placement and layer interactions must be qualified |
Solid core: a straightforward construction with demanding material handling
The simplest form of solid core uses a single plastic layer and a protective varnish rather than separate laminate overlays. Where more durability is required, a solid core can also be protected by overlays on both sides. In either case, the core provides most of the card's structural thickness. Its stiffness, surface condition, thermal response, and printability must therefore be considered together.
A thick solid-core sheet may be attractive because there are fewer internal interfaces to bond. That advantage does not eliminate processing constraints: the chosen sheet must travel reliably through the press and subsequent machines, and its thermal behavior must remain suitable for the intended finishing route.
Split core: two printed halves and a central bond
A split-core design uses two thinner PVC sheets rather than one thick body. One representative nominal thickness calculation is two 320 µm half-cores plus two 60 µm overlays, totaling 760 µm before accounting for real manufacturing tolerances and the effects of printed and bonding layers. It is an architectural example, not a universal bill of materials.
This approach can make front-and-back artwork management and sheet handling more practical. It also introduces a critical central core-to-core interface. That interface must acquire sufficient strength under the selected temperature, pressure, and time without compromising the printed faces adjacent to the outside overlays.
The finished thickness is a fixed design budget. Choosing a thicker overlay without adjusting another layer does not make the additional microns disappear. In practice, layer selections must be verified after consolidation, not accepted solely on the sum of incoming material nominal gauges.
Multi-core: when functionality is inside the card
A multi-core card incorporates additional internal layers to accommodate a functional inlay or other features while retaining the required external geometry. In contactless applications, the antenna is part of an inlay incorporated into the card body. NFC describes a communication technology; it is not itself a separate plastic substrate layer.
The position of the antenna-bearing inlay, local thickness variation, contact between neighboring materials, and clearance to the eventual punching line are all part of the application design. The inlay must remain in place and functional after the heat-and-pressure cycle, after cooling, and after punching. A flat card with excellent graphics but nonfunctional contactless performance is not a qualified product.
Material selection: PVC is a family, not one behavior
PVC is widely used in plastic card construction because it offers a practical combination of processing options, cost, stiffness, and compatibility with several printing and lamination approaches. But two PVC products with the same nominal thickness may behave differently under the same conditions. Their formulations, additives, sheet-manufacturing histories, retained stresses, surface treatments, and softening behavior can differ substantially.
The technical data sheet should therefore be treated as an incoming-material specification rather than a purchasing formality; alongside gauge and surface finish, a development team should request relevant thermal properties, dimensional-stability information, storage and handling requirements, the intended bonding route, and surface-preparation recommendations. The same approach applies to the overlay material; a suitable core paired with an unsuitable overlay is not a suitable card construction.
Vicat softening temperature: why it matters
Vicat softening temperature is a comparative measure of how a thermoplastic resists indentation while being heated under a specified load. Under ASTM D1525, a standardized flat-ended indenter is driven into the specimen as temperature rises; the reported temperature corresponds to the specified penetration depth. Vicat is not the polymer's melting point, and it does not fully predict lamination performance. It does, however, provide useful information when comparing candidate grades.
For thermally bonded split cores, the core surfaces must reach a condition in which a sound central bond can develop. A lower-Vicat grade may allow bonding at a lower temperature, reducing thermal exposure of the adjacent printed layers. In certain PVC split-core constructions, Vicat values of approximately 70–78°C have been used as material-selection reference points. This is a system-specific range, not a general requirement for plastic cards.
Yet low Vicat is not automatically better. A core that softens easily may also be more vulnerable to dimensional movement or pressure-induced distortion during the lamination cycle. A higher-Vicat grade may offer more dimensional resistance at a given operating temperature, but direct thermal joining of its surfaces may require more heat. Where appropriate, a qualified bonding layer can decouple core stiffness from the need to soften the core to form the bond.
The engineering decision is consequently a balance between the core, the overlay, the joining mechanism, the ink and primer system, and the heat history of the full stack. The correct grade produces a repeatable finished product—not necessarily the grade with the lowest or highest Vicat number.
Dimensional behavior must be measured in both directions
A printed sheet can be in registration before lamination and become misaligned with the punching tool afterward. Heating, consolidation, cooling, and relaxation of residual stresses may change the sheet's dimensions. The response can differ between machine and cross directions, and it may not be uniform across the sheet.
In a production troubleshooting case, the printed image remained correctly positioned on the press, yet the PVC changed dimensionally under heat and pressure. The downstream punching machine also used a different reference strategy from the one established during development. The corrective work began with measurements of the material's thermal movement and an analysis of the production reference system; imposition and alignment rules were adjusted only after those factors were understood.
Material qualification should therefore include measurements before and after the relevant thermal process, along both axes, with reference positions recorded. A compensating artwork shift should only be introduced when the movement is sufficiently understood and repeatable. A graphic correction cannot substitute for an unstable substrate or an unsuitable punching reference strategy.
Surface preparation: corona and primer are manufacturing decisions
Successful LEP printing on PVC depends on more than the image-forming process. The printed layer must be anchored to a prepared surface, and that bond must remain effective after the card has undergone lamination. Surface contamination, additive migration, and the incoming PVC history can influence wetting and adhesion.
A controlled corona-refresh step immediately before priming may improve the surface's ability to be wetted by the selected primer. However, higher treatment power should not be mistaken for automatically better performance. Excessive corona treatment may harm the durability of some material systems, and dyne measurements are process indicators—not direct proof of primer or ink adhesion.
For some PVC constructions, an incoming wetting tension above approximately 36 dyn/cm and a controlled corona refresh to around 46–48 dyn/cm can serve as initial process-development reference points. These figures are not universal setpoints. Qualified targets must match the actual PVC grade, primer chemistry, treatment equipment, and finished-card requirements.
Primer: the interface that must survive the later heat cycle
The primer forms the foundation between the PVC surface and the LEP ink. It must wet the material, dry or cure as required, support printing, and retain appropriate integrity when the printed layer is later heated under pressure. Coat weight and complete drying matter: an unnecessarily heavy or insufficiently dried primer can create a weak or mobile interface even if the initial print looks acceptable.
A suitably designed crosslinked primer may be valuable in demanding card-lamination systems. Crosslinking can increase the integrity of a polymer network and, where the chemistry is appropriate, help the coating maintain its function through the thermal process. This is an engineering qualification route, not a universal claim that any crosslinked formulation performs better. Inadequate crosslink development, excessive stiffness, or poor chemical compatibility can themselves create adhesion problems.
Primer coat weight, drying, substrate wetting, and adhesion do not establish one crosslinked primer as a universally proven remedy. A crosslinked candidate should therefore be validated using the real PVC, real printed ink, real overlay, and full heat/cold lamination cycle. The decisive result is post-lamination bond strength and failure location, not simply whether a tape test passed immediately after printing.
Corona treatment over the already printed ink before overlay bonding is a different decision from corona treatment of bare PVC before primer. It may help some overlay-bonding systems, but it must be assessed separately, with the minimum effective treatment and suitable adhesion testing.
LEP printing: excellent registration is the beginning, not the end
In compatible sheet-fed LEP systems, a multicolor image can be formed and transferred to the synthetic sheet with accurate intercolor registration. That is especially useful for high-definition card graphics, fine lines, short runs, and variable content. Nevertheless, the card must be designed around more than the print boundary.
Prepress should provide positioning and punching references appropriate to the subsequent lamination and converting machines. These references must account for how the finished structure will be measured and held, rather than assuming that a corner or mark remains in an identical geometric relationship to the image throughout the process.
Color targets should be defined for the intended final product. Transparent overlays can alter gloss, reflection, and perceived color even where ink chemistry remains unchanged. A color measurement on unlaminated print is useful as a press control point, but it does not fully approve the finished card's appearance. Any thermal or chemical instability that develops during lamination must be eliminated before the press is asked to compensate for it.
Collation: building the stack without losing position
After printing, the relevant cores, overlays, and optional inlay are brought together in their final order. All layers must align to the production reference strategy and be held in place before entering the laminator. Some processes use localized tacking or temporary fixation to prevent movement during handling.
This stage directly affects the finished card. Misregistration introduced during collation cannot generally be corrected after heat and pressure have consolidated the stack. Cleanliness also matters: dust, particles, and contaminated interfaces can cause local voids, surface defects, or reduced bond integrity. In a multi-core construction, the inlay must be positioned so that its clearance to later punch boundaries is protected by design, not by operator judgment alone.
The hot lamination cycle: transferring sufficient heat, not maximum heat
A card-lamination machine generally consolidates arranged stacks between smooth or textured metal plates under a controlled combination of temperature, pressure, and time. Plate finish can affect the outer surface appearance: a smooth plate may produce a glossier result, while a textured plate can impart a matte texture through the overlay.
The process must be defined by the temperature reached at the bonding interfaces, not by the heater setpoint alone. Heat moves through overlays, printed layers, cores, and any internal components. Thicker stacks and larger cassette loads take longer to reach an appropriate internal temperature. A plate set too hot may overexpose the outer printed regions before the center of the stack has reached its target condition.
Pressure ensures contact, but more pressure is not automatically better. Excess pressure can deform PVC and disrupt the printed layer. The appropriate pressure is the minimum that, together with the thermal conditions and chemistry, reliably produces the required bond and finished geometry.
A valuable development strategy is to evaluate whether a somewhat lower plate temperature, with a controlled adjustment in heating time, can bring the required interfaces into their bonding window with less severe surface exposure. This can be particularly helpful when color appearance or printed-layer integrity is sensitive to peak temperature. However, a longer dwell also increases accumulated thermal exposure and can aggravate dimensional change. It must not be treated as a guaranteed cure.
A practical lamination setup starts at the lowest temperature that develops the required bond strength and increases heat only when measurements justify it. Once the center of the cassette has reached the necessary bonding condition, unnecessary additional heating should be avoided. Evaluating a lower plate temperature with a carefully controlled change in dwell time can be useful, but only if bond integrity, dimensional stability, and finished-card performance remain acceptable.
The cold cycle: locking in geometry as well as the bond
Cooling is part of the lamination process, not simply a wait before the next operation. As the consolidated layers cool, they regain stiffness and develop their final response to retained stresses. Releasing pressure while the PVC remains too soft may permit warpage or additional dimensional movement. Nonuniform cooling can also introduce undesirable stress gradients across the sheet.
Forced cooling may use air or water; water can provide more effective heat transfer under comparable conditions. For certain PVC card constructions, releasing pressure after cooling to approximately 25–40°C has been used as a process reference. That range is not a universal unloading criterion. The appropriate release condition depends on material composition, stack thickness, machine design, and finished-card tolerances.
The hot and cold phases must therefore be qualified together. A heating sequence that gives acceptable LBS can still yield poor flatness after an inadequate cold cycle. Conversely, improved cooling cannot make up for incompatible bonding chemistry. Stability emerges from the combined cycle and material structure.
Surface gathering and overlay deformation
Gathering of the top overlay can manifest as wrinkles, localized waves, or accumulated material after consolidation. One possible explanation is a mismatch between the overlay and the underlying core in thermal softening, dimensional relaxation, or shrink response. Excessive pressure, trapped air, uneven heat, or poor collation may create similar visual symptoms.
The investigation should distinguish those mechanisms rather than label every wrinkle a low-Vicat problem. Comparing the thermal behavior of core and overlay separately, then in the complete laminated stack, can show whether the selected materials are moving incompatibly. Remedies may include a more suitable overlay/core pairing, reduced peak temperature, adjusted heating and cooling, pressure correction, or better layer positioning.
Lamination bond strength: measuring the actual interface
A laminated card needs measurable interlayer integrity. Lamination Bond Strength (LBS) is usually evaluated through a controlled peel or delamination test: one layer is separated from the adjacent layer while the instrument records the required force. The specified test geometry, peel angle, speed, specimen width, conditioning, and reporting rules must be used consistently.
One representative peel-test configuration uses strips 10.00 ± 0.2 mm wide, a 90-degree peel, and a crosshead speed of 300 mm/min under a defined procedure related to ISO/IEC 10373-1. These conditions must be checked against the applicable testing requirements rather than assumed for every card. The test record should preserve the force trace, minimum relevant measurement, sample identity, and any cohesive tearing or other observed failure modes.
The instrument measures force in Newtons (N). To compare results from specimens of different widths, express peel resistance as force per unit width (e.g., N/cm). For a specimen exactly 10 mm wide, 5.5 N of measured peel force corresponds numerically to 5.5 N/cm. That numerical equivalence does not apply unchanged when the test width differs.
Card construction | Illustrative peel-resistance reference | Equivalent force on an exactly 10 mm strip |
|---|---|---|
Security-card construction | 5.5 N/cm | 5.5 N |
Other card applications | 3.5 N/cm | 3.5 N |
The figures shown are illustrative, construction-specific reference values—not universal pass/fail limits under ISO/IEC 10373-1. The controlling product specification, applicable standard edition, and customer or approval-program requirements must establish the actual acceptance level.
Equally important, a peel value without the failure mode tells only half the story. Delamination at the overlay-to-ink interface is not the same defect as primer lifting from PVC, ink separating from primer, core-to-core weakness, or cohesive tearing through a layer. Two samples can produce similar forces and point to entirely different corrective actions. Every application qualification should document both force and fracture location.
Mechanical durability: beyond the peel test
Card performance also depends on dimensional stability, flatness, bending, torsion, handling durability, and resistance to separation after repeated strain. Relevant ISO/IEC 10373 test methods provide controlled ways to measure properties associated with ISO/IEC 7810 card categories, while additional endurance requirements may apply through ISO/IEC 24789 and the product's own qualification route.
A force value in Newtons is not meaningful without identifying the loading geometry, displacement or deflection, number of cycles, and failure criteria. Bending strength, bending stiffness, and peel resistance are different quantities. A card can pass the specified LBS test and still exhibit unacceptable warpage or fatigue behavior. For contactless cards, mechanical conditioning should also be followed by checks of the actual communication function.
Thus, mechanical qualification must examine the finished card under the conditions relevant to its intended life. A printed sheet and a laminated card are different test objects; approving one does not approve the other.
Punching: the final geometry exposes earlier decisions
Punching converts the laminated sheet into individual cards. Tool alignment, punch reference marks, finished sheet dimensions, card-edge quality, and inlay clearance all become critical. If the sheet changes size after lamination, its printed image may no longer align with the tooling, even though it was perfectly located when printed.
A manufacturing troubleshooting case illustrates the importance of tracing positioning references throughout the production route. Measurements showed that the PVC changed dimensions during lamination and that the production punching machine used a reference strategy different from the one used during development. Rather than shift the artwork arbitrarily, the team redesigned the imposition and registration references around the actual geometry of the laminated sheet.
The final punching stage should confirm card dimensions, corner quality, edge integrity, absence of local delamination, and safe clearance of any antenna-bearing inlay. For a contactless structure, functional verification after punching is necessary because a card that passes optical and dimensional inspection may still have been damaged in conversion.
Standards and final application qualification
The production route must end with a qualification plan derived from the intended card category. Standards identify physical characteristics, test procedures, and—for relevant technologies—communication behavior. They do not authorize the substitution of one test result for another, and the applicable edition and external scheme requirements must always be confirmed.
Standard or method | Role in the card application |
|---|---|
ISO/IEC 7810 | Identification-card physical characteristics and card-format requirements, including ID-1 geometry |
ISO/IEC 10373-1 | General identification-card test methods, including relevant mechanical and delamination testing |
ISO/IEC 14443 series | Proximity contactless-card communication and interoperability framework |
ISO/IEC 10373-6 | Technology-specific test methods for proximity/contactless card operation |
ISO/IEC 24789 series | Card service-life and durability evaluation framework where applicable |
ASTM D1525 | Vicat softening-temperature measurement for thermoplastic materials |
The qualification sequence should be traceable from incoming PVC lots through surface preparation, printing, collation, hot and cold cycles, bond testing, dimensional verification, punching, and final function. It should cover representative production conditions and material-lot variation rather than one exceptional laboratory sample. The objective is a usable manufacturing window with margin, not one perfect demonstration card.
Troubleshooting: diagnose the failed interface at the end of the process
Only after the application route has been properly defined does troubleshooting become efficient. The central principle is to start with the point of failure and work backward through the interfaces and process stages that can physically explain it. Avoid changing press calibration, primer, laminate temperature, and material selection simultaneously: the outcome may improve without revealing why.
Observed symptom | First mechanism to investigate | Evidence-led corrective direction |
|---|---|---|
Low LBS at overlay-to-ink interface | Bonding-layer chemistry, surface condition of printed ink, activation during the hot cycle | Verify bonding system and thermal window; evaluate controlled post-print surface treatment only if compatible. |
Low LBS at ink/primer/PVC interface | Surface preparation, primer compatibility, coat weight, drying, thermal integrity | Identify precise failure location; qualify corona refresh and suitable primer, potentially a crosslinked system. |
Cloudiness or color shift after lamination | Optical effect of overlay, heat exposure, or chemical incompatibility | Measure before/after cooling and after conditioning; compare lower peak temperature and compatible primer/overlay chemistry |
Gathering or wrinkling of top overlay | Overlay/core mismatch, pressure, trapped air, or uneven heating and cooling | Compare material softening and shrink response; correct collation, pressure, and the joint thermal cycle. |
Dimensional movement | Residual stress relaxation, different thermal response of layers, or excessive exposure | Characterize machine/cross-direction movement; select suitable materials and thermal cycle before changing artwork. |
Graphic-to-punch offset | Dimensional change combined with unsuitable production references | Rebuild and verify imposition and punching references using the laminated sheet's actual geometry |
Contactless performance failure | Inlay displacement, thermal/mechanical damage, inadequate punch clearance | Review stack geometry, heat/pressure, and punching; verify operation at successive process stages |
For low LBS, the first useful observation is where the specimen actually opened. For a color shift, determine whether the difference comes from overlay optics or evolves under heat and chemistry. For dimensional movement, establish whether the deformation is uniform and repeatable before introducing a compensation. Lower temperature with a carefully validated time adjustment may help a thermal-damage case, but it is not a substitute for compatible PVC, primer, overlay, and bonding chemistry.
Conclusion: the card is manufactured after it is printed
High-quality LEP printing can deliver precise graphics on a properly prepared plastic sheet. Producing a reliable plastic card requires more: an application-specific core architecture, PVC and overlay grades with compatible thermal behavior, appropriate corona and primer preparation, accurate collation, a qualified hot/cold lamination cycle, sufficient and correctly characterized LBS, stable dimensions, accurate punching, and the necessary functional tests.
Solid core, split core, and multi-core are different ways of managing this system; none is automatically correct for every card. Vicat can help explain material choices, but it does not fully predict lamination behavior. A crosslinked primer may improve the thermal robustness of one interface, but only the complete construction can demonstrate that improvement. A lower peak temperature may preserve the print, but only if the resulting bonding and cooling cycle still satisfies the finished-card requirements.
The core lesson is practical: the printing press creates the image, while materials engineering and the downstream process turn that image into a durable, dimensionally accurate, functional card. Success is not the appearance of the printed sheet. It is the finished product's performance.
References and technical notes
The technical discussion draws on plastic-card manufacturing, including card constructions, surface preparation, thermal processing, peel-test methods, and application-specific numeric examples. The dimensional-movement and punching-reference case draws on Ronen Dolev, The Personal Journey of an Industrial Printing Expert, Chapter 7, "The Application That Had to Exist First." That chapter is a literary adaptation of professional experience and should not be treated as a verbatim record of an identifiable manufacturing site.
Standards and test frameworks referenced in this article include ISO/IEC 7810, ISO/IEC 10373-1, ISO/IEC 14443, ISO/IEC 10373-6, ISO/IEC 24789, and ASTM D1525; the applicable current editions must be checked. Crosslinked-primer selection and overlay-gathering mechanisms are engineering hypotheses for application qualification, not universal remedies. Numeric process examples and peel-resistance reference values are specific to the systems in which they were developed. Final operating windows, acceptance criteria, and safety requirements must be established for the actual product and production route.