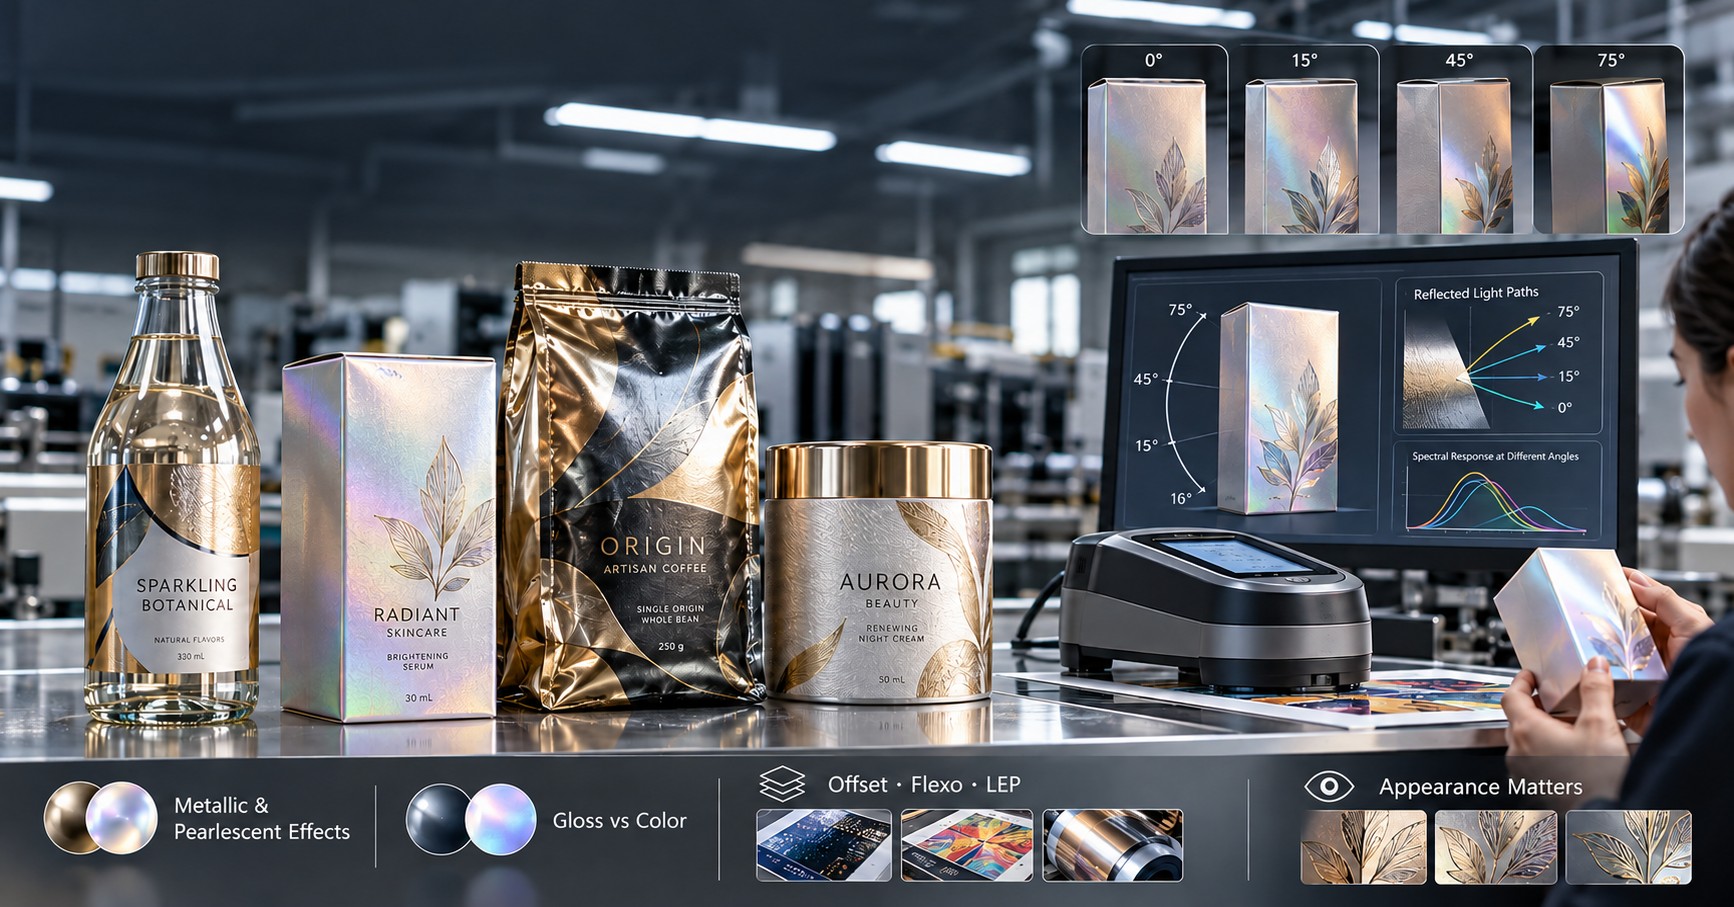
Two packages sit side by side on the quality-control table. One was printed by offset and the other by Liquid Electrophotography (LEP). Both were calibrated, both meet the specified color requirements, and their spectrophotometric measurements produce very similar Lab* values.
The quality manager rotates one package slightly. Suddenly, the difference becomes obvious. One package looks glossier; on the other, the metallic area looks darker. A gold-colored area loses some of its brilliance when viewed from an angle, while the corresponding area on the other package seems relatively consistent. When both packages are returned to their original positions, the difference becomes smaller.
The operator measures the samples again. The color readings still pass. Is this a color problem? Should the profile be corrected? Did the varnish change the hue? Or is the difference an optical phenomenon that conventional color measurements were never intended to describe completely?
Answering those questions requires a distinction between the measured color of a printed surface and its complete visual appearance. In packaging, metallic substrates, pearlescent pigments, effect coatings, and transparent laminates can make appearance depend strongly on viewing and lighting geometry. A single spectral measurement may not be enough.
Multiangle color measurement examines how a surface behaves under defined combinations of illumination and observation angles. It helps separate a genuine color mismatch from differences in directional reflection, scattering, pigment orientation, and surface structure. The distinction is especially useful when comparing printing technologies, because even a close colorimetric match does not guarantee that their ink films and optical structures behave alike.
1. Color and Appearance: Two Related but Different Properties
Printing color control commonly relies on Lab*, the CIEDE2000 color-difference formula (ΔE00), optical density, and tone response. These measurements are essential, but none of them, alone, describes every optical property of a printed object.
Color, in the colorimetric sense, describes a visual response under specified measurement conditions. Appearance also includes gloss, scattering, surface texture, transparency, haze, brilliance, and how a surface behaves when it moves relative to its light source and observer.
Imagine printing the same blue on two substrates. One has a matte finish, and the other is high gloss. Under a controlled measurement geometry, their color coordinates may be close, yet an observer immediately recognizes different surfaces. The high-gloss sample produces a stronger directional reflection; the matte sample spreads more light across other directions.
With metallic and pearlescent inks, the differences can extend beyond gloss and perceived depth. The apparent lightness or even hue may change substantially with viewing angle. This is why color matching at one geometry is not necessarily appearance matching.
2. How Light Interacts with a Printed Surface
When illumination reaches a package, light can reflect off its surface, be absorbed by pigments and layers, scatter within its structure, or pass through transparent components. Two types of reflection shape its appearance.
Specular reflection: directional return of light
Specular reflection sends light predominantly in a direction governed by surface geometry. A smooth, glossy surface tends to generate a stronger specular component. When the package is tilted until that reflection reaches the observer, the surface may produce a bright highlight or glare.
Diffuse reflection: light returned in many directions
On a rougher or optically scattering surface, reflected light is distributed over a wider range of directions. Some incoming light penetrates the ink, interacts with its pigments, and returns after absorption and scattering.
Most printed surfaces combine both effects. Their balance changes with pigment chemistry, binder, substrate texture, coating, and finishing. A regular ink can be highly glossy without being metallic; a metallic pigment can create pronounced angular behavior without necessarily giving the entire surface a uniformly high gloss value. Gloss and metallic effect are not interchangeable concepts.
3. What Is Color Flop?
Color flop describes changes in apparent color as the illumination/viewing geometry changes. The phenomenon is especially noticeable in materials that incorporate effect pigments, including metal flakes and pearlescent particles.
A metallic silver area may look very bright near the direction of specular reflection, then much darker farther away. A pearlescent material may change in both lightness and hue as the angle changes.
Why? Metal-flake pigments are commonly made of small plate-like reflectors. Their collective orientation influences the directions in which light is returned. Pearlescent or interference pigments instead exploit thin optical layers with different refractive indices; their constructive and destructive interference can make the spectral response angle-dependent.
These mechanisms should not be confused. Metallic flakes often emphasize directional brightness, whereas interference pigments can produce substantial hue travel. Both may require multiangle measurement, but they do not necessarily require the same measurement protocol.
4. Metallic Ink, Pearlescent Ink, and Metallic Substrate Are Different Constructions
It is a mistake to assume that every metallic-looking package was printed with metallic ink. Three distinct constructions can produce related visual effects.
Metallic ink on a conventional substrate
Here the reflecting flakes are inside the ink film. Appearance depends on their composition, size, concentration, orientation, the ink binder, the substrate surface, and drying or film-formation conditions.
Pearlescent or interference ink
Here, specially structured particles—sometimes mineral platelets coated with thin metal-oxide layers—produce a pearlescent or angle-dependent appearance through optical interference. Their color travel need not resemble that of conventional metal-flake ink.
Conventional colored ink on a metallic substrate
In this case, the metallic response comes primarily from a layer beneath the ink. Light may pass through a relatively transparent ink film, reflect from the metalized surface, and pass through the ink again on its way to the observer.
These three constructions may look similar at one angle but behave quite differently when rotated. That difference is not necessarily a printing defect: it can be a consequence of the intended optical architecture.
5. Pigment-Particle Orientation and Substrate Texture
Many metallic pigments contain plate-like particles commonly described as flakes. If the flakes lie largely parallel to the printed surface, their reflections may reinforce a stronger directional appearance. If they are distributed across a wider range of orientations, the reflected light is dispersed, and the metallic effect may look softer or less uniform.
It would nevertheless be wrong to conclude that the flattest possible orientation is always best. Some applications deliberately call for a softer, more diffuse metallic appearance. Flake dimensions, shape, surface treatment, concentration, and binder behavior all influence the final result.
A smooth substrate can support a more even film and more uniform angular behavior; a textured or rough substrate may change local flake orientation, the ink film's effective thickness, and the distribution of reflected light. Consequently, the same metallic ink can look different on coated paper, folding carton board, smooth film, and textured stock.
Film formation matters too. An ink that has time to level before setting or curing may not produce the same particle arrangement as a film that rapidly immobilizes its pigments. Metallic appearance is therefore a property of the pigment–binder–substrate–process system, not of the pigment alone.
6. Offset, Flexography, and LEP: Why the Ink-Transfer Mechanism Matters
All three technologies can deliver high-quality printed products, but their ink-film formation mechanisms are different. Those differences can affect surface microstructure, pigment orientation, and the optical response of specialty inks.
Offset: transfer of a comparatively viscous ink through a blanket
In offset, the ink passes from a printing plate to a blanket and then to the substrate. Many conventional offset inks are relatively viscous. During transfer, the ink film splits between contacting surfaces; after transfer, the deposited layer may level, penetrate the substrate, dry, or cure depending on the ink system.
In metallic offset printing, these steps may influence flake arrangement and the ultimate directional reflection. Flake size and shape must also match the ink formulation and transfer process. Not every metallic formulation suits every offset press or curing system.
Flexography: the anilox and plate control liquid-ink transfer
Flexographic ink metering depends strongly on the anilox and on transfer through the printing plate. With metallic pigments, flake dimensions must match the anilox-cell geometry and ensure stable ink release. Oversized or unsuitable particles can cause transfer variability or other production difficulties.
Ink viscosity, drying conditions, printed film thickness, substrate texture, and press speed can also affect the appearance. In some flexible-packaging applications, drying and film formation influence how long pigment flakes can reorient before the film becomes fixed. Thus, an anilox or drying change can alter metallic appearance even if a conventional single-angle color reading remains close to target.
LEP: a polymeric ink film formed before final transfer
In Liquid Electrophotography, pigment-containing polymer particles are dispersed in a carrier liquid. The image develops electrostatically and transfers to a heated intermediate blanket, where the particles coalesce into an ink film before final transfer to the substrate.
This differs from splitting a viscous offset ink film and from drying a liquid flexographic ink film directly on the substrate. Film formation and intermediate transfer may influence surface texture, leveling, and the optical appearance of the final image.
Publicly described specialty LEP formulations include metallic pigments with platelet-like aluminum particles. In documented examples, particles lying substantially parallel to the printed surface contribute to directional reflection and metallic appearance. These examples do not demonstrate that every commercial LEP ink, press, or print setting produces the same pigment orientation. The result remains formulation- and process-dependent; moreover, not all LEP configurations support specialty metallic ink.
For a realistic comparison, distinguish a LEP job using a qualified metallic ink from one that creates metallic appearance by printing conventional inks onto a metalized substrate.
7. Practical Comparison of the Three Printing Technologies
Property | Offset | Flexography | LEP |
|---|---|---|---|
Ink transfer | Plate → blanket → substrate | Anilox → plate → substrate | Electrostatic image → heated blanket → substrate |
Film formation | Splitting, leveling, and ink-specific drying or curing | Metered liquid transfer followed by drying or curing | Polymeric film formation before final transfer |
Metallic ink capability | With a suitable dedicated ink system | With a suitable dedicated ink system | Where the configuration supports qualified metallic ink |
Flake orientation | Depends on transfer, ink leveling, drying, and substrate | Depends also on anilox, transfer, and drying | Depends on formulation and intermediate-film formation |
Main gloss factors | Substrate, ink film, drying, coating | Substrate, metering, drying, coating | Substrate, transferred film, finishing |
Angle-dependent effects | Possible | Possible | Possible in appropriate constructions |
Universally best technology? | No | No | No |
No technology has a universal advantage in metallic appearance. Compare qualified ink/substrate/finishing constructions under the same defined measurement and viewing conditions.
8. Can CMYKOVG Replace a Metallic Ink?
A CMYKOVG ink set adds Orange, Violet, and Green to the conventional Cyan, Magenta, Yellow, and Black process colors. Its purpose is to extend the range of reproducible colors, particularly in selected highly saturated regions of the gamut.
However, ordinary CMYKOVG process inks do not automatically produce the directional reflection of metallic flakes. A yellow-gold hue may be closely matched to a metallic gold reference at one color-measurement geometry, but the reproduced patch will not necessarily exhibit the same appearance when rotated.
If the print construction lacks metallic flakes, a metalized layer, or an equivalent optical structure, a color profile cannot create that missing physical reflection mechanism. The issue isn't simply an inaccurate color recipe.
Can a metalized substrate help? Sometimes. Transparent or semitransparent process inks over a metallic surface can exploit the substrate's reflective layer to build colored metallic effects. The result still depends on transparency, ink-film thickness, surface smoothness, and the complete construction. It should not be assumed to reproduce the angular signature of metallic ink on white paper.
9. The Critical Role of White Ink Under Metallic Printing
In printing on metalized materials, an opaque white underprint can determine much of the finished appearance. It reduces the reflective substrate's contribution, making overprinted process colors behave more like colors on a conventional white surface.
Where the white underprint is intentionally omitted, the metallic substrate can contribute more strongly to the reflected light. Partial or lower-opacity white layers provide intermediate effects. Thus, the white separation is an appearance-control tool, not merely a background layer.
Consider two versions of the same package on metalized film. In version A, an opaque white layer lies underneath the red area. In version B, red is printed directly over the metallic film. Even if the versions approach the same color target at one measurement geometry, they can have very different directional reflections and perceived brilliance.
A change in white opacity or placement may therefore require a new appearance approval, not just an adjustment to CMYK or CMYKOVG percentages.
10. Varnish and Lamination Can Change the Approved Appearance
A print is often approved before finishing, only to look different after varnishing or lamination. That change does not automatically indicate a printing failure. An additional coating or film introduces new optical interfaces that light must travel through.
High-gloss varnish
A glossy overprint varnish can increase specular surface reflection. Depending on the construction, it can also affect a color's apparent depth and the balance between surface highlight and underlying pigment reflection.
Matte varnish
A matte varnish can increase light scattering through its surface microstructure or formulation. It may reduce glare and visibly soften a metallic effect. Increasing metallic ink laydown will not necessarily correct an effect that is being suppressed by the topcoat.
Soft-touch coatings
Soft-touch coatings can alter texture, directional reflection, and tactile feel. Their performance is not fully described by one gloss number; the surface microstructure and scattering distribution can be important.
Transparent lamination
Lamination adds a polymer film and adhesive interfaces to the optical path. Film gloss, haze, adhesive properties, interfacial smoothness, and texture may all influence the final visual response.
Approval before lamination is not sufficient proof of appearance after lamination. When the customer purchases a finished package, acceptance should be based on its finished construction.
11. Why a Single 45°/0° Color Measurement May Not Be Enough
Spectral measurement with a 45°/0° geometry is common and highly useful in graphic-arts color control. The illumination and detector are set in a defined geometry, providing reproducible evidence for conventional color comparisons.
Yet this single geometry cannot fully characterize every appearance change when the package is tilted. Metallic or pearlescent samples may reflect very different amounts and spectra of light at other angles.
What about d/8° sphere geometry?
Integrating-sphere instruments using d/8° geometry can measure color under different reflection conditions; some let you include or exclude the specular component. Such measurements are valuable, but they are not equivalent to collecting a complete angular response for an effect pigment.
What about M0, M1, and M2?
These are measurement illumination conditions defined for graphic arts, including differences related to ultraviolet content and the behavior of fluorescent materials such as optical brightening agents. M1 does not mean multiangle. Illumination condition and viewing geometry answer different questions, and neither substitutes for the other.
12. How Multiangle Measurement Works
Multiangle instruments examine a surface's spectral or colorimetric behavior at multiple defined geometries. Some instruments illuminate at a fixed angle while measuring at several detector angles; other designs use different illumination geometries.
A useful concept is the aspecular angle: an observation angle defined relative to the specular reflection direction. A measurement close to that direction may capture a very bright metallic response; a measurement farther away may capture a darker response.
Some instrument configurations use aspecular positions such as 15°, 45°, and 110°. These are examples—not universal mandatory settings. The instrument geometry and angular set must correspond to the material, the applicable standard, and the inspection task.
Spectral reflectance and derived color coordinates can be compared at each geometry. A package may meet its approved standard at one specular angle but diverge at another.
Measurement position | Approved reference | Production sample | Possible interpretation |
|---|---|---|---|
Near specular reflection | Very bright | Noticeably darker | Difference in strength of directional reflection |
Intermediate angle | Target hue | Similar hue | Good agreement at this geometry |
Far from specular | Darker tone | Different hue or lightness | Difference in angular color response |
This table illustrates the logic of the comparison, not actual experimental readings. It shows why one measurement cannot always represent a customer's experience when handling a package.
13. Gloss Measurement Is Not a Substitute for Multiangle Color Measurement
Gloss measurement focuses on light returned in a defined specular direction. Common industrial coating geometries include 20°, 60°, and 85°, selected according to method and surface-gloss range.
Multiangle color measurement instead examines variation in colorimetric or spectral response across defined viewing geometries. Two samples can have similar gloss values and different color flop. Conversely, they may show similar color trends across several viewing positions while differing visibly in gloss or microtexture.
The methods complement each other. For specialty packaging, you may need to specify both gloss and multiangle color acceptance criteria, along with visual inspection of the finished package.
14. What Do the Relevant Standards Cover?
The test method must fit the construction being evaluated. Metallic-flake and interference-flake materials do not necessarily need the same measurement protocol.
ASTM E2194 — metallic-flake pigmented materials
This standard covers multiangle color measurement of materials containing metal-flake pigments. It supports controlled characterization at specified geometries. A colorimetric match at multiple positions does not automatically guarantee complete appearance equivalence when surface texture or gloss differs.
ASTM E2539 — interference-flake pigmented materials
This method addresses multiangle color measurement of materials incorporating interference-flake pigments, including relevant pearlescent constructions. Their response depends on the pigments and on the medium and film construction in which the flakes are dispersed.
ISO 2813 — specular gloss
This standard describes gloss determination at defined geometries, notably 20°, 60°, and 85°, for appropriate coating surfaces. It does not replace angular color characterization.
ISO 3664 — viewing conditions
This standard defines controlled conditions for visually evaluating graphic-arts and photographic images. The 2025 edition supports consistent inspection. Standard viewing conditions do not remove the need for additional measurements when a material itself has an angle-dependent effect.
ISO 13655 — spectral measurement and colorimetry
This standard establishes spectral measurement and colorimetric computation practices for graphic-arts images. Compliance with ordinary spectral measurement requirements does not mean every spectrophotometer can characterize the full angular appearance of metallic or pearlescent products.
For production specifications, always verify the applicable edition, scope, test geometry, and customer requirement rather than relying on a standard number alone.
15. Distinguishing Metamerism from Angle-Dependent Appearance
A customer may say the same color looks different, but several mechanisms can cause it.
Metamerism occurs when two samples with different spectral reflectance functions match under one illuminant but not under another. The lighting spectrum is the decisive variable.
Angle-dependent appearance occurs when differences emerge as the illumination or observation geometry changes, even with the same illuminant. The mechanism may involve directional reflection, surface texture, metallic flakes, or interference effects.
To investigate, first keep the observation geometry fixed while changing between controlled light sources. Then keep the light source fixed while varying the viewing angle in a controlled way. If the difference tracks illuminant spectrum, investigate metamerism. If it tracks viewing geometry, investigate angular appearance. Both effects can coexist, and gloss, haze, transparency, and texture must also be considered before assigning a diagnosis.
16. Troubleshooting: Color Passes, but the customer Rejects the Appearance
Case A — A metallic package looks darker after moving between print technologies
A metallic-ink offset package is reproduced using another print construction, possibly conventional inks over metalized film. Single-angle color readings are close, but the customer sees a difference after tilting the samples.
First action: establish whether the source of the metallic effect is inside the ink or underneath it. If those constructions differ, the angular response may differ even in the absence of a color-management error. Compare the final constructions using multiangle measurements and determine the feasible degree of appearance match.
Case B — Metallic brilliance decreases after varnishing.
The printed surface passes inspection before coating but looks duller afterward. Preserve matched samples from before and after varnishing. Test whether the overcoat changes surface reflection, scattering, or microtexture. A matte varnish may naturally reduce brilliance; increasing metallic ink volume is not an automatic remedy. Evaluate a finish compatible with the approved appearance.
Case C — The same metallic ink appears different on two substrates
A metallic formulation may look one way on smooth coated paper and another on rough stock. Compare substrate texture, ink laydown, film leveling, and process conditions. If the effect depends on flake orientation or film formation, the solution may require a new substrate or ink/process qualification—not simply a color-profile correction.
Case D — CMYKOVG gold matches the color but not the metallic reference
The digital separation reproduces the target's color coordinates at one geometry, yet the result lacks metallic brilliance. The missing property may be the physical reflection mechanism. Explain that matching a hue is different from matching the effect. A qualified metallic ink, metalized substrate, or different construction may be needed.
Case E — Appearance changes only after lamination
The unlaminated print matches the approved sample, but the laminated pack does not. Examine the film, adhesive, gloss, haze, and optical interfaces. Measure the finished construction against a finished reference; a bare printed sample is not the appropriate approval target for a laminated product.
17. Troubleshooting Reference Table
Symptom | Possible source | First diagnostic check | Corrective direction |
|---|---|---|---|
ΔE00 passes, but appearance differs | Gloss or angular response | Gloss and multiangle measurement | Identify source before editing color |
Gold appears flat | Missing metallic reflection mechanism | Ink/substrate structure | Reconsider print construction |
Metallic hue darkens at one angle. | Different flake orientation or film structure | Multiangle reading | Investigate formulation and process |
Metallic appearance varies along web. | Transfer, drying, or substrate drift | Samples across the run | Stabilize process conditions |
Appearance changes after varnish | Modified light reflection/scattering | Before/after coating test | Qualify an appropriate varnish |
Appearance changes after lamination | Film or adhesive changes optical path | Measure finished laminate | Adjust finishing materials |
CMYKOVG differs from metallic ink | Different optical mechanisms | Appearance comparison | Select suitable effect technology |
Samples diverge under LED light only. | Potential spectral mismatch | Controlled illuminant comparison | Investigate metamerism |
Differences appear mainly on rotation. | Directional reflection or texture | Controlled angle comparison | Define appearance tolerances |
Change follows substrate replacement. | Roughness, opacity, or gloss | Compare unprinted and printed substrates | Requalify the construction |
18. Establishing Acceptance Criteria for an Effect Package
For conventional printed materials, color tolerances can often be based on ΔE00 measured under agreed conditions. For angle-dependent products, approval may require more than one metric: selected multiangle color differences, gloss, visual appearance, and consistency across production.
There is no single universal ΔE00 value that certifies appearance across every angle and every effect pigment. Tolerances should be based on the product requirement, the measurement method, observed production capability, and the differences the customer can perceive.
Begin with a reference sample of the approved finished construction, including its varnish or lamination. Specify the illumination and measurement geometry, the sample orientation, and the viewing positions relevant to handling or retail presentation. For optically directional substrates, maintain a consistent measurement direction relative to printing or web travel.
Finally, establish which deviations are unacceptable and how conflicts between numerical and visual results will be resolved. A useful acceptance criterion describes the appearance of the article the customer will actually receive—not merely a number from one instrument.
19. A Practical Production Qualification Procedure
For a new job containing metallic ink, pearlescent pigment, or strongly directional substrate reflection, use a controlled workflow:
- Define the complete structure. Document substrate, ink set, white underprint, coatings, adhesives, and lamination.
- Establish a finished reference. Approve an actual representative construction rather than an unfinished proof alone.
- Select appropriate instruments. Determine whether ordinary spectral color, gloss, multiangle readings, or a combination is required.
- Run a representative production trial. Include all visually important effect regions and realistic processing conditions.
- Measure and view consistently. Compare with the reference under specified illumination and observation geometries.
- Assess after finishing. Recheck once varnish or lamination has been applied, when those processes are part of the deliverable.
- Freeze the approved conditions. Retain sample, process settings, substrate and ink specifications, instrument geometry, and tolerances.
Any change to substrate, ink, coating, or lamination structure should trigger a documented evaluation of its effect on appearance. Do not assume an approval remains valid merely because the single-angle color measurement still passes.
20. The Engineering Lesson: Matching Color Is Not Always Matching a Surface
The distinction between color and appearance becomes critical when a design moves between printing technologies. Offset, flexography, and LEP form and transfer ink films differently. For ordinary process colors, qualified profiling and calibration can deliver close color agreement when substrates and viewing conditions are properly controlled.
However, when an effect pigment, metalized layer, or specialty finish becomes part of the optical construction, colorimetric agreement may not be enough. Appearance can differ even when the press is running correctly.
Sometimes the challenge is not reproducing the same color, but reproducing the same angular optical behavior. The project must therefore define whether acceptance means a match at one geometry, a close overall visual match, or a specified reproduction of the effect as the package moves. These are different requirements, and not every ink/substrate system can satisfy all of them.
Conclusion — Color Is Only Part of What the Customer Sees
Color measurement is central to printing quality control, but it cannot by itself characterize every visual property of a finished package. Metallic inks, pearlescent pigments, metalized substrates, and specialty finishes may produce appearances that change with illumination and viewing angles.
Offset, flexography, and LEP can all produce effect printing when suitable materials and equipment are available. Their ink-transfer and film-formation mechanisms differ, so their optical results may differ as well. No one technology has a universal advantage: the final construction and intended effect determine what should be compared.
Likewise, the extended gamut of CMYKOVG does not automatically replace a metallic or pearlescent mechanism. And a low ΔE00 at one measurement geometry does not prove a complete appearance match.
When two packages measure alike but look different as they rotate, don't start by changing the color profile or ink quantity. First identify the optical mechanism responsible for the difference.
The instrument tells us what the color is under defined conditions. Surface engineering determines how that color will look in the real world.
Glossary
Term | Meaning |
|---|---|
Appearance | The complete visual character of a surface, including color, gloss, texture, and angular response |
Multiangle Color Measurement | Measurement at more than one defined illumination/observation geometry |
Color Flop | Change in apparent color or lightness as viewing geometry changes |
Specular Reflection | Directional reflection of light |
Diffuse Reflection | Light reflected or scattered over many directions. |
Aspecular Angle | A measurement angle expressed relative to the specular-reflection direction. |
Metallic Pigment | Pigment containing metal flakes that reflect light directionally |
Pearlescent Pigment | Effect pigment that produces a pearl-like appearance, often through layered optical structures |
Interference Pigment | Pigment whose optical interference contributes to its color/effect |
Flake Orientation | Alignment of platelet-like pigment particles within a film |
Gloss | Specular-reflection property evaluated under a defined geometry |
Haze | Scattered light near the specular direction or in transmission, depending on the method |
LEP | Liquid Electrophotography |
CMYKOVG | Cyan, Magenta, Yellow, Black, Orange, Violet, Green |
ΔE00 | Color-difference measure calculated using the CIEDE2000 formula. |
Metamerism | Agreement under one illuminant and disagreement under another due to differing spectra |
Spectrophotometer | Instrument that measures the spectral response of a material |
Functional Appearance | The appearance an article must exhibit under its intended viewing and use conditions. |
Technical References
- ASTM E2194-14(2025), Standard Test Method for Multiangle Color Measurement of Metal Flake Pigmented Materials. https://store.astm.org/e2194-14r25.html
- ASTM E2539-25, Standard Test Method for Multiangle Color Measurement of Interference Flake Pigmented Materials. https://store.astm.org/standards/e2539
- ISO 2813:2014, Paints and Varnishes — Determination of Gloss Value at 20°, 60° and 85°. https://www.iso.org/standard/56807.html
- ISO 3664:2025, Graphic Technology and Photography — Viewing Conditions. https://www.iso.org/standard/83759.html
- ISO 13655, Graphic Technology — Spectral Measurement and Colorimetric Computation for Graphic Arts Images.
- Influence of Pearlescent Pigments on Light-Fastness of Water-Based Flexographic Inks. https://www.sciencedirect.com/science/article/pii/S0143720816311202
- US9335649B2, Making a Liquid Electrophotographic Paste (public patent documentation). https://patents.google.com/patent/US9335649B2/en
- Comparative Studies of Gloss Development in Electrophotography and Offset Printing. https://doi.org/10.2352/J.ImagingSci.Technol.(2008)52:1(010504)
- Influence of Printing Surface Attributes on Print Quality in Electrophotography. https://hrcak.srce.hr/83903
Engineering note. This article explains general industrial principles and inspection methods. The troubleshooting cases are illustrative scenarios, not results from a controlled three-technology experiment. Production settings and acceptance limits must be validated for the actual equipment, materials, construction, and applicable standards.