By Ronen Dolev | 2026
The failure that is not visible at the printing press
One of the most difficult situations in industrial printing occurs when a job looks entirely acceptable as it leaves the printing press but fails at the next manufacturing stage. Color is on target, registration is controlled, the image is visually uniform, and nothing obvious suggests that the printed product will not survive converting. Hours later, however, the ink begins to scuff in a cutting machine, a printed area lifts during an adhesion test, a varnish fails to remain bonded, or a laminated construction separates under heat and stress.
A common response is to search immediately for a stronger primer, a heavier coating, a higher transfer temperature, or a tougher protective varnish. Sometimes one of these changes helps. But an improvement following an adjustment does not, by itself, identify the cause of failure. It may simply shift the failure from one interface to another or hide a weakness that reappears during a longer production run.
Liquid electrophotography (LEP) makes this distinction particularly important. Its transferred polymeric ink film interacts with the substrate surface, a possible primer layer, and every coating or adhesive applied afterward. The decisive question is not which setting can be raised. It is which material or interface actually failed, why it failed under the imposed load, and what controlled evidence would demonstrate that the proposed correction is durable.
A successful troubleshooting process begins with the failure mechanism, not an assumption about the component to blame.
The LEP ink film and the meaning of adhesion
In LEP printing, a digitally formed image is transferred using charged pigment-bearing polymer particles and a thermally assisted intermediate-transfer process. The resulting ink layer behaves principally as a polymeric film at the substrate surface. Its interaction with the substrate differs from that of a liquid ink system that relies heavily on penetration into the porous fiber network before drying.
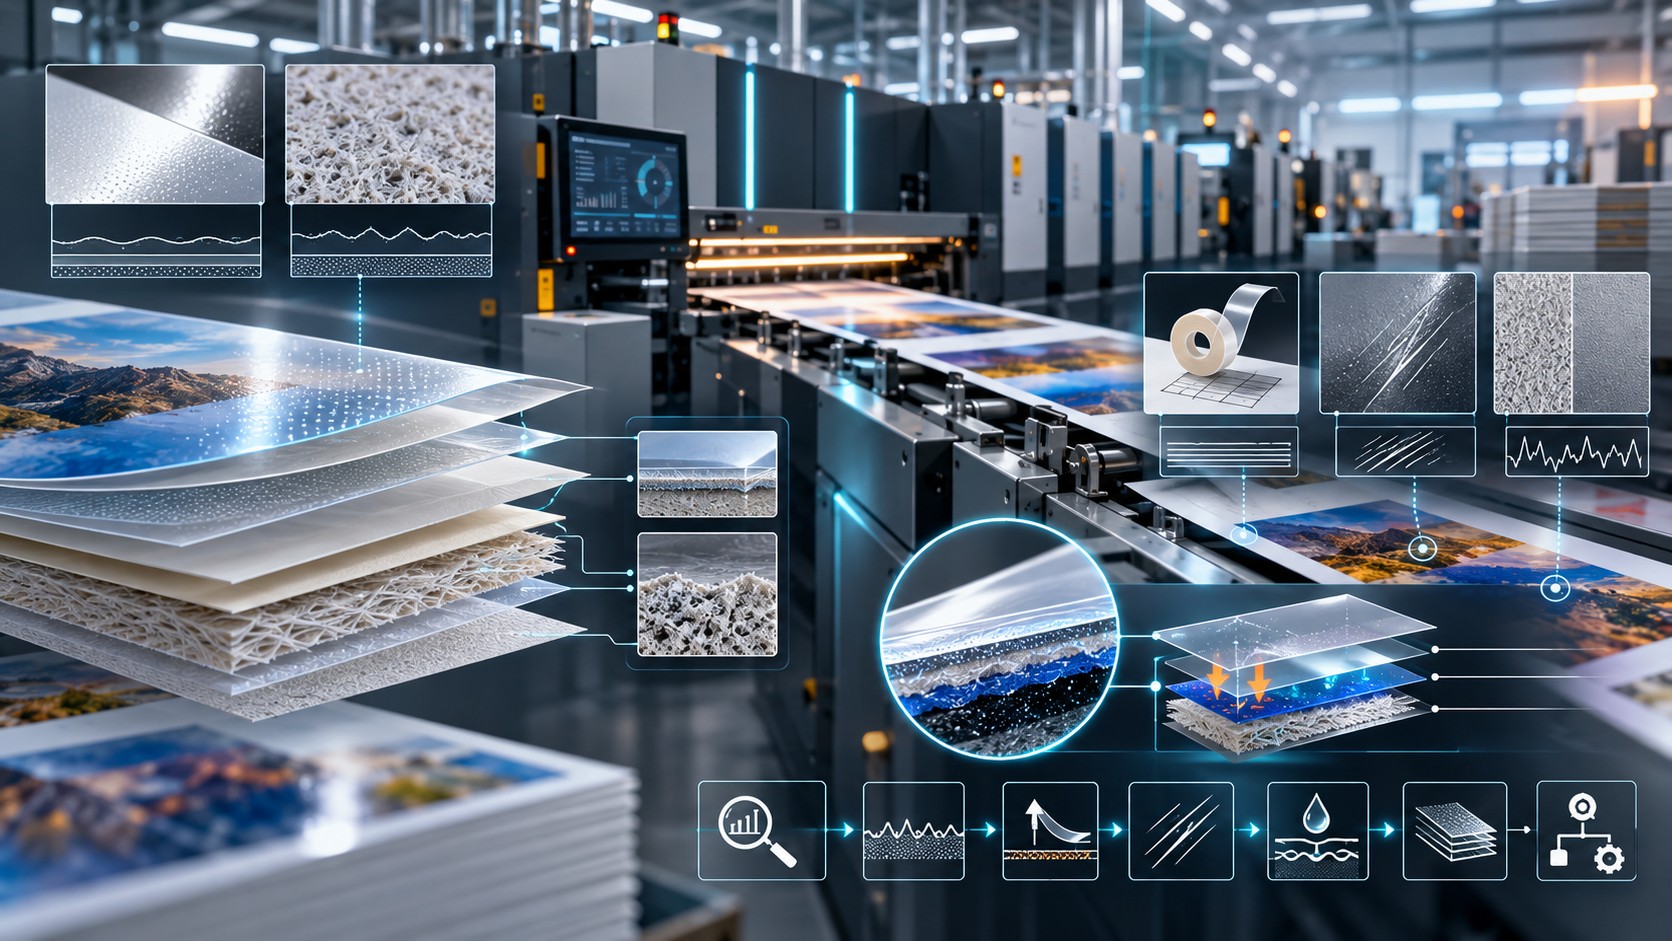
The finished construction may contain several distinct interfaces: substrate to surface coating, substrate to primer, primer to ink, ink to protective overprint varnish, ink to laminating adhesive, and adhesive to lamination film. Each interface has its own chemistry and strength. A product may therefore fail even when the ink is cohesive, and the printing press transfers the image correctly.
Two terms must remain separate. Adhesion refers to the bonding between different materials at an interface. Cohesion refers to the internal strength of one layer or material. When ink releases cleanly from a primer, an adhesive interface may be weak. When a paper coating splits within itself, or paperboard plies separate, the limiting property is within the substrate rather than necessarily within the ink.
A heavier primer cannot be assumed to repair a paper coating with insufficient internal strength. Indeed, if a better ink-to-primer bond increases the force transmitted to a weak coating, the visible failure may migrate deeper into the paper. That is why every adhesion or peel test should record not only the force or pass/fail result but also the location and appearance of the fracture.
Identify the exact failure plane before changing anything.
Suppose an adhesive tape removes an area of printed color. The observation is real, but "poor ink adhesion" is not yet a diagnosis. Examine the removed material and compare it with the area remaining on the sheet. Is the primer still on the substrate? Did it leave together with the ink? Does a chalky pigment layer remain? Are fragments of coating or paper fibers attached to the removed film?
The answers determine where the next test should be directed. A clean separation between ink and primer suggests a different mechanism from a separation between primer and paper. Fiber tear may indicate that a bonded interface exceeded the local strength of the fibrous material; it does not prove that the complete printed construction is suitable for every downstream process.
Observed result | Possible failure plane | First diagnostic direction |
|---|---|---|
Ink lifts while the primer remains | Ink–primer interface | Verify primer compatibility, ink-transfer conditions, and dwell time before testing. |
Ink and primer lift as a single layer | Primer–substrate interface | Investigate substrate chemistry, surface preparation, and primer anchorage |
Pigmented paper coating lifts | Inside the coated-paper layer or at its base-paper interface | Measure coating strength and inspect the paper grade |
Paper fibers tear and remain with the removed material | Cohesive failure in the fiber network | Evaluate whether fiber strength meets the application load |
Only varnish lifts | Varnish–ink interface | Examine wetting, varnish chemistry, drying and cure |
Laminating film removes ink or paper coating | One of several interfaces beneath the film | Map the fracture under magnification and compare peel specimens |
The failure surface is evidence. Photograph, describe, and retain it alongside the specimen. A single tape test without fracture analysis provides far less information than a controlled test with a clear map of what separated from what.
Paper grades are not interchangeable printing surfaces
A common diagnostic mistake is to treat paper as a uniform, passive carrier. A sheet described as "suitable for premium printing" may be excellent for one ink-transfer mechanism and troublesome for another. Basis weight, whiteness, smooth appearance and nominal finish do not fully define the material's surface chemistry or mechanical behavior.
Different grades contain different fibers, fillers, surface-sizing systems, pigments, binders and functional additives. Their surfaces may vary in roughness, porosity, absorbency, coating cohesion and dimensional response to heat and moisture. Two stocks with identical grammage can therefore produce significantly different LEP transfer, adhesion, or converting performance.
The diagnostic implication is straightforward: whenever a problem is associated with a specific stock, compare it with a well-performing reference substrate under controlled conditions before modifying multiple press settings. If the same print and coating system works reliably on one grade and consistently fails on another, investigating the paper itself becomes a high-priority path.
Uncoated paper: topography, fibers and absorption
Uncoated paper often exposes more of its fibrous structure than a heavily pigment-coated sheet. Its microscopic surface contains peaks, valleys, pores, exposed fibers, fillers, and different degrees of surface sizing. These attributes may influence how completely the polymeric LEP ink film contacts the material during transfer.
On a relatively rough grade, intimate contact may be easier at the surface peaks than within the depressions. Transfer defects or locally weak anchorage can occur when the system operates near its contact and transfer limits. Loose fibers, dust, or an insufficiently consolidated surface can add a second mechanism: the ink may adhere to a weak surface component that subsequently detaches.
Water-based priming creates another consideration. Part of the liquid primer may penetrate a porous stock rather than remain at the outer surface where it is needed. The wet coating applied is therefore not necessarily equivalent to a continuous, accessible dry primer film. An apparent response to a higher coat weight might reflect improved surface coverage, but it might also introduce excessive moisture, curl, dimensional change, or drying problems.
Uncoated offset, bond, kraft, and recycled papers should not be grouped together as though they behaved identically. Their preparation and fiber characteristics differ. A more effective response may involve a different grade or surface sizing, an adjusted priming method, or a verified coating window rather than simply applying more primer.
Coated paper: a smooth surface can hide a weak structure
Coated paper typically has a pigment-rich surface layer held together by binders and other additives. That layer can create the uniform, smooth, visually attractive surface required for high-quality graphics. But it is also an independent mechanical and chemical structure, with properties that must be distinguished from those of the underlying fiber sheet.
The surface may be smooth and glossy yet possess insufficient coating-to-base-sheet bond or weak internal cohesion. Certain binder distributions may produce local differences in wetting or strength without obvious visual evidence. During drying of a paper coating, binder movement or redistribution can contribute to such variability, depending on the formulation and manufacturing conditions. Binder migration is a possible mechanism to investigate, not an automatic explanation for every adhesion defect.
A strong primer-to-ink bond may transfer conversion stresses through the pigment coating. If the coating is the weakest part of the structure, the coating can split or release despite acceptable image quality and apparently good ink anchorage. This is especially important for folding cartons and printed papers later subjected to lamination, scoring, folding or heated processing.
Surface smoothness and surface strength are different properties. An attractive gloss value cannot substitute for testing the integrity of the layer supporting the printed image.
Gloss, silk, satin and matte: appearance is not a performance specification
Finishing terms describe broad visual or tactile characteristics, not guaranteed values for coating cohesion or compatibility with LEP. A high-gloss grade may be smooth but chemically difficult for a particular primer. A matte grade may have topography that complicates uniform transfer. A satin or silk sheet may contain a coating structure that behaves differently under heat, peel, or rub tests than a superficially similar stock.
The terms also do not specify a universal roughness hierarchy. Manufacturing methods, binder systems, calendering, porosity, and additives vary. Consequently, the question is not whether gloss is better than matte. It is whether the selected commercial grade presents the properties needed for this LEP mode and the complete finishing workflow.
Paper or board family | Potential constraint | Useful investigative test |
|---|---|---|
Uncoated offset paper | Roughness, absorbency or fiber picking | Print-surface roughness, surface strength and transfer comparison |
Coated gloss paper | Weak coating cohesion or unfavorable surface chemistry | Failure-plane inspection and coating-strength tests |
Silk or satin coated paper | Variability in coating structure or contact | Comparative transfer and adhesion evaluation |
Matte coated paper | Topography, porosity or coating chemistry | Roughness, wetting behavior and fracture analysis |
Recycled grades | Variation in fibers, fillers and surface contamination | Incoming-lot comparison and surface-strength sampling |
Folding boxboard and multilayer board | Weak interfaces inside the board and fold-related strain | Internal bond, folding and post-converting adhesion |
Barrier-coated paper | Functional surface chemistry incompatible with primer or ink | Specific chemical compatibility and interface testing |
This table identifies candidate mechanisms. It does not claim that every paper within a category suffers from the associated difficulty.
Paperboard: the weakest interface may be inside the sheet
Folding carton boards often contain multiple fibrous layers, sometimes topped by a pigment coating. They are engineered for stiffness, conversion, printability, and cost rather than for a single universal interface strength. The complete construction must withstand localized stress during creasing, folding, die-cutting, and sometimes adhesive bonding or lamination.
A tape or peel test may remove the printed image together with part of the board coating. At first glance, the result resembles ink failure. Inspection may instead show that the ink remains attached to primer and coating while the coating separates from the underlying fibrous layer. Increasing the ink bond may not help because the limiting strength resides below it.
Tests of surface pick resistance, through-thickness cohesion, and internal bond can help separate these mechanisms. Interpret their results against the product's actual loads, not as isolated numbers. A board could be adequate for printing alone but inadequate for construction exposed to significant heat, bending, or peel stresses.
Roughness and the real contact area during transfer
At the microscopic scale, two apparently flat surfaces contact each other at discrete regions determined by pressure, temperature, material compliance, and surface topography. When paper roughness is high, the actual contact area with a transferred polymeric ink layer can be lower than its nominal surface area.
This may result in incomplete transfer, inconsistent image density, or weak adhesion concentrated in particular regions. Press settings can sometimes change the available transfer window, but physical limits constrain how much a process can compensate for the substrate's topography.
A structured test should compare the problematic grade with a known-good reference under the same image, environmental conditions, and appropriate supported transfer settings. Surface characterization then helps explain any performance difference. If the evidence consistently points to a paper property outside process capability, a different grade may be a more reliable engineering correction than repeated press changes.
Characterizing paper without confusing one test with another
Several measurements are useful when evaluating paper and paperboard surfaces, but each addresses a different material property. Print-surface roughness characterizes aspects of surface topography. The Cobb Test (ISO 535) measures how much water paper or paperboard absorbs over a defined period under standardized conditions. The result is expressed in grams per square meter (g/m²). A higher Cobb value indicates greater water absorption, while a lower value indicates higher resistance to water penetration. This measurement helps assess the substrate's water absorptiveness, which may influence the application and distribution of water-based primers.
Surface pick resistance evaluates a paper surface's tendency to release fibers or coating particles under specified mechanical stresses. Internal bond measurements assess the strength of the material within the paper or paperboard structure. However, none of these tests independently determines the adhesion performance of an LEP ink system.
For example, a Cobb result does not reveal exactly how much functional primer remains on the surface after application and drying, because primer behavior also depends on its chemistry, solids content, viscosity, and interaction with the substrate. Similarly, surface roughness alone cannot establish chemical compatibility between a paper coating and a primer. A substrate may meet its roughness specification yet still fail because the coating lacks sufficient internal cohesion.
A reliable diagnosis therefore combines substrate characterization with direct application testing, including ink transfer quality, primer coverage and uniformity, ink adhesion, mechanical durability, and performance throughout the final converting process.
The objective is not simply to identify a material property outside specification, but to establish how that property contributes to the observed failure mechanism.
Is primer always mandatory in LEP printing?
This question requires a qualified answer, not a universal rule. Primers can be essential for both complete transfer and adequate adhesion in many LEP applications. This is particularly important for synthetic substrates and for specific transfer modes that require a primed or otherwise qualified surface.
Nevertheless, some optimized commercial papers can deliver adequate results without additional priming in supported Multi-Shot configurations. That exception is not a blanket approval for every paper grade, ink sequence, or finishing application. Certain lower-performing stocks, including some silk or coated grades, may still require primer. In the relevant One-Shot workflows, primer is part of the mandatory substrate preparation approach.
The apparent tension between broad primer requirements and qualified no-primer exceptions is resolved by distinguishing a general durability and transfer recommendation from specific substrate-and-process conditions. A statement that primer is necessary for a validated configuration must be respected within that configuration. It should not be converted into an unqualified claim that every LEP job on every commercial paper requires the same treatment, nor into a claim that printing without primer is universally safe.
A further distinction is essential: an unprimed paper that performs acceptably immediately after printing may not withstand varnishing, lamination, cutting or folding. Product qualification must therefore be performed end to end.
The acceptance criterion is the durability of the finished application, not the first visually acceptable printed sheet.
One-Shot and Multi-Shot: what changes mechanically?
In a Multi-Shot configuration, color separations are transferred to the substrate in distinct passes. In a One-Shot configuration, several color layers are assembled on the intermediate transfer surface before being delivered to the substrate together. The methods differ in how the ink structure is formed and how the substrate experiences transfer.
Certain supported Multi-Shot workflows can achieve good results on optimized commercial paper without primer. One-Shot workflows may offer advantages in registration and dimensional stability, but on the relevant systems they rely on suitable priming. These are application-specific process capabilities, not a universal quality ranking.
Switching modes simply to stop scratches is not a complete troubleshooting plan. It changes the ink sequence and the structure of the transferred image and may require color recalibration and new adhesion testing. Any comparison must use the same paper batch, equivalent image elements, a representative coating process, and a defined final-use test.
The K-First strategy: changing the exposed ink structure
When printed surfaces show scuff marks or scratches, color-layer order may be a useful diagnostic variable on supported Multi-Shot configurations. A K-First and Y-on-top strategy moves the black separation earlier in the transfer order. Where multiple process colors overlap, the resulting arrangement can change which materials are most exposed to abrasion.
However, not every black area gains protection from another color; a solid black-only object remains different from a multilayer black build. The effect also depends on artwork and ink-film structure. The appropriate conclusion is therefore not that K-First always eliminates scratches, but that a controlled ink-sequence trial may reveal a meaningful durability difference.
When the strategy changes, color matching must be revisited, and a new calibration or color setup may be needed. Assess mechanical performance on the completed graphic, not solely infer it from the layer sequence.
Priming is also about transfer uniformity.
A primer provides a functional interface between substrate and ink. Depending on the system, it can improve transfer completeness, reduce variability, and enhance adhesion. A print defect that resembles poor ink laydown may therefore be connected to primer continuity, drying, or local substrate conditions.
The challenge is especially clear when comparing rough and smooth paper. The same nominal application rate can yield different dry-film continuity because of surface area, absorbency, and coating distribution. On an absorbent stock, part of the primer may be drawn below the top surface. On a heavily coated stock, the primer may remain near the surface but face a wetting or compatibility problem.
Primer coat weight should consequently be optimized to the specific paper grade and coating method. The goal is a stable functional film, not the highest possible wet application amount.
Primer presence is not primer coat weight.
A chemical indicator suited to the particular primer family may reveal whether primer is present and help identify uneven coverage. That does not mean the same indicator quantitatively measures dry coat weight or proves printability. Interpreting color change as a complete quality test can therefore produce false confidence.
When a primer issue is suspected, examine its identity, surface coverage, applied amount, solids content, drying, and adhesion to the base surface. If necessary, compare several controlled coat weights and inspect the results after printing and finishing. The test should also record curl, blocking, or other undesirable changes introduced by increased moisture or coating.
Indicator tests are useful screening tools. They do not replace mass-balance measurements, coating process verification, or end-product adhesion testing.
Priming uncoated stock: an absorption problem
On a highly absorbent uncoated sheet, the aqueous phase of a primer can penetrate into the paper network before a uniform functional layer develops at the surface. This is not a universal failure: controlled penetration may be compatible with a validated process. The problem occurs when the surface is left with insufficient or uneven primer for the LEP ink transfer and adhesion requirements.
A trial should distinguish applied wet weight, measured dry weight, and the resulting film's actual continuity. Consider absorbency, solids level, application method and drying conditions together. A second primer pass should not be introduced automatically. It may increase coverage on one stock but create excess moisture, dimensional instability or blocking on another.
Sometimes the more reliable intervention is to switch to a paper with better-suited surface sizing or a more stable surface structure. That decision should follow a comparison between an approved reference and the problematic grade, with all downstream durability tests repeated.
Priming coated paper: wetting and surface chemistry
Coated paper presents a different challenge. An aqueous primer may remain largely at the surface, yet still wet it poorly or form an inadequate bond because of the particular coating chemistry. Binder type, additives, and manufacturing variations can affect the interface without producing a clear visual sign on the unprinted stock.
Applying a heavier layer is not automatically beneficial. If the coating chemistry is incompatible, more of the same primer may simply create a thicker weak interface. A comparative trial with an appropriate alternative primer family, paired with an approved substrate grade, can help determine whether the limitation is chemical or mechanical.
Coating strength must be checked in parallel. A primer that bonds perfectly to a friable pigment coating does not turn that coating into a mechanically strong foundation. Where separation occurs within the paper coating, changing the paper grade or its performance specification may be more effective than adjusting the LEP engine.
Corona treatment belongs to a specific material mechanism.
Corona discharge treatment is commonly used to improve the wetting characteristics of certain polymer films. For synthetic materials such as polypropylene, polyethylene, polyester, and polyvinyl chloride, a compatible surface-treatment process may be appropriate before priming. Storage, surface contamination, migrating additives, and aging can reduce the effectiveness of an earlier treatment, making a refresher treatment useful in some applications.
Paper and paperboard are not equivalent to untreated polymer film. Their porosity, fiber structure, and pigment coatings create different mechanisms. Routine corona treatment should not be presented as a universal preparation step for paperboard before primer. On a problematic paper grade, investigate coating chemistry, surface strength, absorbency and primer compatibility first.
A separate question arises after LEP printing. Some overprint-varnish systems benefit from a controlled surface treatment of the printed ink film. Do not confuse that operation with corona treatment of raw synthetic film. It requires its own compatibility and durability validation.
Why dyne measurements do not solve every adhesion problem
Wetting-tension measurements are useful screening tools for many polymeric films, but a suitable result does not, by itself, establish strong ink adhesion. A contaminant layer or incompatible primer can defeat an apparently satisfactory surface-energy reading.
On porous paper, test-liquid penetration and surface texture make a simple dyne-pen interpretation particularly problematic. Values developed for polymer films must not be transplanted directly as mandatory thresholds for coated or uncoated papers. Paper characterization should instead emphasize the mechanisms that the available methods can genuinely measure, and then verify actual ink and finishing behavior.
The strongest approach combines physical measurements, chemical compatibility checks, and real product tests. No single dyne number, roughness value, or adhesive tape result can certify the complete LEP construction.
Primer viscosity: why a stable start-up may deteriorate during the shift
Aqueous priming systems are dynamic process liquids. Repeated circulation, evaporation, temperature changes, and contamination can alter their viscosity or concentration. That can change transfer through the coating rollers and the delivered coat weight, even when the operator has not deliberately changed a setting.
A sound troubleshooting routine records viscosity with a defined cup or viscometer, at a stated temperature, using the same method throughout the shift. Solids content, coating appearance, and storage conditions may also need monitoring. A change in the measurement should trigger a check of concentration, circulation, and cleanliness rather than an unmeasured attempt to restore flow by adding liquid.
If dilution is approved for a specific primer formulation, it should follow that formulation's validated process window. Values specified for one chemistry cannot be assumed to apply to another. The same applies to shelf life after priming: different chemistries may remain effective for very different periods, and storage conditions can matter as much as elapsed time.
Primer replacement and cleaning: the chemistry of residues
Replacing one primer with another can introduce a new failure mechanism. Even after a tank is drained, old material may remain in hoses, pumps, rollers, containers or coating-unit recesses. A new primer with substantially different chemistry may interact unfavorably with those residues and cause deposits, flocculation, abnormal viscosity, foaming, roller contamination or an uneven film.
Cleaning must therefore be treated as part of change control, not merely housekeeping. The appropriate procedure depends on both the formulations and the machine's materials of construction. One chemistry may tolerate a cleaning agent that destabilizes another. Acidic or alkaline cleaners must never be selected by analogy without checking their compatibility and the equipment's approved maintenance process.
When print defects begin immediately after a primer change, the investigation should include cleaning records, tank condition, roller condition, residual material, and measured primer properties. Changing transfer settings alone may obscure the actual cause.
Scuffing and scratching are not the same as poor adhesion
Scuffing usually refers to surface damage created by friction and repeated contact. Scratching often involves a more localized, concentrated contact with an abrasive or hard feature. Both may damage a properly anchored ink film. Neither automatically proves that the ink-to-substrate bond is defective.
The first question is where and when the mark appears. If the printed sheet passes an appropriate adhesion test but scratches at a recurring position in a cutting or folding machine, inspecting guides, rollers, belts, and contact points may be more productive than changing the primer. If damage appears over broad printed regions during stack handling, ink-film construction and surface durability become more likely variables.
Total ink coverage and multilayer builds also influence the mechanical behavior of printed areas. High-coverage regions deserve targeted examination, but a universal numerical cutoff should not be asserted for all LEP products without reference to the platform and job specification.
The right response to high ink coverage
A dense CMYK build can have a different thickness and deformation behavior from a single-color patch. This matters when the product later experiences folding, rubbing, heated pressure, or lamination. However, a high ink percentage alone is not proof of causation.
A useful experiment compares the original artwork with a color-managed alternative using a reduced total ink build, while preserving the intended appearance as closely as possible. Produce the samples on the same substrate batch and expose them to identical finishing stresses. If abrasion or cracking improves consistently, ink construction is a plausible contributor.
A protective varnish may help with scuffing, but it cannot be expected to repair a weak adhesion interface below the ink. A strong varnish over poorly attached ink can simply detach with the ink in one coherent sheet.
Overprint varnish: another bond, another failure plane
Overprint varnish (OPV) can protect a printed film from rubbing, scratches, and some environmental stresses. In LEP applications, however, varnish introduces another material interface. It must wet the ink surface, form a continuous film, dry or cure properly, and remain bonded through the product's actual use conditions.
When only the varnish lifts, the investigation should focus on varnish chemistry, surface wetting, applied weight, and drying or curing. When varnish and ink lift together, the weak interface may be deeper in the structure. An apparently impressive rub result from an intact varnish film does not establish that the varnish is adequately anchored underneath.
Water-based varnishes depend on appropriate liquid removal and film development. Radiation-curable varnishes depend on a suitable curing process. In either case, a dry-to-touch surface does not automatically prove that the final properties have been reached. Check after a defined conditioning time as well as shortly after application.
When post-print surface treatment is useful
Some compatible varnishes may require or benefit from a controlled post-print treatment of the LEP ink surface. The aim is to obtain the wetting and bonding needed for the specific coating, not to maximize a surface-treatment setting.
A meaningful trial compares varnished samples with and without treatment under otherwise equivalent conditions, then follows with relevant tests: adhesion, rub resistance, heat exposure, flexibility, and the actual converting operation. Excessive treatment can be counterproductive. Do not apply a fixed treatment recipe to all varnishes or papers simply because it has worked once.
Lamination: a failure that appears only under heat and pressure
Lamination adds at least one film, an adhesive layer, and a bonding process to the printing construction. Depending on the equipment and chemistry, the product may be exposed to heat, pressure, mechanical tension, and a defined development or cure period. These loads can uncover a weak interface that was not evident during initial printing.
After a peel failure, inspect both separated surfaces carefully. If the printed ink remains on the paper but the adhesive releases, adhesive compatibility or adhesive-layer development becomes a strong candidate. If the ink transfers with the laminated film, investigate primer-to-ink and primer-to-paper bonds. If the paper coating itself comes off with the film, examine the grade and internal strength of the coated substrate.
Peel force alone is not sufficient. Two structures can yield similar recorded forces while failing at entirely different interfaces. Record fracture type, sample conditioning, peel geometry, and the time elapsed since lamination. If adhesive curing is involved, premature testing can make a valid construction appear weak, while delayed failure may reveal a distinct environmental sensitivity.
Temperature, pressure and dwell: more heat is not always the answer
When a post-print bond is weak, raising temperature may appear attractive. Yet a higher temperature may also soften a polymeric ink film, amplify strain, modify a paper coating or worsen the weakest interface. The displayed heater temperature is not necessarily the actual temperature at the bond line.
The appropriate engineering experiment examines temperature, contact pressure, and dwell together, using a controlled matrix. In some qualified processes, a lower temperature paired with a suitable longer dwell can provide adequate bonding with less thermal stress. That is not a universal lamination prescription: the adhesive's chemistry and the finished product's performance must still be met.
Measure or characterize process conditions at the interface where possible. Separate the effects of material compatibility from those of thermal exposure. A modification that reduces visible ink damage but fails the bond-strength requirement is not a successful correction.
The tape test: useful evidence, limited scope
Adhesive-tape tests provide practical information about localized adhesion and surface strength, but their results depend on tape type, pressure, contact time, removal speed, and removal angle. Results obtained under one procedure should not be casually compared with a different procedure.
Paper adds special interpretation challenges. Fiber tear can mean the tested interface was stronger than the paper's local fiber network. In another application, that same weak paper network may be unacceptable under laminate peel or repetitive folding. Tape testing is therefore a screening or comparative method, not a complete qualification of end-use durability.
Document the exact procedure and the failure appearance. For a product exposed to multiple downstream processes, supplement tape testing with application-specific rub, scuff, fold, peel, heat, or humidity tests.
Build the investigation from a reproducible symptom.
Before changing the process, define the complaint in observable terms. Does the failure occur immediately after printing or only after several hours? Is it associated with a specific color, paper batch, side of the sheet, region of the image, or machine contact point? Did it appear after a primer change, a new varnish, a new paper lot, or a change in storage conditions?
Secure a known-good reference sample and preserve the defective sample. Record substrate identity, lot and conditioning, transfer mode, primer method, ink sequence, coating and finishing conditions. Without this baseline, the team may unknowingly compare products made under several different sets of conditions.
The next test should be selected to distinguish between competing explanations. If the problem follows the paper lot, investigate the paper. If it follows the varnishing operation, examine the varnish and the underlying interfaces. If it follows a new primer batch, investigate its concentration, age, and application system. Avoid replacing the press settings, primer and paper simultaneously: a multi-variable change may appear successful but cannot establish a credible root cause.
A practical root-cause test matrix
Investigation stage | Measure or compare | Main diagnostic value |
|---|---|---|
Incoming material | Paper grade, side, lot, coating, roughness and moisture | Establish substrate dependence |
Reference substrate | Same image on a proven good paper | Separate paper-related behavior from common process problems |
Transfer configuration | Supported mode and ink order under controlled conditions | Test ink-transfer or film-construction contribution |
Primer | Identity, compatibility, viscosity, coat weight, coverage and dry state | Determine whether functional surface preparation is stable |
Adhesion | Immediate and conditioned tests with fracture documentation | Identify weak interface and time-dependent behavior |
Paper mechanical strength | Surface pick and internal bond tests as appropriate | Distinguish paper cohesion from ink adhesion |
Mechanical durability | Rub, scuff and scratch in representative equipment | Test wear rather than assuming adhesive failure |
Varnish | Wetting, adhesion, applied weight, drying and curing | Identify the varnish-to-ink mechanism |
Lamination | Peel force, fracture plane, temperature, pressure and dwell | Identify the limiting layer in the bonded structure |
Final product | The actual folding, cutting, handling, or use simulation | Validate the proposed correction end to end |
Not every fault requires every test. The table is a decision framework. The most efficient investigation tests the hypothesis that best explains the failure's location, timing, and appearance, then expands only when the evidence demands it.
A controlled example: coated silk paper fails after varnishing
Consider a printed silk-coated paper that looks correct and passes initial visual inspection, but shows ink lifting after OPV is applied. A poor response would be to increase primer, change varnish, raise drying temperature, and switch printing mode in the same trial. Even if the defect disappears, the team will not know which change caused the improvement or whether the new condition is robust.
A structured investigation would first verify the failure plane. Then it would compare the problematic silk grade with a coated reference stock of demonstrated performance. Samples would be tested both before and after varnishing. If adhesion is sound before OPV but only the silk grade fails afterward, the investigation would examine whether varnishing stresses reveal a weak coating, or whether the varnish and underlying LEP surface are chemically incompatible.
Only then would the trial alter one variable at a time: perhaps a verified alternative primer system, a different coating process condition, or a different paper grade. Repeatability must be confirmed over multiple samples and after an appropriate conditioning period. The example illustrates a diagnostic method; it should not be represented as a documented production failure with a proven outcome unless actual test records support that claim.
When can a result be called the root cause?
A successful adjustment shows improvement, not automatically causation. To establish a root cause, explain the mechanism by which the changed variable influences the failure. If a new paper works, what property changed: roughness, surface strength, coating chemistry, absorbency, or moisture response? If more primer helps, did it improve coverage, alter transfer, or merely shift the fracture plane?
A strong finding combines three elements: an identifiable failure mechanism, a test that discriminates that mechanism from alternatives, and a reproducible correction. It also requires checking for unintended consequences such as blocking, curl, color change, or accelerated wear in downstream equipment.
The aim is to replace intuition-only troubleshooting with evidence that can be incorporated into the manufacturing specification.
Solutions must follow the confirmed mechanism.
Confirmed limiting mechanism | Engineering response to evaluate |
|---|---|
Excessive roughness or discontinuous contact | Qualify a more suitable paper grade, surface preparation, or transfer condition. |
Primer penetration into a porous uncoated paper | Optimize application and dry functional coverage, or select better surface sizing. |
Poor wetting on coated paper | Change to a compatible surface chemistry or qualified primer system. |
Weak pigment-coating cohesion | Select paper with adequate surface/coating strength; revise incoming specification. |
Low internal bond within board | Evaluate a more robust board construction and conversion loads. |
Transfer-mode-dependent adhesion | Validate the supported mode, primer configuration, and color strategy. |
Scuffing with good ink adhesion | Remove machine contact causes and qualify appropriate mechanical surface protection. |
Poor varnish anchorage | Investigate surface treatment, varnish chemistry, dry weight, and curing. |
Lamination-only separation | Identify adhesive and ink fracture planes; optimize materials and bonding window. |
Viscosity drift during production | Stabilize and monitor primer concentration, temperature, circulation, and cleanliness. |
Failure following primer replacement | Verify cleaning, chemical compatibility, and residual contamination. |
Repeated variability between paper lots | Require material properties beyond grammage and visual finish. |
The objective is not simply the strongest bond obtained in one laboratory test. It is a repeatable product that survives its required printing, converting, storage, and end-use sequence without creating new process problems.
Relevant material-test standards and their limitations
International test standards can provide consistent measurements, but they are not universal pass/fail specifications for LEP print adhesion. The choice of method must follow the property being investigated and the scope of the standard. Current editions should be confirmed when preparing a formal manufacturing specification.
Method or standard | Property evaluated | Interpretation for LEP troubleshooting |
|---|---|---|
ISO 8791-4 | Print-surface roughness by the Print-Surf method | Helps characterize contact-related paper differences |
ISO 3783 | Resistance to picking in paper and board | Describes substrate strength under its defined test conditions, not LEP transfer directly |
ISO 535 | Water absorptiveness by the Cobb method | Characterizes water uptake, not the retained functional primer coat weight |
ISO 16260 | Internal bond strength | Helps investigate failure inside paper or board |
ISO 15754 | Z-directional tensile strength | Assists with through-thickness material failure investigations |
ISO 8254-1 | Specular gloss | Describes optical appearance, not coating adhesion or cohesion |
These measurements are most valuable when combined with carefully documented ink-adhesion and converting tests. A compliant roughness value does not guarantee a qualified primer bond. A high gloss value does not certify coating strength. A strong laboratory bond does not prove that the finished article will resist every thermal or mechanical stress.
Why changing primer is not always the correct repair
Primer is a powerful interfacial tool, but it is not a cure for every substrate weakness. It cannot be assumed to transform a friable paper coating into a strong structural layer. Nor can a small additional coating reliably compensate for surface topology or penetration far outside the coating process's capability.
When several properly applied primers give only intermittent improvement, the troubleshooting process should return to the substrate. Paper grade, surface sizing, pigment-coating cohesion, or even the product's converting demands may be the limiting factor. A more compatible grade or a revised finishing specification may provide a genuinely repeatable solution.
The strongest response is to stop cycling through materials blindly and identify the property that constrains the application.
Prevent recurrence by turning the diagnosis into a specification.
Once the mechanism has been established, the solution should become a controlled production standard. This may include approved substrate grades, critical surface and strength properties, conditioning requirements, supported LEP transfer configurations, ink order, compatible primer families, coat-weight and drying windows, and the downstream coatings or adhesives authorized for the job.
Incoming material controls must be connected to the failure mechanism. If the cause was a weak pigment coating, monitoring grammage and whiteness alone will not protect production. If the cause was primer-viscosity drift, an initial sample alone will not protect a long shift. If the problem appeared only under lamination heat, an immediate tape test cannot be the sole release criterion.
A robust specification documents sampling frequency, test methods, failure-plane categories, and acceptance criteria. New paper lots, coating changes, or transfer-mode changes should trigger appropriate requalification when they can affect the proven mechanism.
Conclusion: before repairing the ink, understand the paper
LEP printing is a system in which a transferred polymeric ink film must interact with a specific substrate surface. That surface is not mechanically or chemically uniform merely because the sheet looks smooth and prints sharply. Uncoated paper may introduce topography, porosity, loose fibers, and primer penetration. Coated paper may have an attractive finish while containing a mechanically weak or chemically unsuitable pigment layer. Multilayer paperboard may fail within its own structure during folding or lamination.
Transfer mode, ink-layer sequence, primer chemistry and coating conditions all matter. So do varnish, adhesive, heat, pressure and the time allowed for materials to develop their properties. A weak product can therefore emerge from a perfectly functioning printing press when a material interface is mismatched to the final application.
The appropriate response is to identify the actual failure plane, characterize the material, isolate variables through controlled comparisons, and establish a reproducible correction. Then confirm the result under final-use stresses and translate it into process controls.
Print quality does not begin solely at the printing press. It begins with understanding the surface the ink is expected to remain on.
And when an apparent adhesion failure occurs, the most useful question is not which primer to increase or which temperature to raise. It is: What exactly failed, and which test will prove why?