Cutting Is Only the Beginning: When Converting Determines Whether a Folding Carton Will Actually Work
Die-Cutting, Creasing, Punching, Stripping, Blanking, Folding, and Gluing — How Knife Selection, Crease Design, Sheet Grain Direction, and Paperboard Construction Determine Carton Accuracy and Performance
By Ronen Dolev
When the Printing Is Perfect, but the Carton Will Not Fold
Printed sheets for premium cosmetic cartons leave the printing press. The colors are accurate, registration is correct, the varnish is uniform, and the embellishments sit precisely where the artwork specifies. Every print-quality inspection has passed.
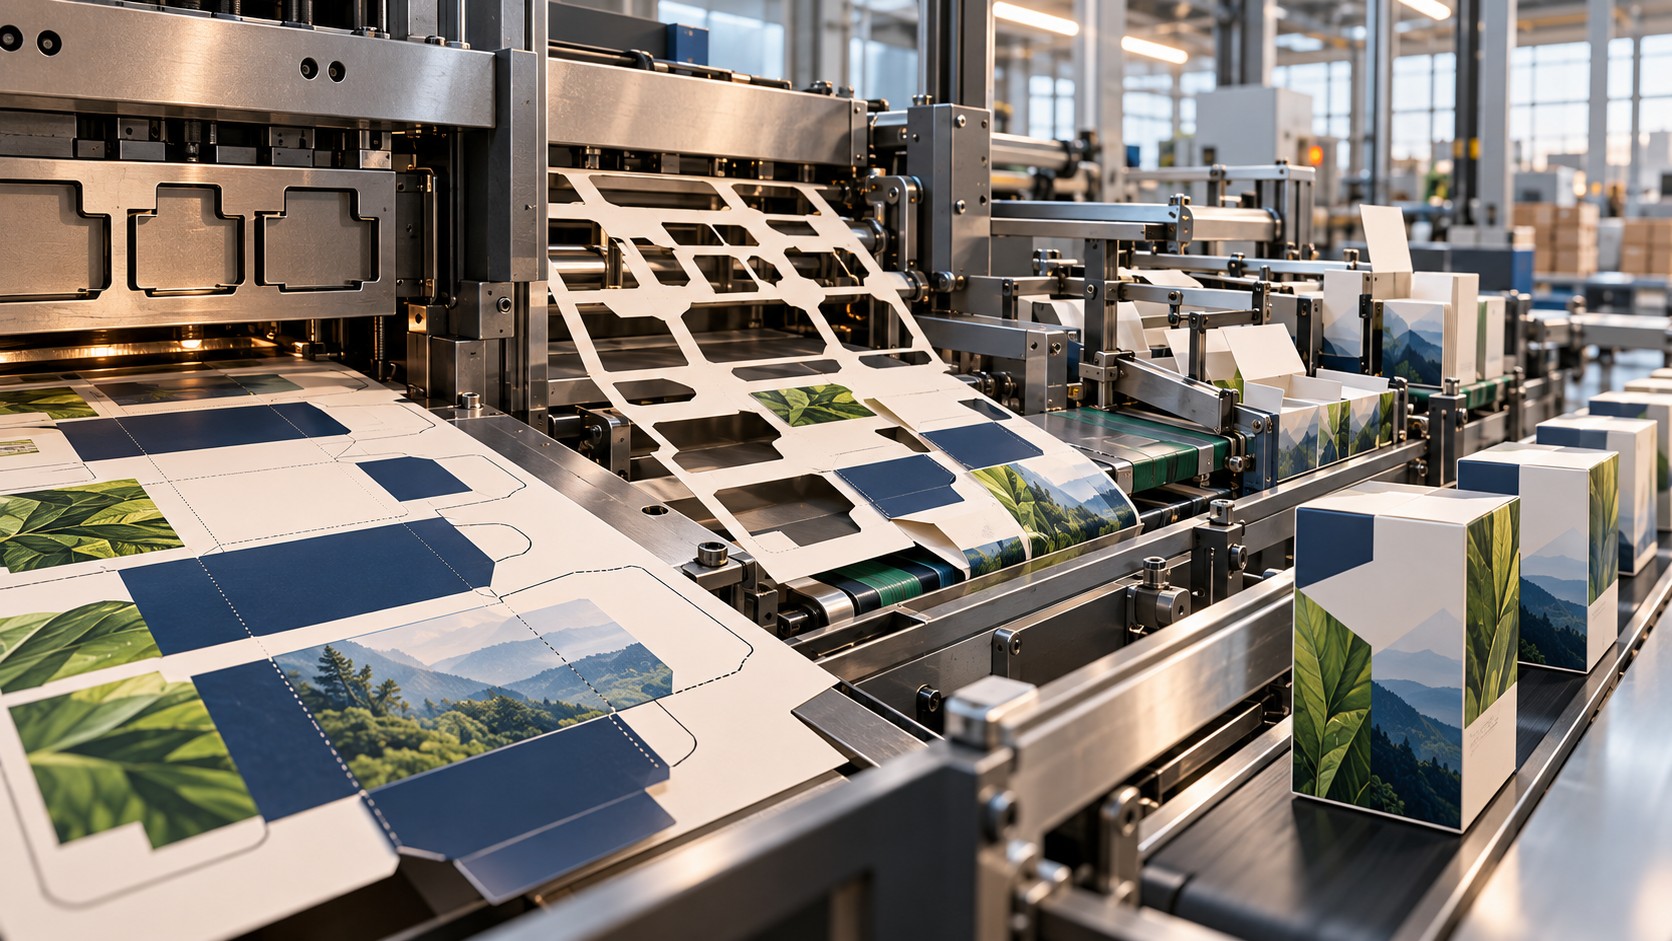
The sheets move to a die-cutting machine, where the carton outline is cut and the crease lines required for folding are formed. Waste is then removed, the blanks are separated, and the finished blanks proceed to the folder-gluer.
But as soon as folding begins, a problem appears. Some cartons do not fold precisely along the intended lines. Fine cracks develop along printed corners on others. Several cartons show misalignment between panels, and the gap at the glue flap is not consistent.
The folder-gluer operator changes belt positions and transport pressure, slows the machine, and adjusts the pre-breaking conditions. Some results improve, but the underlying problem does not disappear.
Inspection of the die-cut blanks shows that the crease lines do not behave consistently. Some creases look relatively deep and sharply defined; others are broad and shallow. Comparing fold lines reveals another difference: creases running parallel to the grain behave differently from those running across it.
A review of the board specification reveals that the job was qualified on 700 × 500 mm long-grain sheets, where the grain runs parallel to the 700 mm edge. A later delivery, however, was short grain, where the grain runs parallel to the 500 mm edge. The carton layout was unchanged, but its orientation relative to the fibers had changed.
The fault was not necessarily created in the folder-gluer. It began with sheet selection, carton layout, and the relationship between grain direction and the die-cutting and creasing tools.
This is a fundamental principle of folding-carton engineering: converting is not a collection of independent operations. It is a chain in which one operation establishes the process window of the next. The cutting rule determines edge quality; creasing determines folding behavior; grain direction influences rigidity and dimensional response; stripping must preserve blank integrity; and gluing must produce a dependable joint.
A carton is not qualified merely because it was printed and cut accurately. It is qualified when it can be folded, erected, glued, and used as a functioning finished package.
From a Printed Sheet to a Three-Dimensional Package
A folding carton is usually produced from printed paperboard sheets that pass through several finishing stages. First, a dieline defines the panels, cut lines, crease locations, locking tabs, openings, and glue flaps. Following printing and embellishment, the sheets undergo die-cutting and creasing. Stripping removes unwanted material, while blanking separates and stacks the usable carton blanks.
The blanks then enter a folder-gluer for alignment, preliminary folding, final folding, adhesive application, compression, and delivery. The result is commonly a side-seamed carton in flat form, which must subsequently be erected into a three-dimensional shape by the packer's equipment or by hand.
At every stage the material has already been changed by a preceding operation. The board may carry high ink coverage, varnish, foil, and other surface finishes. Those layers influence how the substrate responds to cutting, compression, bending, and adhesive bonding. Knife selection and crease design cannot be separated from the full construction and intended use of the carton.
Long Grain and Short Grain: Correctly Describing Grain Direction in Sheets
Paper and paperboard contain fibers with a preferred orientation established during papermaking. In manufacturing terms, the direction of travel through the paperboard machine is the machine direction (MD), and the perpendicular direction is the cross direction (CD).
For sheetfed folding-carton production, however, grain direction relative to the dimensions of a delivered sheet is normally specified as Long Grain (LG) or Short Grain (SG). This terminology describes the sheet itself; it does not indicate which edge leads into the printing press.
On a 700 × 500 mm sheet, the distinction is straightforward:
Sheet designation | Grain orientation | Meaning |
|---|---|---|
Long Grain (LG) | Parallel to the 700 mm edge | Grain Long |
Short Grain (SG) | Parallel to the 500 mm edge | Grain Short |
A long-grain sheet does not necessarily enter the press with its long edge leading. Likewise, a short-grain sheet need not enter with the short edge leading. Feeding direction is determined by press configuration, gripper position, and imposition; grain direction is an inherent characteristic of the supplied material.
Two 700 × 500 mm sheets of identical grammage and caliper can behave differently during converting if one is long grain and the other short grain. Paperboard stiffness, bending resistance, dimensional stability, and the way a crease is formed can vary with fiber orientation.
The orientation of the carton blanks on the sheet determines whether a particular fold line runs parallel or perpendicular to grain. That relationship can affect the crease geometry required, folding torque, spring-back, and the rigidity of the erected carton panels. For these reasons, grain direction belongs on the material specification and the CAD dieline—not solely on the purchasing order.
What Happens When a Crease Line Runs Parallel to Grain?
It is tempting to assume that folding along the grain is always easier. Creasing in folding carton production is more complicated. Technical guidance from Iggesund indicates that achieving an optimal crease whose line is parallel to the grain may be more challenging than creasing across the grain, depending on board construction.
The distinction relates to fiber deformation, controlled internal ply separation, and the mechanical resistance that develops when the carton folds. In some cases, crease lines parallel to grain require adjustments to channel width or other tooling parameters. But there is no universal instruction to place every fold line across grain.
A carton may have major folds in two perpendicular directions, and its erected walls must provide sufficient stiffness as well as ease of folding. Consequently, carton engineering requires a balance between crease formation, the folding process, final-panel strength, and the requirements of the customer's packaging machine.
One 700 × 500 mm Sheet, Two Grain Orientations
Consider a 700 × 500 mm sheet carrying several carton blanks. With long grain, fibers run parallel to the 700 mm edge. A crease drawn parallel to that edge is also parallel to the grain; a crease parallel to the 500 mm edge runs across it.
With short grain, those relationships reverse. The same die-cutting tool may form the same geometrical lines in the same locations, yet the underlying board is being deformed in different fiber orientations. Fold resistance, the resulting bead, and the behavior of the erected carton may change. Switching from LG to SG is therefore an engineering change that warrants qualification, not just a logistical substitution of paperboard inventory.
Die-Cutting: Creating the Carton's Geometry
Die-cutting forms the carton outline from the printed sheet. Its tooling typically combines cutting rules with creasing rules, perforation elements, and any other cutting features required by the dieline.
In flatbed die-cutting, widely used for folding cartons, the tool works against a counter-surface during a controlled press stroke. Rotary and digital cutting technologies are also available, with their own suitable applications and limitations. The correct process depends on the paperboard, dieline complexity, production length, required accuracy, and converting configuration.
Regardless of the technology, the underlying question is the same: how can the board be separated accurately while avoiding unnecessary damage to its structure? A good cut must provide clean edges, correct dimensions, consistent cut-to-print registration, and adequate integrity in the areas that must remain connected until waste removal.
Selecting the Die-Cutting Rule
Traditional flatbed tools use steel cutting rules shaped and installed to match the dieline. Selecting a rule involves body thickness, height, bevel profile, edge angle, steel properties, and expected life under repeated loading.
Cutting rules are often described in points, with common nominal examples as follows:
Nominal rule thickness | Approximate thickness |
|---|---|
1.5 pt | 0.53 mm |
2 pt | 0.71 mm |
3 pt | 1.06 mm |
4 pt | 1.41 mm |
A 2-point rule is common in folding-carton applications, but it is not universally correct. A thinner rule may be useful for fine details but must retain sufficient mechanical stability. A thicker rule may suit other loads or constructions yet produce a different local compression pattern in the board.
The bevel profile is another consideration. A center bevel positions the cutting edge centrally, whereas a side bevel is asymmetrical. They can distribute material displacement differently and may affect edge quality and geometric accuracy. Bevel angle influences the compromise between sharpness and durability: a very sharp edge can require less penetration force but may be more vulnerable to damage, while a more robust profile may demand different cutting forces.
There is no single ideal bevel angle for all boards. The final decision should consider grade and caliper, coating structure, small radii and intricate details, run length, expected wear, and production trials.
Cutting-Rule Height, Cutting Plate, and Make-Ready
A common nominal reference height in many folding-carton steel-rule systems is 23.80 mm, but other tooling heights exist. The rule height must match the die system and cutting-machine design.
If a section of the rule is too low, a partially cut area can remain. If a section is too high or overall impression is excessive, the rule may damage the counter-surface or wear prematurely.
The cutting plate provides support against the rules. Its flatness, wear, and condition influence the pressure distribution. Make-ready allows localized adjustment where the impression is insufficient, but excessive make-ready can introduce new damage and overloading.
When a cut is incomplete, increasing total machine pressure should not be the first reflex. Examine rule height and condition, plate wear, alignment, local support, and the pattern of the incomplete cut. Increasing overall pressure may cure one small area and damage several others.
Creasing: Creating a Controlled Folding Hinge
Creasing has a different objective from cutting. A cutting rule separates the material; a creasing rule creates controlled mechanical deformation that reduces bending resistance in a defined region.
In a conventional system, a smooth rounded creasing rule forces the board into a channel in a counter-die or creasing matrix. A properly designed crease creates a hinge-like region while retaining the integrity of the outer layers.
In multilayer paperboard, controlled internal separation between fiber plies can be a desirable part of crease formation. It permits some internal movement during folding and reduces excessive tensile stress at the external surface. This must not be confused with uncontrolled delamination or cracking that spreads beyond the crease.
The target is a sharp, accurate, repeatable fold without unacceptable damage to the board, ink, coating, or embellishment.
Choosing Creasing-Rule Thickness, Rule Height, and Channel Width
The first input is actual board caliper, not grammage alone. Boards with the same g/m² can have different thicknesses, density profiles, ply structures, and folding responses.
One CITO starting method for selected folding-carton tooling systems expresses the geometry as:
A ≈ c
B = (1.5 × c) + d
h = 23.80 − c
where c is board caliper in mm, d is creasing-rule thickness, A is channel depth, B is channel width, and h is creasing-rule height in a system with a 23.80 mm cutting-rule reference. These are initial design relationships within the applicable tooling method, not universal production settings.
An indicative selection table for certain creasing-rule systems is:
Paperboard caliper | Initial creasing-rule thickness |
|---|---|
Up to 0.30 mm | 1.5 pt, approximately 0.52 mm |
Above 0.30 to 0.58 mm | 2 pt, approximately 0.71 mm |
Above 0.58 to 0.85 mm | 3 pt, approximately 1.05 mm |
Above 0.85 to 1.20 mm | 4 pt, approximately 1.42 mm |
Above 1.20 mm | 6 pt, approximately 2.10 mm, depending on system |
These values are starting points. Grade, coating, fiber direction, crease orientation, and actual folding requirements can all require adjustment.
Worked Example: 0.45 mm FBB on a 700 × 500 mm Sheet
Consider FBB paperboard with a caliper of 0.45 mm and a 2-point creasing rule approximately 0.71 mm thick. The stock is supplied as 700 × 500 mm sheets, specified Long Grain, parallel to the 700 mm edge.
Initial channel width: B = (1.5 × 0.45) + 0.71 = 1.385 mm.
Initial channel depth: A ≈ 0.45 mm.
Initial creasing-rule height: h = 23.80 − 0.45 = 23.35 mm.
These numbers guide tool selection, not direct machine setup without testing. Inspect crease lines parallel to the 700 mm edge separately from those parallel to the 500 mm edge, because in this long-grain sheet they have different relationships to fiber direction.
Evaluate fold accuracy, bead geometry, visible cracking, the integrity of printed and coated layers, and fold resistance under the conditions of the intended folder-gluer and cartoner.
Why Creasing-Channel Width and Depth Matter
A channel that is too narrow may concentrate deformation and increase the likelihood of external cracking. A channel that is too wide may produce a poorly defined hinge, allowing the fold to drift from the desired line.
An insufficient crease may leave excessive bending resistance. Excessive deformation can crush or damage layers. The objective is not the deepest possible crease but a balanced hinge with predictable geometry and adequate strength.
Adapting Creases to Long Grain and Short Grain
The calculation above provides an initial geometry, but actual performance can differ for crease lines parallel and perpendicular to grain. Industry guidance describes circumstances in which creases parallel to fibers require special optimization, including possible changes to channel width relative to the starting formula.
Do not make such changes automatically. Observe the grade, coating integrity, and fold resistance. On the CAD layout, specify an explicit grain-direction arrow: for a 700 × 500 mm Long Grain job, the arrow follows the 700 mm edge; for Short Grain, it follows the 500 mm edge.
A material designation alone is not enough—the engineer must relate grain direction to each important crease in the imposition.
Scoring Versus Creasing
The terms scoring and creasing are sometimes used interchangeably, although the processes are not always identical. Traditional folding-carton creasing normally uses a rounded rule and a counter-channel. Other graphic-finishing scoring systems can use opposing rotary wheels to produce a fold line as the sheet passes through them.
Both must be distinguished from partial cutting or kiss-cutting, in which a blade deliberately penetrates only part of a structure. Conventional mechanical creasing is intended to facilitate bending without severing the outer board layers, while a partial cut creates a controlled weakening by material removal or penetration.
The bead direction is also relevant. In a conventional carton-creasing configuration, the deformation and intended fold direction must be coordinated with the rule and counter-channel so that the resulting hinge works as designed.
Why Cracks Develop During Folding
As a carton folds, the external region of the bend experiences tensile stress while internal regions undergo compression and rearrangement. If the creasing geometry does not distribute those strains properly, cracking can develop in the fiber structure, coating, ink, or varnish.
Identifying the failing layer is essential. If board fibers remain intact but the varnish cracks, examine coating flexibility and compatibility with folding. If the fibers themselves fracture, investigate board construction and crease geometry. If the defect occurs predominantly in fold lines of one orientation, examine the relationship to grain.
For example, on a 700 × 500 mm sheet, repeated cracks along lines parallel to the 700 mm edge mean those lines are parallel to grain when the stock is LG and perpendicular when it is SG. This is a valuable diagnostic clue, although not proof of the root cause by itself.
Paperboard is hygroscopic, so storage and conditioning also matter. Very dry board may be more susceptible to cracking in some conditions; excessive moisture may contribute to curl, dimensional changes, and feeding instability. Record storage and conditioning conditions as part of the investigation.
Punching and Perforation for Functional Features
Folding cartons frequently require holes or features beyond their external outline: hang holes, windows, handles, locking details, or controlled opening regions. Punching forms openings with an appropriate tool, sometimes comprising a punch and matching die. Small openings require particular attention to waste ejection so that cut-outs do not lodge in the tool.
Perforation is different: alternating cut segments and uncut ties form a planned tear line. Weak ties can allow premature opening during transport or converting; excessively strong ties make consumer opening difficult. Geometry must be selected to achieve the intended opening force and tear path.
Function should be validated on the erected, completed carton—not merely on the flat die-cut sheet.
Stripping and Blanking: The Cut Must Also Release Cleanly
Once the carton is die-cut, surrounding and internal scrap must be removed in stripping. Blanking then separates and stacks the usable carton shapes. Small intentional connections called nicks can keep pieces together temporarily during sheet transport.
Poorly designed nicks lead to problems. Connections that are too weak release material prematurely; those that are too strong tear fibers or leave visible marks during separation. Ejection rubber also matters because it helps release the sheet from the rules after the cutting stroke. Incorrect rubber characteristics or placement can distort blanks, damage edges, or destabilize waste removal.
A professional die should therefore be designed as a system integrating cutting, creasing, material retention, ejection, stripping, and blanking—not as an outline of sharp blades alone.
Folding-Gluing: From Flat Blank to Carton
After die-cutting and creasing, blanks enter a folder-gluer for feeding, alignment, pre-breaking, folding, adhesive application, compression, and transfer. Carton constructions include straight-line, crash-lock bottom, four-corner, and six-corner configurations, each requiring a different folding and gluing path.
Pre-Breaking
Pre-breaking bends a crease in a controlled manner before final folding, helping establish the hinge and reduce initial folding resistance. It can help the flat carton erect reliably later. However, it cannot reliably repair a crease placed incorrectly or formed with unsuitable channel geometry. Repeated folding may worsen cracking or distortion when the underlying crease is defective.
Spring-Back
After folding, paperboard may partially recover toward its earlier form. This spring-back depends on board stiffness, creasing geometry, grain direction, and folding conditions. Excessive spring-back may prevent the carton from staying flat or make it difficult to erect. What looks like a folder-gluer alignment fault can therefore originate from the board and crease design.
Gluing: The Final Joint Depends on Earlier Layers
Gluing joins carton panels using adhesive systems selected for the structure, equipment, and application. Water-based and hot-melt adhesives are common, but adhesive performance depends on the actual surface being bonded.
If a glue flap is covered by varnish, foil, lamination, or ink with incompatible surface characteristics, wetting and adhesion can suffer. Bonding areas should be designed with those interfaces in mind; in many cartons, avoiding problematic embellishment or coatings in the glue zone is appropriate.
When bonding over a printed or coated layer is required, qualify the complete combination. Corona or plasma treatment may be an option in equipment specifically designed for it but is not a universal cure. The treatment must not damage the ink or varnish and must demonstrably improve the actual bond.
After gluing, assess adhesive placement, setting time, and joint strength. Fiber tear on separation can indicate that the bond exceeds the local board-ply strength under test conditions, but it does not automatically prove compliance with every product acceptance criterion.
Quality Control: What Must Be Checked Before Carton Approval?
A flat blank may look correct yet fail once folded. Quality control therefore needs gates at several stages. After die-cutting, check dimensions, cut-to-print registration, edge quality, and crease positioning. After creasing, inspect hinge geometry, board response during folding, and integrity of external layers. After stripping and blanking, verify complete scrap removal and undamaged blanks.
After folding-gluing, assess squareness, seam position, glue integrity, spring-back, and ease of erection. For automatically packed cartons, validate performance on representative erecting and filling equipment. A carton that folds well by hand may behave differently on a high-speed line.
Bending or folding-resistance tests can help compare crease designs and paperboard grades, but there is no universal acceptance value. Acceptance limits must be established from the required carton function and actual production equipment.
Troubleshooting: Die-Cutting, Creasing, and Folding
Symptom | Possible causes | First diagnostic action |
|---|---|---|
Incomplete cutting | Rule height, uneven pressure, cutting plate | Check tool and make-ready before increasing impression |
Loose fibers on edges | Worn rule, edge profile, ejection rubber | Inspect the edge and material support |
Cut-to-print misregistration | Sheet feed, registration, dimensional movement | Check grippers, sensors, and board stability |
Cracks at folds | Crease geometry, coating, grain direction | Identify the failed layer and confirm LG/SG |
Different behavior between folds | Grain relationship to crease lines | Compare creases parallel and perpendicular to grain |
Poor fold accuracy | Wide or off-center channel | Check channel width and alignment |
Weak crease | Insufficient penetration or incorrect rule height | Evaluate crease geometry and folding force |
Damage to back surface | Excessive pressure, debris, unsuitable matrix | Inspect matrix and make-ready |
Scrap will not release | Incomplete cutting, nicks, stripping system | Check waste and stripping-tool geometry |
Damage during blanking | Excessively strong nicks or poor alignment | Inspect blanking setup |
Excessive spring-back | Board stiffness, creasing, pre-breaking | Reassess hinge design and grain direction |
Folder-gluer deviation | Crease, feeding, folding mechanism | Check blanks before major machine changes |
Weak gluing | Bonding surface, adhesive, set time | Identify the failure plane |
Excess glue | Application amount, position, viscosity | Adjust adhesive application |
The table is a diagnostic starting point, not a replacement for controlled trials. Identify the first stage where the defect appears and the layer that fails. Keep a qualified reference sample, change one principal variable at a time, and record the result.
Case Study: One Carton, Two Grain Directions
Consider a cosmetic carton made from coated FBB with a caliper of 0.45 mm. Its blanks are imposed on 700 × 500 mm sheets. Initially the material is supplied long grain, with fibers parallel to the 700 mm edge.
During qualification, cutting and folding pass. The carton folds accurately, and its exterior surfaces remain intact. Weeks later, another lot arrives with the same sheet dimensions, grammage, and caliper—but now it is short grain, with fibers parallel to the 500 mm edge. The print file and die-cutting tool remain unchanged.
At first the job looks fine. In the folder-gluer, however, one group of creases shows higher resistance, several cartons exhibit increased spring-back, and small cracks appear in some areas.
Simply increasing impression pressure would be premature. The same dieline now interacts with a different fiber orientation: some creases formerly parallel to grain are perpendicular, and vice versa.
A sound response compares the two grain orientations, measures or assesses folding resistance, examines coating damage, and identifies which crease lines are most sensitive. Based on the result, the team may qualify a revised crease geometry or reassess blank orientation on the sheet. Any modification must also be evaluated for panel stiffness, carton squareness, gluing, and ease of erection.
This is why LG/SG must be recorded in the product specification—not left as an incidental purchasing detail.
Qualifying Die-Cutting and Folding-Gluing as a Complete Process
For a new folding carton, start with the finished package and work backward. Define the product, erecting requirements, filling process, carton construction, and acceptable functional limits. Select the paperboard grade and caliper, and specify grain orientation relative to the 700 × 500 mm sheet and the dieline.
Then design cutting and creasing tools. Select rule thickness, height, bevel geometry, creasing-rule dimensions, channel geometry, and any punching or perforation features. Plan stripping, blanking, nicks, and ejection. Make the first die-cut samples and inspect the cut edges and creases—not just blank dimensions.
Next, fold the blanks and assess external-layer integrity, hinge resistance, and geometry. Run them through the folder-gluer, and finally erect representative finished cartons. The desired output is a documented process window that can be repeated, not a single acceptable sample.
The Construction and Converting Card
A repeatable process benefits from a Construction and Converting Card recording the qualified configuration. It should state paperboard grade, sheet size, caliper, grammage, and Long Grain or Short Grain. For example:
Sheet size: 700 × 500 mm — Grain direction: Long Grain, parallel to 700 mm.
Or: Sheet size: 700 × 500 mm — Grain direction: Short Grain, parallel to 500 mm.
Record blank orientation and grain relative to key folds. Then document cutting-rule grade, profile and height, creasing-rule thickness and height, channel width and depth, make-ready, nicks, ejection arrangements, stripping and blanking settings, and edge-quality acceptance criteria.
For folding-gluing, record folding geometry, adhesive specification, glue-zone design, setting time, and acceptance tests. Specify triggers for requalification: a change in paperboard grade, caliper, grain direction, or relevant surface construction can matter even if sheet size and the printed dieline remain unchanged.
Cutting Is Not the End of the Process—It Is the Beginning of Carton Function
The printing industry rightly invests in color accuracy, registration, ink adhesion, uniformity, and coating performance. Yet a well-printed sheet is not necessarily a usable carton. A blank can be dimensionally correct and still fold badly; a glued carton can look acceptable and then fail during automatic erection.
Die-cutting, creasing, punching, stripping, blanking, folding, and gluing give the carton the geometry and mechanical characteristics it needs to function. Cutting-rule selection, creasing-rule height, channel width, and grain orientation may appear to be small details. In production, they determine whether the carton folds where intended, whether its surfaces remain intact, and whether the customer's line can run reliably.
When I encounter a folding problem, I do not automatically begin by increasing folder-gluer pressure. I want to know the board grade and caliper; whether a 700 × 500 mm sheet is long or short grain; how the dieline is oriented relative to grain; and how the crease was designed. I want to locate the first appearance of the fault and identify the layer that failed.
The right knife is not simply the one that cuts. The right crease is not merely the one that leaves a visible impression. And a high-quality folding carton is not just the one that looks perfect while flat.
Real success is a carton that can be folded, erected, glued, and used accurately and repeatedly—exactly as designed.
Professional References and Further Reading
- 1.
- 2.
- 3.
- 4.
- 5.
- 6.
- 7.
TECHNICAL NOTE Knife sizes, rule heights, channel dimensions, and calculations shown here are design starting points for appropriate tooling systems. Verify all settings against the substrate, grain direction, equipment and tooling specifications, and the results of product qualification. They are not universal machine settings.