By Ronen Dolev | 2026
When the Results Change but Nobody Knows Why
For several weeks, a plant producing high-quality labels using Liquid Electrophotography (LEP) struggled with inconsistent ink adhesion. The failure did not follow an obvious pattern. Some jobs passed every quality check, while others showed localized weakness after converting and mechanical handling. The same artwork could perform well on one roll and less reliably on another nominally identical roll. Sometimes the variation emerged early in a run; other times, it appeared only after subsequent production steps.
Visually, the printing looked correct. Color remained within the defined tolerance, image uniformity was acceptable, and calibration records showed no significant deviation. The weakness appeared only when the printed construction was subjected to the mechanical resistance test specified for the application.
The local production and technical teams carried out an extensive investigation. They reviewed incoming material properties, surface preparation, primer application, and the approved press working conditions. They compared different rolls and production histories and conducted controlled trials intended to improve the printed interface. Some adjustments produced better adhesion, but none explained why the problem kept returning unpredictably.
This uncertainty made the case particularly frustrating. The facestock met its purchasing specification. The press operated within its approved conditions. The primer had been applied according to the process requirements. Yet the adhesion results continued to vary.
When the recurring failure remained unresolved, an application expert from the printing-press manufacturer arrived at the plant.
Looking for the Variable Nobody Had Measured
The expert began with the inspection records, retained samples, and sequence of earlier trials. He compared successful runs with weaker ones, looking not only at test results but also at the conditions under which they were produced.
One finding stood out. Incoming surface-response measurements varied between rolls. Several rolls associated with weaker adhesion had readings toward the lower end of the plant's historical range, although they still complied with the acceptance criteria. That was a technically credible lead: coated facestock behavior and the interface it presents to the next layer can depend on material history and surface condition.
The expert asked the team to conduct a controlled comparison using an additional, approved surface-preparation step. They kept the rest of the printing route as consistent as practical and compared the resulting adhesion performance.
The treated sample performed better. The team repeated the comparison, and the improvement appeared again.
But the expert distinguished between the observation and the proposed explanation. The trial showed that strengthening the surface preparation could improve adhesion. It did not establish why nominally similar rolls sometimes passed and sometimes failed under the routine production process.
If surface response alone explained the variation, a stronger and more consistent relationship between the incoming measurements and production results would be expected. The available records showed none. The expert therefore continued searching for another variable that had not been captured by the usual quality and press reports.
A Clue from the Storage Area
During a discussion with the operators, the expert asked whether they had noticed any circumstances shared by the weaker runs that did not appear in the recorded press data.
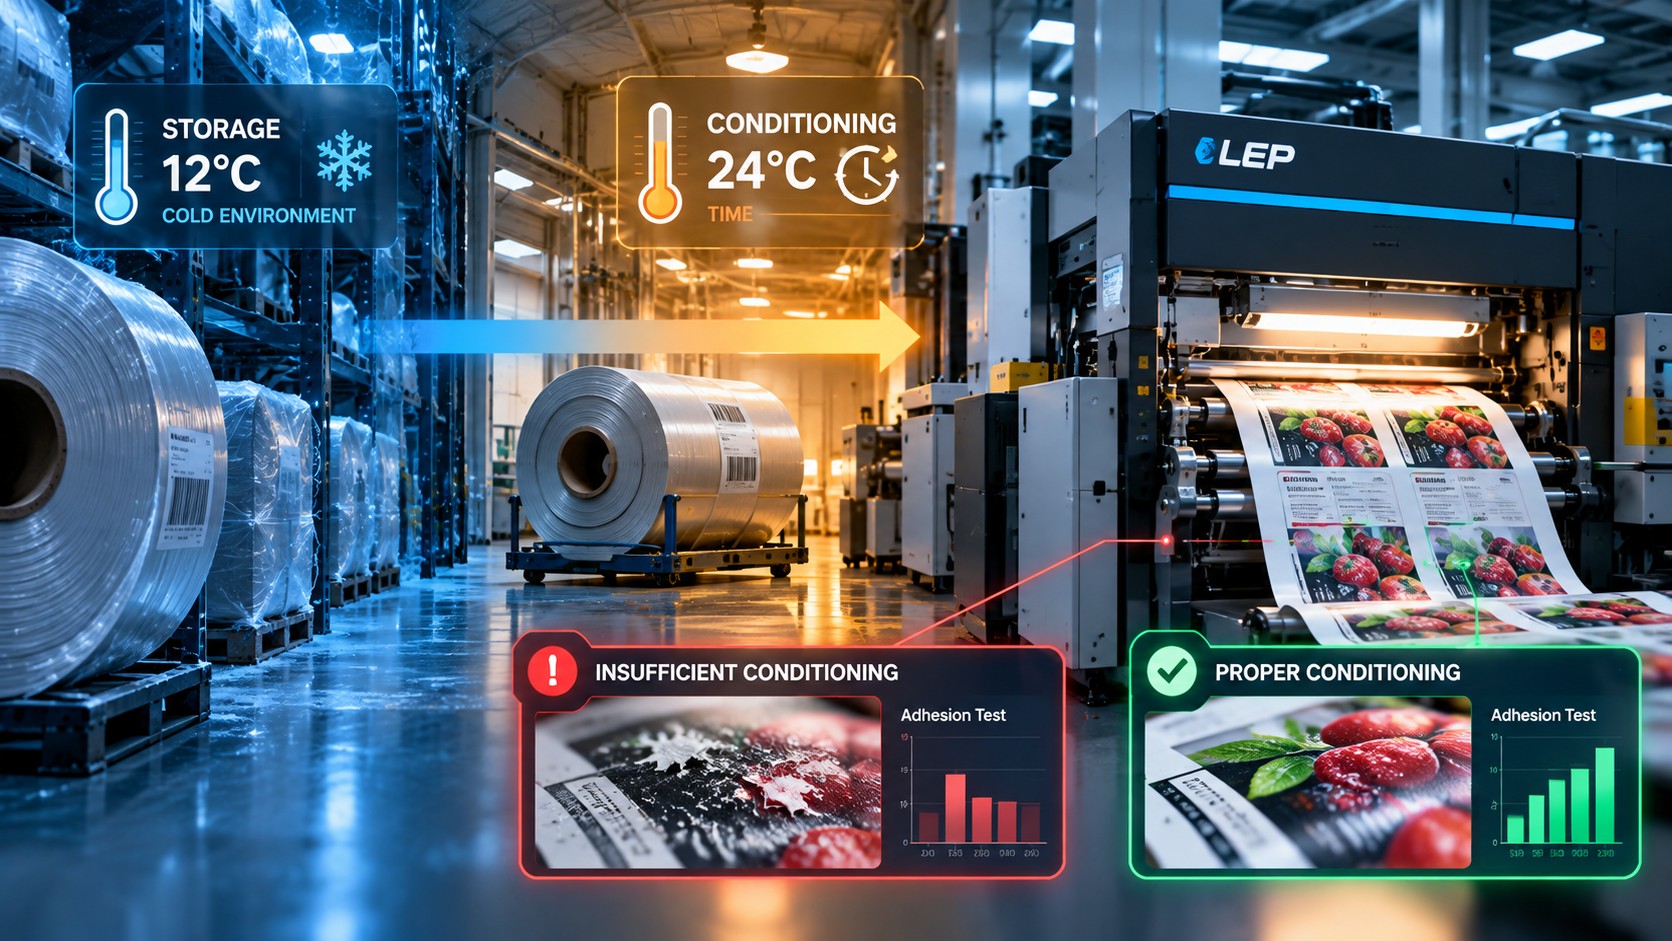
One operator recalled that some of the troublesome rolls had arrived directly from a side-storage area, where the temperature was lower than in the production hall. She had also noticed that rolls left near the press for several hours often behaved more consistently than rolls taken straight from storage.
The observation was not a diagnosis. Other weak runs had been reported later in the day, and no one could yet say whether temperature was the determining factor. Nevertheless, it identified a difference between materials the plant had been treating as equivalent.
The expert asked to see the storage area and the material-staging procedure. During colder periods, the temperature difference between that space and the controlled production environment could be substantial. The plant's work instructions included a conditioning requirement for sensitive applications, but over time compliance with that requirement had become less consistent. When a job was urgent, rolls were sometimes transferred directly from storage to the press.
No one had formally withdrawn the requirement. Production pressure had simply turned a defined preparation step into something treated as optional.
The team measured the temperature of recently transferred rolls and compared them with material that had been staged in the production environment. The differences were meaningful. They also recognized that a roll's outer surface and its inner layers do not necessarily reach thermal equilibrium at the same time.
The material grade was approved, and the lot identification was correct. But the material's physical condition when it entered the printing process was not always the same.
The missing variable was not hidden in a press parameter. It was part of the material's history before printing began.
The Experiment That Separated the Symptom from the Cause
The expert proposed a comparison designed to isolate the effect of material conditioning, rather than another attempt to improve adhesion by changing the printing process.
Comparable rolls of the same facestock were separated into two groups. One group was allowed to reach the defined conditioning state in the controlled production environment. The other followed the accelerated staging route that had become common during urgent production, within the boundaries of a controlled investigation.
The press baseline, primer route, artwork, operator practices, and evaluation method were kept consistent as far as practical. No additional surface treatment was introduced to rescue the weaker condition. Samples were collected through the run and assessed after the production steps relevant to the complaint, not merely judged by their appearance as they left the press.
The conditioned material gave stable results. Material introduced through the accelerated route showed greater adhesion variation, especially in sections produced near the beginning of the roll. As more material passed through the production environment, the results tended to become more consistent.
The team repeated the investigation with another comparable roll. The direction of the result was the same: adequately conditioned material performed more reliably, whereas material entering the process in a different thermal state showed greater early-run variation.
The repeated tests established that conditioning history was a meaningful process variable. They also clarified the earlier surface-treatment trial. Additional treatment improved the robustness of the printed interface, but it did not remove the inconsistent material-entry condition. It improved process margin, but it did not prove that inadequate surface preparation was the primary source of the recurring variation.
That distinction changed the corrective action completely.
What Can Actually Change When a Roll Enters the Press Cold?
A substrate does not lose its physical history when it reaches the printing press. Depending on its construction, coating, and the chemistry of the printed interface, its behavior may be sensitive to storage conditions, temperature equilibration, and the time spent in the production environment.
Those effects are application-specific. The same temperature change does not produce the same response in every coated facestock, and adhesion results alone cannot identify a unique microscopic mechanism. Temperature-dependent behavior may involve coating properties, wetting or formation of the primer interface, or other interactions in the layered construction. Each proposed mechanism requires its own evidence.
In this case, the controlled comparisons demonstrated that material conditioning influenced adhesion consistency. They did not establish which molecular or microscopic process was responsible. There was no documented visible condensation, so it would have been unjustified to turn moisture condensation into an assumed root cause merely because colder rolls were being moved into a warmer area.
The defensible conclusion was narrower and more useful: this application needed the facestock to enter printing in a defined and controlled thermal condition. When that requirement was not maintained, the interface became less predictable under the conditions tested.
That was sufficient evidence to introduce a targeted, verifiable correction without inventing a mechanism the investigation had not measured.
The Solution Was Upstream of the Printing Press
The principal corrective action did not require a new press setting, a different primer, or replacing a printing component. The plant reinstated material conditioning as a mandatory release requirement for the sensitive application.
Rolls arriving from storage areas with a different temperature were staged in the controlled production environment until they reached the condition established by the approved procedure. The material-handling and production-planning sequence was revised so an urgent roll would not be moved directly from colder storage to the press before it was ready. Where the risk justified it, the team verified material temperature rather than relying on the hall's air temperature or an assumed waiting period.
The plant kept the option of using a more robust, approved surface-preparation route for applications where testing showed a genuine advantage. But that route was no longer treated as an automatic workaround for material that had not undergone the required conditioning.
There was no reason to redesign a printing process that performed reliably when the material entered under the correct conditions. The task was to make sure those conditions were consistently present.
Why Did Such a Familiar Requirement Become Invisible?
From the outside, the final action might look almost too simple. Conditioning material before printing is not new. For sensitive products, it is a familiar part of industrial manufacturing.
The difficult work lay in demonstrating that this neglected step explained a variation the local team had spent weeks trying to resolve elsewhere.
The investigations had concentrated on the stage at which the failure was detected: the printed construction. Rolls were regarded as equivalent because they carried the same product description, satisfied the same incoming specification, and often belonged to the same supply family. But the records did not consistently include the material's actual thermal condition at the time of use.
As a result, the team could not discover the relationship simply by examining press logs, calibration results, or supplier lot numbers. The key variable was absent from the data set.
The expert shifted perspective to ask whether approved material was being used under the same conditions as when the application was originally qualified. That question linked production quality to material logistics and handling, without assuming the press had to change to solve every problem that became visible after printing.
Thinking Beyond the Obvious Does Not Require a Complicated Remedy
People often describe thinking outside the box as finding an unusual technical trick or creating an entirely new solution. In industrial troubleshooting, it can mean something more disciplined: questioning the investigation's boundaries.
In this case, the surface measurements and additional treatment trial were valuable. They explained part of the interface behavior and showed one way to improve robustness. But the expert did not confuse a successful improvement with a complete explanation of recurring failures.
He widened the investigation to include the material's journey before the press. An operator's observation supplied a previously unrecorded variable. A controlled comparison then established its effect on the result.
The solution was not innovative because conditioning is novel. It was innovative in the way the evidence was connected. The investigation moved beyond the subsystem where the problem appeared and identified a condition that ordinary, press-focused checks had not captured.
This is an important distinction. Creative troubleshooting is not random experimentation, and it does not mean changing a process simply because a different approach is possible. It means pursuing a recurring failure with a wider view, while using controlled evidence to decide which variable truly matters.
The Lesson for Printing Plants
When a technical problem returns despite apparently successful adjustments, teams should distinguish between three questions: what makes the product perform better, what caused the variation, and what must be controlled to prevent the failure from returning. Sometimes one corrective action answers all three. Sometimes it does not.
Improving surface preparation can be technically useful. But if an uncontrolled material-conditioning step drives the variation, more treatment may only widen the process margin while leaving the source of instability untouched.
A printing substrate is more than a commercial name, a technical data sheet, or a lot number. It has a manufacturing and storage history; it has been transported, staged, and exposed to physical conditions before reaching the press. For some applications, that history materially affects the outcome.
The same is true of the people involved in production. Operators may recognize timing or material-handling patterns that standard reporting systems do not collect. Their observations do not replace measurements, but they can identify what needs to be measured next.
A sound investigation turns those observations into testable hypotheses, validates the result under production-relevant conditions, and avoids extending the conclusion beyond the evidence.
Conclusion: The Answer Was Outside the Press
After weeks of testing adhesion, substrate properties, surface preparation, and primer performance, the plant identified an influential variable in a place that had not been central to its original investigation.
Rolls had been reaching the press in different thermal states even though, on paper, they were classified as the same approved material. Controlled comparisons showed that adequately conditioned facestock delivered more consistent adhesion results, while the accelerated material-staging route increased variation in the sensitive application.
The corrective action was to restore control of material preparation, not to introduce another change to an otherwise effective LEP printing process.
That is the principle behind thinking beyond the obvious. If a process is working correctly, there is no reason to invent a problem or redesign it for novelty's sake. But when a failure continues to return, the investigation must be willing to look beyond the system in which the symptom is observed and identify which condition is actually changing.
Expertise is not measured by how many press parameters we know how to adjust, but by our ability to identify which variable truly controls the result.
Sometimes the best way to solve a problem that appears on the printing press is to begin with what happened to the material long before it arrived there.
Author's note: This article is a freely adapted professional narrative inspired by "The Wrong Direction" in The Personal Journey of an Industrial Printing Expert. The case is illustrative, not a documented account of an identifiable customer or plant. The sequence and portrayal of the visiting expert have been adapted for this article. The described result should be verified for each material, press configuration, and application; it does not establish a universal material-level mechanism.