By Ronen Dolev | 2026
Playing cards: a small product with demanding engineering requirements
A deck of playing cards looks deceptively simple: fifty-two cards, graphics on both sides, a protective finish and a small package. Yet anyone who handles cards regularly recognizes the difference between a well-engineered deck and one that performs poorly. Some cards travel smoothly between the fingers, while others stick together. Some recover promptly after being bent; others remain curved. In one deck the edges and corners feel uniform, while in another the smallest cutting variations are perceptible.
The consequences extend beyond comfort. A slight change in the shade or positioning of a single card back may make that card recognizable during a game in which every back is expected to be indistinguishable. What would be a minor cosmetic defect on another printed product becomes a functional defect in playing cards.
Playing-card manufacturing therefore combines printing technology, paperboard engineering, coating chemistry, dimensional control, mechanical converting and quality assurance. Cards are handled repeatedly throughout their useful life: they are dealt, shuffled, bent, pressed, spread across tables and stacked again. Their printed layers must withstand this handling without making the product too stiff, too slippery or too resistant to movement.
The substrate must be rigid enough to hold its shape, yet sufficiently resilient to recover after bending. The coating must protect the image while also defining the friction between adjacent cards. The converting process must yield precisely cut, dimensionally consistent cards that form a complete deck. For that reason, engineering begins with the finished deck's performance, not simply the choice of printing press.
Playing-card applications and product families
Playing cards are not a single standardized product. Conventional Poker and Bridge decks emphasize repeated shuffling, fast recognition of suits and ranks, and a consistent reverse design. Magician cards may require particularly predictable handling, bending, and controlled movement between cards. Tarot cards are often larger and may carry complex graphics on a different board grade. Trading and collectible cards may incorporate specialized finishes and require both handling durability and long-term storage stability.
Application | Common dimensions | Principal requirements |
|---|---|---|
Poker playing cards | Approximately 63 × 89 mm | Regular dealing, repeated shuffling, uniform backs |
Bridge playing cards | Approximately 57 × 89 mm | Comfortable handling and consistent flexibility |
Magic playing cards | Often Poker size | Predictable bending, recovery and controlled card movement |
Tarot cards | For example, 70 × 121 mm | Large-format graphics, adequate stiffness and durability |
Trading and collectible cards | Often approximately 63 × 89 mm | Image quality, protection, embellishment and storage stability |
Promotional and customized cards | Defined by the product brief | Branding, versioning, personalization and fit-for-purpose handling |
These are familiar commercial dimensions, not mandatory measurements established by an international playing-card-size standard. Substrate weight and thickness also vary by application. A casino-style deck, for example, can require a different structure from an illustrated Tarot deck or a collectible card. The specification should therefore identify the intended use, card count, dimensions, stiffness, opacity, handling feel, security expectations and manufacturing volume before material selection begins.
The playing-card structure: more than printed paperboard
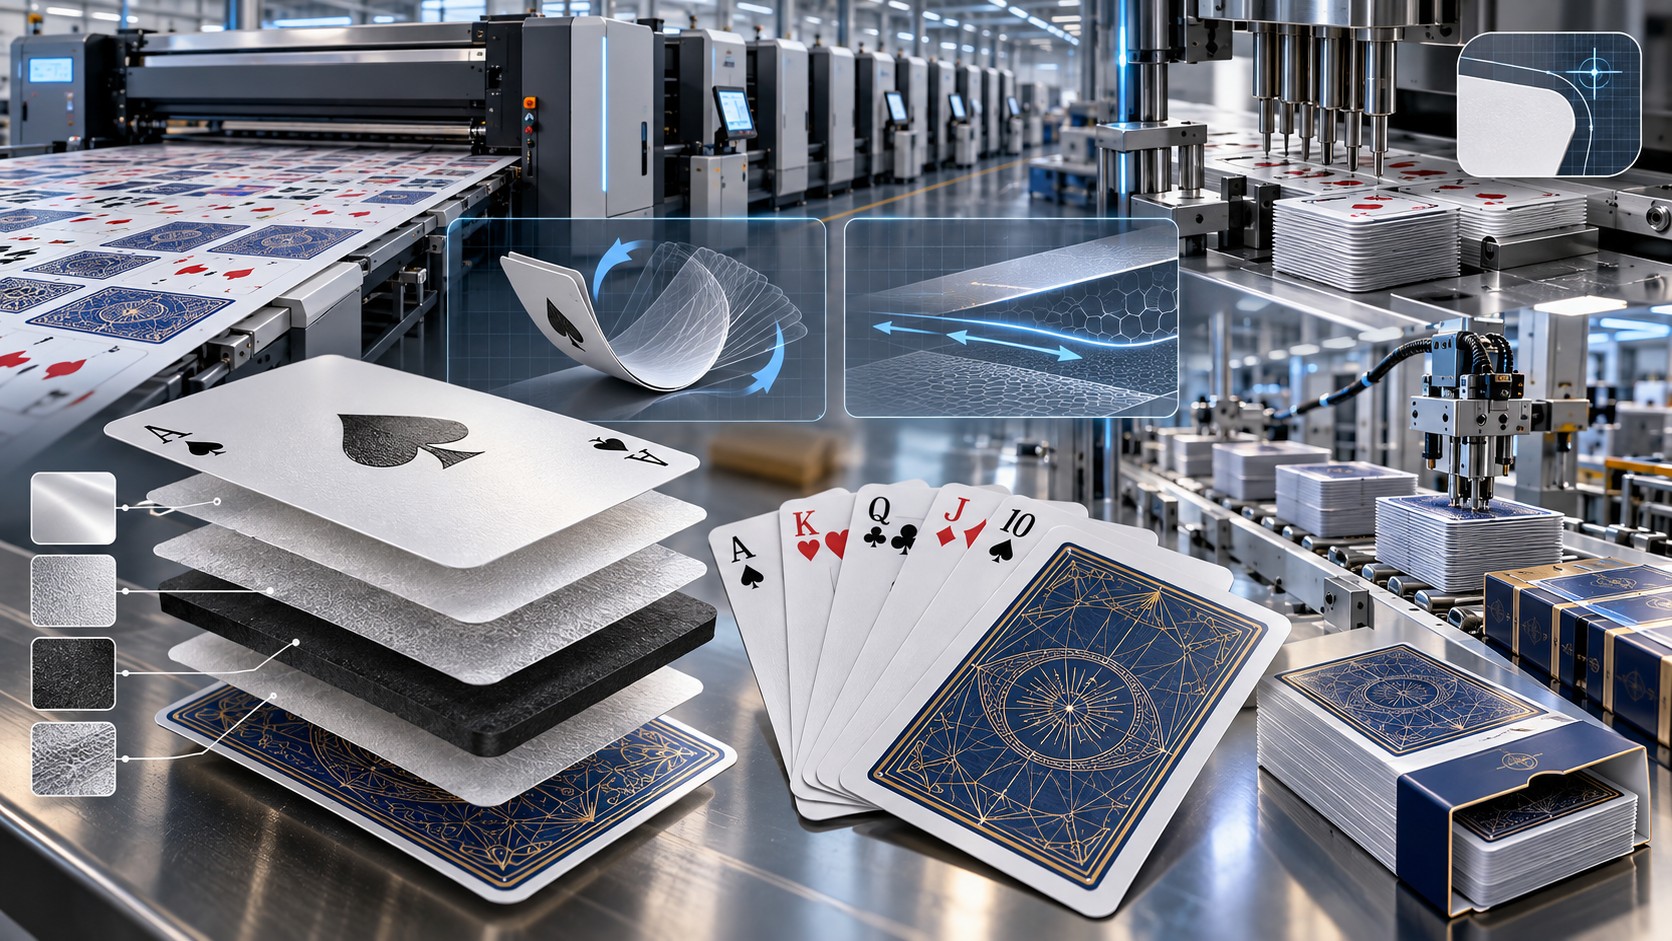
A paper-based playing card must meet optical, mechanical, and surface-performance requirements at the same time. A typical construction begins with a board suitable for printing on both sides. Some grades include an opaque or black core to reduce light transmission through the card. The two surfaces receive their respective images and protective functional coatings. In LEP applications, a primer may also be needed between the paperboard and the ink.
Layer or component | Function in the finished card |
|---|---|
Functional card coating, first side | Abrasion protection and controlled sliding behavior |
Printed ink, first side | Face graphics, ranks, suits and illustrations |
Primer, where required | Compatibility and adhesion between board and LEP ink |
Print-receptive coated surface | Smooth, consistent base for imaging |
Paperboard structure | Thickness, stiffness, strength, and bending recovery |
Optional black or opaque core | Reduced light transmission and better visual concealment |
Print-receptive coated reverse | Consistent base for back printing |
Primer and printed back image | Uniform back design and durable color |
Functional card coating, reverse. | Surface protection and controlled card-to-card friction |
This is a conceptual cross-section, not a universal bill of materials. The opaque core may be integrated into a multilayer board, the primer may be unnecessary on an approved substrate, and protective coatings may differ in chemistry. What matters is that both surfaces operate as a balanced structure. A significant mismatch between the two sides can contribute to curl, changes in hand feel, and uneven aging.
Black-core paperboard and optical security
Black-core playing-card board incorporates a dark interior layer to reduce light transmission. Its purpose is functional rather than decorative. In games where the face of a card must remain unknown, the ability to infer suits, ranks, or printed details through the reverse side can undermine fair play. An opaque structure helps prevent that information from being recognized under unfavorable lighting conditions.
Some commercial playing-card stocks are available at approximately 300–320 g/m² and use a dark central ply. The board's mass alone, however, does not guarantee opacity. Fiber composition, ply structure and density, pigmentation, surface coatings, and the black core itself all affect optical performance. Two boards of identical grammage may transmit very different amounts of light.
A standard opacity measurement provides useful material information, but a security-sensitive deck also requires inspection of the actual printed construction under relevant lighting. A card can meet a basic opacity specification and still display an unwanted visual difference in a particularly demanding application. Opacity and concealed-image resistance must therefore be evaluated on the finished card, rather than inferred from thickness alone.
Grammage, caliper and stiffness are different properties
Grammage, commonly expressed as grams per square meter (g/m² or GSM), is frequently the first property used to compare playing-card boards. But it does not fully describe handling performance. Two boards weighing 310 g/m² can have different calipers, densities, fiber structures, and bending behavior. A more compact board may respond differently from one with a bulkier construction, even though both have the same mass per unit area.
The engineer needs to consider grammage alongside caliper, density, bending resistance, elastic recovery, and the failure behavior observed after repeated handling. A card should not simply be made as difficult as possible to bend. Excessive rigidity can make shuffling awkward; insufficient stiffness can make the deck feel weak and unstable. The right balance depends on the intended application, fiber direction, and the finished coating system.
Grain direction and the mechanics of bending
Paperboard is anisotropic: its mechanical properties need not be the same in every direction. During paper manufacture, some fibers tend to align along the machine direction (MD). The cross direction (CD) is perpendicular to it. Differences between MD and CD affect bending resistance, dimensional response to moisture, and how a card recovers after being flexed.
Playing cards are repeatedly bent and released, particularly during shuffling. A poorly chosen relationship between grain direction and card geometry can produce noticeably different bending resistance along the two axes. It may also affect long-term recovery and the way a deck behaves in the hand.
Consequently, grain direction must be considered during sheet imposition. Maximizing the number of cards on a press sheet is not sufficient if the resulting orientation undermines the required mechanical behavior. Verify the grain direction for the selected board and align it with the production brief, ideally through physical comparison of the finished card in its intended use. Record it as part of the substrate specification, not as a converting convenience.
Dynamic snap: stiffness combined with recovery
One of the distinctive properties of a playing card is its dynamic snap: the way the card bends under load and responds when that load is released. A good card exhibits an appropriate combination of resistance, elasticity and recovery. It can flex during handling without remaining permanently distorted after the stress is removed.
Dynamic snap is not the same as stiffness alone. A very stiff card may feel unpleasant in a shuffle. A card that bends with almost no resistance may feel too soft or may lose its form rapidly. The desired response lies between these extremes and is influenced by the board's elastic properties, caliper, ply construction, grain direction, moisture content, and coatings.
No universal numerical dynamic-snap value can be assigned to every playing-card design. Results depend on the testing apparatus, specimen dimensions, loading direction, conditioning and evaluation method. A manufacturer must therefore define its own controlled acceptance window using a representative reference deck and a repeatable testing procedure.
Measuring dynamic snap rather than relying on feel alone
Experienced operators can often identify a substantial difference in card response by hand. Manual bending, spring-back, and shuffle trials provide useful qualitative feedback, especially during material development. Yet they are not sufficiently reproducible on their own for a robust industrial specification.
Instrumented bending-resistance testing, cyclic bending, and recovery measurements can provide comparable numerical results when the method is defined. Direction, angle or displacement, loading rate, recovery time, and cycle count must remain consistent. Testing in both grain-related directions is especially informative. The same sample may need to be evaluated before and after humidity conditioning, because moisture changes the mechanical response of paperboard.
The key question is not merely whether a new card resists bending. It is whether its resistance and recovery remain within an acceptable range after repeated, realistic handling. The finished, coated card—not just the unprinted raw sheet—is the relevant test object.
Moisture content and environmental conditioning
Paper and paperboard are hygroscopic. They absorb and release moisture in response to ambient conditions, and those changes influence mechanical performance and dimensions. Excessively dry material can become more vulnerable to cracking or irreversible deformation; material with higher moisture content may lose some rigidity and feel softer.
Humidity differences may also create sheet curl, dimensional movement and registration difficulties in two-sided printing. These effects are particularly relevant when the production process includes printing, coating, cutting and stacking in separate areas of a plant. Condition materials in a controlled pressroom environment, and have the manufacturer document how long packaged stock needs to equilibrate before use.
A temperature around 21–24°C and relative humidity near 50% can serve as a practical starting environment for some paper-based playing-card workflows, but these figures do not replace the substrate supplier's specification. Consistent conditions matter more than treating a single set point as universal. Finished-card testing should reflect both manufacturing conditions and the climate in which the product will be used or stored.
Smooth, glazed and embossed surface finishes
The surface texture of playing-card stock affects a deck's tactile character. A smooth or glazed surface can provide one type of contact, while an embossed finish—often described commercially as a linen finish—introduces a micro-topography that changes how neighboring cards touch and slide.
An embossed surface may affect perceived grip, separation between cards, and air movement during shuffling. Neither smoothness nor embossing is inherently superior. The correct surface depends on the desired style of play and the functional coating applied afterward.
Surface texture also affects printability. A pronounced embossing pattern introduces peaks and valleys that can change ink contact, coating distribution, and fine-detail quality. Rougher surfaces may require different pre-print preparation or primer application. Therefore, the choice of finish should be qualified through printing, adhesion, coating, and actual shuffle testing—not selected solely by appearance or visual texture.
Prepress: two sides that must align precisely
Playing cards are typically printed on both sides. The face contains ranks, suits, figures, or specialized illustrations. The reverse generally uses one common design for every card in the deck. The back creates a particularly stringent quality requirement: each card must look indistinguishable from the others when placed face down.
A small difference in image position, border width, tint or local uniformity can become a recognizable mark. In a competitive game, what looks like an insignificant print deviation may compromise the function of the deck. Prepress must therefore control front-to-back registration, symmetry, trim position, print variation, and the relationship between design elements and the cutting tool.
A symmetric card-back design can reduce the visual impact of rotation and some alignment differences, but symmetry does not eliminate the need for manufacturing accuracy. Monitor back-side color uniformity across the sheet and throughout the production run. Trim tolerances should be considered when choosing border widths, especially when the artwork contains narrow, high-contrast lines near an edge.
Bleed, safe areas and cutting registration.
The prepress file must define bleed around each card so that minor trimming variations do not expose unprinted edges. A 2 mm bleed can be a useful starting arrangement for certain sheet-fed card-cutting systems, but the required value must be confirmed with the equipment and tool design. Bleed and safe area have different purposes: the former extends background artwork beyond the nominal cut; the latter protects meaningful content from the cut path.
Registration marks, slitting marks and front-to-back alignment references must be positioned for the actual converting line. Where needed, marks can be printed on the reverse and at sheet edges so that sensors and operators can control slitting accurately. Fine borders need special attention: even a small trim displacement can look substantial on a narrow card-edge graphic. The final proof should therefore be evaluated against the intended cutting tolerances, not only as a flat printed image.
Imposition: deck composition and grain direction on the same sheet
Industrial production benefits from arranging multiple cards on a single press sheet. On a nominal B2 sheet of approximately 750 × 530 mm, certain production layouts can accommodate roughly 55 Poker- or Bridge-format cards, depending on the actual printable width, bleed, tool clearances, and cutting arrangement.
But imposition is more than a sheet-utilization calculation. It determines grain orientation, alignment of front and reverse artwork, how rows are slit, and the collection sequence after cutting. The converter may require cards to be arranged in a specific order so that the finishing line automatically assembles an accurate deck. Jokers, instruction cards, and supplementary pieces must also be accounted for.
The intended deck composition should be reconciled with the layout before printing starts. A standard 52-card playing deck may also contain additional Jokers or information cards, depending on the commercial specification. The workflow must guarantee that the conversion and collection equipment ultimately delivers the correct number and sequence of cards, without unwanted duplicates or omissions.
Printing technologies: conventional offset and LEP
Conventional offset has long been widely used for playing-card printing, especially in substantial production volumes. Digital liquid electrophotography (LEP) provides another manufacturing path, particularly attractive for shorter editions, multiple artwork versions, personalized decks, prototypes, and collector or promotional releases.
Comparison | Conventional offset | LEP digital printing |
|---|---|---|
Typical commercial strength | Efficient for high-volume repeat production | Flexibility in short and medium runs and multiple versions |
Variable artwork and personalization | Requires an appropriate hybrid or additional process | Digital data can change from sheet to sheet |
Substrate compatibility | Depends on press, ink, and board grade | Depends on press, transfer mode, substrate and primer |
Color management | Calibration and process control required | Calibration and process control required |
Finished-card durability | Determined by materials, printing and coating | Determined by materials, printing and coating |
Converting requirements | Accurate trim, coating and deck assembly | The same downstream accuracy and mechanical qualification |
No technology automatically produces a longer-lasting card. Wear resistance, sliding behavior and resilience come from the combined substrate, ink, coating and converting process. The commercial choice should consider run length, variation, quality requirements, total finishing cost and qualification of the complete application.
LEP printing and ink-transfer architecture
LEP creates the image through an electrophotographic process and transfers a thin polymer-based ink layer to the substrate through a controlled intermediate-transfer system. For playing cards, ink-to-board adhesion matters, but so does the interaction between the printed image and the functional coating applied afterward.
Some LEP platforms can operate in different transfer architectures. In a Multi-Shot process, color layers are transferred to the substrate in separate steps. In a One-Shot process, the color layers are assembled on the intermediate transfer surface and transferred together. The latter approach can reduce some sources of intercolor misregistration, while the former may behave differently on certain paper grades and with different surface preparation.
Neither architecture can be declared categorically superior for every playing-card construction. The choice depends on the press capability, material grade, image demands, substrate transport and adhesion performance. Press-specific ink separation sequences, calibration practices and transfer parameters should follow the qualification for the installed equipment rather than being assumed interchangeable.
When is a primer needed for LEP?
A primer is an engineered interface between the playing-card surface and the polymer-based ink. It can improve wetting, transfer, and adhesion, but it is not automatically necessary on every paperboard. Some materials are prepared at the mill, and others can perform adequately without an additional coating under a given LEP transfer mode.
One-Shot workflows can be more dependent on qualified primer/substrate combinations, while certain Multi-Shot workflows may show good initial adhesion on selected paper grades without a separate primer. Neither observation should replace testing. The proper decision is based on actual ink adhesion, transfer performance, and the condition of the printed product after protective coating, cutting, and repeated shuffling.
Primer may be applied inline, offline or through a suitably pretreated board, depending on the press and substrate. Its chemistry, dry coat weight and time between coating and printing must remain within a qualified window. Excessive primer is not necessarily beneficial: too much may introduce drying or blocking difficulties, while too little or poorly distributed primer may leave weakly bonded regions. The evaluation must include the full printing and finishing system.
Embossed stock and the limits of inline priming
Pronounced embossed or rough surfaces create an additional challenge. An inline priming unit that meters a relatively low coating weight through an anilox roller may not deposit sufficient primer into every part of the surface topography. The problem is not necessarily the primer chemistry; the coating system may simply be unable to achieve adequate coverage on that surface.
In such a case, an offline application method qualified for the board and primer may provide better control. Increasing the primer setting beyond the equipment's practical coating capacity is not a reliable solution. The objective is uniform ink adhesion while preserving the desired surface texture, board flexibility, and handling characteristics. Verification must follow through to coating and bending tests of the printed cards.
Color management: the back of the card is a functional feature
A modest color variation may be acceptable on some printed products. On the backs of playing cards, it can make a particular card recognizable. Color consistency is therefore not merely a brand requirement but an element of functional uniformity and, in some applications, game integrity.
A suitable control plan needs to define viewing conditions, measurement conditions and an approved color target. It must monitor consistency across the sheet, between sheets and over the full run. Particular attention should be given to large, uniform back designs in which local changes in hue or density become visible.
LEP platforms can use calibration and process-control functions appropriate to their hardware. Yet even well-controlled average color values do not guarantee that every card back will look the same. Local uniformity, registration, edge borders and the optical effect of the final coating must also be checked. Final color approval should be performed on the finished coated construction, not solely on an unvarnished print.
Optical density, tonal response and ΔE00
Optical density measurements can help monitor aspects of ink laydown, while tonal response and tone value increase (TVI) can characterize print behavior when the control method is appropriate for the technology. Spectral measurements and color-difference metrics such as ΔE00 provide another way to compare a printed card with a reference target.
No universal optical-density value automatically qualifies all playing cards. Targets depend on the board, ink system, print condition, and finish. The manufacturer must specify measurement mode, illumination, and viewing requirements. Where the two sides of a card have different coating structures, it may be necessary to evaluate them separately.
The goal is stable, repeatable production with no detectable, unauthorized distinguishing marks on card backs. This requires both instrumental evidence and visual examination under agreed conditions.
Functional varnishing: where print protection meets playability
On many printed products, varnish primarily changes gloss and protects against scuffing. For playing cards, its role is more fundamental. It determines much of the sliding behavior between adjacent cards and significantly influences the hand feel of the deck.
A varnish that performs exceptionally well in a flat-sheet rub test may still make a deck difficult to shuffle if friction is too high. Conversely, a coating with very low friction may cause uncontrolled sliding, making cards difficult to handle. The coating must balance abrasion resistance, ink protection, flexibility, and a desired level of controlled slip.
The appropriate coating is not simply the hardest or glossiest formula. It is the one that enables the finished cards to separate, move, stack and withstand repeated use with the intended tactile response. Selection should therefore include card-to-card friction measurements, shuffle trials, scratch and scuff tests, and examination of the coated cards after mechanical flexing.
Static and kinetic coefficient of friction
The coefficient of friction (COF) relates sliding resistance to the normal force between contacting surfaces. Static COF addresses the resistance that must be overcome to initiate relative motion; kinetic COF characterizes resistance once the surfaces are already moving. Both can influence card handling.
High static friction can cause cards to cling together and resist separation during a deal. Excessively low kinetic friction can make the deck feel unstable and prone to slipping from the hand. The useful range depends on the intended style of play, surface texture, coating chemistry, application weight and conditioning.
For that reason, no single mandatory COF value applies to all playing cards. A manufacturer should develop a reference range using the chosen material, an agreed measurement method and a set of performance trials. Measurements should be performed on finished cards after the coating reaches its representative condition and under documented temperature and humidity.
Coating effects on dynamic snap and curl
A varnish adds material to the card structure and can change the way the board flexes. Depending on its chemistry, thickness, and modulus, it may add stiffness or create internal stresses. Coating only one side—or coating the two sides to different weights—can also contribute to curl through an imbalance of moisture, shrinkage, or mechanical response.
A card that feels excellent before coating may respond differently afterward. Therefore, repeat flexibility and recovery tests on the finished construction. Surface protection should not come at the expense of resilience, and the coating process must not disturb the card's two-sided balance. Rather than maximizing dry coat weight, the aim is to find the lowest qualified coat weight that delivers the required protection and playability.
Water-based and UV-curable playing-card coatings
Both water-based and UV-curable systems can be formulated for playing-card applications. Evaluate each as a specific product rather than through broad assumptions about its chemistry.
Attribute | Water-based coating | UV-curable coating |
|---|---|---|
Film formation | Water removal and formulation-dependent development | Photochemical cure |
Abrasion and scuff resistance | Depends on the formulation | Depends on the formulation |
Controlled friction | Achievable with a suitable playing-card grade | Achievable with a suitable playing-card grade |
Flexibility | Depends on polymer chemistry and coat weight | Depends on chemistry, cure and coat weight |
Curl risk | Affected by moisture, drying and two-sided balance | Affected by cure shrinkage, stiffness and balance |
Required verification | Shuffling, COF, adhesion and wear | Shuffling, COF, adhesion and wear |
It would be incorrect to claim that water-based varnish is always more flexible or that UV coating is always more abrasion resistant. The result depends on the particular formulation and the full application process. A grade developed specifically for playing cards is a sensible starting point, but qualification is still needed on the final printed board.
Surface treatment before coating LEP prints
When a functional varnish is applied over LEP ink, the printed surface must support appropriate wetting and interlayer adhesion. Certain systems benefit from controlled corona treatment after printing and before varnishing. Surface treatment can change the surface properties of the polymeric ink layer and make it more receptive to coating.
A wetting-tension range of approximately 40–44 dyn/cm is sometimes used as a starting evaluation target for selected LEP/coating combinations. It is not a mandatory target for every varnish or press platform. The correct level must be established through coating-specific wetting, adhesion, and durability trials.
More aggressive treatment is not automatically better. Excess treatment can negatively affect the printed surface or a subsequent interface. Surface preparation should be controlled, measured where appropriate, and validated by testing the coated card after realistic handling.
Drying, curing and the final shuffle feel
The friction and durability of a coating may continue to change until the film has properly dried or cured and its properties have stabilized. A deck tested immediately after coating may behave differently after storage. Water-based varnishes require sufficient drying and appropriate film development; UV systems require a degree of curing suited to the chemistry and intended use.
A surface that feels dry to the touch is not, by itself, proof that the coating has reached its final characteristics. Consequently, the manufacturing specification should define any required conditioning or waiting period before friction and durability testing. It should also control the thermal load imposed on the paperboard, since moisture changes can alter stiffness, flatness, and the card's response during shuffling.
Slitting, punching and corner quality
After printing and coating, the sheets must be converted into individual cards. Dedicated finishing lines may combine directional slitting, card collection, stack formation and a final punch that forms the finished outline and rounded corners.
Rounded corners are not merely decorative. They influence tactile comfort, reduce the presence of sharp edges, and affect how cards move between fingers during play. Variations in corner radius, burrs, ragged fibers, or edge delamination can quickly become apparent when a deck is used repeatedly.
The converting process must preserve the ink and coating at the cut edge. A cutting tool that fractures a coating, pulls fibers or causes ink lift can undermine the performance of a correctly printed sheet. Tool condition, pressure, alignment, registration and waste removal must therefore be part of the product qualification. Inspection should include edge cleanliness, final card dimensions and consistency between cards from different positions on the same sheet.
Cutting accuracy as part of card integrity
A playing deck depends on the apparent interchangeability of its cards. A small dimensional difference, unusual corner, or inconsistent border can make a card recognizable. In applications requiring strict impartiality, cutting quality therefore has security implications as well as aesthetic and handling consequences.
The manufacturer should measure height, width, corner radius, and edge quality across the finished deck. A comparative inspection of card backs is particularly important. The goal is to prevent individual cards from being distinguished unintentionally by sight or touch. Review trim accuracy alongside prepress border design, because the two determine the visible result.
Cut, stack, collate and wrap: converting sheets into complete decks
Once slit, the cards must be collected in the intended order. In an integrated line, a press sheet may first be slit in one direction, then rotated for further cutting and separation. Individual card stacks are collected, aligned, and combined before final punching. The deck is then wrapped and, where required, inserted into a folding-carton box.
The collection sequence must match the imposed layout. A deck missing one card or containing a duplicate is defective, even when every card is perfectly printed. Quality control must verify the deck composition, count, and orientation. Automated inspection and counting can reduce the likelihood of missing, duplicated, or misplaced cards, but they must be validated against the product definition.
Wrapping also needs appropriate control. Excessive tension or uneven pressure may distort a deck, while inadequate packaging can expose it to moisture and damage during distribution. Depending on the product, the finished deck can be overwrapped with transparent film, enclosed in a paper band, or placed directly into an engineered carton. The packaging must protect flatness and keep the deck intact until the consumer opens it.
A finished-deck quality-assurance plan
You can't certify playing-card quality at the press exit alone. The quality plan must follow the product from raw board through printing, coating, mechanical conversion, and final packaging.
Production stage | Principal checks | Engineering objective |
|---|---|---|
Raw board | Grammage, caliper, moisture, opacity, bending behavior | Qualified mechanical and optical base |
Grain direction | Bending response in MD and CD | Appropriate stiffness and recovery |
Primer, where applied | Coating consistency, wetting and ink adhesion | Reliable LEP printing interface |
Printing | Color, registration, back uniformity and adhesion | Consistent and secure graphics |
Varnishing | Static and kinetic COF, scuff, cure/dryness | Controlled handling and protection |
Dynamic snap | Bending, recovery and repeat-cycle response | Long-term resilience |
Slitting and punching | Dimensions, corners and edge integrity | Interchangeable finished cards |
Stacking and collation | Count, sequence, alignment | Complete, accurate decks |
Packaging | Wrap integrity, compression and flatness | Protection in distribution |
Finished deck | Shuffle feel, sliding, appearance and repeated handling | Demonstrated application suitability |
Material and process variability must be considered. Changes between board lots, humidity conditions, or varnish batches can alter the finished feel even when the printed image remains within color tolerances. Document results at representative production speeds and with sufficient samples across the run. A good prototype is useful, but it does not by itself establish the process capability of a commercial production line.
Relevant standards and measurement methods
No single ISO standard defines all quality requirements for every style of playing card. The practical approach is to use established measurement methods for paperboard and printing, then add application-specific limits for dynamic snap, shuffle feel, appearance, and card-to-card consistency.
Standard | Measurement scope | Relevance to playing cards |
|---|---|---|
ISO 187:2022 | Standard atmosphere for conditioning and testing paper and board | Comparable tests under documented conditions |
ISO 536:2019 | Grammage of paper and board | Incoming-board mass consistency |
ISO 534:2011 | Thickness, density and specific volume | Structural characterization |
ISO 2471:2008 | Opacity by the paper-backing method, within its scope | Optical assessment of opaque stock |
ISO 15359:1999 | Static and kinetic friction of paper and board | Sliding behavior of card surfaces |
ISO 2493-1:2010 | Bending resistance using the constant-rate-of-deflection method | Material bending characterization |
ISO 287:2017 | Moisture content of a lot of paper and board | Moisture control and comparability |
ISO 13655:2017 | Spectral measurement and colorimetric computation | Printing color evaluation |
These methods should not be confused with universal acceptance specifications. ISO 15359 provides a measurement approach; it does not prescribe the ideal playing-card COF. Likewise, bending-resistance testing does not establish one universal dynamic-snap target or replace a defined cyclic-recovery method. Poker and Bridge card dimensions are commercial conventions and should not be attributed to ISO 216, which addresses paper-size series rather than playing-card dimensions.
Troubleshooting: when the printing is good, but the deck performs poorly
Many playing-card defects are not apparent when inspecting a printed sheet. They only become visible after coating, converting, or repeated handling. A systematic investigation must identify the process stage and interface where the failure first appears.
Symptom | Potential mechanism | Investigation and corrective direction |
|---|---|---|
Cards stick together | High COF, blocking or incompletely stabilized coating | Evaluate varnish, drying/cure and storage conditions |
Cards slide uncontrollably | COF too low for the intended feel | Requalify coating chemistry, coat weight and texture |
Cards retain curl | Unbalanced layers, moisture change, or board structure | Examine two-sided coating balance, humidity and grain |
Poor dynamic snap | Inadequate board recovery or bending response | Review board construction, caliper, and fiber orientation |
Ink wears or lifts during shuffling. | Weak ink/primer interface or poor varnish adhesion | Identify the failure interface and requalify adhesion |
Varnish cracks during flexing | Excessive coating stiffness or thickness | Adjust the selected system and dry coat weight |
Card backs vary visibly. | Local color differences, registration or coating variation | Control color uniformity and finishing consistency |
Borders vary between cards. | Printing-to-cutting misalignment or trim drift | Check imposition, registration, and conversion settings. |
Corners fray or break down. | Tool condition, punching geometry, or weak board edges | Inspect die/punch tooling and board specification |
Face content is visible from the reverse | Inadequate board opacity | Reevaluate black-core construction and light transmission |
Missing or duplicate cards | Collation, counting, or collection error | Verify collection order and deck composition |
Feel changes after storage. | Moisture movement or continuing coating development | Control conditioning, cure, and package environment |
A deck that sticks during shuffling does not automatically need less varnish. The problem may be the coating chemistry, insufficient drying, excessive blocking, or a poorly controlled static-friction response. Similarly, persistent curl does not automatically require a heavier board: check moisture, imbalance between the two coated surfaces, and grain direction first.
If printed ink lifts during handling, first locate the failure interface: ink to board, ink to primer, or coating to ink. If dynamic snap is unsatisfactory, distinguish insufficient stiffness from poor elastic recovery. If the card backs vary in appearance, examine registration, local color uniformity, and varnish before changing global color targets.
Increasing coating weight does not guarantee better durability. Increasing board thickness does not guarantee better recovery. Adding more primer does not necessarily correct adhesion. Each change should respond to an identified physical mechanism and be validated on the finished deck through controlled comparisons.
Conclusion: playing-card quality is measured in the hand
Manufacturing playing cards is an end-to-end engineering process that combines paperboard construction, color reproduction, surface chemistry, and precision conversion. The board supplies the mechanical foundation. An opaque core helps prevent unwanted transmission of visual information. Grain direction influences bending. Printing creates the graphics. When needed, primer provides a stable interface. Functional varnish protects the artwork and establishes controlled friction. Slitting, punching, collation, and wrapping turn the printed sheets into a complete deck.
All of these operations serve a common purpose: producing cards that look, feel, and behave consistently. LEP printing makes it possible to create customized, short-run and versioned decks with considerable graphic flexibility, but the printing technology is only one component of the application. Performance is demonstrated after coating, cutting, and repeated real-world handling.
The printing press creates the image. The board engineering, functional coating, and converting process make it a playing card. Ultimately, quality is not measured only by print sharpness or registration accuracy. It is experienced when a player lifts the deck, shuffles the cards, and finds that each one slides, bends, and returns just as expected.