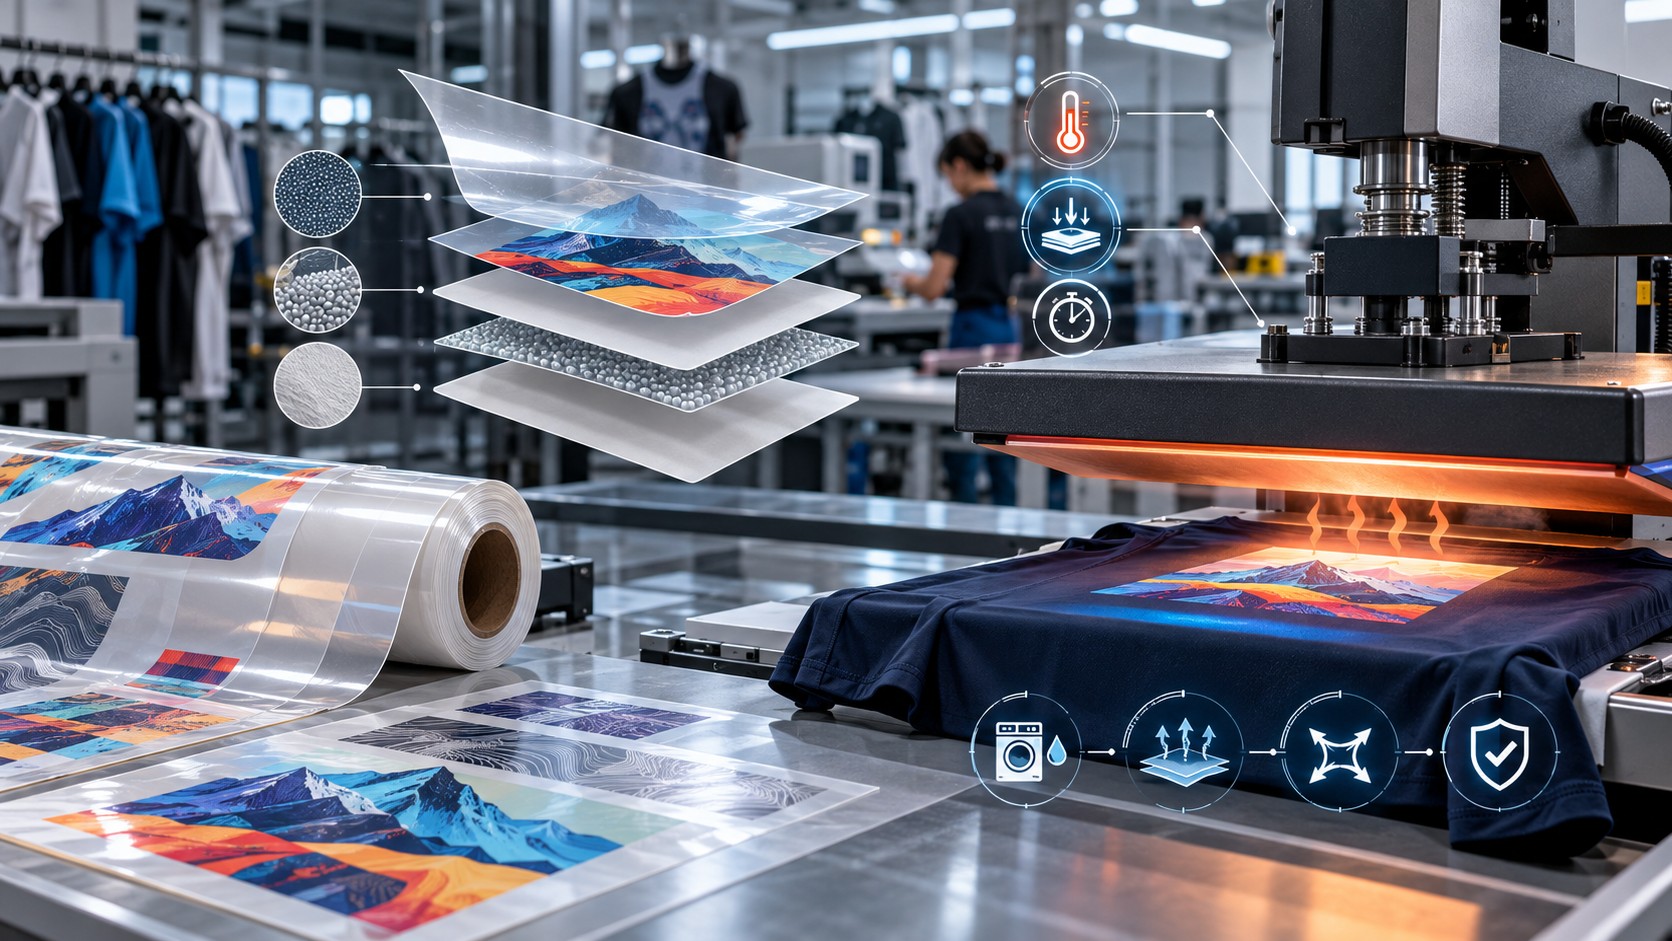
When printing is not meant to remain on its original substrate
Most industrial printing applications are designed around a permanent bond between ink and the material it is printed on. Labels, packaging films, cartons, and many other printed products are expected to retain their image on the original substrate throughout their service life.
Heat transfer printing reverses part of that logic. The image is initially produced on a temporary carrier, yet the intended finished product is a garment. The printing system must therefore remain stable through printing, registration, coating, and handling, then deliberately release the graphic when heat and pressure are applied. At the same time, the transferred structure must establish a durable bond with the textile.
These requirements involve two interfaces with very different functions. The interface with the carrier must provide temporary retention followed by controlled release; the interface with the garment must provide long-term adhesion despite bending, stretching, perspiration, and repeated laundering. The printed colors, backing layers, functional coatings, and thermal adhesive must perform as one construction.
A crisp graphic on the carrier is only the starting point. The real qualification happens after Transfer to the garment and after exposure to the mechanical, thermal, and chemical conditions the garment will encounter in use.
The application and the products it serves
Heat Transfer Labels for Garments are printed or coated constructions transferred from a temporary substrate onto a textile through a controlled thermal process. Applications include athletic jerseys, player names and numbers, logos, fashion graphics, workwear identification, cap graphics, internal neck labels and promotional garments.
The graphic can be manufactured independently of the garment and applied at a separate facility or production stage. This separation supports short runs, multiple garment sizes and colors, personalized names and numbers, and more efficient management of variable designs. Digital imaging is especially useful where many versions or complex multicolor artwork are required.
Nevertheless, the same transfer construction will not necessarily perform the same way on cotton, polyester, stretch fabrics, or garments with functional textile finishes. Fabric chemistry, surface texture, elasticity, and dimensional changes during washing all affect the final bond. Product development must therefore begin with the intended fabric and use conditions, not solely with the required visual appearance.
Heat transfer is not the same as dye sublimation.
Heat transfer and dye sublimation are sometimes discussed as if they were interchangeable. Their physical structures are different. In dye sublimation, selected dyes are transferred under suitable thermal conditions and diffuse into compatible polymeric fibers, most commonly polyester. In a multilayer heat transfer label, inks, backing coatings, and a heat-activated adhesive form a distinct construction attached to the textile surface.
This distinction matters most for garments previously decorated or colored by sublimation. Under the heat used to apply a new transfer, some dyes already present in the fabric can become mobile. They may migrate into the newly applied graphic, altering its appearance. This is dye migration, and it can happen even when the original graphic was printed and transferred correctly.
A white image on a red sublimation-dyed polyester jersey, for example, may gradually develop a pink cast. This is not necessarily a printing color-management problem; it may be a diffusion problem that requires a suitably designed barrier within the transfer construction.
Hybrid Transfer and Print-and-Cut Transfer
Two common production approaches are Hybrid Transfer and Print-and-Cut Transfer. Both can yield useful products, but they differ in the degree of control provided over individual functional layers.
Attribute | Hybrid Transfer | Print-and-Cut Transfer |
|---|---|---|
Production concept | Initial printed image followed by functional coating or screen-printing steps | Printing followed by cutting and transfer, as supported by the media system |
Additional layers | May include white backing, clear binder, anti-migration barrier, and adhesive | Often relies on a predefined transfer-media construction. |
Process complexity | Greater; several printing and curing interfaces | Generally simpler, depending on the system |
Formulation flexibility | Individual layers can be tailored to textile and durability demands | Limited by the approved media and Transfer construction |
Typical use | Industrial or performance-oriented garment decoration | Promotional and other applications where the system meets the required durability |
Neither approach has a universally guaranteed wash life. Performance is determined by the specific carrier, inks, coatings, adhesive, textile, and heat-transfer cycle. The remainder of this article focuses on the multilayer engineering of Hybrid Transfer, where each functional layer can be evaluated separately.
The functional layer structure
A typical hybrid construction is built on a temporary carrier, usually PET, with a controlled-release system. A print-receptive layer or primer may be present above the release coating. The graphic is printed, followed by optional white backing, dye-migration barrier, a functional clear layer, and a heat-activated adhesive.
Layer | Primary engineering function |
|---|---|
PET carrier | Provides mechanical support and positional stability during production |
Release coating | Retains the construction temporarily and enables controlled separation |
Print-receptive coating/primer | Establishes the required imaging interface where applicable |
Printed color layers | Produces the design, tone and detail. |
White backing | Improves opacity and color appearance on dark garments |
Anti-migration barrier | Limits dye transfer from selected textile constructions when required |
Functional clear or binder | Supports layer cohesion and compatibility with the adhesive |
Heat-activated adhesive | Establishes the final attachment to the garment |
Not every design requires every layer. Some clear formulations also perform an adhesive function; others separate the two functions. An anti-migration layer is unnecessary where dye migration is not a relevant risk. The engineering task is to use only the layers required to satisfy appearance, comfort and lifetime performance, while ensuring compatibility at every interface.
PET carrier selection and dimensional stability
The temporary carrier must withstand printing, screen-finishing, drying, conversion and the final transfer operation. Oriented PET films, including BOPET, offer a useful combination of strength, dimensional stability and thermal performance. Yet a PET film is not dimensionally invariant.
Heat can relax stresses introduced during film production, and subsequent dimensional changes can become critical in a multilayer process. Even a small expansion or contraction can cause misregistration between the printed image, the screen-applied white, and the adhesive outline. Differences between machine direction and transverse direction also matter.
Carrier selection must cover film thickness, flatness, coating uniformity, transport behavior, and response to repeated thermal exposure. A film that prints well but changes size during the screen-finishing stage does not qualify for the full application.
The release coating: temporary adhesion by design
The release coating is among the most distinctive features of the application. During printing and intermediate finishing, the graphic must remain sufficiently attached to the carrier to survive handling and registration. During final Transfer, the balance changes: the garment-side adhesive must establish the stronger functional bond, allowing the carrier to be removed without damaging the graphic.
Release systems are formulated for different removal conditions. Some are designed for cold peeling, after the transferred construction has cooled. Others are designed for warm or hot peeling. These methods are not interchangeable unless the complete material system has been qualified for both.
Removing a cold-peel carrier too early may lift color or functional layers. Conversely, delaying separation in a construction designed for hot peeling may produce a different failure mode. The specified peeling temperature, speed, and direction are therefore process parameters, not operator preferences.
A conventional tape-peel test on the unreleased carrier may be misleading: a system intentionally designed to release can transfer material to the tape without indicating a defect in the final textile bond. Testing must reflect each interface's intended function.
Preconditioning before printing
For applications that demand accurate registration between digital imaging and subsequent screen printing, thermal stabilization of the carrier can help. A controlled preconditioning cycle may relieve part of the film's residual orientation stress before precise images and registration marks are created.
For certain qualified films, a development trial around 130°C–140°C for one to two minutes may be considered. This is a material-specific experimental starting point, not a universal conditioning recipe. The film and release-coating manufacturer must establish the permitted thermal limits. Excessive temperature, uneven heating, or unsuitable infrared exposure can cause the deformation that conditioning was intended to prevent.
The practical validation method is to measure dimensions and printed reference distances before and after conditioning, then again after subsequent drying and screen-printing steps. The objective is not maximal heat exposure; it is predictable final geometry within the agreed registration tolerance.
Environmental control and acclimation
Production-room conditions affect handling and registration. Temperature, relative humidity, storage time, and tension history can influence both the carrier and some coating systems. Controlled ambient conditions, for example, approximately 21–24°C and 50–60% relative humidity in an approved process, can provide a useful starting point, but the correct values must be established for the actual materials and equipment.
It is also important to distinguish room conditions from the stored material's temperature. A film moved from a cold warehouse into a warm production area may require acclimation before printing. Stable storage and consistent handling reduce batch variation and help preserve alignment through the E2E process.
Mirrored artwork and prepress engineering
In transfer constructions where the printed side faces the garment during application, the artwork is printed in mirror orientation so that the finished image reads correctly after release. Mirroring, however, is only one element of prepress preparation.
The file must also define the separation order, white backing, adhesive contour, and the positional references used by downstream equipment. Registration marks should be placed where all relevant machines can detect them reliably. The feed direction and reference edge must remain consistent through printing and screen-finishing.
An artwork file that looks perfect on screen can still produce white halos or exposed adhesive if the functional-layer outlines aren't engineered to match the production line's achievable registration.
Registration between digital printing and screen printing
Hybrid Transfer often combines two fundamentally different imaging processes. The main graphic is produced on a digital printing press; functional layers are subsequently applied on a screen-printing machine. The processes must share a consistent positional and dimensional reference.
A fixed placement error can often be corrected by registration adjustment. A scale error requires a dimensional correction. A nonuniform distortion along a sheet or roll cannot always be corrected by a simple X/Y offset. For that reason, it is useful to print reference targets or a measurement grid and to record scale changes after the film passes through heating and coating stages.
Address the underlying deformation first. Repeatedly shifting the screen image to chase a drifting carrier may improve a small sample but does not establish a stable industrial process.
White backing and opacity on dark garments
A white backing layer is essential in many designs transferred to dark textiles. Without an adequate opaque underbase, the fabric color influences the perceived saturation and hue of the overlying graphic. Yellow may look muted, red may darken, and pale shades may lose impact.
The white layer may be produced during the primary print stage, by screen printing afterward, or by a qualified combination of the two. Required opacity depends on garment color, image content, and the chemistry of the white pigment and binder.
More white is not always better. Thicker layers can change hand feel, flexibility, and stretch durability. Excessive build may increase the risk of cracking or a visibly raised transfer. The correct target is sufficient opacity with the minimum practical structure that still meets durability requirements.
White choke and trapping
To prevent a visible white border around the color design, the white contour is often placed slightly inside the printed image boundaries. The practice is commonly described as white choke or negative trapping.
In some production systems, an inward offset of approximately 0.1–0.2 mm is a useful development starting range. The final value must reflect screen registration capability, carrier stability, fine artwork features, and the planned color-to-white overlap.
Too little choke can expose a white halo after even a modest registration deviation. Too much can leave the color image without enough opaque backing near its edges. White geometry should therefore be tested on the actual garment color and after the full heat-transfer cycle.
Selecting and qualifying the printing process
The primary image can be produced by a suitable digital technology, including Liquid Electrophotography (LEP), if the transfer media and ink system are qualified together. The digital stage provides detailed graphics, complex color, and the ability to vary content between images. Screen printing then supplies functional layers that may require heavier coating deposits or different chemical properties.
Both stages must be qualified as a system. The inks must remain compatible with the release construction during printing and with the later white, clear and adhesive layers. Appropriate drying, fixing or curing is essential before the next layer is applied. Printing quality alone does not demonstrate process readiness if the subsequent finishing layer causes swelling, loss of adhesion or inadequate cohesion.
Screen printing the functional layers.
Screen printing allows controlled application of white, clear, barrier and bonding materials. Mesh specification, stencil geometry, squeegee hardness, coating rheology and print speed influence the resulting deposit and edge definition.
Each layer has different requirements. A white underbase may demand substantial opacity, while a clear interface layer may be selected primarily for cohesion and compatibility with powdered adhesive. An anti-migration coating may require continuity and an adequate barrier thickness rather than a particular optical density.
Each deposited layer must be sufficiently dried or cured before the next step, unless the qualified chemistry specifically requires wet-on-wet processing. Interlayer registration and edge shaping must remain within defined limits. The resulting stack needs to function as a flexible unit after Transfer, not merely appear uniform on the carrier.
Dye migration from sublimation-colored polyester
Dye migration is a central engineering risk when applying a heat transfer to certain sublimation-dyed polyester garments. Heat can increase the mobility of dyes already present within the textile. Over time, the dyes may diffuse into the newly transferred graphic, especially into white or other pale areas.
The manifestation may be immediate or delayed. A bright white number placed on red polyester may acquire a pink tint even though the initial digital color measurement and transfer appearance were correct. This is not necessarily a color-calibration defect; it can be a transport phenomenon driven by the textile's dye chemistry and the application's heat history.
A dedicated anti-migration barrier may be needed between the print structure and the garment-side adhesive. Some systems use a carbon-black-containing layer, but carbon black alone does not prove sufficient dye-blocking ability. The barrier's chemistry, dry coating weight, continuity and compatibility with adjacent layers determine its effectiveness.
The barrier must be validated against representative dyed fabrics, transfer cycles and accelerated storage conditions. It should also be checked for any unintended influence on opacity, flexibility or color appearance. Lowering transfer temperature, when compatible with adhesive activation, may also reduce the driving conditions for dye migration, but is not a substitute for validating the complete structure.
The functional clear layer
A transparent binder or clear layer may be incorporated between the printed image and the final adhesive. Its purpose is not necessarily decorative. It can improve cohesion in the multilayer graphic, create an interface compatible with the adhesive, and improve durability after Transfer.
The clear layer must have mechanical properties appropriate to the textile. An excessively rigid formulation may crack when the fabric stretches; a poorly bonded layer may become the point of failure after laundering. Its design should therefore be evaluated with the same attention given to the image and adhesive layers.
The thermal adhesive: connecting polymer and textile
A heat-activated adhesive supplies the final bond between the Transfer and the garment. Common material families include thermoplastic polyurethane (TPU) and suitable copolyesters. Under appropriate heat and pressure, the adhesive softens or melts, contacts textile fibers, and forms a functional bond as the assembly cools.
Different textiles present different adhesion challenges. Cotton has a fibrous, moisture-responsive surface. Polyester has a different polymer chemistry and thermal behavior. Highly elastic garments place substantial repeated strain on the graphic. Hydrophobic or water-repellent textile finishes may interfere with adhesive wetting and bonding.
No adhesive family should be described as universally superior. Selection must reflect the garment, the application cycle, the expected laundering and the required flexibility and hand feel.
TPU and copolyester adhesives
Property | TPU-based adhesive | Copolyester-based adhesive |
|---|---|---|
Flexibility | May be high in suitably formulated grades | Strongly dependent on polymer grade |
Stretch-garment suitability | Available for elastic applications | Requires selection of an appropriate grade |
Activation temperature | Formulation-specific | Formulation-specific |
Wash resistance | Depends on textile, layer construction and application | Depends on textile, layer construction and application |
Hand feel | Influenced by coat weight and formulation | Influenced by coat weight and formulation |
The selection decision should be based on measured performance. Even an adhesive with excellent initial peel resistance can fail after washing if the transferred stack is too stiff or if the garment changes dimensions more than the graphic.
Applying adhesive in powder form
Some Hybrid Transfer lines use thermoplastic adhesive powder. Apply powder to a suitable receiving layer, often while the layer can still retain the particles. Unwanted powder is removed before a controlled heating step stabilizes the coating.
Powder particle size influences coverage, deposit uniformity, and final texture. Very fine particles do not automatically provide the best performance, nor do coarse particles automatically provide the strongest bond. The chosen distribution must match design detail, adhesive layer weight, and the desired transfer feel.
Powder handling must also be controlled to prevent stray particles from entering the image area. Such particles may bond to the garment where no graphic was intended. The heating stage should stabilize the adhesive for handling and storage while preserving its ability to activate during final garment application.
Fixing and drying before conversion
After the functional layers and adhesive are applied, the Transfer must be made stable enough for stacking, cutting, packaging, and transport. A convection dryer or another qualified heating system may be used depending on the materials. Drying temperature, airflow, and dwell time all affect performance.
Insufficient processing can lead to blocking, unstable layers or poor handling. Excessive processing can deform the carrier, shift registration, or prematurely alter the adhesive. Stabilizing the manufactured Transfer and bonding it to the garment are distinct thermal operations; they should not be assumed to use the same settings.
Cutting and preparing the Transfer for application
Completed transfers may be cut as rectangles using a guillotine or converted with a shaped cutting process. The appropriate approach depends on whether only the printed image transfers, whether a clear or adhesive contour remains around it, and how the material is to be positioned on the garment.
The converting operation must not introduce contaminants or uncontrolled adhesive areas. Accurate placement is particularly important for team numbers, chest logos and internal neck labels. Production jigs or optical positioning systems can reduce variation between operators and garments.
Heat pressing the graphic onto the garment.
During final application, the garment is positioned in a heat-transfer press, and the Transfer is placed with the adhesive facing the textile. Heat and pressure activate the adhesive, while the selected dwell time allows the process to develop the required bond. The carrier is then removed using the specified hot-, warm-, or cold-peel procedure.
Initial visual success is not enough. The bond must be evaluated after the transferred construction has stabilized and again after representative washing, abrasion and stretching. The Transfer should be judged as part of the garment, not only as an isolated printed film.
Temperature, pressure and dwell time
Temperature, effective contact pressure and dwell time determine much of the transfer window. They are interdependent. Higher temperature may shorten the time required for some adhesives but increase the risk of textile damage or dye migration. Higher pressure can improve contact but may create visible platen marks or unwanted deformation.
For certain qualified constructions, trials near 140–165°C and approximately 8–12 seconds may provide a starting range; a 160°C, 12-second cycle is one possible development point. These values must not be treated as universal transfer settings. Fabric type, adhesive formulation, release behavior, and heat-press geometry can require different conditions.
The temperature displayed on a machine is not necessarily the temperature at the adhesive/fabric interface. Similarly, a displayed pneumatic pressure does not directly establish the local pressure distribution beneath the platen. Qualification should focus on actual transfer results under repeatable conditions.
Why raising the temperature is not always the solution
When a transfer begins to peel from a garment, increasing the heat-press setpoint can seem like an obvious response. Yet higher temperature cannot resolve every material incompatibility. A low-energy textile finish, an unsuitable adhesive, or an interlayer weakness may persist despite hotter pressing.
More heat can also worsen unwanted effects: dye migration from sublimation-colored polyester, deformation of heat-sensitive fabrics, a harsh hand feel, or changes in the polymeric graphic structure. Where the adhesive allows, a lower temperature combined with a longer dwell time can sometimes improve the balance between bonding and material protection, but only after controlled trials.
The correct approach is to determine whether failure occurs at the textile/adhesive interface, inside the adhesive, or between functional graphic layers. The selected remedy should address the identified failure mode.
Cotton, polyester and stretch fabrics
Cotton garments can absorb moisture and may change dimensions during laundering. A transfer must tolerate those dimensional changes while retaining its bond. Polyester has different surface chemistry and thermal response, and some dyed polyester fabrics add the additional risk of dye migration.
Stretch fabrics place additional requirements on transfer construction. Adhesion measured on a relaxed specimen may look excellent even when the graphic cracks during garment use. The image, backing, clear layer and adhesive must be able to extend and recover to a degree compatible with the textile.
This is why qualifying one garment type does not qualify all garments. Approval must identify the fabric composition, finish, transfer cycle and intended service conditions.
Elasticity and hand feel
Hand feel is a genuine product requirement, particularly for performance garments and inner neck labels. A heavily built transfer can feel stiff or uncomfortable even if it withstands laundering. Thick white layers, a rigid clear binder, or an excessive adhesive deposit can all create the feel of a plastic patch on the fabric.
Yet simply reducing thickness is not a complete solution: the system must still meet opacity, bond strength and wear resistance. Successful engineering balances coating weight, flexibility, recoverability and appearance. Stretch and recovery tests on the transferred garment complement conventional adhesion measurements.
Wash durability as a system property.
Laundering combines water, detergent, elevated or changing temperature, mechanical agitation, and subsequent drying. The transfer experiences bending, friction, and dimensional movement with the garment. Failures may show up as edge lifting, cracking, color change, reduced opacity, or complete local separation.
State wash durability with the test cycle. Claiming that a transfer survives a particular number of washes is not meaningful unless the water temperature, detergent, drying method, and acceptance criteria are defined. A successful initial peel test cannot replace wash-cycle qualification.
Color fastness and the direction of color movement
Three visually similar outcomes may involve different mechanisms: a graphic loses color, the graphic stains an adjacent fabric, or dye from the garment migrates into the graphic. These should not be conflated.
A faded image may point to instability in the transferred color system. Evaluate staining during rubbing or laundering with relevant color-fastness methods. A pale transfer shifting toward the underlying polyester's color may indicate dye migration from the textile. Correct diagnosis determines whether the remedy belongs in the image chemistry, textile selection, barrier coating, or transfer process.
Perspiration resistance
Athletic wear and labels placed near the skin may be exposed to perspiration. Salts, moisture, and pH variations can affect color stability and certain material interfaces. Testing should therefore evaluate color change and staining, and, when appropriate, the mechanical integrity of the transferred structure after exposure.
Passing a color-fastness-to-perspiration test does not automatically demonstrate the adhesive's long-term peel strength. The qualification plan should include the failure risks relevant to the product's intended wear conditions.
Stretch, recovery and abrasion
A garment rarely remains flat in service. Repeated bending and stretching can expose weakness in the graphic's cohesion or adhesion. Suitable testing applies controlled elongation and repeated extension/recovery cycles while examining cracking, edge separation, and permanent deformation.
Dry and wet abrasion also matter, especially for sportswear and frequently handled regions. No single stretch requirement fits all garments: an elastic athletic jersey and a relatively stable workwear fabric impose different demands. Acceptance criteria must be derived from the intended product.
Chemical safety for skin-contact textiles
Heat transfer labels may be used on garments that remain in close contact with the skin. Their chemical compliance should therefore be evaluated alongside mechanical durability. Depending on market and product category, relevant concerns may include restricted dyes, residual processing chemicals and other substances subject to legal limitations.
In the European Union, REACH Regulation (EC) No 1907/2006 and its Annex XVII restrictions are relevant to certain substances in textiles. Among other provisions, restrictions exist for specified azo colorants that can release designated aromatic amines. Applicability depends on the substance, the article, and the nature of contact.
Compliance cannot be inferred merely from a generic ink-family description. It requires suitable material documentation, assessment of the completed product and any tests needed for the target market. Additional restrictions may apply to children's apparel and other specialized uses.
Standards and appropriate performance tests
Heat transfer labels do not have a single universal test covering all aspects of durability. Standardized textile methods address laundering, color change, staining, perspiration, hot pressing, and dimensional stability, while adhesion and stretch performance may require a documented product-specific protocol.
Standard or framework | Primary scope |
|---|---|
ISO 6330:2021 | Domestic washing and drying procedures for textile testing |
ISO 105-C06:2010 | Color fastness to domestic and commercial laundering |
ISO 105-X12:2016 | Color fastness to rubbing |
ISO 105-E04:2013 | Color fastness to perspiration |
ISO 105-X11:2026 | Color fastness to hot pressing |
ISO 5077:2007 | Dimensional change in washing and drying |
ISO 3758:2023 | Textile care labeling symbols |
REACH, Regulation (EC) No 1907/2006, Annex XVII | Applicable restrictions on selected substances in textiles |
The standards define procedures or legal frameworks, not one universal acceptance level for every garment. Passing a laundering color-fastness test does not necessarily demonstrate that the adhesive bond survives cyclic stretching. A relevant end-use specification must combine complementary tests and explicit pass/fail criteria.
End-to-end quality qualification
Qualification should include measurements and functional checks at every major production handoff. This approach makes it easier to identify when a defect first appears and prevents the finished garment from being treated as a single opaque failure.
Production stage | Critical checks | Qualification objective |
|---|---|---|
PET carrier | Thickness, flatness, thermal dimensional change | Stable printing and finishing |
Release system | Temporary retention and defined peel behavior | Controlled Transfer from the carrier |
Preconditioning | Dimensional change before/after heat | Stable interstage registration |
Primary printing | Color, completeness, position and image integrity | Correct graphic formation |
Screen finishing | Registration, white opacity, layer continuity | Complete functional stack |
Anti-migration barrier | Color stability on representative dyed fabrics | Reduced textile dye migration |
Adhesive application | Coverage, deposit and fabric compatibility | Reliable garment bond |
Heat press | Actual cycle, consistency and peel method | Repeatable Transfer |
Finished garment | Washing, rubbing, perspiration, stretch and appearance | End-use performance |
Tests must reflect the intended material function. A tape test on a deliberately releasing carrier may give a misleading result, whereas a controlled adhesion check after garment transfer provides relevant information. Each release, coating, and bonding interface should be evaluated at the stage for which it was designed.
Troubleshooting: when the finished Transfer fails
A properly structured investigation begins with the defect's location and timing. Registration errors observed before garment transfer require a different investigation from edge lifting that first appears after repeated laundering.
Symptom | Possible mechanism | Recommended investigation |
|---|---|---|
Misregistration between digital print and screen layers | PET dimensional change, skew or incorrect scaling | Measure carrier distortion; verify conditioning and stage-to-stage registration. |
White outline around the design | Incorrect white choke or registration | Revise underbase geometry and verify repeatability |
Insufficient opacity | White deposit too low or uneven | Optimize white construction without excessive stiffness |
Color shift on sublimation-dyed polyester | Dye migration from garment | Validate anti-migration barrier and thermal cycle |
Transfer lifts from garment. | Adhesive incompatibility or inadequate interface activation | Locate failure interface; qualify heat, time, and contact pressure. |
Graphic cracks under stretch | Excessive layer stiffness or thickness | Evaluate ink, clear, and adhesive flexibility |
Delamination after washing | Weak textile or interlayer bond | Compare pre-wash and post-wash failure locations |
Carrier difficult to remove | Peel temperature or release system mismatch | Verify approved release method and cooling sequence |
Color shift after pressing | Optical, thermal, or chemical effect | Compare measured color before and after each step |
Harsh hand feel | Thick or rigid transfer structure | Balance backing, clear and adhesive coat weights |
Distortion after laundering | Differential shrinkage between fabric and Transfer | Assess garment dimensional stability and transfer recovery |
If a graphic lifts from the garment, determine whether the separation occurs between fabric and adhesive, within the adhesive, or within the printed stack. If colors change, distinguish textile migration from chemical or optical changes in the graphic. If registration drifts, establish whether the root cause is dimensional film movement before adjusting screen placement.
Raising transfer temperature, adding more white, or increasing adhesive weight are not universal solutions. Each intervention may improve one property while damaging another. Controlled experiments should address the verified mechanism and then revalidate the garment under the intended service conditions.
Conclusion: the graphic succeeds when it becomes part of the garment
Heat Transfer Labels combine polymer science, digital imaging, screen printing, adhesive chemistry, and textile engineering. The carrier must stay aligned throughout production. The release system must provide temporary support and controlled separation. The printed image must deliver color and detail, while white backing, functional clear coatings, and any anti-migration barrier must meet opacity and durability requirements without making the graphic unnecessarily rigid.
The thermal adhesive must bond appropriately to the selected textile, and heat pressing must activate that bond without damaging the fabric or the printed structure. Even then, qualification is incomplete until the transferred design has been tested against the washing, rubbing, perspiration, and stretching demanded by its intended use.
A printing press creates the image. The functional layers, adhesive, and Transfer cycle turn it into a part of the garment.
The real measure of quality is not the moment the carrier is peeled away. It is whether the graphic remains attractive, flexible, and durable after the garment has been worn, stretched, and washed repeatedly.
Standards and professional framework
- ISO 6330:2021 — Textiles: Domestic Washing and Drying Procedures for Textile Testing. Standardized washing and drying procedures used in performance evaluation.
- ISO 105-C06:2010 — Color Fastness to Domestic and Commercial Laundering. Evaluation of color change and staining under defined laundering conditions.
- ISO 105-X12:2016 — Color Fastness to Rubbing. Evaluation of color transfer during dry and wet rubbing.
- ISO 105-E04:2013 — Color Fastness to Perspiration. Assessment of color fastness under defined perspiration conditions.
- ISO 105-X11:2026 — Color Fastness to Hot Pressing. Assessment of color behavior under specified hot-pressing conditions.
- ISO 5077:2007 — Determination of Dimensional Change in Washing and Drying. Measurement of textile dimensional changes after defined treatment.
- ISO 3758:2023 — Textiles: Care Labeling Code Using Symbols. Symbols communicating suitable textile-care procedures.
- Regulation (EC) No 1907/2006 — REACH, including Annex XVII. Applicable chemical restrictions, including relevant limitations for certain textile uses.
Testing methods and acceptance thresholds must be selected for the specific garment, carrier, transfer chemistry, heat-press process, and target market. A compliant raw material or one successful laboratory measurement is not a substitute for end-to-end qualification of the finished decorated garment.