Ronen Dolev | 2026
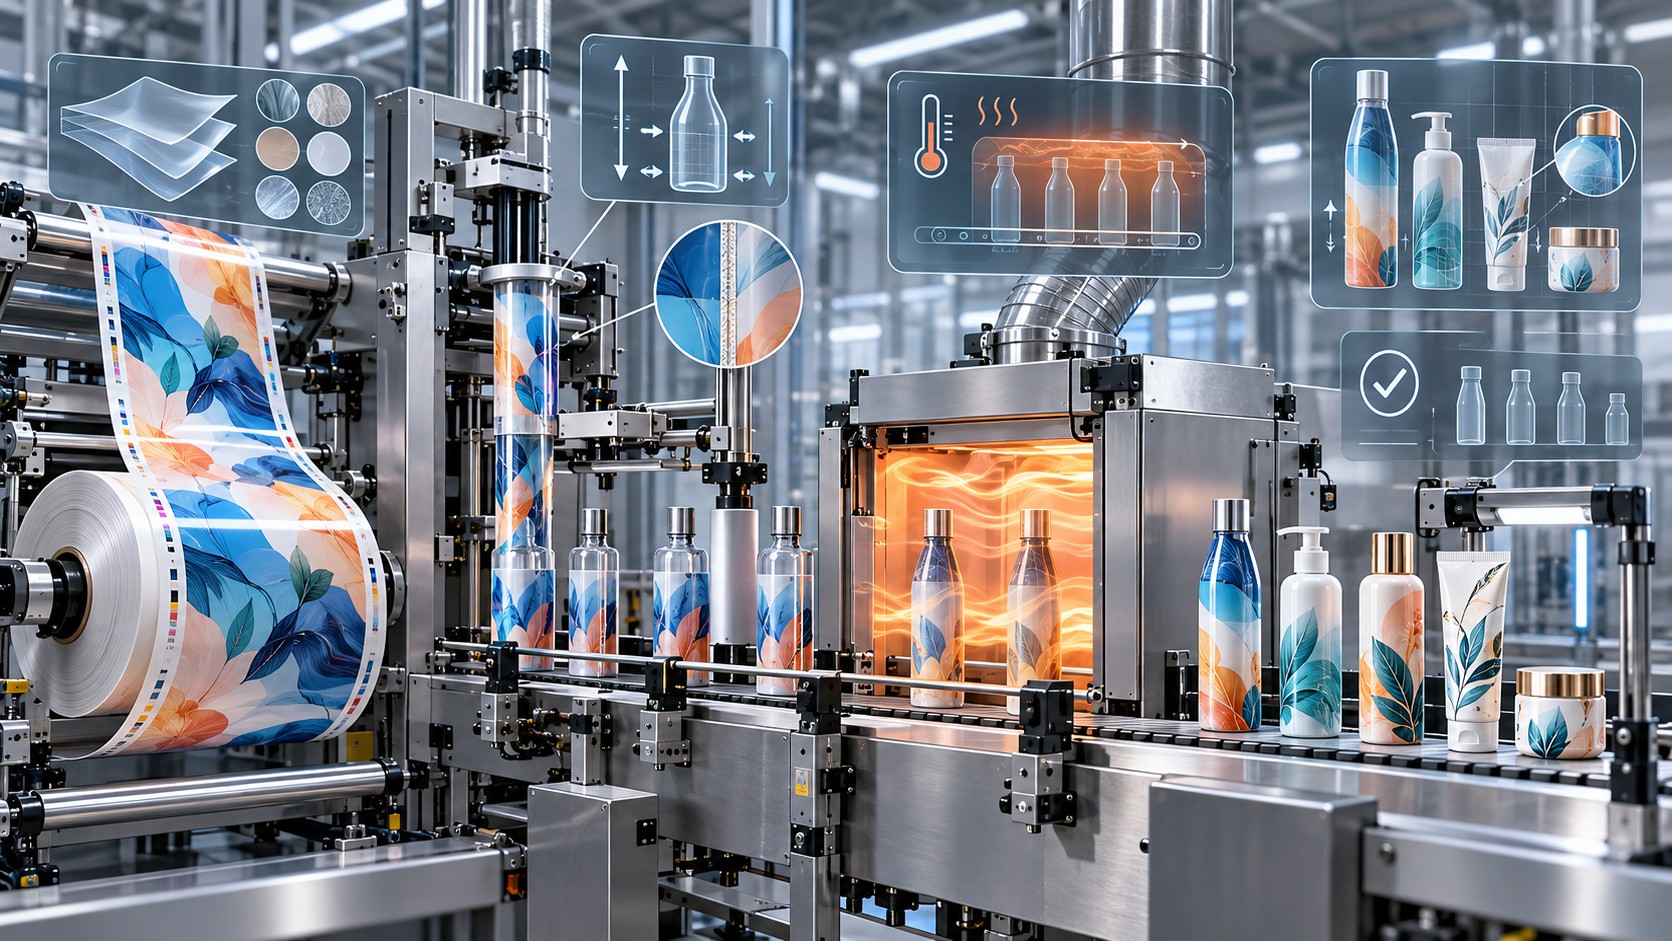
A shrink sleeve is one of the rare packaging applications in which dimensional change is not a defect to be prevented but an essential part of the product's design. A graphic is printed on a flat, oriented polymer film and ultimately applied to a three-dimensional container whose diameter, shoulders, grooves, and neck may differ substantially. Between those two states, the film must be printed, protected, slit, formed into a tube, seamed, applied, and heated. Every operation must preserve the film's ability to shrink predictably.
That's why you can't qualify a successful shrink sleeve at the printing press alone. A clean image and accurate color register are necessary, but they do not demonstrate that the final sleeve will conform to the container without wrinkles, cracked ink, weak seams, misplaced graphics, or trapped air. The application is a complete materials-and-process system, and development has to begin with the finished package.
The application: what is a shrink sleeve and where is it used?
A heat-shrink sleeve is a label manufactured from a specially oriented plastic film. The printed film is formed into a tubular sleeve, placed over a container, and exposed to carefully controlled heat. As its orientation relaxes, the film contracts around the container and follows its contours. The result can be a narrow tamper-evident neck band, a partial-body label, or an almost full-body graphic with 360-degree visibility.
The technology is widely used for beverages, sauces and other foods, personal-care products, cosmetics, cleaning products, and selected pharmaceutical and nutraceutical packages. It is particularly attractive for containers with an unusual silhouette or when the brand requires a large, uninterrupted display area. Shrink sleeves can also be designed to hold together selected multipacks, provided the film and container system are qualified for the mechanical forces involved.
Unlike a conventional pressure-sensitive label, a traditional heat-shrink sleeve does not depend on a full-area adhesive to remain attached to the container. Controlled shrinkage creates its final fit. That does not mean adhesion or anchoring is irrelevant: certain labeling lines use localized positioning aids, and the sleeve's inner-surface friction is fundamental to accurate application.
The film also becomes part of the package's optical appearance. With reverse printing, the transparent film protects the image from direct abrasion and moisture, while the underlying ink and opaque white layers establish contrast against the actual container. The color seen on the shelf therefore results from both the printed construction and the geometry of the shrunk label.
Not all sleeve systems are the same
Three technologies are frequently grouped under the broad term "sleeves," although their materials and converting sequences differ. Traditional transverse-direction heat-shrink sleeves are formed and seamed before application. Roll-fed shrink systems use films primarily oriented in the machine direction and may form the wrap around or immediately above the container. Stretch sleeves use mechanical elasticity instead of heat.
Sleeve system | Film behavior and conversion | Typical application consideration |
|---|---|---|
Heat-shrink sleeve (TDO) | Predominant transverse-direction shrink; printed film is converted into a pre-seamed tube. | Full-body coverage, contoured bottles, narrow necks, tamper-evident bands |
Roll-and-shrink (MDO) | Predominant machine-direction shrink; roll-fed application and a joining operation close to the container. | Straight-wall and partial-cover applications, subject to equipment capability |
Stretch sleeve | Elastic film is stretched over the package; no heat-shrink tunnel is required. | Specific shapes and applications where mechanical stretch is preferable |
The rest of this article concentrates on traditional TDO heat-shrink sleeves. Their large shrink potential gives designers significant freedom, but it also demands tighter coordination among film selection, artwork, seaming, and tunnel performance.
The science of TDO and MDO: making polymer orientation work for the package
An extruded film can be drawn in the direction of web travel, across the web, or in both directions, depending on the manufacturing process. This stretching changes the arrangement of the polymer chains and develops orientation-related mechanical properties. A purpose-designed shrink film retains a controlled tendency to recover part of that deformation when exposed to an appropriate temperature.
TDO means Transverse Direction Orientation: the main designed shrink direction is across the web. When the film is subsequently formed into a tube, that direction corresponds principally to the container's circumference. MDO means Machine Direction Orientation: the primary designed contraction is along the web's running direction. The two film families are not interchangeable simply because both can shrink when heated.
The common expression "thermal memory" is a useful illustration, but the underlying mechanism is relaxation of molecular orientation and stored stresses. Polymer chemistry, degree of orientation, thermal history, and film-manufacturing conditions determine when shrinkage begins, how quickly it develops, the maximum attainable shrink, and the force imposed on the container.
An important qualification follows: maximum shrink percentage is not the complete performance specification. A film may offer sufficient eventual shrink but contract too rapidly for a particular machine or bottle design. Another may shrink more progressively and therefore give a much wider processing window, even if its maximum shrink percentage is lower.
First design the container, then select the film.
A sleeve project should start with the actual package geometry and its filling-line conditions. The engineering team needs the maximum and minimum circumferences over the area to be covered, shoulder transitions, recesses, label height, the orientation of critical graphics, and any areas where trapped air might accumulate. A nominal bottle diameter is rarely enough for a complex container.
The container's material and mechanical stiffness are equally important. Glass and rigid metal can tolerate shrink forces that may deform a thin-wall or squeezable plastic bottle. Filled and empty containers also exchange heat differently. Product temperature, filling order, line speed, and whether shrinking occurs before or after filling can all change the result.
A useful first calculation is the shrink demand between a larger and smaller circumference. For a simplified circular container, the theoretical reduction required to move from circumference Cmax to Cmin can be written as:
Required circumferential reduction (%) = 100 × (Cmax − Cmin) / Cmax
That calculation is a starting point, not a prediction of finished-label quality. The final fit depends on where the material first contacts the package, the film's shrink curve, local heating, the seam, and the sequence in which the sleeve is anchored.
For a very contoured container, it may be appropriate to select a film with a maximum shrink potential somewhat above the calculated minimum. However, excess shrink capability is not an advantage if it comes with unacceptably high force or an overly narrow heat-processing window. The decision must be based on testing the film and the actual container together.
Choosing the polymer: PETG, PVC, OPS, polyolefin, and other candidates
Several different film families can be manufactured for shrink-sleeve applications. Their general characteristics provide a shortlist, but the decisive choice is the specific grade, not merely the polymer name. Commercial grades within one family can have very different shrink-initiation temperatures, MD growth, shrink forces, opacity, and chemical resistance.
Film family | Typical strengths | Main engineering considerations |
|---|---|---|
PETG | High clarity and gloss; high shrink potential, with some grades approaching 75–80% | Shrink speed and force may be high; rigid versus squeezable containers, tunnel capability, and recycling compatibility matter. |
PVC | Broad range of shrink behavior; often cost-effective; moderate force in suitable grades | MD-related shape distortion, chemical compatibility, and recycling-system restrictions need attention. |
OPS | Low shrink force; useful for squeezable and intricately shaped containers | Greater sensitivity to storage and handling, and more limited chemical resistance in many grades |
Polyolefin blends | Potential for low-density, floatable sleeve constructions and controlled shrink force | Different clarity and seaming behavior; exact polymer mix and recycler qualification are essential. |
Purpose-designed PET or crystallizable polyester grades | Can help address compatibility with selected PET-recycling processes | Grade-specific shrink profile, adhesion, and seaming requirements must be validated |
Specialty hybrid or bio-based films | Can combine targeted shrink, softness, clarity, or sourcing characteristics | Stability, brittleness, cost, supply, and actual end-of-life acceptance vary significantly. |
PETG is often considered for demanding silhouettes because suitable grades offer high shrink capacity. That same characteristic may be undesirable on a soft or thin-wall bottle. OPS can offer a gentler mechanical response for squeezable containers, but it may require tighter storage and converting control. Polyolefin constructions can help certain separation processes in PET recycling when density and other requirements are met; they still need qualification for the complete sorting and washing system.
PVC remains technically useful in some shrink applications, but regulatory and end-of-life requirements may make another family preferable. These are not interchangeable sustainability claims: a material that performs well in the shrink tunnel is not automatically compatible with a particular collection or recycling stream.
Film thickness and shrink force
Many conventional shrink sleeves use films around 40–50 µm thick, although thinner and thicker specialty grades exist. Down-gauging can reduce material consumption, but it changes web handling, distortion resistance, slit-edge durability, and the film's interaction with the container under shrink tension.
The appropriate gauge depends on the balance between stiffness during converting, clarity, shrink force, line speed, sleeve geometry, and the container's mechanical strength. The thinnest available film is not necessarily the most stable or economical option once you include handling losses and quality rejects.
Reading the complete shrink curve
Film qualification should compare shrinkage as a function of temperature, preferably using a consistent method and exposure time. Pay particular attention to the onset of shrinking, the slope of the curve, its final achievable contraction, and any growth or contraction in the machine direction. A steep curve can make temperature variations inside the tunnel translate into large differences in final appearance.
Two films that both shrink 65% under one laboratory condition may behave quite differently on a moving bottle. One may begin contracting before the sleeve is correctly positioned; the other may not complete the required contour within the available residence time. Selection should therefore use the film's data together with practical trials on the actual shrinking equipment.
Engineering the artwork: printing the wrong shape to obtain the right image
Shrink sleeves reverse a familiar design assumption. On a flat label, the goal is usually to preserve the printed geometry. On a heat-shrink sleeve, the goal is for intentionally pre-distorted artwork to become visually correct after the substrate deforms on a three-dimensional surface.
A logo printed with its original proportions may appear compressed across a bottle's neck. Fine text may become unreadable. A face or illustration may stretch into an unnatural proportion. The right prepress strategy applies controlled compensation to artwork in areas that will shrink by different amounts.
A practical development method is to print a calibrated grid, seam it into a sleeve, apply it to a representative container, and run it through the intended shrinking process. By measuring where and how the grid deforms, the team establishes a geometric map for artwork compensation. Three-dimensional design and simulation software can reduce iteration time, but the physical prototype remains the acceptance reference because film behavior also depends on actual heat delivery and sleeve placement.
The final design should be approved on the finished container, not merely on a screen rendering or a flat printed proof.
Protecting critical information
Do not place text, logos, regulatory information, or barcodes indiscriminately across the sleeve. High-shrink areas, fold lines, and the seaming zone should be treated as high-risk locations for small or critical content. As an initial artwork rule, regions requiring more than roughly 60% shrink are often unsuitable for delicate details unless testing demonstrates otherwise.
Barcode orientation also matters. Lines and spacing may distort differently depending on the film's predominant shrink direction. Scan testing must verify placement and orientation after the sleeve is fully shrunk on the production container. Correct appearance is not enough if functional information cannot be read.
Sizing the lay-flat and defining no-print zones
After converting, the flat tubular sleeve is measured by its lay-flat width. The flat web's slit width must also account for the additional material consumed by the seam overlap. For a substantially circular container, a common preliminary sizing approximation is:
Lay-flat width ≈ (maximum container diameter + allowance) × π/2
Slit width ≈ 2 × lay-flat width + seam overlap
These are layout estimates; an irregular container should be assessed from its actual perimeter, sleeve fit, and the converting machine's requirements. Seam overlap is often 6–10 mm, with a clean joining region around 4–7 mm, but the validated requirement depends on the actual system. Small clear areas at the top and bottom can also be needed for slitting and cutting. All such zones must be explicitly included in the prepress layout.
Reverse printing: the sleeve is its own protective window
Most transparent heat-shrink sleeves are reverse printed so that the ink faces toward the container in the finished product. The transparent oriented film therefore protects the image from direct mechanical contact, while the graphic remains visible through the film.
A typical reverse-printed construction consists of the oriented film, a compatible surface-preparation or primer layer where required, the ink image, an opaque white backing where specified, and a suitable inner-facing protective or slip layer. The exact layer sequence must be defined for the chosen printing technology and artwork. Opaque films may require a different, surface-printed arrangement.
The final inner layer does more than protect ink. It influences friction against the container and the labeling equipment, and it can influence blocking behavior when the converted sleeves are stored in a roll. These considerations mean that high opacity, print adhesion, low friction, and shrink flexibility must be developed as one compatible layer system.
Surface preparation: dyne level, corona, and primer
Film surfaces differ in their ability to be wetted by primers and printing inks. Their properties can also change during storage through additive migration or contamination. Incoming surface wetting should therefore be checked before the production route is finalized.
A working wetting-tension value around 38 dyn/cm before treatment may be a useful reference for certain sleeve films, but it is not a universal acceptance specification. More importantly, a satisfactory dyne indication does not prove that the primer will survive the later converting and shrink processes. Chemical compatibility, primer coat weight, drying, film treatment, and the finished product's exposures all matter.
A controlled corona-refresh step can improve wetting immediately before priming, where suitable for the material. More corona power is not necessarily better. Over-treatment can create a surface that passes an initial print test yet performs poorly under subsequent water exposure or strain. The correct treatment level is the minimum effective one verified through actual adhesion and end-product testing.
The primer must anchor the ink while accommodating the shrinkage the product demands. A coating that appears successful after printing but cracks or separates in high-shrink regions is not qualified. Pre-treated films may eliminate a separate priming operation, but the converter must still confirm suitability for the intended ink, seaming method, and thermal process.
Lane priming: an apparently small detail with major consequences
Most shrink sleeves must be joined along a narrow seam. In solvent-compatible constructions, the seam requires direct interaction with the film material. If a primer, ink, or varnish interferes with that interface, the joining chemistry may no longer function properly.
One robust approach is selective or lane priming, in which the intended seaming strip is deliberately left clear. The artwork and subsequent protective coating must respect the same zone. Even a slight misalignment between the clear lane and the printed image may introduce ink or coating into the seam, reducing its integrity.
Certain specialized systems allow a seam to be formed through a specifically qualified primer using a compatible joining method. That capability should never be assumed for ordinary primers. It must be demonstrated by a joint film/primer/seaming qualification, rather than inferred from printability alone.
LEP printing: web control is as important as color register
LEP printing can provide high-quality image reproduction, sharp type, and accurate color registration on compatible shrink films. Yet the substrate's intentional heat sensitivity introduces application constraints that differ from those of an ordinary label stock.
Excessive or unbalanced thermal exposure can start dimensional change before the film reaches the shrink tunnel. A stop in a heated zone may affect a stationary segment differently from a continuously moving web. Excessive web tension can stretch or distort the film and cause variation in print-repeat length.
The printer must therefore qualify dimensional consistency, machine and cross-direction scaling, temperature-related changes, print-repeat length, and roll handling together with image quality. A roll can pass color inspection and still be unsuitable for conversion if the cut position drifts relative to the repeated graphic.
White opacity versus layer flexibility
Reverse-printed graphics frequently depend on an opaque white backing to maintain color appearance over transparent, dark, or colored containers. But white coverage adds to the thickness and mechanical character of the printed construction.
Increasing white laydown without considering subsequent shrink can raise the risk of cracking in demanding areas. The right design balances opacity, visual appearance, interlayer adhesion, and the combined image's ability to tolerate the required deformation. Color should also be evaluated on the shrunk container: the changed geometry and optical stack can affect apparent hue and opacity even when the pigment has not chemically changed.
Overprint varnish, slip chemistry, and coefficient of friction
The sleeve's inner-facing surface often needs a protective or slip formulation that allows it to travel over the container during high-speed application. The relevant parameter is the coefficient of friction (COF) between the actual contacting surfaces under representative conditions.
If friction is too high, the sleeve may catch, position incorrectly, or fail to slide over the bottle. If too low, it may shift or become unstable under handling and tunnel airflow. A COF around 0.15–0.20 is a useful starting reference for certain sleeve-labeling configurations, not a universal target for every machine and container.
Slip additives may migrate toward the coating surface after printing or curing. Consequently, an immediate post-coating COF measurement may not represent the value seen during application a day or two later. Qualification should define the stabilization time and measure performance at the relevant production age.
An inner varnish can also improve resistance to abrasion, chemicals, or moisture where required. However, it must be sufficiently flexible to survive high shrink without cracking, and fully dried or cured before winding to avoid blocking. Excessive coat weight, inadequate cure, and an unsuitable polymer chemistry can all compromise the process. The seaming lane must remain compatible with the intended joining method.
Slitting: creating accurate edges without planting a crack
Once printing and coating are complete, the master web is slit to the widths required for sleeve forming. Slit accuracy controls the tubular circumference and the consistency of the seam overlap. Edge quality is equally important.
A dull or incorrectly presented blade can leave microscopic damage, rough edges, or an uneven cut. These can become initiation points for ink cracking or tearing when the sleeve later contracts. Blade condition, geometry, alignment, and suitable web tension are therefore process-control variables, not routine maintenance details to be considered only after a defect occurs.
The slitting operation should also limit static buildup and avoid introducing dust that could contaminate the subsequent seam. Inspect cut-edge condition under representative lighting and magnification when developing a demanding application.
Seaming: converting a printed web into a tubular sleeve
Seaming closes the flat web into a tube by overlapping its edges and forming a bond compatible with the film chemistry. The result is a tubular sleeve that can be wound flat and supplied to the labeling line.
The joining mechanism depends on the selected polymer and equipment. Some systems use solvent-assisted bonding, while others employ thermal or other validated joining technologies. Solvent use requires suitable engineering controls, safety precautions, and supplier-approved procedures; do not assume the same solvent is suitable for different film families.
The seam must remain continuous and sufficiently strong through cutting, sleeving, and thermal contraction. Too little joining medium may leave weak or open sections; too much may damage or distort the film, cause blocking, or alter the seam's geometry. Web tension, overlap accuracy, nip loading, joining-media delivery, and material compatibility all affect the outcome.
Test seam strength under standardized in-house conditions, record the specimen direction and width, and check whether failure occurs at the seam or by tearing the surrounding film. A destructive material failure can be qualitatively different from a clean seam opening, even when the force values appear similar.
The converted sleeve's lay-flat geometry and seam alignment should be inspected before the roll is released. A seam that looks acceptable on the flat web can fail only when shrink forces rise inside the tunnel, so representative shrink testing remains necessary.
Winding and seam buildup
The overlapping seam is thicker than the rest of the sleeve. If every successive turn positions that thick region directly over the previous one, the wound roll can develop a raised band and localized pressure. Oscillating the rewind position can distribute this buildup over a wider region.
Winding tension must be high enough to form a stable roll but low enough to avoid sleeve deformation and cracking at lay-flat folds. This balance is especially important for thin films and heavy printed constructions. Static, contamination, and residual joining medium also require control before packing and shipping.
Sleeving: placing the tube accurately over the container
During labeling, the tubular sleeve is opened, cut to the required height, and lowered over each container. High-speed equipment must coordinate sleeve feed, cut length, container movement, and vertical position.
The sleeve's lay-flat width, inner-surface friction, cut-height accuracy, and seam orientation determine whether this operation is repeatable. A sleeve that catches on a shoulder or slides too easily may enter the tunnel in an incorrect position. No later temperature adjustment can reliably compensate for an unstable initial placement.
The container condition must also be specified. Filled and empty containers can respond differently to the same heat profile, and a squeezable container must not be compressed or deformed by the shrink forces imposed during finishing.
Shrinking: controlling the order in which the sleeve contracts
The shrinking tunnel supplies the energy that allows the oriented film to relax and conform to the container. The central engineering task is not simply to reach the greatest shrink percentage; it is to deliver heat in the right locations and sequence so the sleeve can move into its final shape without trapping air, wrinkling, or damaging the image.
The selected system may use steam, hot air, infrared radiation, or a combination. Each has advantages and limitations.
Heat-delivery method | Operating principle | Engineering considerations |
|---|---|---|
Steam tunnel | Efficient transfer of thermal energy by steam contact | Often provides good uniformity for complex full-body sleeves; moisture management and condensation must be considered |
Hot-air tunnel | Controlled streams of heated air around the container | Zone control and directional heating are possible; airflow shadows and uneven exposure can occur |
Infrared (IR) | Radiation absorbed by the film and surrounding surfaces | Can support targeted heating; absorption depends on material and image characteristics, so local overheating is possible |
Combined or staged systems | Different heat sources or progressively controlled zones | Broader control options, with additional complexity in process qualification |
Steam often provides useful uniformity for strongly contoured full-body labels. Hot air can be directed to specific regions, but a recessed bottle surface may sit in a heat shadow. With infrared exposure, colors, coatings, and container materials may absorb differently and change the local heating rate. Selection must be made for the whole package and production line, not from a generic preference for one tunnel technology.
Why staged heating can be better than maximum heat
If a sleeve contracts too early in one region, it can block air escape or restrict movement needed elsewhere. Properly staged heating lets the label position and anchor first, then complete the remaining shrink in a controlled sequence. On some containers, gentle preheating followed by stronger, zoned heating yields better results than a single aggressive thermal exposure.
Increasing temperature can improve a genuinely under-shrunk region, but it can just as readily worsen wrinkles, distort color, damage the film, or exaggerate the mechanical load on a thin-walled container. The aim is an adequate, reproducible thermal profile—not the hottest profile the film can tolerate.
Air entrapment and bridging over recesses
Deep grooves and bottle indentations can trap air when a sleeve contacts surrounding regions before the cavity beneath it has vented. The film may bridge over the feature rather than follow its contour. This is not necessarily evidence that the film lacks enough theoretical shrink capability.
The first response should be to review the heating and anchoring sequence. Where appropriate, carefully positioned micro-perforations may provide a controlled air-release route. Such openings must be assessed for appearance, functional integrity, and product requirements before they are introduced into production. They are not appropriate where the sleeve is expected to provide a barrier or a tamper-evident function that the openings would compromise.
Designing for recycling and product stewardship
A shrink sleeve must be considered together with the container's end-of-life route. Full-body printed sleeves can affect optical sorting if they obscure the container material. Film density, separation behavior in wash processes, compatibility of the sleeve polymer with the container stream, and ink or coating release can all influence recycling performance.
A low-density polyolefin sleeve may float while PET sinks in a suitable float-sink separation process; that benefit depends on the full sleeve construction and the recycling system. Certain polyester sleeve grades may be engineered for specific PET-recycling compatibility, while others may require removal before PET reprocessing.
Neither the polymer name nor the absence of a full-area adhesive is enough to claim recyclability. Qualification should reflect the collection, sorting, washing, and reprocessing practices in the intended market. This requirement belongs at the film-selection stage, not after artwork and converting have already been approved.
Quality qualification from film to finished container
The technical qualification program should progressively demonstrate four things: incoming film suitability; stable printing and protective coatings; reliable converting and seaming; and correct behavior on the finished container after shrinking.
Characteristic | Relevant test framework or control | Why it matters |
|---|---|---|
Film thickness | ASTM D374 | Gauge stability for printing, shrinking, and machine handling |
Tensile properties and elongation | ASTM D882 | Mechanical response in machine and transverse directions |
Unrestrained thermal shrinkage | ASTM D2732 | Shrink percentage under defined laboratory conditions |
Orientation-release stress / shrink tension. | ASTM D2838 | Force-related behavior during heating |
Coefficient of friction | ASTM D1894 | Sliding behavior during handling and sleeving |
Haze and light transmission | ASTM D1003 | Optical clarity and transparent-film appearance |
Gloss | ASTM D523 | Surface appearance before and after processing |
Film wetting tension | FINAT FTM 15 or validated appropriate method | Incoming wetting and treatment consistency |
Ink adhesion and scratch/rub durability | Applicable FINAT methods and production-specific testing | Survival of printing, converting, and final shrink |
Seam integrity, cut geometry, and tunnel outcome | Qualified application-specific protocols | Functional integrity and repeatability of the finished sleeve |
Test standards establish methods and terminology; they do not automatically establish a universal acceptance threshold for every film grade. For example, an acceptable COF, maximum dimensional drift, seam-peel force, or shrink percentage must be set by the materials, equipment, application, and customer requirements.
Final approval should include a representative shrink-tunnel simulation or production trial on the actual container, preferably under real filling conditions. Finished sleeves should be checked for graphic distortion, text and barcode readability, ink integrity, seam strength, wrinkles, fogging, trapped air, and the correct fit over the full required height. Also consider production-age effects, including stabilization of slip additives and storage-related film changes.
Troubleshooting: when a finished sleeve fails
Troubleshooting is most effective when the converter distinguishes between the appearance of a defect and the physical stage that created it. A film can print cleanly but fail at slitting; a sound seamed tube can be incorrectly positioned; a properly positioned sleeve can be damaged by an unsuitable heat sequence. The table below links common symptoms to plausible mechanisms and initial engineering checks.
Symptom | Likely mechanisms to investigate | Focused corrective route |
|---|---|---|
Wrinkles or incomplete shrink | Film shrink curve not matched to shape; insufficient or uneven heat; incorrect sleeve placement. | Validate actual film/tunnel/container combination, heat distribution, and cut geometry. |
Smiling or frowning at sleeve edge | Undesired MD change during shrink; grade-specific anisotropic behavior | Select film with suitable MD growth/shrink response and recheck pre-distortion |
Skiving or ink cracks near seam | Rough slit edge; local stress concentration; incompatible ink/primer/protective layers | Inspect blade and slit quality; qualify flexible layer construction and local heat profile. |
Cracking at lay-flat folds | Excess rewind tension; repeated bending; insufficient ink-layer flexibility | Reduce mechanical loading and qualify coating/white build for folding and shrink. |
Weak or opening seam | Contamination by primer/ink/varnish; insufficient or excessive joining medium; mismatched film chemistry | Restore a properly cleared seam lane; control overlap and qualified joining parameters. |
Blocking in the wound roll | Inadequate drying or cure; excessive coat weight; rewind pressure; residual joining medium | Verify complete coating cure, winding tension, roll storage, and chemical compatibility. |
High or low COF | Unsuitable inner slip layer; insufficient stabilization time; contamination | Measure under actual conditions and adjust qualified slip chemistry or application timing. |
Cloudiness or fogging | Optical changes in film/coating or local high-shrink stress | Compare unprinted and printed controls and assess coat weight and thermal profile |
Trapped air or bridging | Early anchoring around recess; inadequate air-release path | Modify staged heating and, if appropriate, validate micro-perforation design |
Wet-look / unwanted optical contact | Local contact and optical interference; possible moisture retention | Assess sleeve fit, inner-layer characteristics, tunnel moisture, and finished appearance |
A defect seen at the tunnel exit does not prove that the tunnel created it. A weak seam often originates earlier in selective priming or joining chemistry. Ink cracks at a lay-flat fold may reflect winding tension or ink-film stiffness, while white haze may derive from coatings or optical contact rather than pigment instability. Likewise, an under-shrunk neck may call for a different film grade or staged heating rather than a blanket temperature increase.
Process adjustments should be changed one controlled variable at a time wherever possible, with representative samples retained for comparison. The acceptance decision belongs to the finished package—not merely to the roll of printed film.
Conclusion: engineering a controlled transformation
Shrink sleeves illustrate how printing, polymer science, converting, and thermal engineering depend on one another. The substrate is designed to deform; the artwork is distorted in advance; the printed layers must remain intact under movement; the seam must endure shrink forces; and the heating system must guide the sleeve into a three-dimensional form without compromising the container or its information.
Successful production starts with the container geometry and application requirements. It continues through a film chosen for its complete shrink curve, correctly prepared surfaces and printed layers, precise slitting and seaming, controlled winding, accurate sleeve placement, and a qualified tunnel profile. Consider recycling compatibility and functional information from the start, not as optional additions at the end.
The real achievement is not printing a perfect image on a flat film. It is creating a finished sleeve that wraps around the container exactly as intended—while preserving the image, the seam, the material integrity, and the package's functionality.
Standards and Technical References
- ASTM D2732 — Standard Test Method for Unrestrained Linear Thermal Shrinkage of Plastic Film and Sheeting.
- ASTM D2838 — Standard Test Method for Shrink Tension and Orientation Release Stress of Plastic Film and Thin Sheeting.
- ASTM D882 — Standard Test Method for Tensile Properties of Thin Plastic Sheeting.
- ASTM D1894 — Standard Test Method for Static and Kinetic Coefficients of Friction of Plastic Film and Sheeting.
- ASTM D1003 — Standard Test Method for Haze and Luminous Transmittance of Transparent Plastics.
- ASTM D523 — Standard Test Method for Specular Gloss.
- ASTM D374 — Standard Test Methods for Thickness of Solid Electrical Insulation (method suitability to the film under test should be confirmed).
- FINAT Technical Handbook — applicable test methods for wetting, ink adhesion, rub, scratch, and chemical resistance; use current editions and method applicability requirements.
- Applicable, current packaging-recyclability design and qualification guidance for the intended container material and market.