By Ronen Dolev | 2026
The factory is efficient. So why is the order still late?
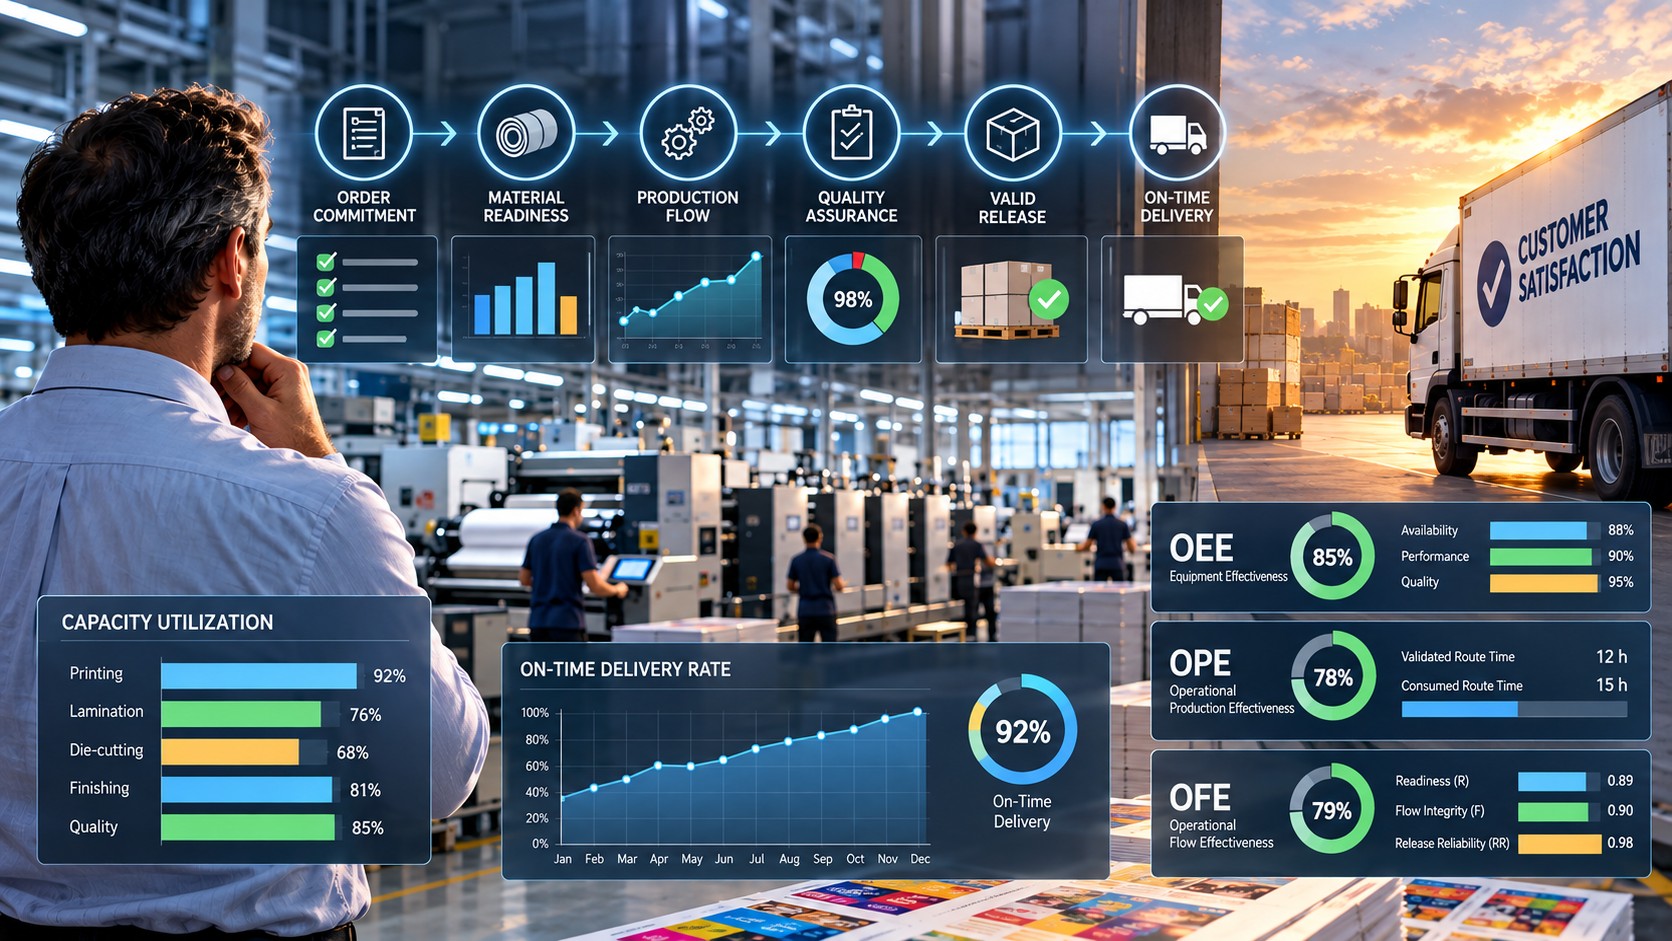
A production manager ends a shift with good reason to be satisfied. The printing press has performed efficiently, waste was below the planned allowance, production speed met its validated target, and the run was completed within its allocated window. Overall Equipment Effectiveness (OEE) reached 85%, an excellent result relative to the press's recent performance.
But the printed order is still not ready for delivery.
The printed rolls are waiting for lamination. A required curing period must follow. The slitting machine is committed to another job, and final quality verification is not yet complete. From the customer's perspective, the factory has not delivered an efficient press or a successfully printed roll. It has promised an approved, finished product by an agreed date.
This is one of the recurring contradictions of industrial operations: every department can meet its local performance target while the complete customer order still fails to meet its commitment. Printing finishes on time. Finishing works to the current production schedule. Quality correctly refuses to release the product before the evidence is complete. Planning uses the capacity available to it. Each decision may be defensible within its own boundary, yet the overall system may not produce the required outcome.
The problem is not necessarily poor machine performance or weak operational discipline. It may lie in how an organization defines, coordinates, and measures success. To address it, we must distinguish between an individual resource's efficiency, the production route's effectiveness, and the factory's ability to fulfill the entire commitment it accepted from the customer.
Why OEE alone is not enough
Overall Equipment Effectiveness is an established measure of equipment performance. It combines Availability, the proportion of defined planned production time in which the equipment operates; Performance, the actual operating rate relative to the validated rate for the selected production condition; and Quality, the proportion of conforming output.
OEE = Availability × Performance × Quality
OEE is valuable because it reveals losses from downtime, speed, and quality within a defined equipment boundary. Its strength is also its limitation: the measurement boundary ends with the equipment. OEE does not determine whether material was ready by the committed production time, whether finishing capacity was secured, whether the correct approved artwork version is being produced, or whether the finished order satisfies all release conditions.
Even the Performance component must reflect the actual approved production condition. A digital print job requiring a seven-separation color mode should not be judged against a faster mode that cannot reproduce the approved product. The validated rate must correspond to the mode and operating conditions required by the order.
OEE can therefore be entirely accurate while leaving the central management question unanswered: did the factory fulfill the customer commitment? Stretching OEE to include every delay and problem outside the press would undermine its established meaning. The better response is to preserve it and add a framework that connects local measures to the complete order.
Local efficiency versus operational excellence
Local efficiency describes how well a machine, department, or activity performs within its defined responsibilities. Operational excellence requires a broader test: can the organization convert a customer requirement into a conforming, authorized product and deliver it under the agreed conditions?
The distinction is practical. A factory can shorten press changeovers, yet achieve little if the next job has no approved file or properly conditioned material. A digital press can finish a short run in minutes, while the same order remains in the plant for days awaiting cutting or converting. Moving work to an alternate route may rescue one delivery commitment but consume capacity already protected for another.
These examples point beyond equipment utilization. The essential issue is how the customer promise travels through materials, people, machines, planning decisions, technical evidence, finishing operations, and release authority. It calls for a way to manage the relationship between those elements without reducing the entire factory to one misleading percentage.
What is Operational Flow Excellence (OFX)?
Operational Flow Excellence, or OFX, is a methodology for governing the complete operational lifecycle of a customer order. It begins with the approved customer requirement and follows that requirement through operational Translation, commitment, route selection, Readiness, controlled execution, governed handoffs, valid release, and learning for future orders.
OFX does not replace production planning, maintenance, quality management, engineering, or existing performance measures. Its purpose is to connect these disciplines around the customer commitment so that managers can see not only what has happened, but what must still remain true if the order is to finish as promised.
Four questions remain visible throughout the order: What was promised? What evidence supported that promise? Who had legitimate authority to make the necessary decisions? And when did those decisions need to be made?
This does not mean assigning every decision to a single manager. Technical, planning, execution, quality, release, and commercial authorities retain their proper responsibilities. OFX connects their work through evidence, decision boundaries, and traceable commitments; it does not replace their professional judgment.
How OFX governs the lifecycle of an order
The methodology consists of ten connected stages, supported throughout by Operational Governance.
Stage | Operational purpose |
|---|---|
Approved Customer Requirement | Establish the controlled, approved version of what the customer expects. |
Operational Translation | Convert the requirement into verifiable production, inspection, and release conditions. |
Operational Commitment | Make a defensible operational commitment supported by current evidence. |
Dynamic Route Selection | Select the production route best supported by quantity, capability, capacity, cost, risk, and timing. |
Route-Specific Readiness | Verify that the selected route can credibly support the commitment. |
Execution Readiness | Confirm that this specific order is authorized and ready to start now. |
Controlled Execution | Produce within the approved operating conditions and decision boundaries. |
Governed Handoffs | Transfer identity, evidence, open decisions, ownership, and stop conditions together with the work. |
Valid Release | Close the order only when all applicable release conditions are satisfied and authorized. |
Prospective Learning | Improve future standards and decisions without rewriting the history of the completed order. |
Operational Governance surrounds these stages. It preserves ownership, evidence, authority, deadlines, escalation, permitted work, stop conditions, Controlled Reopening, and the original chronology of each commitment.
From a commercial request to an executable plan
The lifecycle begins before a press is scheduled. An order for flexible packaging may name a quantity, substrate, finish, and delivery date, yet still leave unanswered questions about graphic versions, color appearance, converting requirements, functional properties, packing, and final acceptance.
A request for a "matte finish," for example, may refer to a matte varnish, a matte laminate, or a specific appearance approved against a customer reference. Operational Translation converts the commercial language into technical and operational conditions the plant can produce, inspect, and release.
Only then can the organization make a credible Operational Commitment. That commitment may be Confirmed, Conditional, or Declined. A conditional commitment is not automatically a failure; it can be responsible if the open conditions, owners, decision deadlines, and available alternatives are explicit. A delivery date entered in a planning system is not, by itself, evidence that the commitment can be protected.
Selecting the complete production route
Several technologies may be capable of producing a product, but the correct route depends on the complete order and the factory's current conditions. Quantity, number of versions, artwork-release timing, material condition, setup requirements, validated printing speed, cost, finishing capacity, and release requirements can all change the preferable route.
The fastest press is not necessarily part of the fastest or most reliable end-to-end route. Dynamic Route Selection remains valid as long as the evidence supporting it remains valid. It is reopened when new evidence materially weakens an assumption behind the selected route—not every time the schedule changes by a few minutes.
Route readiness is not execution readiness.
OFX distinguishes two different readiness questions. Route-Specific Readiness asks whether the selected route is sufficiently capable and protected to support the commitment. Execution Readiness asks whether the actual assigned order can start now.
A qualified route may still be waiting for a conditioned material roll, the latest approved artwork, assigned equipment, tooling, a reference sample, or a necessary authorization. The distinction prevents an available press from becoming a reason to begin a job that is not yet ready.
Reversible preparation may proceed while an open issue is resolved, provided credible options remain protected. Irreversible activity must not consume material, capacity, order identity, or release choices before the required evidence is available.
Controlled execution and governed handoffs
The job does not end at the printing press. As rolls, sheets, or partially finished goods move through lamination, coating, cutting, folding, gluing, inspection, and packing, their identity and decision history must travel with them.
Transferring a roll to finishing is not a complete handoff if the receiving team is unaware of a pending quality condition, the applicable artwork version, a decision deadline, or a stop requirement. Governed Handoffs preserve the current commitment, accepted condition, evidence, open decisions, authorized work, and receiving ownership.
The order reaches Valid Release only after the applicable customer, quality, functional, regulatory, packing, and timing conditions are met, and the authorized release function has accepted the evidence. Physically finished production is not always validly released production.
How is the result of OFX measured?
OFX establishes how the commitment is managed. Operational Flow Effectiveness, or OFE, is the completed-order result associated with the framework. It is calculated only after the defined order-level measurement boundary has closed.
OFE does not measure a single press, and it does not convert all factory operations into a plant-wide ranking. It evaluates three distinct dimensions of the finished order:
Readiness (R) asks whether the applicable mandatory domains satisfied their required conditions by the committed readiness time.
Flow Integrity (F) asks whether the order retained a credible, connected route through the protected capacities, identities, evidence, and decision authorities needed to finish.
Release Reliability (RR) asks what share of the approved quantity reached valid release under the applicable release and protected-timing conditions.
Each component is expressed on a scale from 0 to 1. The defining relationship is:
OFE = R × F × RR
The multiplicative formulation is central: a strong result in one component cannot freely compensate for a critical failure in another.
The mathematical rationale: why multiplication instead of an average?
Assume an order has Readiness of 0.90, Flow Integrity of 0.90, and Release Reliability of 0.90. Their arithmetic average is 90%. The OFE calculation produces a different result:
OFE = 0.90 × 0.90 × 0.90 = 0.729 = 72.9%
Multiplication preserves the combined effect of weaknesses in distinct mandatory conditions. It is also zero-absorbing: if any component is zero, the result is zero. For example:
OFE = 0.95 × 0 × 1.00 = 0
However, assign zero only under the component's actual rules, not simply whenever a minor task is late. In the Readiness component, for example, a critical mandatory condition that cannot be satisfied by its required point—and has no credible protected alternative—may reduce Readiness to zero. A condition that remains open but has a protected and actionable alternative can produce a reduced, nonzero Readiness result.
Importantly, the multiplication does not establish statistical independence between the components, nor should OFE be interpreted as the mathematical probability of order success. It is a management measurement function designed to keep weaknesses visible rather than mask them through averaging. OFE must therefore always be shown with its three-component profile and the evidence behind it.
Component 1: Readiness (R)
Readiness is a retrospective completed-order result, not the same thing as the live Route-Specific Readiness decision. It records the extent to which the applicable mandatory readiness domains met their conditions at the committed readiness point. These domains depend on the actual route: they may include material, prepress, press, tooling, color, finishing, inspection, packing, and shipping.
For a simple example with equally counted applicable domains, Readiness may be expressed as:
R = Readiness domains completed on time ÷ Applicable readiness domains
Suppose an order has nine mandatory readiness domains. Eight have been satisfied at the committed readiness time. Finishing capacity remains open, but a credible alternative window, a named owner, and a decision deadline still allow the original customer commitment to be protected.
R = 8 ÷ 9 ≈ 0.89
The result is approximately 89%. But if the missing finishing condition were critical and no credible alternative remained, the order should not be portrayed as 89% ready simply because eight other checks passed. Under the framework's critical-condition rule, Readiness would be zero.
The eight-to-nine ratio is an illustrative implementation, not a universal claim that all readiness conditions carry identical importance in every plant. What matters is that the readiness evidence reflects the actual requirements of the selected route and does not conceal an unprotected critical condition.
Component 2: Flow Integrity (F)
Flow Integrity asks whether the order remained executable as one connected route. It is not just a measure of speed. A job may pass quickly through printing and still lose the protected finishing, testing, or release capacity essential to its completion.
A practical implementation can examine each mandatory resource window and use the weakest protected condition as the order's Flow Integrity result:
F = min(f₁, f₂, …, fₙ)
Here, each f term represents an evaluated protected condition for a mandatory route window, on a 0-to-1 scale. This minimum-based model is one practical implementation described by the framework; it is not a universal calculation prescribed for every factory.
Imagine that printing and coating proceed as expected, but a priority job is inserted into the die-cutting schedule, reducing the protected capacity still available to the original order. The route remains feasible, yet its weakest mandatory window retains only 90% of the required protected condition.
F = 0.90
The order may eventually be recovered, but the route exposure should not disappear merely because someone found a late solution. Managers need to distinguish between work completed through a stable flow and work completed because exceptional intervention rescued a weakened flow.
Component 3: Release Reliability (RR)
Release Reliability measures the approved quantity that reached Valid Release under the applicable customer and operational conditions. A printed, converted, or physically packed product is not counted as validly released while an applicable approval, functional test, version reconciliation, regulatory condition, or protected timing requirement remains unmet.
For a simple order with uniform units, the calculation can be expressed as:
RR = Quantity meeting all required release conditions ÷ Approved required quantity
Where an order contains lots or authorized release groups of unequal size, calculation should be quantity-weighted. Counting a large group and a small group as equal would distort the result.
Assume a 1,000-label order. Nine hundred and eighty labels pass final inspection and reach Valid Release within the protected release window. Twenty fail final inspection and require replacement. Those twenty replacement labels are eventually produced, inspected, and released, but only after the original protected release window.
The replacement quantity cannot simply disappear, and the order-level OFE cannot close while the original approved order remains unfinished. Once the replacements have achieved Valid Release, the completed-order boundary closes. In this example, the 980 labels that met the original protected-window conditions receive full credit, while the twenty recovered late do not receive that timing credit.
RR = 980 ÷ 1,000 = 0.98
Release Reliability is therefore 98%. The distinction matters: the order may eventually have all 1,000 conforming units, yet still show a weaker result under the protected operational release condition. Customer delivery timing and the internal protected release window should not be silently treated as the same boundary.
Worked example: calculating OFE for a completed label order
Consider a customer order for 1,000 paper labels with a matte-varnished finish. The selected route includes digital printing, varnishing, die cutting, inspection, packing, and authorized release.
At completion, the order evidence shows the following:
Component | Observed result | Value |
|---|---|---|
Readiness (R) | Eight of nine readiness domains met their committed condition, with a credible protected alternative for the remaining domain. | 0.89 |
Flow Integrity (F) | The weakest mandatory downstream resource window retained 90% of its protected requirement. | 0.90 |
Release Reliability (RR) | 980 of 1,000 units met the protected Valid Release window; 20 replacement units were released later but were valid. | 0.98 |
Using the rounded component values:
OFE = 0.89 × 0.90 × 0.98 = 0.78498 ≈ 78.5%
If Readiness is carried through as the unrounded fraction 8/9, the result is 78.4%; the difference is attributable solely to intermediate rounding. The managerial interpretation is unchanged.
An OFE of about 78.5% does not mean that the press ran at 78.5% efficiency, nor that 21.5% of the labels were defective. It reflects the completed-order result across three distinct exposures: Readiness before production, integrity of protected route capacity during execution, and reliable release of quantity under the agreed operational conditions.
The result is reported with its component profile:
[OFE; (R, F, RR)] = [0.785; (0.89, 0.90, 0.98)]
That profile points to practical actions: strengthen finishing Readiness, protect the die-cutting capacity window, and investigate the final-inspection rejection that required late replacement production. The score summarizes the result; the profile explains where management should investigate first.
Why the OFE number must never travel alone
Two completed orders can have exactly the same OFE result despite very different operational histories:
Measure | Order A | Order B |
|---|---|---|
Readiness | 1.00 | 0.80 |
Flow Integrity | 0.80 | 0.90 |
Release Reliability | 0.90 | 1.00 |
OFE | 0.72 | 0.72 |
In Order A, Readiness was complete, but protected route continuity weakened and release reliability fell. Management should investigate downstream capacity protection and the causes of missed release conditions. In Order B, Readiness was weaker, flow was relatively stronger, and the entire approved quantity met release requirements. Management should prioritize readiness planning rather than assume the same defect exists in both orders.
A dashboard showing "72%" for both could lead to an inappropriate generic improvement program. The profiles, supporting evidence, and original order chronology produce a more defensible response.
Where OPE fits between OEE and OFE
Between the equipment-level OEE measure and completed-order OFE, the book also uses OPE as a route-execution measure. OPE follows the selected route from the approved Execution Readiness boundary to Valid Release, without absorbing readiness failures that occurred before execution began.
OPE = Validated Route Time ÷ Consumed Route Time
Validated Route Time is the demonstrated, approved duration for the specified quantity, version structure, construction, route, required stages, and release condition. Consumed Route Time is the actual time from Execution Readiness until the applicable Valid Release condition is closed.
For illustration, if an approved route should take 12 hours but consumes 15 hours:
OPE = 12 ÷ 15 = 0.80 = 80%
OPE should preserve continuous route chronology. If production moves to another approved press or resource after execution has started, the order-level OPE clock does not restart. Each piece of equipment may begin a new local OEE record, but that does not erase elapsed route time.
OPE can exceed 100% if execution is faster than the validated standard. Such a result should prompt examination of the supporting evidence, not automatic rewriting of the standard after a single unusually good run.
Measure | Measurement boundary | Question answered |
|---|---|---|
OEE | Individual equipment in defined planned production time | How effectively did this resource perform? |
OPE | Approved execution route, from Execution Readiness to Valid Release | How effectively did the selected route execute? |
OFE | Completed customer order, including Readiness, flow integrity, and release reliability | How well did the complete order satisfy its operational commitment conditions? |
OFX is the operating methodology that governs the decisions and evidence connecting these boundaries. None of the measures should be asked to perform the role of another.
Managing change without rewriting history
Real factories do not operate under perfectly stable conditions. Quantities change, artwork versions are revised, material is delayed, finishing equipment becomes unavailable, and new evidence changes what can responsibly be done.
OFX handles those changes through Controlled Reopening. When evidence supporting a specific decision is no longer valid, only the decisions actually affected are reopened. A failed material condition may reopen Readiness and the affected execution condition. A lost finishing slot may require reconsideration of protected capacity, the customer commitment, or—if the assumptions behind the chosen route are materially weakened—Dynamic Route Selection.
Decisions whose evidence remains valid should stay closed. Equally important, the original commitment and every authorized revision must remain traceable. Moving a job to a later production slot is not the same as erasing the original delay. Updating a current schedule should not erase the operational history that made the change necessary.
This discipline lets the factory adapt without concealing what was promised, what changed, when the decision was made, or who had the legitimate authority to accept its consequences.
Can OFE be calculated before production is finished?
A live order can—and should—display its current readiness condition, route exposure, open decisions, remaining protected options, and release status. This information is valuable because it lets management act before the last credible alternative disappears.
However, a live status is not a completed-order OFE. The final result cannot be declared while the defined order-level measurement boundary remains open. Capacity may still be recovered; quality may discover a new failure; outstanding quantities may be released later; or a valid approval may remain pending.
Operational monitoring describes the order's present condition and the choices still available. OFE describes the result once the approved completed-order boundary has closed. Keeping these purposes separate prevents forecasts, temporary recoveries, or partial releases from being mistaken for finished performance.
The management value: protect commitments, not just utilization
OFX's main contribution is not another percentage on the wall. It is a change in management perspective. Instead of asking only which press is running and which is idle, the production and operations team asks which customer order is exposed, which mandatory condition is no longer protected, who must decide, and when the remaining useful option will disappear.
A press could be filled with an alternate short job to improve utilization. Yet the added changeover might cause an already committed order to lose the only viable finishing window. The local decision could improve OEE while increasing the risk to the larger system.
OFX exposes the broader consequence while a decision is still possible. It does not remove professional judgment or consolidate every authority in one role. Rather, it connects evidence, timing, legitimate authority, and customer impact so that decisions can be made responsibly.
How to implement OFX in a production facility
Implementation doesn't need to start with a large software project or a new dashboard. A practical pilot starts with one production route and a small group of representative orders: a routine job, an exposed job, and one that crosses multiple departments or shifts.
For each order, reconstruct the approved customer requirement, the original operational commitment, the selected route, its readiness criteria, and the events that affected execution. Examine whether handoffs carried the correct version, evidence, open conditions, and decision owner; whether changes were approved by the proper authorities; and whether the product reached Valid Release under the applicable conditions.
Define readiness domains, critical-condition rules, protected resource windows, release criteria, and the evidence needed to compute R, F, and RR. Preserve the original chronology rather than modifying it after the outcome is known. Calculate OFE only after the order has closed and the measurement logic is stable enough to make the result meaningful.
The value comes from targeted Learning. If repeated orders lose finishing slots, investigate protection of downstream capacity—not just speed. If late file approvals prevent Readiness, improve prepress approval and decision deadlines. If the largest losses occur during final release, investigate inspection evidence, release authority, and the causes of rework.
After a pilot has survived real operating conditions, expand it to another production route. Prospective Learning should improve future standards and rules, but must not retrospectively clean up legitimate historical results. A later recovery is not proof that the original exposure never existed.
The questions production managers should ask each morning.
A useful daily review should extend beyond yesterday's equipment dashboard. What did we actually promise? Which requirement is no longer secure? What decision must be made next? Which credible option will disappear first, and when? Who has authority to make that decision? What evidence is still missing? Which preparation may safely continue, and where must work stop?
These questions do not require a premature OFE score for every live order. They require a plant to preserve its operational commitment, current decision state, and remaining options. Once those are visible, managers can act not only on the output already achieved, but on the commitments that still need protection.
Conclusion: operational excellence does not end at the press
Industrial plants need efficiency measures. OEE provides essential equipment information; OPE extends measurement through the approved production route. Yet neither, by itself, establishes whether the factory fulfilled the complete customer commitment.
OFX widens the management boundary to the full order lifecycle, connecting customer requirements, Readiness, protected capacity, decisions, execution, handoffs, and Valid Release. OFE provides a structured, quantitative view of the completed order through Readiness, Flow Integrity, and Release Reliability.
The multiplicative result is not a substitute for production managers' or industrial engineers' expertise. It exposes systemic weaknesses that would otherwise be hidden behind strong local numbers. The model's value lies in reading the total alongside the evidence-rich profile that produced it.
A highly efficient press is an important asset. But customers do not buy machine efficiency. They buy a product that meets the approved requirements, with reliable delivery under the conditions the factory agreed to accept.
Operational excellence begins when the plant stops measuring only how well its individual parts work and also manages how reliably the entire system keeps its promise to the customer.
About the development of the methodology
Operational Flow Excellence (OFX) and its accompanying measurement model, Operational Flow Effectiveness (OFE), were developed by Ronen Dolev through the combination of his education in Industrial Engineering and Management and his earlier professional experience in operations management and the printing and packaging industry.
Engineering knowledge in operations research, production planning, capacity management, process analysis, and performance measurement, together with practical experience managing manufacturing operations, provided the foundation for a systems-oriented approach to operational excellence.
The development sought to address the gap between local efficiency in machines and departments and a plant's ability to fulfill its complete commitment to the customer. It established a framework linking Readiness, operational flow integrity, evidence-based decisions, and authorized release of the finished product.
The methodology and its mathematical model are presented in Dolev's 2026 book, When Efficiency Becomes Excellence: Operational Excellence in Industrial Printing.
Source and methodological note
Ronen Dolev, When Efficiency Becomes Excellence: Operational Excellence in Industrial Printing (2026), especially Chapters 10–15 and Appendix A, "OFX and OFE in Practice."
OFX and OFE are presented as the author's original conceptual and explanatory framework and completed-order measurement model. They are not described here as internationally standardized metrics or as replacements for established equipment measures. Numerical examples illustrate the book's operating logic; industrial implementation requires route-specific definitions, evidence rules, qualified authority, and validation under actual plant conditions.