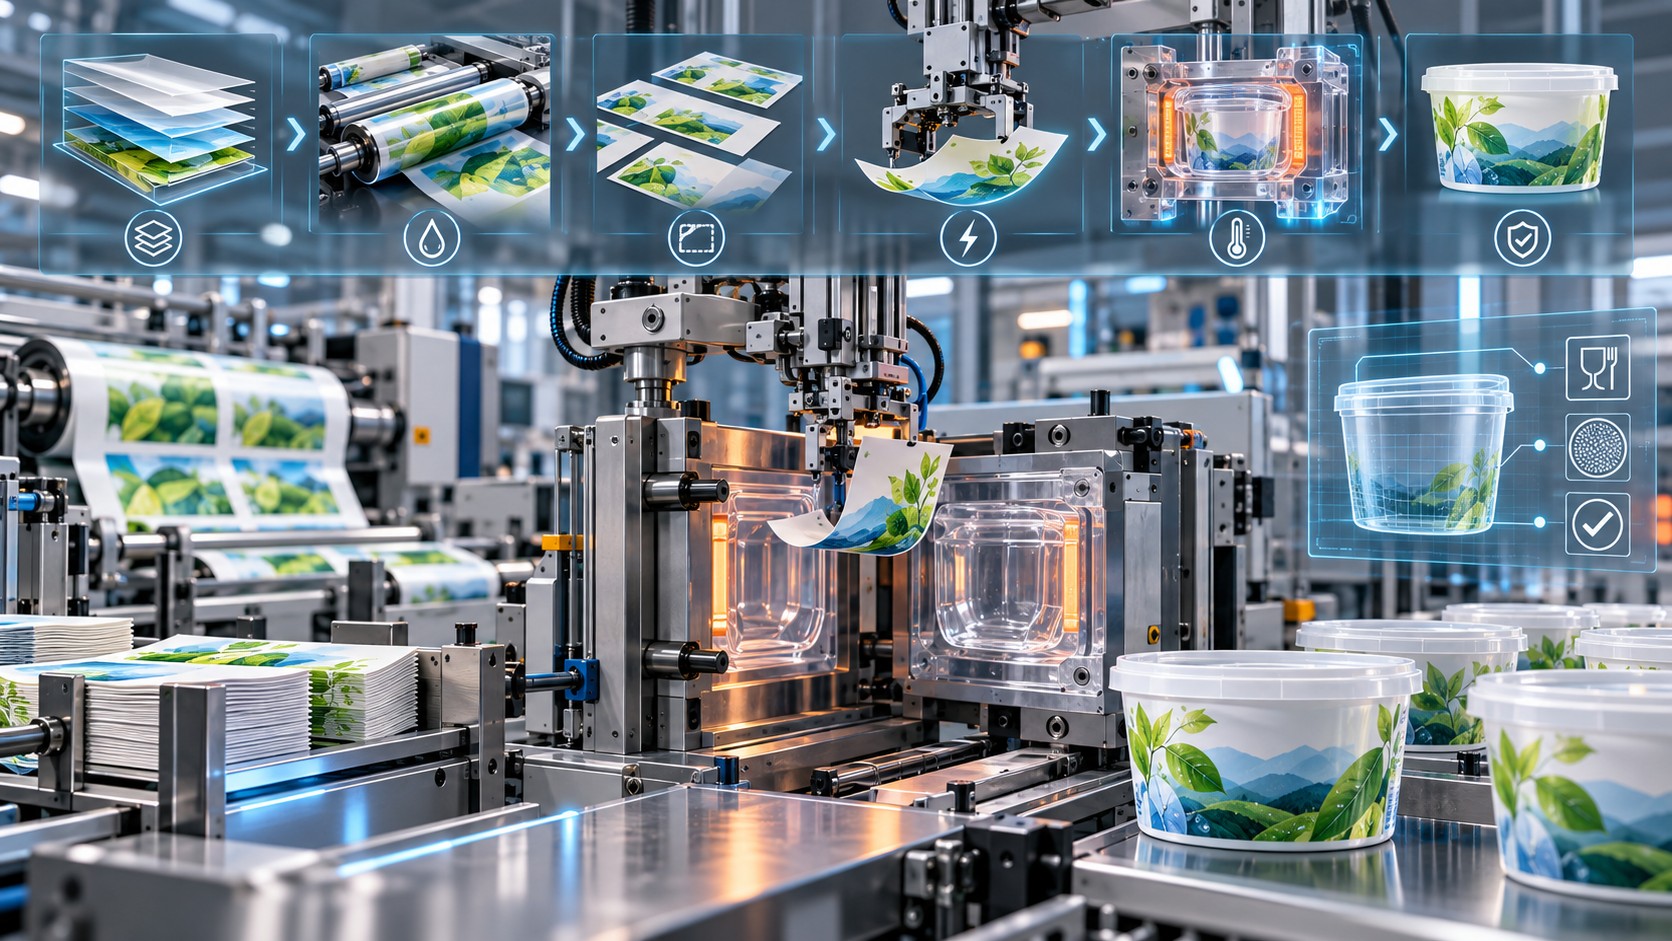
A label that is created together with the product
A tub of ice cream, a dairy container, or a bottle of household detergent may carry graphics that seem to belong to the plastic itself. There is no visible paper edge and no obvious separately applied sticker. In many such products, the graphic is integrated into the container during manufacturing. This is the principle of In-Mold Labeling (IML).
Unlike a pressure-sensitive label applied after a package has been made, an in-mold label is positioned inside a mold before the plastic part is formed. The molding material then meets the back of the label, and, under appropriate processing conditions, a permanent bond develops between the label's compatible polymer surface and the container. After cooling and demolding, the printed decoration forms an integral part of the finished article.
The apparent simplicity of the finished surface conceals a demanding production sequence. The label must print accurately, tolerate coating and converting, remain flat after die-cutting, separate individually from a stack, travel reliably through robotic feeding, and remain precisely positioned in the mold. It must also tolerate the thermal and mechanical loads of molding without ink washout, distortion or damage to its protective coating.
For food packaging, a further requirement is critical: every component and every possible route of chemical transfer must be considered in the food-contact assessment. A technically excellent print is not a qualified IML application until the complete container has passed the relevant functional and regulatory tests.
What IML is and where it is used
IML is an approach to decorating molded plastic articles in which a preprinted label is integrated during the molding cycle. Its applications extend beyond retail food containers. Injection-molded tubs and lids for yogurt, ice cream, cheese, spreads, and other refrigerated foods are familiar examples. In personal care and household chemicals, IML may appear on bottles and containers for shampoo, cleaning liquids, and detergents. Durable products include storage boxes, cases, toys, sporting goods and selected industrial components.
The term In-Mold Decoration (IMD) is also used, particularly for decorative layers incorporated into long-life plastic articles. Although the terminology overlaps, IML commonly refers to a label integrated into a container, while IMD is often used for broader decoration of durable molded components.
The benefit is not merely visual. Integrating decoration into molding can eliminate a separate post-molding labeling operation. With the correct materials, the finished graphic can withstand moisture, handling, friction, and the chemicals relevant to its intended use. These advantages come with a trade-off: a failed label can interrupt the molding machine itself. Consequently, the converter and the plastic molder must develop the construction together.
IML, pressure-sensitive labels and shrink sleeves
All three methods can give a product a decorated appearance, but their attachment mechanisms and manufacturing responsibilities differ.
Characteristic | In-Mold Labeling | Pressure-Sensitive Label | Shrink Sleeve |
|---|---|---|---|
Application stage | During plastic molding | After the container is made | After the container is made |
Attachment | Thermal integration with a compatible plastic surface | Pressure-sensitive adhesive | Thermal shrink fit around the package |
Typical equipment | Mold, feeding robot, and molding machine | Label applicator | Sleeve applicator and shrink tunnel |
Main functional demands | Flatness, handling, heat resistance and resin compatibility | Adhesive and container-surface compatibility | Controlled shrinkage and shape conformance |
Visual potential | Integrated, nearly seamless decoration | Defined label boundary | Extensive wraparound coverage |
No single method is superior for every application. IML is especially attractive when the decorated article is produced repeatedly in a controlled molding system. A separate applied label may remain preferable when identical undecorated containers need frequent label changes after manufacture. Shrink sleeves may be chosen when extensive wraparound coverage and complex container profiles are priorities.
Three molding routes, three different thermal environments
In-mold labels are used in injection molding, blow molding, and selected thermoforming processes. The common principle is placing the decoration before or during shaping, but material flow, heat-transfer mechanisms, and label-retention methods vary significantly.
Molding process | How the part is formed | Typical IML applications | Engineering priority |
|---|---|---|---|
Injection molding | Molten polymer is injected into a closed mold | Cups, tubs, lids and rigid components | Gate-region heat and pressure, label retention, thin-wall stability |
Blow molding | Heated polymer is expanded against the mold by air pressure | Bottles and hollow containers | Label placement, vacuum retention and compatibility with the parison |
Thermoforming | A heated polymer sheet is shaped by vacuum, pressure, or tooling | Cups, trays and thin-walled containers | Bond formation under a different, often lower, interface heat budget |
A label qualified for one route cannot automatically be transferred to another. Even with polypropylene-based articles, the temperature delivered to the label's bonding layer, the duration of contact, and the shape change can differ significantly.
The end-to-end IML manufacturing chain
IML production usually involves a polymer film supplier, a printer or label converter, a plastic molding plant and, where relevant, the food or consumer-goods filling plant. A single integrated producer may perform several stages, but the technical interfaces remain the same.
The sequence begins with article geometry, mold design and label specifications. The manufacturer produces suitable film and prepares it for printing. The converter then prints the artwork, applies functional protection, dries or cures all layers, die-cuts the individual labels, and stacks or otherwise prepares them for automation. At the molding plant, a robot or dedicated feed system transfers each label to the mold. The article is molded, cooled, and removed with the decoration integrated. The final part proceeds to inspection and, for consumer packaging, filling, sealing and distribution.
This sequence makes an important point: press quality and print registration are necessary but insufficient. A label can leave the printing press in perfect condition and still fail in the magazine, at robotic pickup, against the mold wall or at the polymer-to-label interface.
The label is a multilayer engineered structure.
A typical surface-printed IML construction includes a polymer film with a print-receptive surface, a primer when required, ink layers, and a protective overprint varnish. The film's opposite surface is selected or engineered to bond with the material molded against it. Unlike a pressure-sensitive label, no release liner normally supports each die-cut piece during molding.
Each layer has a distinct job. The outermost varnish must protect the artwork and may also control friction and electrical charging behavior. The ink must retain color and cohesion during the molding cycle. Where needed, the primer must keep the ink bonded to the polymer. The film provides stiffness, dimensional behavior, and compatibility with the container resin. A specially designed bonding skin may be needed where the available molding temperature is insufficient for a conventional film.
Surface printing protected by a suitable varnish is common. Other constructions may use reverse printing on a clear film and additional protective lamination, especially where extraordinary durability is required. Such constructions add interfaces, thickness, cost, and the risk of heat-related lamination defects; therefore, select them for a defined performance requirement rather than assuming they are universally better.
Selecting the label film: compatibility comes first
The film and the container should have a compatible bonding interface. Polypropylene labels are common for polypropylene food containers, while polyethylene-based container applications require their own suitable label construction. Products made from polystyrene, ABS, polycarbonate, or polyester may require different engineered films or functional layers.
Chemical similarity helps but does not guarantee bonding. The interface must also encounter sufficient temperature, pressure, and contact time. The molding cycle must fuse the materials without damaging the image or distorting the part. The film supplier, converter and molder therefore need a shared specification, including resin grade, film orientation, thickness, surface treatments, storage conditions and required molded-part performance.
The same-material concept can also support recyclability. A PP container with a compatible PP label may simplify material separation compared with some multi-polymer decorations. Nevertheless, recyclability of the finished article still depends on pigments, coatings, additives, sorting performance and the available collection and recycling systems.
Cavitated BOPP, solid-core BOPP and CPP
Three important film families are cavitated biaxially oriented polypropylene (BOPP), solid-core BOPP and cast polypropylene (CPP). They differ in internal structure, density, processing behavior and final appearance.
Cavitated BOPP contains small internal voids produced during film manufacture. These voids reduce density and can affect stiffness, thermal behavior, and the visual texture after molding. Solid-core BOPP has a comparatively continuous, dense structure and can be selected for smooth, white or transparent finishes. CPP is cast rather than biaxially oriented to the same extent; consequently, its elasticity and thermal behavior are different.
Property | Cavitated BOPP | Solid-Core BOPP | CPP |
|---|---|---|---|
Structure | Oriented film with internal voids | Dense oriented film | Cast polypropylene film |
Relative density | Typically lower | Higher | Generally relatively high |
Surface appearance | Can produce a matte or orange-peel texture | Can be smooth or glossy, white or clear | Depends on the film grade |
Converting response | Grade-dependent balance of stiffness and die-cutting behavior | Good die-cutting behavior in suitable grades | Greater elasticity may complicate die-cutting |
Molding response | Voids may help moderate shrinkage and thermal stresses | Residual orientation can affect shrinkage | Different thermal stability and softening behavior |
Best selection criterion | Thin-wall stability and desired texture | Smooth appearance, size, and stiffness needs | Specific bonding and forming requirements |
Descriptions such as 'cavitated' or 'solid core' do not define a universal performance ranking. Two films of similar density can behave differently because of skin-layer chemistry, void distribution, and orientation history. The finished molded article, not the film category alone, determines suitability.
Thickness, density and stiffness
Many IML films fall in approximate ranges from 40 to 120 micrometers, although applications outside that span exist. Some injection-molded food containers use films around 40-70 micrometers. Larger labels and certain blow-molded articles may use thicker constructions, often around 80-120 micrometers. These ranges are development references, not acceptance standards.
A thicker film may be easier to manipulate mechanically, especially when labels are large and unsupported by a liner. Yet extra thickness can increase residual stress and, in a thin-walled container, may contribute to warping or poor shape retention. Likewise, density affects both material consumption and visual texture; it cannot be considered independently of film structure.
The proper specification should therefore address thickness tolerance, stiffness, shrinkage behavior, density, flatness and compatibility with the selected mold and robotic handling system.
Designing for the actual mold geometry
The mold defines the label's final job. A round lid label, a conical body label and a broad rectangular panel label experience very different geometry and material movement. Artwork design must therefore be based on a production-approved dieline and mold drawing, not on an isolated graphic rectangle.
Label edges should avoid locations where folding, rapid material displacement, or tool geometry may compromise flatness and adhesion. Leave sufficient area for vacuum cups or other pickup tools. For conical or multi-panel labels, the developed shape must match the final article without forcing the film into wrinkles or excessive in-plane strain.
Print coverage is also relevant. Abrupt transitions between heavily printed regions and almost unprinted regions can create uneven layer thickness and local stress. After die-cutting, those stresses may contribute to curling. Graphic balancing may therefore form part of an engineering solution, provided the additional ink does not produce new thermal or mechanical problems.
The injection gate: a high-load local region
In injection molding, the gate is the entry point through which molten polymer reaches the cavity. Local flow, pressure, and heat conditions near that point can differ from those across the rest of the part. Where a printed label covers the gate area, the graphic can be exposed to a more severe short-duration thermal and mechanical event.
Possible symptoms include ink displacement, color change, or localized washout. The polymer melt may be processed at temperatures of roughly 200-250 °C in some applications, but that figure must not be confused with the temperature reached by the ink. The mold is cooled, the film provides thermal resistance, and the actual exposure depends on time, flow geometry, and material properties.
The gate should be considered during artwork planning. Avoid fine text and delicate graphics in high-stress regions when the design permits. Ink coverage, polymer film structure, primer, and protective coating should be assessed together. If the part requires artwork directly over the gate, validation must include that exact region of the molded article.
Surface preparation: corona without overtreatment
Polyolefin films have relatively low surface energy and may require treatment to achieve appropriate wetting by a primer or ink. Corona treatment can modify the surface and improve initial wettability. Films frequently arrive with an extrusion-stage treatment, so subsequent production may require only controlled refreshing rather than aggressive treatment.
Excessive corona exposure is not a universal route to stronger adhesion. Depending on film and coating chemistry, overtreatment can contribute to undesirable surface changes and reduced durability, including after humidity exposure. The practical target is sufficient wetting and adhesion with the lowest process intensity that delivers reliable performance.
The printing side and the molding side of an IML film may have different surface functions. A treatment beneficial to printing must not automatically be transferred to the bonding side. Testing should confirm each interface in its intended role.
Primer chemistry and coat weight
A primer acts as an engineered interface between the polymer film and the ink when the selected printing system requires it. In IML, the primer must maintain adhesion through subsequent varnishing, die-cutting and molding rather than passing only an immediate press-side adhesion test.
Primer chemistry, corona treatment, dry coat weight, dryer efficiency and web tension all influence the result. A high coat weight does not necessarily improve performance. Excess primer may create more drying work, blocking risk, or stress within the thin unsupported label. Too little primer, or nonuniform coverage, may leave local areas of weak ink adhesion.
The optimum condition is the minimum controlled layer that provides the necessary coverage and bond strength for the qualified film and ink system. Offline-coated films also require control of primer aging and storage time before printing; performance may change as the treated or coated surface ages.
Drying primers without destabilizing the film
Water-based primers require sufficient water removal and proper film formation before the next operation. BOPP films can be sensitive to the combined effects of dryer temperature and web tension. Higher heat may accelerate evaporation but can also alter film dimensions and residual stresses; high rewind tension can worsen distortion and blocking.
In suitable systems, increased airflow and effective drying design can reduce the need for excessive web temperature. The correct balance depends on film thickness, primer formulation, and equipment. Verification should include primer adhesion, residual moisture or drying performance (as appropriate), film flatness, and dimensional stability.
Static discharge equipment should also be considered throughout film handling. Uncontrolled charge can interfere with coating quality, stacking and later robotic separation.
Printing: several technologies, one functional requirement
IML artwork may be produced using offset, flexography, gravure or compatible digital technologies, including liquid electrophotography (LEP). The selection depends on order length, image quality, substrate dimensions, variability and the available converting process. No printing technology alone makes an IML construction suitable for molding.
The printing system must deliver accurate color and stable ink adhesion while preserving the film's dimensions. Drying or curing must be sufficient before rewinding or coating. With UV-curable systems, the energy delivered, exposure time, spectral compatibility, and ink-film thickness determine the degree of cure. With systems using volatile carriers, validate the drying conditions and the ink's final state.
Color should ultimately be assessed on the molded article when molding or coating changes its appearance. A press-side pass in color measurement is useful process control, not an automatic qualification of the final package.
Repeat length, scaling and web tension
In roll-fed printing, the repeat length determines the relationship between one printed image and the next. Later die-cutting uses that repeat to align the tool with the graphic. Heat, tension, and the film's residual orientation can cause the actual repeat to differ from the artwork target.
The converter should establish a film-specific scaling profile and include suitable registration marks. A persistent uniform offset may be corrected through process calibration; a variable distortion over the roll may indicate a more fundamental tension or thermal stability problem.
Tension should be controlled at the unwind, printing, coating, and rewind stages. More tension can sometimes improve local transport stability, but it may also elongate film and store stress. In IML, the eventual die-cut label is unsupported, so excessive rewinding and drying stresses may emerge as curling only after the label has been separated from the web.
Surface printing, reverse printing and protective lamination
Surface-printed IML labels are commonly protected with a functional overprint varnish. The construction is comparatively straightforward and can provide the necessary abrasion, moisture and chemical resistance if all layers are appropriately selected and cured.
For selected durable applications, consider reverse printing on a clear film followed by protective lamination. This can protect the image behind a polymer layer, but the added film and adhesive create additional interfaces and thermal stresses. Under the molding conditions, the lamination bond must survive without bubbles, local delamination, or image distortion.
The choice should follow performance requirements. A well-qualified surface-printed construction is often preferable to unnecessary lamination complexity when it already meets the application's durability target.
The overprint varnish is a functional machine-interface layer
An IML varnish does more than change gloss. It protects the ink against scratches and rubbing during converting, transport, and consumer use. It also influences the friction between labels in the stack and may be engineered to support controlled electrostatic charging and release inside the mold.
The varnish must combine abrasion resistance, thermal resistance, flexibility, appropriate coefficient of friction (COF), and electrostatic properties suited to the molding system. A varnish developed only for conventional self-adhesive labels may fail one of these additional requirements.
Coating weight is particularly important. More coating can improve some protective properties but also increases film stress and the potential for curling after cure. Both inadequate cure and excessive brittleness can lead to problems. UV-curable and water-based varnishes should therefore be assessed as complete film/ink/coating systems, not by chemistry alone.
Coefficient of friction and single-label feeding
After converting, cut labels are usually collected in stacks. The molding machine then has to extract one label at a time. Excessive interlabel friction can disrupt feeding or promote double-picking. Inappropriate surface properties can also interfere with vacuum pickup and precise positioning.
Some IML systems work with indicative COF values around 0.15-0.20, but no universal target applies to all robots, labels, and mold geometries. COF must be measured under defined conditions on the fully finished and conditioned label. It should be evaluated alongside blocking resistance, electrostatic behavior, and feeder performance.
A low value alone does not guarantee successful feeding. The labels must also lie sufficiently flat and separate consistently from the magazine.
Static electricity: discharge first, charge later
Static control has a distinctive dual role in IML. During printing, coating, cutting, and stacking, uncontrolled static charge is undesirable because it can make labels cling together, promote double-picking, and complicate accurate feeding. Active or passive discharge stations may be needed along the process.
In some injection-molding installations, the robot deliberately charges an individual label after pickup. The controlled charge helps hold the label against the mold wall until polymer injection begins. In other systems, particularly some blow-molding setups, vacuum features in the mold perform the primary retention function.
These are not contradictory requirements. The process needs a predictable electrostatic state at each location: neutralization for reliable separation, followed by deliberate retention where the selected molding equipment needs it. Coating choice can materially affect both operations.
Varnish drying and curing: durability without curling
Water-based varnishes rely on water removal and coating-film development. UV varnishes rely on a photochemical curing reaction. Both must reach their specified condition before converting and stacking, but the mechanisms are not interchangeable.
Excessive dry coat weight can amplify the stress imbalance between the top and bottom of a thin film. UV cure shrinkage or an overly rigid coating may cause curling, tubing, or cracking. Conversely, insufficient cure can create tackiness, blocking, weak scratch resistance, or mold release problems. A cooling roller after UV exposure may help limit the thermal load on sensitive films.
A fingertip surface check can identify obvious tackiness but cannot prove complete cure or low migration. Functional validation should include abrasion, adhesion, flexibility, flatness and, for food packaging, relevant chemical risk assessment. Coating conditions should be qualified jointly with printing and molding requirements.
Die-cutting: when the unsupported label is created
After printing and finishing, the web is converted into individual labels. Rotary or semi-rotary die-cutting is common, although other technologies may be suitable. The cut must match the mold geometry while producing clean, consistent edges free from unwanted tabs and distortion.
A crucial transformation happens at this stage. As part of a continuous web, film stress can be distributed over a larger area. After die-cutting, each label becomes an unsupported part. Differences in shrinkage or tension among the film, primer, ink, and varnish can then show up as curling or tubing.
Flatness is therefore not simply a cosmetic attribute. A curled label may fail vacuum pickup, rotate in the feeder, enter the cavity inaccurately or shift before molding. A good die-cutting result includes shape accuracy, edge quality, and stable lay-flat behavior after the coatings have fully developed their final properties.
Cut-and-stack and cut-in-place
In a conventional cut-and-stack workflow, labels are cut at the converting plant and collected in prepared stacks. These stacks travel to the molder, where automated magazine feeding and robotic pick-and-place deliver labels to the tool. The process requires stable dimensions, controlled static charge, suitable friction, and resistance to blocking during storage and shipment.
In a cut-in-place approach, cutting occurs close to or within the molding automation rather than at a remote converting stage. This can shorten handling and reduce some intermediate operations, but requires a closely integrated control architecture and synchronization with the molding cycle. Neither approach removes the need to qualify film flatness and surface behavior.
Injection molding: fusion inside the mold
For injection molding, a cut label is picked from the magazine and positioned inside the cavity, often using controlled electrostatic retention. The mold closes, and molten resin fills the part geometry. At the interface with the label's compatible reverse surface, the thermal and pressure history must be sufficient to form a stable bond. The article then cools and is removed with the decoration integrated.
Local conditions vary widely within the cavity, especially near the gate. The film and coating system must therefore be validated on the molded article, not only against a nominal resin processing temperature. Suitable measurements include label position, edge adhesion, gate-region image integrity, warpage and functional resistance after environmental exposure.
Blow molding: the label inside a hollow article
In extrusion blow molding, a label is positioned against the mold wall, typically held in place by vacuum. A hot polymer parison enters the mold, the mold closes, and internal air pressure expands the polymer outward. The expanding material contacts the label, and the compatible surfaces fuse under the specified thermal history.
Large bottle labels place strong demands on stiffness, shape consistency, and robot handling. The film must also tolerate the curved mold surface and the timing of the parison expansion. For some applications, a thicker or different film construction is preferable to a thin injection-grade label. The right solution depends on the bottle geometry, resin, and molding process.
Thermoforming: bond formation at a different heat budget
Thermoforming starts with a heated sheet or web rather than an injected polymer melt or a blow-molded parison. Vacuum, air pressure, or tooling forms the material into a cavity. The pre-positioned IML label must bond under the available contact temperature and time.
That interface heat budget may be lower than in injection molding. Consequently, a conventional injection-mold IML film may fail to bond even though both parts are polypropylene-based. Dedicated thermoforming-compatible multilayer films can use a lower-softening bonding skin to create the required connection. The engineered skin, forming sheet, and process window must be qualified as a system.
Food-contact safety: migration and all set-off routes
Many IML applications hold food, so chemical compatibility must be evaluated for the finished container. Surface-printed ink is not necessarily in intended direct contact with food, but that fact alone is not a complete risk assessment. Potential migration through the label and container wall must be considered under the relevant food type, time, and temperature conditions.
Set-off creates additional possible transfer routes. During roll winding, the printed face can contact the reverse film surface. After die-cutting, stacked labels may place the varnished image against the bonding side of adjacent labels. Importantly, completed cups and tubs are frequently nested together: the external printed surface of one article can contact the internal food-contact surface of the next. In some applications, this finished-container nesting is one of the most important stages to examine.
Set-off may be chemical without visible color transfer. Therefore, a clean appearance cannot be used as evidence that unwanted constituents did not transfer. The risk assessment must consider printing materials, coatings, resin layers, stack pressure, contact time, storage temperature, and subsequent food use.
Low migration, UV cure and NIAS
Low-migration inks and varnishes are formulated to limit the potential transfer of constituents. The designation does not mean all mobile substances are absent, nor does it automatically approve the finished packaging for every food-contact condition.
For UV systems, cure efficiency and relevant residual species require attention. Potential migrants may include certain unreacted formulation constituents, photoinitiator-related components and reaction or degradation products. Non-Intentionally Added Substances (NIAS) may also need assessment, depending on the system.
Selection should be supported by supplier information, a documented risk assessment and appropriate analytical testing where needed. Validation must consider the actual final structure, including the molded polymer wall and the mechanical contact conditions during nesting and storage.
HACCP, ISO 22000 and FSSC 22000
Food packaging manufacture benefits from a systematic hazard-management approach. HACCP identifies and evaluates biological, chemical and physical hazards and determines the measures required to control them. In IML production, potential hazards can include chemical migration, unintended set-off, contamination, foreign material and failures that compromise container integrity.
Not every printing, coating, or molding parameter is automatically a Critical Control Point (CCP). Control measures and the classification of critical points must follow a documented hazard analysis. ISO 22000 establishes a framework for a food safety management system across the food chain. FSSC 22000 combines ISO 22000 with applicable prerequisite programs and additional scheme requirements; packaging-related prerequisite standards include the relevant parts of the ISO 22002 series.
These management systems complement, but do not replace, the legal food-contact obligations for the packaging structure itself. They help organize controls and evidence, while migration limits and material compliance must still be evaluated separately.
Food-contact regulations and end-product qualification
For the European Union, Regulation (EC) No 1935/2004 provides the general framework for materials intended to contact food. Regulation (EC) No 2023/2006 addresses good manufacturing practice, including preventing unacceptable transfer from printed surfaces. Regulation (EU) No 10/2011, as amended, covers relevant plastic food-contact materials and layers within its scope, including applicable migration and composition provisions.
The regulatory status of each constituent is not interchangeable. Ink, primer, varnish, label film, and molded resin may be governed by different requirements or guidance, depending on their position and intended function. In the United States, the relevant FDA provisions should be evaluated for each material and the expected conditions of food contact.
Final suitability is demonstrated for the defined construction, food category and use scenario. An individual supplier declaration or a 'low migration' label does not substitute for assessment of the completed article.
Recyclability and compatible polymer design
When both container and integrated label belong to the same compatible polymer family, separation demands may be lower than in multi-material packaging. This is a useful design-for-recycling opportunity, especially for polypropylene-based containers and labels.
Still, recyclability depends on more than the headline resin. Coatings, pigments, density, closures, additives, sorting systems and locally available recycling processes can all influence whether an article is successfully recycled. Claims should be supported by an evaluation of the completed package and the intended regional collection and treatment routes.
Quality assurance throughout the process
A reliable IML qualification program is stage-specific. Film and print tests cannot substitute for label feeding tests, and successful molding does not replace food-contact assessment. The finished container must be evaluated after the same heating, cooling, handling, and storage events it will experience in production.
Stage | Principal checks | Intended outcome |
|---|---|---|
Raw film | Thickness, density, orientation, dimensional stability | Compatible film for printing and molding |
Surface preparation | Wetting, primer uniformity, adhesion | Reliable ink-film interface |
Printing | Color, registration, repeat length, ink cohesion | Consistent decorated web |
Varnishing | Cure/dry state, COF, abrasion, flexibility | Durable and feedable surface |
Die-cutting | Dimensions, edges, lay-flat behavior | Clean, robot-ready labels |
Stacking | Blocking, electrostatic state, single-pick repeatability | Stable magazine feeding |
Molding | Placement, bond, gate region, release, warpage | Integrated decorated article |
Finished use | Moisture, chemicals, freeze, dishwasher or other defined conditions | Functional service-life performance |
Food packaging | Migration, NIAS and set-off assessment | Food-contact qualification |
The acceptance limits must be defined for each application. For example, a lay-flat criterion appropriate for a small lid label may not suit a much larger bottle label. Repeatability across production batches matters as much as a successful initial sample.
Practical durability testing on the finished container
Tape or peel evaluations can help locate weak interfaces, but results require interpretation. Very low-COF coatings can prevent test tape from bonding properly and produce misleading outcomes. Alternative adhesion and abrasion tests may be necessary when the coating surface is deliberately engineered to release easily.
Tests may include scratch resistance, controlled abrasion, crease or crinkle tests, immersion in water, freezer conditioning and exposure to the actual packed product or representative chemicals. Reusable articles may also require defined dishwasher cycling. Microwave suitability, where intended, needs its own validation and must not be inferred from water or dishwasher performance.
Molded-container nesting, handling and shipping should also be reproduced where relevant. Mechanical performance, appearance and food-contact risks should all be reviewed after representative conditioning rather than only immediately after molding.
Troubleshooting: when a correctly printed label fails later
IML problems often become visible after printing, where several material interfaces and machines interact. Troubleshooting should identify both the stage at which a defect appears and the physical mechanism responsible, rather than changing ink, varnish, or molding temperature at random.
Symptom | Potential mechanism | Focused investigation |
|---|---|---|
Curling or tubing after die-cutting | Residual film stress, differential layer shrinkage, high coat weight or web tension | Film construction, varnish cure, coat weight and tension history |
Double-picking from a stack | Static, blocking or unsuitable COF | Static neutralization, coating surface and separation performance |
Label shifts in the mold | Inadequate electrostatic or vacuum retention, or curl | Robot placement, mold retention method and label flatness |
Ink washout near the gate | Localized thermal and flow stress | Gate design, ink coverage, film insulation and injection profile |
Poor label-to-container adhesion | Polymer incompatibility, low interface heat or reverse-side contamination | Bonding skin, resin grade, set-off and contact conditions |
Varnish sticks to the mold | Inadequate cure, coating mismatch or unsuitable mold conditions | Cure validation, mold cleanliness, temperature and release behavior |
Blocking in a wound roll | Incomplete drying or curing, excessive rewind pressure | Drying performance, coating development and web tension |
Color change after molding | Thermal, optical or chemical changes | Measurements before and after molding at critical areas |
Thin-wall part warps | Differential shrinkage or a film too stiff for the wall | Label thickness, cavitation, wall geometry and cooling |
Food-contact result fails | Migration or set-off in the manufacturing chain | Source identification and assessment of the finished structure |
A curled label may lead to pickup failure even if the printer produced perfect registration. The correct investigation therefore starts with film stress, coating balance and the history of drying and winding, not automatically with the printing press.
Likewise, a white or discolored area near the injection gate may be related to a localized flow-and-temperature event. Adjusting molding parameters, reducing sensitive coverage at the gate, or selecting a different film structure may be appropriate, but any change must preserve container filling, bonding, and dimensional integrity.
When adhesion between label and container fails, the interface should be examined directly. The polymer grades may not be compatible; the bonding layer may not reach the required state; or contaminants from primer, ink or varnish may have transferred to the reverse side during winding or stacking. Raising temperature alone will not resolve every one of these mechanisms, and can create a new image or part-quality problem.
Conclusion: the label and the container are engineered as one
In-Mold Labeling joins printing engineering to polymer processing more directly than many other decoration technologies. The printing press creates the image, but film selection, functional coating, electrostatic control, cutting, robotic handling, and molding determine whether that image becomes a reliable part of the product.
The film must match the polymer and process. Primer and ink must maintain a stable interface. Varnish must balance protection, friction, electrostatic behavior and flexibility. The individual label must remain flat after cutting and enter the mold in the exact intended position. The resin must then form an adequate bond without destroying the image or distorting the article. Where the finished container holds food, the construction must also satisfy the applicable safety assessment for migration and set-off.
The real qualification takes place on the finished container, after all relevant manufacturing and use conditions have been represented. Excellent press output remains important, but it is only one stage of a complete industrial application.
The printing press produces the graphic. Polymer engineering, coatings, and molding make that graphic part of the container.
In IML, the label is not added after the product has been made. It is created together with it.
Standards and regulatory frameworks
- ISO 4593:1993 — Plastics: Film and sheeting — Determination of thickness by mechanical scanning.
- ISO 8295:1995 — Plastics: Film and sheeting — Determination of the coefficients of friction.
- ISO 8296:2003 — Plastics: Film and sheeting — Determination of wetting tension.
- ISO 11501:1995 — Plastics: Film and sheeting — Determination of dimensional change on heating.
- ISO 11502:2018 — Plastics: Film and sheeting — Determination of blocking resistance.
- Regulation (EC) No 1935/2004 — General European requirements for materials and articles intended to come into contact with food.
- Regulation (EC) No 2023/2006 — Good manufacturing practice for food-contact materials and articles.
- Regulation (EU) No 10/2011, as amended — Requirements for plastic food-contact materials and articles within its scope, including applicable composition and migration provisions.
- Codex Alimentarius CXC 1-1969 — General Principles of Food Hygiene and HACCP principles.
- ISO 22000:2018, as amended — Food safety management systems.
- ISO 22002-100:2025 and ISO 22002-4:2025 — Prerequisite programs, including the food packaging manufacturing sector.
- FSSC 22000 — Food safety system certification scheme, subject to the current scheme version and sector requirements.
Standards provide defined measurement methods and management frameworks, but they do not establish one universal acceptance limit for all IML constructions. Each film, printing system, coating, mold, resin, and finished container must be qualified against its intended application and market requirements.