By Ronen Dolev | 2026
Introduction — When Print Quality Extends Beyond the Human Eye
Production speed, graphic complexity, and demand for consistent quality have transformed how printing companies monitor their processes. Modern web-fed and sheetfed presses can produce substantial volumes quickly, combining complex color imagery, microtext, barcodes, variable data, varnishes, and functional coatings on the same product.
Yet an operator's ability to identify defects through direct observation remains limited. As production speed increases, registration errors, spots, scratches, missing text, and coating irregularities may pass the inspection point before they can be recognized. Some defects appear only on one sheet in a long run; others emerge intermittently on a printed web or immediately after a temporary change in production conditions. In other cases, a defect already exists at the printing stage but is not discovered until after lamination, slitting, die-cutting, folding, gluing, or pouch making, when corrective action is considerably more expensive.
Machine-vision systems address this gap by combining industrial cameras, controlled illumination, image processing, automated anomaly detection, and digital records. Their engineering value, however, is not simply detecting a difference between two images. It is the ability to connect an observed defect to its location, severity, possible origin, and the action required to prevent a nonconforming product from reaching the customer.
This distinction matters most in three production environments: continuously moving webs, individually transported sheets, and varnish or coating applications, where a defect may be nearly invisible under ordinary lighting. This article examines the engineering principles, application-specific challenges, capabilities, and limitations of automated inspection, and explains how image acquisition can become a reliable part of industrial quality assurance.
- From Visual Monitoring to Automated Print Inspection
Printing operations have historically relied on sampling, direct observation, and magnified camera views. On web presses, cameras synchronized to the graphic repeat can display a seemingly stationary image even as the substrate moves at production speed. Often described as web-viewing systems, these arrangements help an operator inspect selected regions, magnify small details, and recognize visible changes. They do not, by themselves, perform automatic acceptance or rejection: the operator remains responsible for interpreting the image.
Automated inspection uses software to compare the acquired print image with an approved reference and detect deviations according to defined rules. Three system categories should therefore be distinguished:
- Web or sheet viewing: The operator views and enlarges an image to assess print appearance and investigate a suspected problem.
- Automated print inspection: Software automatically identifies differences against an approved reference or specified inspection criteria.
- 100% print inspection: The acquisition architecture is designed to inspect the complete specified area of the web or every designated sheet throughout the run, subject to the system's stated coverage and detection limits.
The term 100% inspection describes the extent of inspection coverage; it does not mean that 100% of every conceivable defect will be detected. Defects below the effective detection limit, defects with inadequate optical contrast, or conditions not included in the inspection logic may still pass without an alarm. Coverage and actual detection effectiveness are separate performance claims and should be validated separately.
- Engineering Architecture of a Machine-Vision System
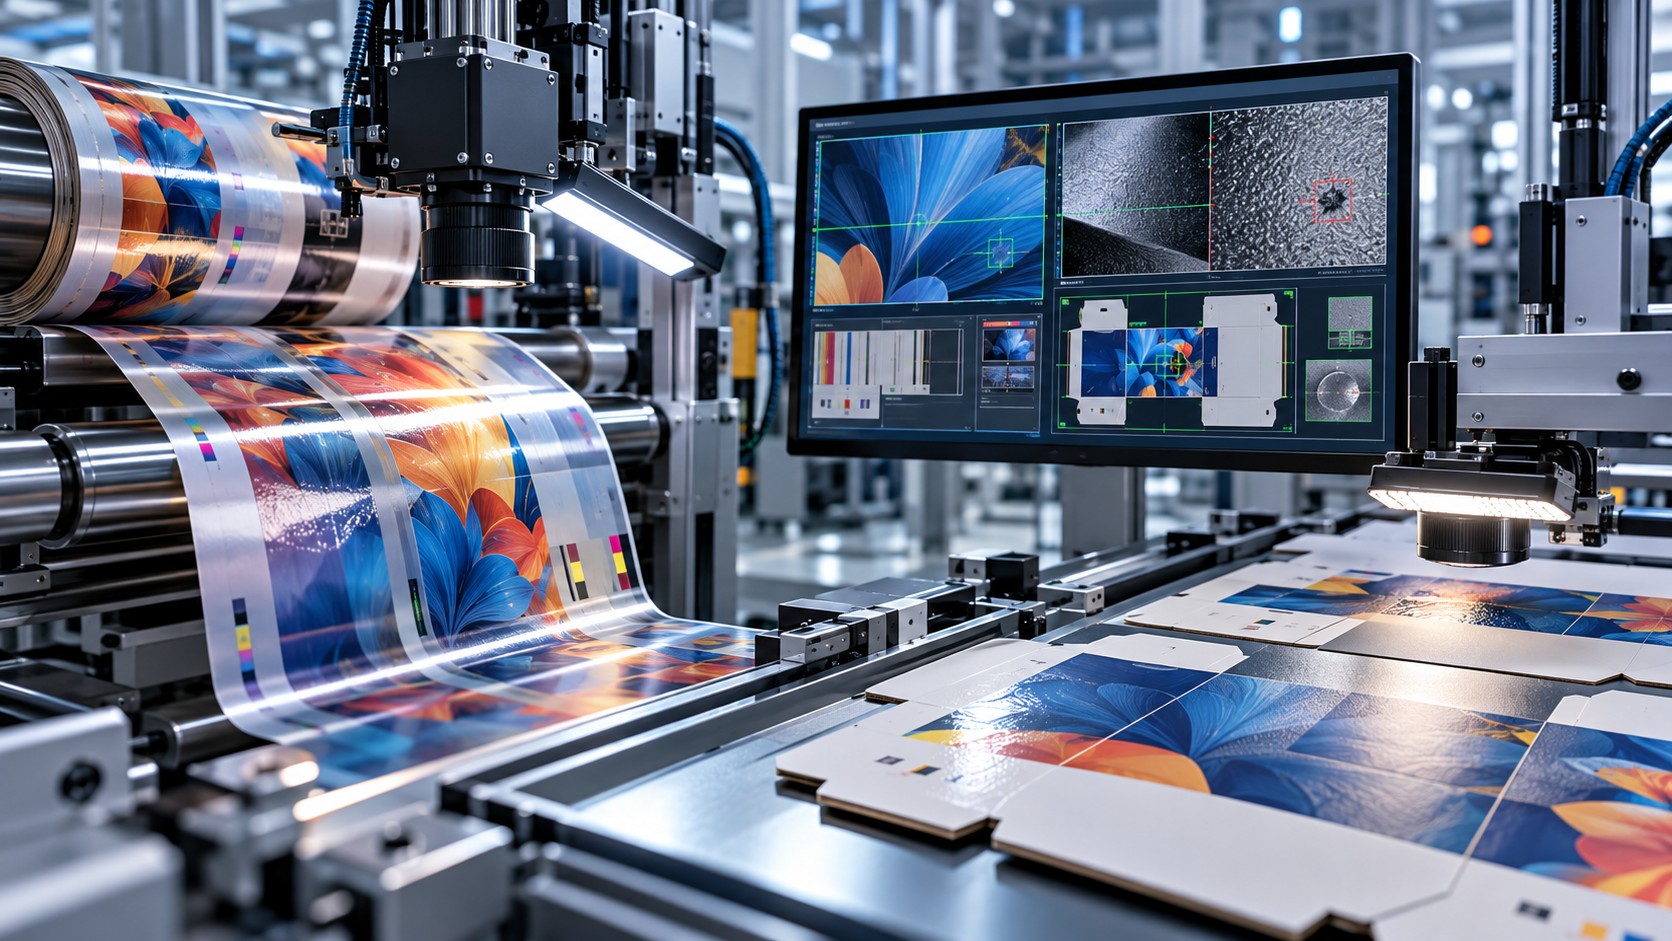
An industrial vision system brings together controlled lighting, optics, cameras, synchronization, image processing, and a decision layer. A printed substrate passes through a defined inspection area. Light reflected by or transmitted through the material is captured by digital sensors. The system corrects the resulting image, geometrically aligns it, compares it with the approved reference, and evaluates it against the inspection criteria.
Performance depends on the entire optical and mechanical chain. A high-pixel-count camera cannot compensate for inappropriate lighting, poor focus, substrate vibration, or motion blur. Reliable inspection is a system-level engineering problem.
Line-Scan Cameras
A line-scan camera acquires one line, or a small number of lines, per sampling cycle. As the substrate moves through the inspection area, the successive lines form a two-dimensional image. This arrangement suits continuous web production, but it can also be used on sheetfed presses where each sheet moves through a synchronized scanning station.
Cross-web spatial sampling depends on the number of sensor pixels and the covered field of view. Sampling in the direction of travel depends on line rate and substrate speed. Some systems use multiple cameras to cover wide formats or to combine different imaging capabilities.
Area-Scan Cameras
An area-scan camera acquires a two-dimensional frame at each exposure. Such cameras are often used for targeted inspection, registration control, high-magnification observation, and checks of localized details.
They are not inherently limited to sampling a few locations. With appropriate synchronization, frame overlap, and processing, area-scan cameras can also contribute to full-area inspection. The key distinction is not the sensor name but the actual acquisition architecture and verified coverage. Many installations combine continuous inspection with a separate high-magnification viewing camera for operator investigation.
- Resolution, Illumination, and Speed: What Sets the Detection Limit?
A vision system cannot reliably detect a defect if it provides insufficient optical information at the sensor. Spatial resolution determines how a small feature is represented, but pixel size alone does not establish detection capability. Optical sharpness, contrast against the background, image noise, focus, motion, and defect orientation also matter.
A mark spanning one pixel may not be consistently detectable against a complex printed image. High-speed motion further limits exposure time: excessive exposure can produce motion blur, while very short exposure reduces the light available to the sensor. High-performance inspection therefore requires coordinated control of lighting intensity, sensor speed, optical resolution, and processing capacity.
Illumination Is Part of the Measurement
Illumination geometry can make a defect visible or conceal it. Different approaches serve different purposes:
- Bright-field illumination: Highlights printed image differences and certain surface characteristics.
- Dark-field illumination: Can emphasize light scattered by scratches, particles, and some surface topography.
- Transmitted illumination: Can reveal holes, contamination, or interruptions in transparent and translucent materials.
- Specular illumination: Uses controlled reflection angles to inspect glossy regions, varnish, and surface texture.
- Polarized illumination: Uses optical polarization to suppress or exploit selected reflections and distinguish surface features.
Specialized applications may use illumination outside the conventional visible range when substrate or coating properties make it useful. No single lighting arrangement is optimal for every material and defect. A black spot on white paper and a missing patch of clear varnish on a high-gloss carton present very different optical challenges.
- Reference Images: Golden Sample and PDF-to-Print Inspection
After image acquisition, the system needs a meaningful reference.
Golden Sample
A golden sample is an image acquired from a printed sheet or web section that has been inspected and approved. Subsequent production is compared against the approved physical result. This accommodates the actual appearance created by the ink, printing technology, substrate texture, and coatings.
The weakness is equally important: a defect unintentionally accepted in the golden sample may become part of the system's definition of a good print. A controlled reference-approval procedure, revision identification, and retained records are therefore essential.
PDF-to-Print Inspection
PDF-to-print inspection compares the printed product with approved digital artwork, after the necessary image preparation. It can help find missing content, incorrect text, missing graphic elements, or mismatched document revisions.
However, a PDF is not a photograph of the eventual print. Rasterization, color reproduction, print geometry, substrate appearance, and imaging conditions must be taken into account. Both methods also require geometric alignment so that permissible web movement or sheet-position variation is not mistaken for missing image content.
For applications with high content-integrity requirements, a properly designed combination of an approved digital master and an approved printed reference may reveal classes of deviation that either one alone would miss.
- Automated Quality Control on Web-Fed Presses
On a web-fed press, the substrate moves continuously through printing units and onward to rewinding or converting. Inspection in this environment must accommodate high speed, web-tension variation, lateral movement, local substrate changes, and sometimes thermally induced elongation. The system must not merely take pictures quickly: it must maintain a reliable relationship between image coordinates, artwork repeat, and the moving physical material.
In wide-web printing, the main design challenge is covering a large web width while retaining adequate spatial sampling. Narrow-web printing, commonly used for labels, may place even greater emphasis on tiny characters, codes, and individual graphic elements. Both require reliable synchronization and a clear definition of the smallest critical defect.
Continuous Inspection Along the Web
The inspection station acquires a synchronized image and compares it against the approved reference using the expected repeat length. It can identify both defects that recur at a consistent image position and random anomalies that appear elsewhere in the roll.
A recurring mark may suggest a repetitive production mechanism, whereas irregularly located marks may suggest contamination, substrate inconsistency, or transient disturbance. Such observations help focus troubleshooting but do not, by themselves, establish a root cause. The optical record should be correlated with press and material information before an engineering conclusion is drawn.
Web Tension and Image Geometry
Paper and polymer films respond differently to tensile forces. Changes in web tension may produce extension, registration shifts, wrinkles, or dimensional distortion. The system therefore needs suitable geometric compensation so that permitted substrate movement is not classified as missing print or other false defects.
The compensation itself must be controlled. If tolerance is too narrow, nuisance alerts accumulate. If too generous, genuine registration or dimensional problems may disappear into the correction algorithm.
Web-Specific Defects and Substrates
Commonly inspected classes include missing print, spots, streaks, smearing, registration errors, wrinkles, variable-data defects, and issues exposed after die-cutting or matrix stripping. Transparent films and metalized webs require different optical settings than coated paper or white labelstock. Inspection following lamination must be validated independently from inspection of the printed web before lamination.
Digital Defect Maps and Rewinder Integration
A web inspection system can record defect class, severity, cross-web position, and measured position along the roll. The resulting map can be transferred to rewinding or slitting equipment, so operators can quickly locate rejected sections. Effective operation requires handling splices, rewinding direction, trimmed material, web-length changes, and separation into multiple lanes. Positional integrity is part of the qualification requirement.
Typical Optical Defects
Defect category | What the system may observe | Why it matters |
|---|---|---|
Missing print | Absent ink, text, or graphics | Incomplete image or information |
Spots/splashes | Localized unwanted marks | Contamination or ink-transfer instability |
Streaks | Continuous or intermittent lines | Repetitive or temporary print issue |
Misregistration | Misalignment of separations | Loss of detail and visual quality |
Color or density variation | Visual differences from approved image | Possible process drift |
Haze/mottle | Irregular tone or cloudy region | Non-uniform coverage or surface effect |
Wrinkles | Creases or changes in geometry | Web handling and material issues |
Label or matrix defects | Missing label or retained waste | Defect introduced during converting |
Optical detection depends on the anomaly's visibility. A tiny mark in a critical pharmaceutical code may justify rejection even when a larger mark in a decorative area does not. Defect zones should therefore be assigned acceptance criteria based on function and risk, not only physical area.
- Automated Quality Control on Sheetfed Presses
Sheetfed printing presents a different tracking problem. Rather than a continuous roll, each sheet is a discrete production unit transported through the printing sections and delivered to the pile. An inspection system must acquire and analyze each designated sheet while preserving the relationship between the captured image, sheet identity, and downstream conversion.
Inspecting Every Sheet
Depending on its architecture, a sheetfed system can scan the full specified print area or selected regions of each sheet, compare the image with an approved source, and record nonconformities. For pharmaceutical cartons, cosmetics, and consumer-product packaging, this is especially important for microtext, codes, missing information, scratches, spots, or print contamination.
Registration, Feed Position, and Sheet Geometry
Each sheet is positioned and conveyed through a mechanical handling system. Variations in feeding, gripping, or transfer may cause image displacement that differs from true color-to-color misregistration. The system must distinguish permissible sheet shifts from actual separation misalignment, dimensional change, or print distortion.
For heavy paperboard, flatness, grain direction, coating balance, and moisture history can affect how the sheet travels through the press and presents itself to the camera. Optical registration should therefore be interpreted alongside material behavior.
One-Sided and Two-Sided Inspection
Some products contain graphics on one side and instructions, serial information, or regulatory data on the other. Where front and back are inspected at different points, the tracking architecture must preserve the correct relationship between the side, master image, and individual sheet. A side mix-up is an information-integrity failure, not merely an optical discrepancy.
Location of the Inspection Station
A station positioned after printing but before coating cannot detect defects introduced by a downstream varnishing unit. A camera located after coating may see the combined surface appearance but may not reveal where a problem originated. Multiple inspection points may therefore be useful when separating print defects from coating-related defects is operationally important.
Rejecting or Marking Nonconforming Sheets
Depending on the press and inspection architecture, nonconforming sheets can be marked, recorded by sheet count, separated from the main pile, or tracked for later converting. Where several cartons are imposed on one sheet, a local defect may affect only one carton. Unit-level rejection is possible only where cutting, layout mapping, sheet identity, and downstream equipment support that distinction without losing traceability.
- Web Inspection vs. Sheetfed Inspection: An Engineering Comparison
The image-processing methods may be similar, but transport conditions, positioning logic, and reject strategies differ.
Parameter | Web-fed inspection | Sheetfed inspection |
|---|---|---|
Material movement | Continuous moving web | Individual transported sheets |
Tracking unit | Roll; distance and cross-web position | Individual sheet and its position |
Synchronization | Web velocity and print repeat | Sheet passage, timing, transport position |
Major sources of variation | Tension, lateral drift, wrinkles | Feed position, flatness, sheet deformation |
Defect history | Defect map / virtual roll | Sheet tracking or reject record |
Reject handling | Rewinding, slitting, segment removal | Marking, separation, downstream rejection |
Common applications | Flexible packaging, labels, continuous print | Folding cartons, books, covers, commercial print |
For a web system, the primary challenge is maintaining inspection continuity and an accurate physical location record along a moving substrate. For a sheetfed system, it is maintaining the quality status and identity of each sheet until the relevant downstream operation. Both require more than a camera alarm: inspection results must connect reliably to production decisions.
- Inspection of Varnishes and Coatings: The Challenge of Transparent Layers
Varnishes and coatings are among the most demanding machine-vision applications. Whereas colored ink generally produces visible contrast against a substrate, a transparent coating may cause only subtle changes in gloss, reflection, or surface texture. A varnish may appear satisfactory under diffuse lighting yet reveal missed coverage, streaks, or irregularities under illumination from another direction.
Two goals must be differentiated:
- Visual coating inspection: Does the coating cover the specified area with acceptable visible uniformity and registration?
- Functional coating qualification: Does the coating provide the actual specified performance—abrasion resistance, adhesion, barrier, sealability, or other functional property?
The first may be addressed by suitable vision technology. The second generally requires additional physical or chemical testing.
Water-Based Varnish
Water-based varnishes are used in folding cartons, commercial printing, and many coating applications. Potential visible issues include streaks, missing areas, bubbles, mottle, spots, foam marks, and inconsistent gloss. An optical system may detect some of these problems, but it cannot determine from appearance alone whether the coating has dried sufficiently for subsequent handling or finishing.
UV Varnish
UV-curable varnishes can create high-gloss, matte, decorative, and other finishes. Visual inspection may detect non-uniformity, missing regions, streaks, spots, or registration errors. A visually sound coating is not proof of adequate cure; degree of cure and durability must be validated with methods suited to the varnish chemistry and product requirements.
Gloss and Matte Finishes
Gloss coatings produce a strong direction-dependent reflected component. Matte finishes scatter light differently and can reveal changes in surface microtexture in other ways. Camera angle and lighting geometry must be selected for the intended finish. Do not assume the same optical settings suit all gloss levels.
Spot Varnish
Spot varnish is applied to selected design regions. Inspection has two distinct tasks: determining whether varnish is present and sufficiently uniform, and determining whether its position matches the graphics. Registration against an approved digital varnish mask can be particularly valuable, but only if the chosen illumination and imaging arrangement reliably reveals the varnish boundary.
Tactile and Soft-Touch Coatings
Some coatings are specified principally for their tactile or topographic effect. Specialized optical arrangements may reveal uneven coverage or visible texture variation, but a normal camera does not necessarily measure touch sensation, flexibility, abrasion durability, or the specified functional effect.
Functional Coatings
You can monitor heat-seal, cold-seal, and barrier coatings visually for missing coverage, contamination, streaks, or incomplete application. Optical continuity does not, by itself, prove seal strength, hot tack, OTR, WVTR, or other functional performance. Material approval must include appropriate end-use testing.
- How Can Transparent Varnish Defects Be Detected?
A clear varnish can be difficult to inspect because the visual distinction between coated and uncoated regions may be weak. Detection becomes more feasible when the coating changes specular reflection, effective surface refractive behavior, or microtexture.
One approach uses illumination at controlled incidence and viewing angles to enhance differences in reflected light. Another uses multiple illumination directions or methods that emphasize surface topography. In some applications, fluorescence or a marker material may help identify coated regions under suitable illumination.
A marker is not always desirable or permissible, especially where the coating must meet strict functional or regulatory criteria. Accordingly, purpose-built optical methods can also exploit intrinsic coating appearance without modifying the formulation. Such claims must be validated against the actual substrate, varnish, target defects, and production speed.
Common Varnish and Coating Defects
Defect | Defect | Description | Description | Possible consequence | Possible consequence |
|---|---|---|---|---|---|
Missing varnish | Missing varnish | Specified region remains uncoated | Specified region remains uncoated | Visual or protection failure | Visual or protection failure |
Coating starvation | Coating starvation | Locally insufficient application | Locally insufficient application | Inadequate coverage | Inadequate coverage |
Streaks | Streaks | Longitudinal or transverse marks | Longitudinal or transverse marks | Uneven application | Uneven application |
Pinholes | Pinholes | Local interruptions in coating | Local interruptions in coating | Loss of coating continuity | Loss of coating continuity |
Mottle | Mottle | Patchy or cloudy finish | Patchy or cloudy finish | Non-uniform appearance | Non-uniform appearance |
Orange peel | Orange peel | Uneven, dimpled surface texture | Uneven, dimpled surface texture | Undesired surface appearance | Undesired surface appearance |
Bubbles/foaming | Bubbles/foaming | Trapped air or foam marks | Trapped air or foam marks | Irregular film formation | Irregular film formation |
Misregistration | Misregistration | Coating does not match artwork | Coating does not match artwork | Decorative or functional mismatch | Decorative or functional mismatch |
Gloss variation | Gloss variation | Local changes in reflectance | Local changes in reflectance | Inconsistent appearance | Inconsistent appearance |
Contamination | Contamination | Particles within or on the coating | Particles within or on the coating | Visual or functional defect | Visual or functional defect |
A defect list should never be interpreted as a universal guarantee of detection. Detection depends on the coating chemistry, coat thickness, printed background, defect geometry, illumination design, and image-processing setup.
- Where Should Coating Inspection Be Installed?
Inspection-station placement determines what the system can legitimately assess. A station before the coater provides a reference for the printed surface and any defects already present. Inspection after coating can reveal changes introduced by that step. However, a coating may look different while still wet or curing, and its final surface appearance may not exist until drying or polymerization is complete.
On Web-Fed Lines
A web-inspection station can be located after the coating unit, where the material is sufficiently stable for reliable imaging. Processes with multiple coating, lamination, or drying steps may require observation at more than one location. Inspection before and after an operation helps separate incoming defects from defects newly introduced by the operation.
On Sheetfed Lines
A sheetfed system can inspect coated sheets after an appropriate process section, depending on press construction and access. For spot varnish, the inspection can compare the observed coating position with the approved mask. If further drying or curing occurs after the camera, early optical inspection must not be presented as proof of the final coating properties.
- Gloss Measurement Is Not the Same as Image Inspection
A vision system may detect areas that appear brighter or less glossy than an approved reference. Such a difference is not automatically a standardized gloss measurement. Gloss instruments measure reflected light under specified geometries and produce results that can be expressed in gloss units according to the applicable method.
ISO 2813 describes measurements at 20°, 60°, and 85° for coatings within its scope. Paper and paperboard may require methods suited to those materials, such as the 75° geometry addressed by ISO 8254-1. The selected method must match the product and acceptance specification.
Pixel-intensity differences should not be labeled standardized gloss units unless a suitable calibrated and validated measurement method establishes that relationship. Similarly, visible coating continuity does not directly measure dry coat weight in g/m². If coat weight is a product requirement, evaluate it using a fit-for-purpose test and correlate it with relevant functional performance.
- Why Image Inspection Is Not the Same as Color Measurement
A color camera can detect visible differences between a production image and a reference, but it is not automatically equivalent to a spectrophotometer. An RGB image records sensor responses affected by illumination, optics, filters, and the material's spectral properties. Spectral color measurement evaluates reflected light as a function of wavelength and converts it to defined colorimetric values under stated conditions.
This distinction matters when compliance with color standards, brand specifications, CIELAB values, or ΔE00 tolerances is required. Without an appropriate calibrated measurement method, a change in RGB pixel values cannot simply be called a verified ΔE00 difference.
The two inspection functions are complementary. Machine vision can detect a missing character or isolated mark that barely affects an average patch measurement; spectral color control can quantify a color difference according to a defined measurement protocol. High-demand production environments may need both.
- Barcodes, Data Matrix, and Variable Information
Pharmaceutical, food, and consumer-product packaging often contains printed information whose correctness is just as important as its appearance. A vision system may inspect code presence, code location, missing characters, or variation in printed variable data. Three activities must remain distinct:
- Code presence: Verifying that a symbol exists in the required position.
- Code reading: Decoding the information represented by a symbol.
- Code verification: Grading symbol print quality using a specified standardized method.
A code readable by one camera is not necessarily compliant with the applicable symbol-verification standard. ISO/IEC 15415:2024 addresses two-dimensional code print-quality assessment, while ISO/IEC 15416:2025 addresses linear barcode print-quality assessment. A general print-inspection camera is not automatically a compliant code verifier.
Likewise, a perfectly printed and verifiable code may contain an incorrect serial number, date, or product identifier. Variable-data workflows therefore need content validation against the authoritative data source as well as optical inspection and, where required, standardized verification.
- Artificial Intelligence: From Anomaly Detection to Classification
A production process exhibits some normal variation. Not every difference between two images warrants rejection. Sensitivity set too high can generate excessive alerts; sensitivity set too low can allow important defects to pass. Two error types must be distinguished:
- False positive: A conforming region is incorrectly classified as defective.
- False negative: A genuine defect is not detected.
Machine-learning methods can support defect classification, differentiate process texture from meaningful anomalies, and help prioritize operator review. A regulatory text area, for instance, may be designated as more critical than a decorative background, so similarly sized defects receive different dispositions.
AI does not eliminate the need for defined acceptance criteria. The model aids decision-making and must be validated on representative materials, artworks, operating speeds, and risk categories. Uncertain cases may need human adjudication or a secondary verification step.
- Turning a Defect Map into a Practical Production Tool
One of the most valuable advances in industrial inspection is transferring inspection information to downstream converting operations. When a defect is detected during printing, the system can record its cross-web position and location along the roll, together with its class and severity. This information forms a defect map, sometimes called a virtual roll.
At slitting, rewinding, or another finishing step, the defect map can guide the operator or equipment to nonconforming sections for removal or review, reducing repeated manual searching.
The challenge is maintaining accurate correspondence between digital positions and physical material. Splices, removed segments, reverse winding, stretch, and lane separation can all shift the relationship. A map that isn't synchronized with the actual web may remove good material while defective sections remain in the product. Traceability and positional accuracy are therefore core requirements, not optional software conveniences.
- How Should an Inspection System Be Qualified for Production?
Inspection equipment should not be approved merely because it produces impressive camera images or because its specification lists many sensors. Performance Qualification (PQ) must show that the inspection system consistently meets defined acceptance criteria under actual production conditions, considering the product, process, substrate, and critical defect risks.
First, define the critical defect classes, minimum relevant defect dimensions, required inspection area, production speed, substrate families, and intended disposition. Then prepare a representative reference set, including verified defect samples and conforming samples that reflect normal production variation. Perform the tests at realistic operating speeds and under relevant environmental and illumination conditions—not solely in a static demonstration.
Practical Qualification Metrics
- Detection rate/recall: The proportion of known, relevant defects correctly identified.
- Precision: The proportion of defect alerts that actually correspond to relevant defects.
- False-alarm rate: The frequency of alarms that do not justify rejection or investigation.
- Detection latency: The delay between the occurrence of a defect and the corresponding signal or action.
- Location accuracy: Accuracy in locating a defect for inspection, removal, or downstream rejection.
- Classification accuracy: Performance in assigning a detected anomaly to the correct defect category.
- Traceability: Reliable linkage between the result and the physical roll, sheet, production batch, or product.
An effective PQ procedure should be standardized, repeatable, documented, and practical for routine production environments. Where appropriate, a validated reference kit containing representative defects and acceptable samples can simplify qualification, support consistent results, and provide objective evidence during customer or regulatory audits. The procedure should be efficient enough to minimize production disruption without compromising its ability to demonstrate reliable inspection performance.
Varnish inspection needs additional reference samples for low-contrast defects, missing transparent coating, register shifts, and surface-reflection variation. Both printed and varnished substrates should be assessed at the intended production speeds. Reassess performance as appropriate after changes in artwork, media grade, material batch, cleaning procedures, camera configuration, or inspection software, based on the potential impact of those changes.
A successful factory acceptance test is not just evidence that a defect was found once. It demonstrates that the complete detection-and-disposition workflow operates with the required reliability, including identification, classification, location, and action. Factory acceptance testing and production Performance Qualification serve complementary purposes; successful factory testing does not replace verification under actual operating conditions.
Ultimately, qualification should establish confidence in the inspection system without becoming a production bottleneck. The objective is not to perform more tests, but to perform the right tests consistently, efficiently, and with documented evidence of performance.
- Three Engineering Case Studies
Case 1 — A Repeating Defect in Flexible Packaging on a Web Press
A converting plant prints flexible packaging on a polymer film. The inspection system identifies a narrow longitudinal streak that appears across portions of a roll. Because the streak passes through complex artwork, its effect on a global color measurement is small. Image-based inspection nevertheless detects the localized difference and records its position along the web.
The operator can investigate whether the streak consistently reappears in the same cross-web lane, whether its occurrence changes with press speed, and whether it correlates with another process event. Once the responsible mechanism is confirmed and corrected, the defect map provides a basis for finding the affected sections already produced.
The case illustrates why average color measurement and spatial image inspection complement each other: a localized defect may be unacceptable even when overall color readings remain within tolerance.
Case 2 — Intermittent Defects on Folding-Carton Sheets
A sheetfed plant prints paperboard sheets for folding cartons. Intermittently, small marks appear in areas containing user instructions and regulatory information. A camera acquires an image of each sheet and detects deviation from the approved master.
The system associates the result with a sheet identity and defect location. Depending on the installed handling architecture, the sheet may be marked, separated, or flagged for later converting. Where several cartons are imposed on the same sheet, the manufacturer can determine whether one carton or several are affected. Rejecting only the damaged units is practical only if unit mapping and the physical converting process preserve traceability.
Early identification can prevent products with damaged regulatory text from passing into die-cutting, folding, and gluing, where correction is typically more expensive.
Case 3 — Missing Clear Spot Varnish
A plant produces cartons with a clear spot-varnish pattern intended to emphasize selected graphical elements. The underlying color print is correct, but finished cartons show regions of missing varnish or misalignment with the artwork.
Under ordinary color-camera illumination, the optical difference between coated and uncoated zones is too weak to detect reliably. By adjusting viewing and illumination geometry, the plant improves contrast and evaluates the measured coating boundary against the approved digital varnish mask.
Additional gloss and adhesion tests are carried out where required by the product specification. The case demonstrates why verifying coating presence and position optically is separate from approving the coating's physical and functional properties.
- What Machine Vision Cannot Guarantee
Despite rapid technological progress, conventional image inspection cannot independently qualify every characteristic of a printed or converted product. It is not automatically a replacement for spectrophotometric color measurement, standardized gloss measurement, adhesion testing, abrasion testing, or seal-strength measurement.
It does not necessarily prove that a UV-curable coating has cured adequately, that a barrier coating meets the required gas-transmission rate, or that a folding carton will withstand repeated creasing or folding without cracks.
The finished product may need tests selected for its intended performance. Examples include print or coating rub testing according to a suitable method, such as ASTM D5264 where applicable; gloss measurement using the required instrument geometry; and application-specific tests for peel adhesion, sealing, chemical resistance, or barrier performance.
Likewise, a successful image comparison does not certify the correctness of the variable information or that a barcode has passed a standardized verification procedure. These claims require their own validated workflows. Product quality results from coordinated control of the printing process, optical inspection, material properties, functional tests, and documented acceptance limits—not from a single camera system.
- The Future: From Finding Defects to Preventing Them
Machine vision is moving beyond isolated alarms toward integration with process data and production automation. When a plant records defect category, location, frequency, duration, and timing, the information can be correlated with press speed, substrate changes, coating conditions, process sensors, and maintenance events.
A defect that increases after a speed change may indicate a relationship between motion conditions and printed appearance. Coating defects repeatedly concentrated in one cross-web location can point the investigation to a particular part of the application system. A rise in alarms after a new substrate batch arrives may justify additional incoming-material checks.
These relationships can guide root-cause analysis, but correlation alone does not prove causation. Controlled trials and independent verification are still needed before process changes are adopted as corrective actions.
The next level of integration connects visual inspection with production-management systems, press data, intelligent alerting, and—when safely validated—automatic adjustments or selective rejection. The goal is not necessarily to remove the operator, but to give people faster, more trustworthy information so they can respond before a small process deviation becomes a large volume of waste.
Conclusion — Quality Is More Than What the Camera Sees
Machine vision has become an important part of quality assurance in industrial printing. On web-fed presses, it supports continuous observation of moving material, defect mapping, and traceability through slitting and rewinding. On sheetfed presses, it can assess individual sheets and link inspection results to their disposition during finishing. For varnishes and coatings, tailored illumination and inspection methods can reveal abnormalities that are difficult to see under normal viewing conditions—particularly in transparent, special-effect, and functional layers.
But the ability to image every meter or every sheet does not itself guarantee a conforming product. The inspection method must be qualified for the substrate, coating, optical environment, critical defect types, and final application. Its decisions must be connected to clear acceptance criteria and reliable production actions.
The purpose is not to create a factory in which every imperfection is photographed and archived. It is to create a factory in which trustworthy evidence reduces avoidable rejection, guides corrective action, prevents unnecessary material waste, and protects the quality of the delivered product.
The true value of an automated inspection system is measured not only by how many defects it can see, but by how consistently it turns visual information into dependable engineering decisions across the entire production chain.
Technical Standards and Reference Context
The article is a technology-neutral engineering overview informed by industrial approaches to web inspection, sheetfed inspection, camera systems, and coating inspection (including publicly documented approaches from AVT and BST). The standards below cover complementary measurement and verification activities; consult them in their current official editions and apply them only within their stated scopes.
Selected standards: ISO/IEC 15415:2024 — Print-quality test specification for two-dimensional barcode symbols; ISO/IEC 15416:2025 — Print-quality test specification for linear barcode symbols; ISO 2813:2014 — Specular gloss of non-metallic paint films at 20°, 60°, and 85°; ISO 8254-1:2009 — 75° specular gloss measurement for paper and board (TAPPI method); ASTM D5264 — Abrasion resistance of printed materials using a Sutherland rub tester (check the applicable revision for the intended test).