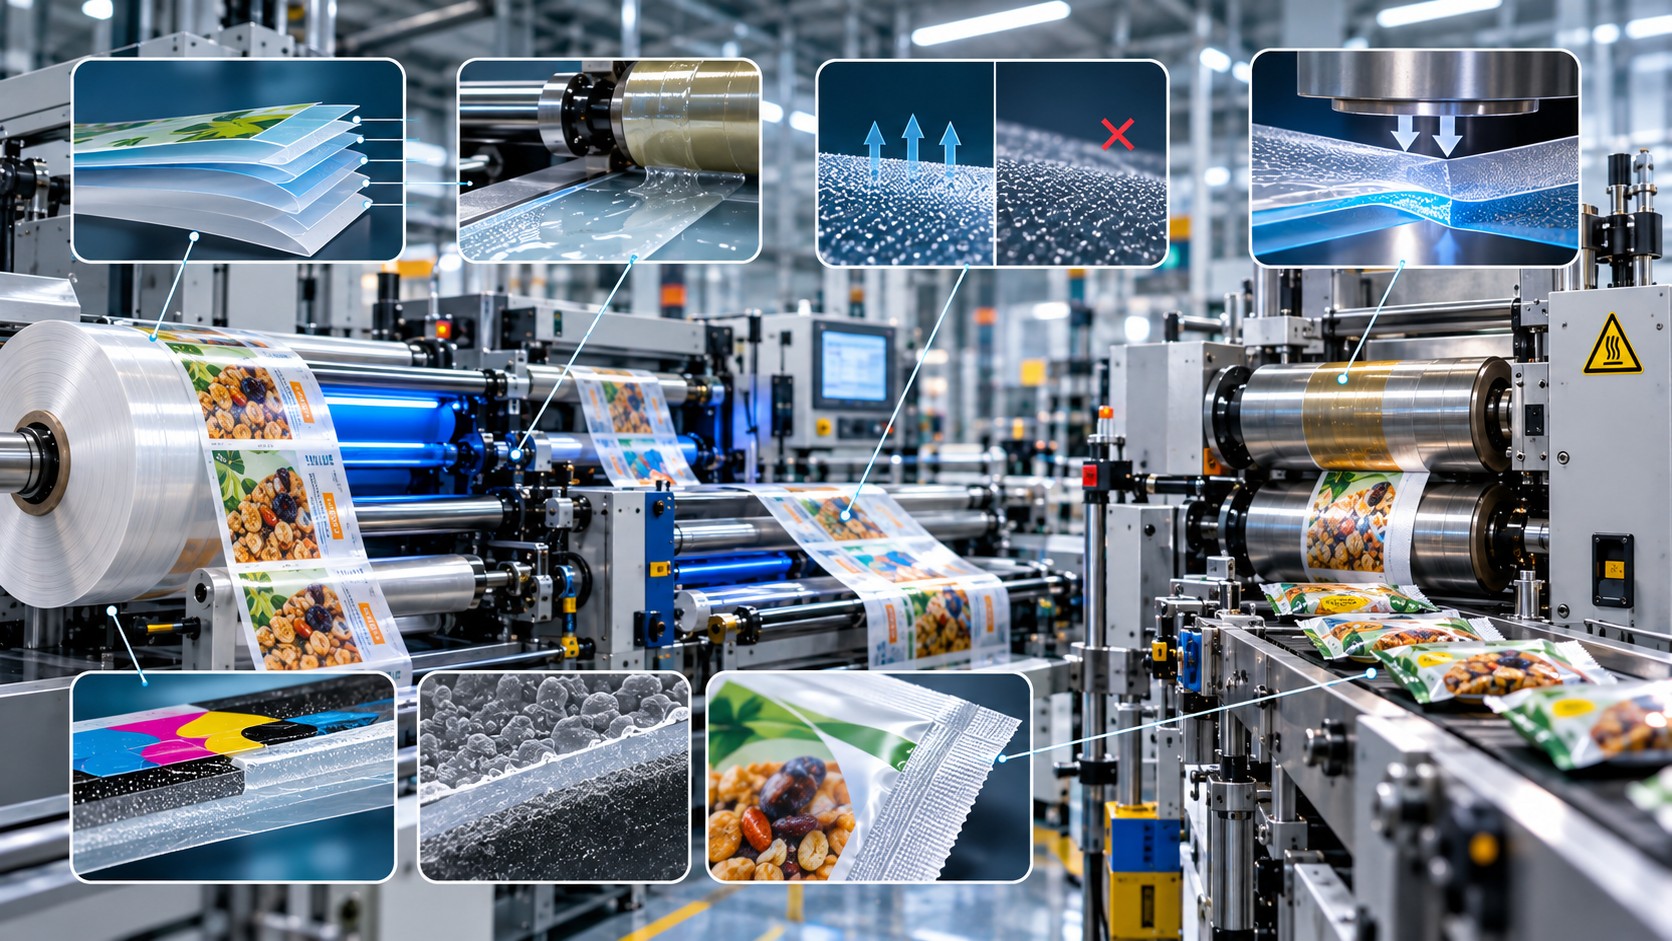
In flexible packaging, sealing is sometimes regarded as the final step of converting. In reality, it is one of the operations that most influences package performance. Even when the substrate has been selected correctly, the print looks excellent, and the laminate is sound, a defective seal can turn a protected product into a package that fails its functional requirements.
Most flexible packages use heat sealing: heat, pressure, and dwell time are controlled to soften compatible polymer sealing layers and form a joint that develops its ultimate properties on cooling. Heat is not ideal for every application. Heat transfer near the sealing area may affect chocolate, confectionery, and other temperature-sensitive products. In selected applications, thermal deformation of the film or machine-speed constraints may also be significant.
Cold sealing follows another route. A purpose-designed adhesive coating forms a bond when two compatible adhesive-coated areas are pressed together, without intentionally heating the sealing jaws. What appears to be a straightforward substitute for heat is, in fact, an engineered system of interacting surfaces: the adhesive must anchor to its substrate, bond to the opposing cohesive layer under pressure, and still separate cleanly from the back of the adjacent web turn while stored in a roll.
Print layers, primers, release lacquers, and lamination adhesives make those relationships more demanding. Liquid Electrophotography (LEP) opens useful opportunities for digitally printed, variable, and short-run packages, but its polymeric ink film differs from the ink films normally created in solvent- or water-based flexography. The difference matters where ink meets a release lacquer or lamination adhesive. A reliable package is therefore evaluated through printing, coating, winding, storage, unwinding, filling, sealing, distribution, and consumer use—not at any single operation.
1. Cold Seal Versus Heat Seal: Two Different Bonding Mechanisms
With heat sealing, compatible polymer sealant surfaces are heated under pressure, commonly allowing local softening and interdiffusion or fusion. After cooling, the joint is assessed for strength and integrity. Cold sealing uses a dried cohesive adhesive at designated locations. The bond develops through intimate contact and interactions between compatible adhesive surfaces under mechanical pressure; deliberate heat input at the sealing jaws is not part of the basic sealing mechanism.
"Cold" refers to the final sealing operation, not necessarily to the coating line. Water-based cold-seal coatings normally require a controlled drying stage. Proper coating formation can require energy and careful temperature management, even though the finished package may later be sealed without heated jaws.
Characteristic | Heat seal | Cold seal |
|---|---|---|
Bonding principle | Heat-assisted bonding of compatible sealant layers | Pressure-induced bonding between compatible cohesive coatings |
Deliberate jaw heating | Usually required | Not required for the sealing mechanism |
Functional material | Heat-sealable polymer or coating | Specially formulated cohesive adhesive |
Main process window | Temperature, pressure, dwell, cooling | Coating compatibility, pressure, contact, storage history |
Potential advantage | Broad package-structure options and robust seal development | Useful for heat-sensitive products; possible high-speed operation |
Common risks | Undersealing, overheating, distortion | Blocking, seal deadening, anchorage loss |
Neither technology is inherently better for every product. The packaging application, line design, product sensitivity, and performance requirements should drive the decision.
2. The Chemistry of Cold-Seal Adhesives
Cold-seal coatings are often called cohesive adhesives. In conventional systems, the formulation is designed to bond preferentially to a compatible coated surface under pressure. Many products are applied as an aqueous dispersion. As the carrier water is removed, a continuous or sufficiently coherent polymer film develops, providing the contact and cohesive properties needed for sealing.
Depending on the formulation, the mechanism is primarily physical and viscoelastic rather than a new chemical curing reaction triggered by jaw pressure. The balance between surface contact, tack, internal strength, and substrate anchorage determines the result. Natural-rubber latex is common in packaging, but synthetic elastomeric or acrylic systems also exist. Their behavior must be qualified, not inferred from the polymer family alone.
Formulation component | Engineering function |
|---|---|
Natural-rubber latex | Elastic and cohesive bonding behavior |
Synthetic elastomers | Alternative polymer architecture and adjusted mechanical properties |
Acrylic or complementary polymers | Control of tack, anchorage, stability, and bond behavior |
Water | Carrier phase in an aqueous dispersion |
Surfactants | Dispersion stability and substrate wetting |
pH-control agents | Chemical and storage stability |
Defoamers | Reduced foam formation during circulation and application |
Process additives | Rheology, storage stability, coating performance |
These are functional categories, not a universal formulation recipe. A particular commercial adhesive may omit some of them or use other chemistries.
Adhesion is not cohesion. Adhesion describes bonding between the cold-seal coating and the film underneath it. Cohesion describes strength within the coating itself. A useful seal also requires bonding between the two facing cold-seal coatings. If a coating peels away from its film, the mechanism differs from a failure within the adhesive or between its facing layers. Recording the failure interface is at least as important as recording peel force.
3. Cold-Seal Release Lacquer: Preventing the Wrong Bond
Cold-seal constructions must deliberately create two opposite behaviors. During packaging, cohesive-coated regions should bond to one another. During storage in roll form, the cold-seal face contacts the outer face of the preceding or following web turn and should separate without excessive unwind force, adhesive transfer, or damage.
A cold-seal release lacquer (CSRL) controls this second interface. Depending on the formulation, it may also contribute surface protection, appearance, and friction properties. Release coatings can incorporate film-forming resins, functional release additives, waxes, or other components and may be water- or solvent-based. Their chemistry must be compatible with the cohesive adhesive and the surface on which the release lacquer is deposited.
The lacquer is not simply a low-friction varnish. Coefficient of friction (COF) describes resistance to sliding; release force measures the force needed to separate two contacting layers after a defined history of pressure, time, and temperature. A roll can have an acceptable COF yet still block during warehouse storage.
On a surface-printed package, the release lacquer may contact the printed ink layer. This introduces a distinct ink–lacquer anchorage requirement. A lacquer that performs well on bare BOPP or PET cannot automatically be assumed to anchor equally well on a printed polymer film. The lacquer/adhesive pair and the lacquer/printed-surface interface should be qualified separately.
4. Package Architecture and Ink Placement
Before choosing a printing system, locate the ink relative to the cohesive adhesive and release coating. Two common architectural families illustrate why this matters.
Surface-printed structure (outside to inside):
CSRL / INK / PRIMER (if needed) / FILM / COLD-SEAL
Here the CSRL coats the outer printed surface and is in direct contact with the ink. Evaluate its adhesion, coverage, and release behavior across all relevant printed areas, including heavy coverage and opaque white, if present.
Reverse-printed, laminated structure (outside to inside):
CSRL / OUTER FILM / REVERSE INK / LAMINATION ADHESIVE / INNER FILM / COLD-SEAL
Here the ink is protected within the laminate; the release lacquer is normally applied to the exposed outer surface. Direct ink–CSRL contact may no longer exist, but the structure introduces or emphasizes film–ink and ink–lamination-adhesive interfaces. These examples are schematic layer families, not approved recipes. Specific layer order, print direction, release placement, adhesive exposure, and food-contact status must be confirmed for the intended package.
Flexography and gravure are established routes for coating and patterned adhesive application. The graphic layer itself can be produced by several print technologies. The complete material architecture—not merely the print engine—determines qualification requirements.
5. Applying and Drying the Cold-Seal Coating
Cold seal is often pattern-coated: the cohesive is applied only where seams must form, such as longitudinal and transverse sealing zones. Placement accuracy is important. If two coated patterns do not properly overlap at the jaws, more pressure cannot restore missing adhesive contact.
Coat weight, solids content, viscosity, drying, and registration interact. Too little dry coat weight can impair sealing; too much coating can complicate drying, increase blocking, or cause transfer. Wet coating weight does not equal the dry material deposited. For example, a coating containing 40% nonvolatile solids applied at 5 g/m² wet coat weight would theoretically leave approximately 2 g/m² dry material after removal of the volatile carrier. This is a mathematical example, not a production setpoint.
In gravure application, viscosity and flow behavior influence cell filling and release. Flexographic application adds dependence on anilox transfer, plate condition, doctoring, and the coating's behavior under shear. Foam, unstable rheology, improper circulation, or aggressive unapproved adjustments to water and pH can affect uniformity.
Drying must be qualified for the adhesive grade, carrier web, line speed, dry coat weight, and equipment. Under-drying may leave an unstable coating or increase blocking risk. Excessive or inappropriate thermal exposure may affect the adhesive or deform the web. No single dryer-temperature specification applies to all cold-seal formulations.
6. LEP Versus Flexographic Ink: Compare the Ink Film, Not Just the Press
The central technical comparison is the material left on the substrate after printing. Comparing color resolution, throughput, or how often artwork can change is not enough. Both printing routes deposit pigmented, polymer-containing layers, but the chemistry and film-formation route can differ fundamentally.
How an LEP ink film forms
In liquid electrophotography, electrically charged ink particles containing pigment and polymer resin are dispersed in a liquid carrier. The electrophotographic image is transferred to a heated intermediate blanket, where the carrier is reduced, and the particles consolidate into a polymeric ink film. That film is then transferred to the substrate. The web is not the main site for evaporating a freshly deposited, conventional solvent-flexo ink layer after every color transfer.
The resulting surface is a polymeric film whose adhesion depends on the ink, substrate, any approved primer, and process conditions. Film formation before transfer helps in suitable applications, but it does not automatically ensure compatibility with CSRL, lamination adhesive, food-contact requirements, or elevated-temperature use.
How a flexographic ink film forms
Flexography transfers comparatively low-viscosity ink to the substrate through an anilox and plate. Flexible packaging uses a wide variety of resin systems, including nitrocellulose (NC), polyurethane (PU), polyvinyl butyral (PVB), acrylic systems, and combinations selected for surface printing or reverse-print lamination. Solvent- and water-based inks develop their final films as volatile components leave after transfer; radiation-curable chemistries follow a different curing process.
Flexo ink developers can select binders and additives for rub resistance, blocking resistance, overprint compatibility, adhesion, and lamination. Certain established systems have been developed and tested alongside cold-seal release coatings. Others contain slip agents, waxes, or other ingredients that may interfere with the chosen cold-seal/release system. Flexography is therefore not automatically compatible: the specific ink series and full construction must be qualified.
Engineering variable | LEP packaging ink | Flexible-packaging flexo ink |
|---|---|---|
Typical binder architecture | Dedicated thermoplastic polymer/resin ink system | NC, PU, PVB, acrylic and other binder families |
How the ink film is formed | Ink particles consolidate on heated blanket; film transfers to substrate | Liquid film dries on substrate or cures, depending on chemistry |
Substrate adhesion | Ink–substrate–primer compatibility | Binder, surface treatment, drying/curing, substrate compatibility |
CSRL compatibility | Verify wetting, ink–lacquer anchorage, storage and release | Qualified ink–release combinations may be available; additives still matter |
Reverse-print lamination | Verify ink–adhesive bonding and full laminate. | Lamination-specific ink ranges available; process still requires validation. |
Residual volatile components | Distinct from conventional solvent drying; not an exemption from safety testing | Control solvent/water removal and relevant residuals. |
Heat and pressure | Evaluate thermoplastic film and interfaces under intended exposure | Behavior depends on binder, additives, and film formation |
Heavy coverage/white | Evaluate coating anchorage and print-coverage effects | Evaluate drying, coating anchorage, lamination, blocking |
Variable artwork/short runs | Major digital manufacturing advantage | Requires corresponding prepress and plates/changeovers |
The table identifies test priorities, not a general ranking of which ink is stronger, more flexible, or more compatible with cold seal.
7. What LEP Adds to Cold-Seal Packaging
Graphic quality and repeatability. LEP can deliver high-quality fine detail, tonal transitions, opaque or dense areas within the ink system's capabilities, and controlled digital color reproduction. This can be valuable for confectionery and other consumer packages where appearance plays a major commercial role.
Short runs, multiple versions, and variable information. Brand variants, seasonal packs, languages, and promotional designs can be changed without creating a new set of flexographic plates. The commercial benefit depends on run length, SKU complexity, costs, and available converting capacity; it is not an automatic advantage for every volume.
Ink-film formation before transfer. The hot-blanket transfer mechanism differs from drying liquid flexo ink directly on film. This can support suitable flexible-film workflows, but should not be interpreted as a universal heat-resistance or coating-compatibility advantage.
Reverse-printed structures. LEP graphics can be located inside an appropriately qualified laminate, avoiding direct contact between CSRL and the ink. This changes the principal qualification task: the relevant film–ink and ink–lamination-adhesive interfaces must remain reliable, including over areas with heavy color or opaque white.
A digital press does not eliminate the need for an analog coating or conversion step. Where cold seal is applied downstream, integration, registration, roll identification, and process sequencing remain essential.
8. LEP-Specific Risks and Required Controls
Release lacquer on a polymeric printed surface.
When CSRL is applied directly over LEP, it contacts a polymeric ink film rather than bare plastic film. Wetting, coating uniformity, resin compatibility, ink thickness, and the condition of the printed surface can influence lacquer anchorage. A release test that appears acceptable may conceal an anchorage failure if the lacquer itself detaches from the ink during unwinding.
Print coverage and opaque white
A package may include unprinted areas, process-color images, solid dark backgrounds, and substantial opaque-white coverage. These surfaces cannot automatically be expected to coat and release identically. Qualification samples should represent real artwork coverage, not just bare film. If a defect maps to heavy coverage, isolate possible contributions from total ink mass, binder chemistry, and the lacquer application.
Primer and surface treatment
Low-energy films such as PE and PP may require a qualified primer or surface treatment to obtain reliable LEP ink anchorage. Corona treatment can be part of a compatible workflow, but it is not a general remedy for chemical incompatibility. In particular, post-print corona treatment of an LEP ink surface must not be prescribed indiscriminately to improve CSRL wetting; it requires an approved process and evidence that print and surface functionality remain intact.
Heat, pressure and storage
Because the LEP film contains thermoplastic resin, thermal and mechanical behavior must be assessed under the actual exposures of printing, coating, winding, warehousing, and downstream converting. Thermoplastic does not mean that the ink necessarily blocks at ordinary storage temperatures. It means the result is formulation- and condition-dependent and must be tested, not presumed.
Lamination interfaces
In reverse-printed constructions, the ink is part of the load path between laminate films. The film–ink interface, ink cohesion, and ink–adhesive interface should be evaluated, ideally across different coverage conditions. High bond strength in an unprinted strip does not prove adequate bond strength through a thick ink area. Do not assume adhesives qualified for other ink technologies are compatible with LEP without verification.
9. What Flexographic Ink Adds—and What Can Go Wrong
Flexography offers a wide choice of purpose-designed packaging ink formulations. Surface-print inks can be tailored for scuff and abrasion resistance and overprint-coating compatibility; reverse-print inks can be developed for bonding to lamination adhesives. Known CSRL-compatible systems and extensive application history can reduce development uncertainty when the same materials and conditions are used.
However, formulation freedom introduces variables. With solvent-based inks, inadequate drying can leave volatile components and affect odor, functional performance, or other layers. High total ink coverage and opaque white can extend drying demands. Additives such as waxes and slip agents may be incompatible with a given cohesive/release pair, through surface contamination or migration during storage.
The practical difference is not that flexo ink always produces deadening, or that LEP never does. The mechanism must be established for the exact ink chemistry, applied layers, and storage conditions. A flexographic formulation validated for cold-seal applications can be a good starting point; a different series or additive package may behave differently.
10. Which Printing Route Is Better for Cold Seal?
There is no universal winner. For long runs with stable artwork, flexography can be very efficient, especially with a qualified ink/CSRL/cold-seal system. For multiple versions and frequent artwork changes, LEP can offer compelling digital production benefits—provided the complete packaging construction is approved. Commercial selection and functional material qualification are separate decisions.
Qualification item | LEP-focused test | Flexo-focused test |
|---|---|---|
Ink anchorage | Ink-to-substrate/primer after processing | Binder-to-substrate after correct drying/curing |
CSRL anchorage | Lacquer to thermoplastic printed film | Lacquer to binder/additive-containing printed film |
Blocking | Printed ink–CSRL–cohesive contact after storage | Ink-additive–CSRL–cohesive contact after storage |
Lamination bond | Interfacial bond through LEP ink | Interfacial bond through qualified lamination ink |
Aging | Stability of printed and coated interfaces | Ink/additive/release interactions over time |
Food-contact evaluation | Final printed/primed/coated system | Final printed/coated system plus relevant residuals |
Recycling assessment | Effect of ink film and other added layers | Effect of binder/additive system and other layers |
11. Blocking: When the Roll Will Not Unwind Cleanly
Blocking occurs when adjacent web turns bond more strongly than intended. Manifestations include high unwind force, print damage, adhesive transfer, or local tearing. In cold-seal structures, the critical separation usually occurs between the cohesive adhesive and CSRL. Incorrect chemistry, under-drying, inappropriate coat weight, roll hardness, pressure, temperature, or storage duration can all contribute.
With surface-printed LEP, investigate whether separation occurs between cold seal and release lacquer or between the lacquer and underlying ink film. In flexography, also inspect potential contributions from ink-side additives and film formation. The key observation is which material remains after separation. Increasing release-agent loading or reducing winding tension without identifying the failure interface may alleviate a symptom without fixing the cause.
12. Seal Deadening: Strength Loss After Storage
A web can seal adequately on the day of coating and lose strength after weeks in roll form. Possible causes include changes in the cohesive coating itself, aging, surface contamination, or transfer of mobile constituents from contacting layers. In printed packaging, the ink/CSRL/cold-seal system must be evaluated as a whole.
A useful investigation divides cold-seal specimens from the same batch into controlled groups: an isolated coated reference, a specimen stored against a qualified release surface, and specimens stored against the actual printed-and-lacquered structures. Test at the same temperature, pressure, humidity, and time points. Measure unwind/release force, seal strength, and failure mode. A loss occurring only with one printed/release combination suggests a contact-induced interaction; a similar decline across groups points toward adhesive aging or common storage conditions.
An LEP-versus-flexo comparison must recognize that the correct release formulation may differ between ink surfaces. If each print technology uses its own qualified CSRL, the experiment compares systems; a separate controlled study is needed to attribute differences to the ink chemistry alone.
13. Additional Coating and Converting Defects
Anchorage failure. Cohesive adhesive detaches from the base film. Investigate wetting, surface preparation, compatibility, coating formation, and drying. Surface-energy measurements can guide investigation but do not themselves prove adhesion.
Scumming and streaking. Unwanted residue or nonuniform patterning can result from rheology, unstable dispersion, transfer conditions, doctoring, anilox/cell condition, or drying. The visible pattern is a clue, not a diagnosis.
Foaming. Air introduced through mixing, recirculation, or the coating system can disrupt coat weight and uniformity. Verify flow path and defoaming compatibility rather than adding unapproved chemistry.
Weak seals. Candidate causes include insufficient or nonuniform dry coating, inadequate contact pressure, coating-pattern misregistration, localized contamination, aged cohesive, or loss of coating anchorage. The first correction should follow a confirmed mechanism, not the assumption that more coating or higher pressure is always better.
14. Troubleshooting Matrix for Printed Cold-Seal Structures
Observation | Plausible mechanism | Evidence to collect | Controlled response |
|---|---|---|---|
Roll difficult to unwind. | Excess cold-seal/CSRL adhesion | Release force after controlled aging; split-interface inspection | Qualify coating pair; review drying and winding |
CSRL lifts from LEP ink | Ink–lacquer anchorage failure | Peel and microscopic inspection across print coverage | Adjust approved CSRL, primer, or coating process |
CSRL lifts from flexo ink | Resin/additive–lacquer incompatibility | Compare qualified ink/lacquer systems | Correct ink or CSRL formulation |
Seal weakens after storage. | Deadening, contamination, adhesive aging | Isolated and contact-aged samples | Correct the experimentally identified cause |
Low lamination bond over LEP solids | Film–ink or ink–adhesive failure | Bond testing at low/high ink coverage; failure mode | Qualify ink/primer/adhesive/process combination |
Low bond over flexo solids | Ink chemistry or incomplete drying | Laminate peel, retained solvent/film-formation checks | Adjust ink system or validated drying process |
Weak seal at high line speed | Insufficient effective pressure/contact time | Test over speed range; jaw-pressure mapping | Tune sealing mechanics within qualified window |
Cohesive transfers to back surface | Poor adhesive anchorage or excessive back-surface affinity | Inspect both sides after unwinding | Improve the failing interface, not merely coat weight |
Peel acceptable, package leaks | Local discontinuity or contaminated seal | Appropriate package-integrity test | Resolve seam geometry and localized defects |
A defect photograph or single force value rarely determines root cause. Identify the failure interface and reproduce the mechanism under controlled conditions.
15. A Practical LEP-versus-Flexo Qualification Program
A sound comparison uses the same base-substrate family, seal design, intended packaged product, and performance requirements wherever practical. Prepare comparable graphics with unprinted areas, intermediate coverage, solids, and opaque white if relevant. Choose ink and coating systems actually qualified for each technology rather than forcing an unsuitable common CSRL solely for experimental symmetry.
Minimum evaluation should include:
- Ink adhesion to substrate or primer after the print process and representative downstream operations.
- CSRL adhesion to the exposed surface, including high-coverage print areas.
- Release force after controlled contact pressure, temperature, humidity, and storage time.
- Seal strength and failure mode under defined pressure, speed, dwell, and conditioning.
- Blocking resistance and evidence of coating transfer or print damage.
- Lamination bond, where reverse printing is used, across representative ink coverage.
- Package integrity, since a sound average peel force does not exclude localized leaks.
- Aging, including the storage horizon relevant to real converted rolls.
- Food-contact and migration/transfer qualification, whenever the application requires it.
For troubleshooting an ink-coverage effect, compare untreated or unprinted film, moderate process-color coverage, a solid build, and opaque-white regions under the same lacquer application. If only heavily printed areas fail, investigate ink film mass, binder characteristics, coating wetting, and anchorage before blaming an entire printing technology.
16. Test Methods, Reporting and Release Criteria
Seal strength of flexible barrier materials can be assessed using ASTM F88/F88M, with consistent specimen width, test geometry, support mode, speed, and sample conditioning. Record both measured force and the fracture path. A failure inside the cold-seal coating is not the same as a peel from its substrate, and film tearing may indicate that the substrate—not the seal bond—limited the test.
For suitable nonporous flexible packages, ASTM F3039 describes dye-penetration leak detection. Method applicability must be checked for the actual package; it is not a quantitative substitute for a seal-strength test. Other leak-integrity methods can be used when appropriate to the package design.
Unwind/release and blocking assessments also need documented conditioning parameters, not a single unexplained force value. The plant should specify pressure/contact history, time, temperature, humidity, sample orientation, and failure classification. Qualification should include actual production graphics and converted packages, not just an unprinted laboratory coupon.
17. Food-Contact Compliance: The Interfaces That Remain Invisible
A functional seal does not, by itself, demonstrate food-contact suitability. Components may transfer through packaging structures or by set-off when printed and contact surfaces touch in a wound roll. Layer position, the relevant product, use conditions, contact time, and potential migration pathways all matter.
Flexographic systems may require attention to solvent residuals, binder constituents, additives, and other formulation-specific substances. LEP requires assessment of its ink constituents, liquid-carrier-related residues as applicable, primer, coating layers, and the final structure. Ink transfer as a formed polymeric film does not establish zero migration.
In the EU context, Regulation (EC) No 1935/2004 provides the general food-contact framework, and Regulation (EC) No 2023/2006 covers good manufacturing practice. Additional material-specific rules and relevant national requirements may apply. Base final use qualification on the complete construction and intended exposure. For natural-rubber-latex-based systems, assess relevant protein/allergen exposure where warranted; use of latex alone neither proves nor excludes actual product exposure.
18. Cold Seal, Mono-Material Structures, and Recyclability
Moving toward predominantly PE- or PP-based flexible structures introduces another engineering constraint. A multilayer mono-material family package can use different grades of the same primary polymer while also incorporating minor coatings, inks, adhesives, tie layers, and additives. Its dominant polymer identity does not alone prove recyclability.
Cold seal introduces a functional adhesive and a release coating whose chemistries are generally not simply identical to the base PE or PP. Evaluate the effects of these layers, the print, primers, and lamination adhesives together against the actual collection, sorting, and recycling route. Compatibility can differ between natural and colored recyclate applications.
A RecyClass technical review reported specific cold-seal/release-coating evaluations for flexible PP structures. The reported ratings below apply to the tested formulations and boundary conditions, not to all coatings at those percentages:
Tested system and loading | Colored flexible PP stream | Natural flexible PP stream |
|---|---|---|
Natural-rubber/acrylic cold seal, up to 6.7% of structure weight | Full compatibility reported | Limited compatibility reported |
Polyamide-based release lacquer, up to 5.2% of structure weight | Full compatibility reported | Limited compatibility reported |
Discoloration effects on recyclate were a relevant consideration. These observations should be checked against the latest applicable RecyClass guidance and assessment scope before being used for an actual recyclability claim. PP results do not automatically transfer to PE.
The ink comparison matters here too. A thermoplastic LEP film and an NC/PU-based flexo film introduce different polymers and constituents to the recycling stream. Identical base-film composition cannot justify assuming identical recyclate performance for the two printed packages. Validate the finished structure.
Cold sealing can reduce deliberate sealing-jaw heat input and can support high output rates, but it also requires adhesive manufacture, coating, and drying, with possible impacts on recycling. Neither cold seal over heat seal nor LEP over flexography should be declared universally more sustainable without a system-level evaluation that includes energy, waste, product preservation, materials, logistics, and end-of-life.
19. Engineering Perspective: Qualify the Interfaces, Not Just the Individual Products
Cold seal is an interface system. Correctly treated substrate does not guarantee adhesive anchorage. Good ink adhesion does not guarantee lacquer anchorage. Low initial release force does not guarantee resistance to blocking after storage. Strong laboratory seals do not guarantee complete seams at full packaging-machine speed.
LEP adds a printed thermoplastic film that forms and transfers differently from conventional flexographic ink. That may change the relevant contact and lamination interfaces, but it does not change cold seal's basic bonding principle. Success requires identifying each critical interface, defining acceptance tests for it, and verifying that the complete package remains functional through printing, coating, winding, storage, converting, and use.
Conclusion: Make the Right Bond—and Prevent the Wrong One
Cold-seal packaging offers a useful pressure-based sealing mechanism, particularly for products sensitive to heat or when machine architecture favors cold sealing. It is not simply an adhesive substitution for heat sealing. It is a coordinated system of cohesive coating, release lacquer, substrate, printing layers, lamination materials, and production conditions.
LEP can add high-quality digital graphics and manufacturing flexibility; its polymeric ink film calls for careful evaluation of primer, coating, thermal history, and lamination interfaces. Flexography offers mature, formulation-specific packaging inks and many established compatibility pathways, but it requires equally disciplined control over drying, additives, and the ink/release system. In both cases, conclusions should be based on real seal strength, release behavior, failure mode, package integrity, aging, and applicable food-contact and recycling requirements.
A successful cold-seal package is not defined only by the moment two adhesive layers join under pressure. It is defined by the ability to create the intended bond—and avoid unintended bonding—reliably throughout the package's life.
Technical References and Further Reading
- ASTM International. ASTM F88/F88M, Standard Test Method for Seal Strength of Flexible Barrier Materials. Consult the current edition and applicable specimen/test configuration.
- ASTM International. ASTM F3039, Standard Test Method for Detecting Leaks in Nonporous Packaging or Flexible Barrier Materials by Dye Penetration. Verify package/method applicability.
- HP. Technical background on Liquid Electrophotography (LEP) and heated intermediate-blanket ink transfer; consult platform- and ink-specific documentation for application qualification.
- Flexographic Technical Association (FTA). Technical publications on flexible-packaging ink chemistry, solvent/water-based printing, drying and lamination.
- Bostik. Technical guidance on cold-seal adhesive issues including blocking, anchorage, scumming and application stability.
- Lubrizol. Technical information on cohesive cold-seal systems and release-lacquer formulation and compatibility.
- RecyClass. Technical review of cold seals and releasable lacquers for flexible PP (reported March 2026) and current Design for Recycling Guidelines. Reported performance applies only to the tested systems.
- BASF and HP Indigo. Publicly described cooperation on compatible adhesive solutions for digitally printed flexible packaging; the details do not imply universal approval of adhesive/ink combinations.
- European Parliament and Council. Regulation (EC) No 1935/2004 concerning materials intended to come into contact with food.
- European Commission. Regulation (EC) No 2023/2006 on good manufacturing practice for materials and articles intended to come into contact with food.
Engineering note: Material formulations, press configurations, food-contact requirements, and recycling guidance vary by market and can change. The schematic structures, examples, and comparative tests above are educational engineering methods—not universal operating setpoints, supplier approvals, or regulatory certifications.